EN
 DE
 FR
 ES
 RU
 JA EN DE FR ES RU JA
Explore our high-performance membrane switches engineered for extreme durability, IP67/IP68 ingress protection, and chemical resistance. Designed specifically for industrial machinery, medical devices, and maritime control systems operating in harsh tropical climates.
As the cornerstone of Central America’s international commerce, the Colón market—anchored by the Colón Free Zone (Zona Libre de Colón - ZLC) and world-class deepwater container terminals such as Manzanillo International Terminal (MIT), Cristóbal, and Colón Container Terminal (CCT)—demands electronic components engineered to uncompromising standards. Serving as a crucial logistics and assembly node for Latin America, industrial original equipment manufacturers (OEMs), re-export aggregators, and maritime system integrators in Colón face unique environmental and operational challenges.
Operating within a high-humidity tropical maritime zone characterized by ambient humidity exceeding 85%, saline atmospheric conditions, and intense solar exposure, equipment deployed in Colón requires superior human-machine interface (HMI) durability. Standard mechanical switches frequently fail due to contact oxidation, moisture ingress, and substrate degradation. High-performance membrane keypads, backlit capacitive touch panels, and custom silicone rubber switches manufactured with IP67/IP68 perimeter gas-sealing technology have emerged as the industry standard for ensuring uninterrupted operational longevity.
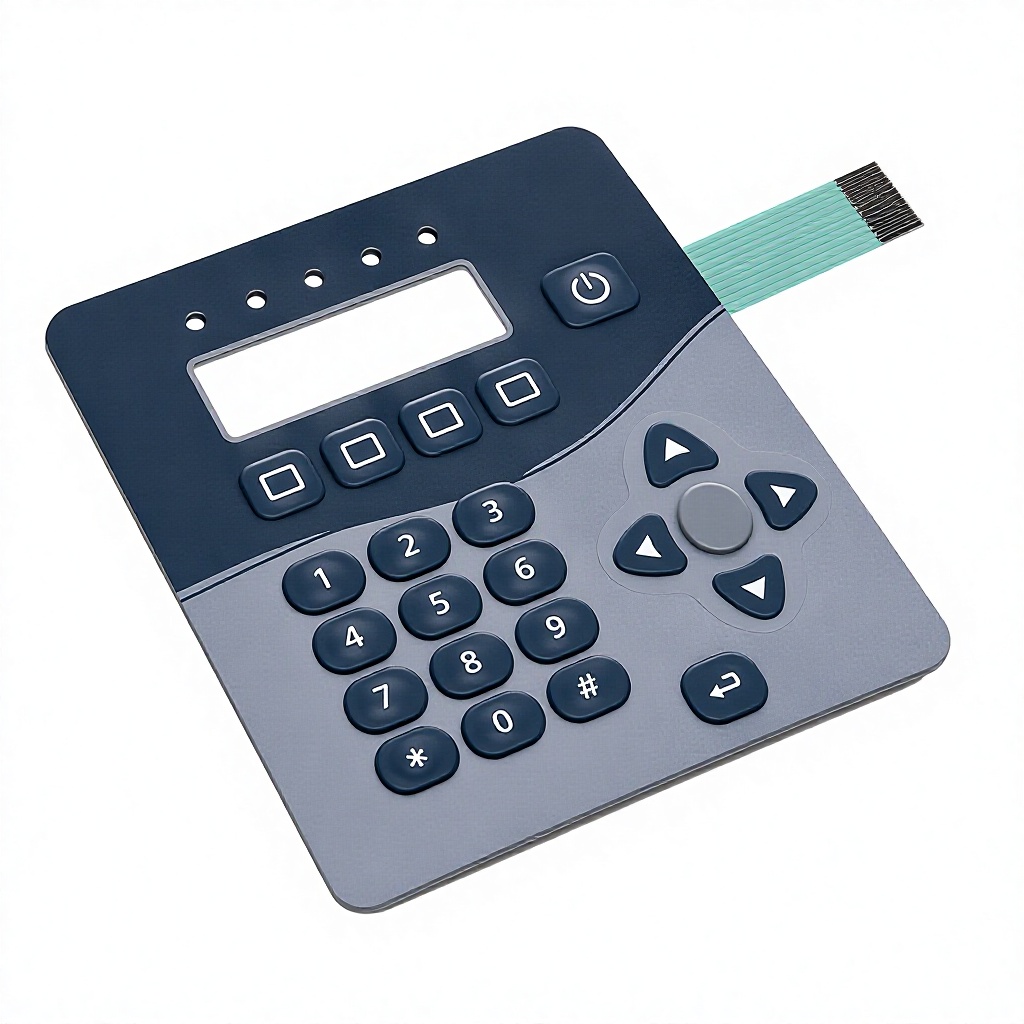
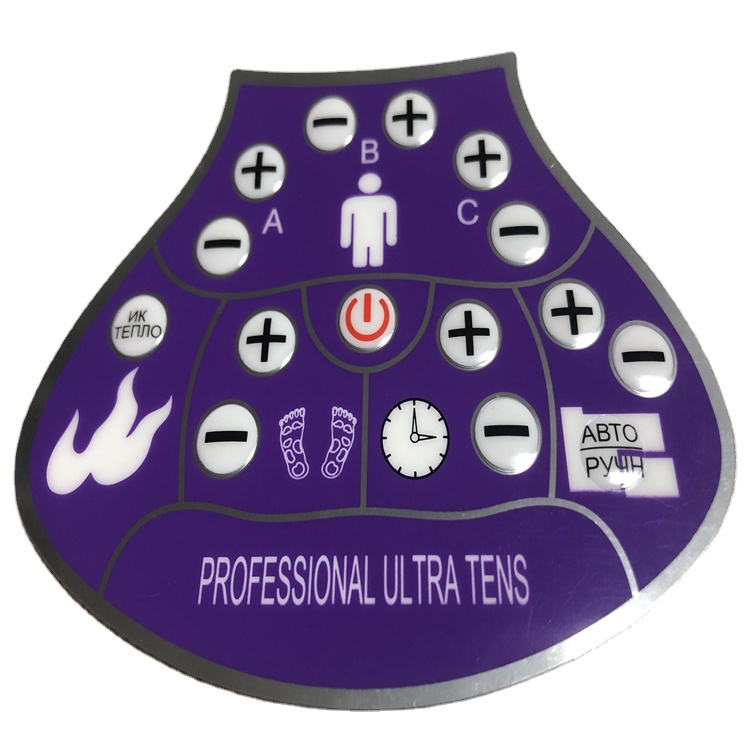
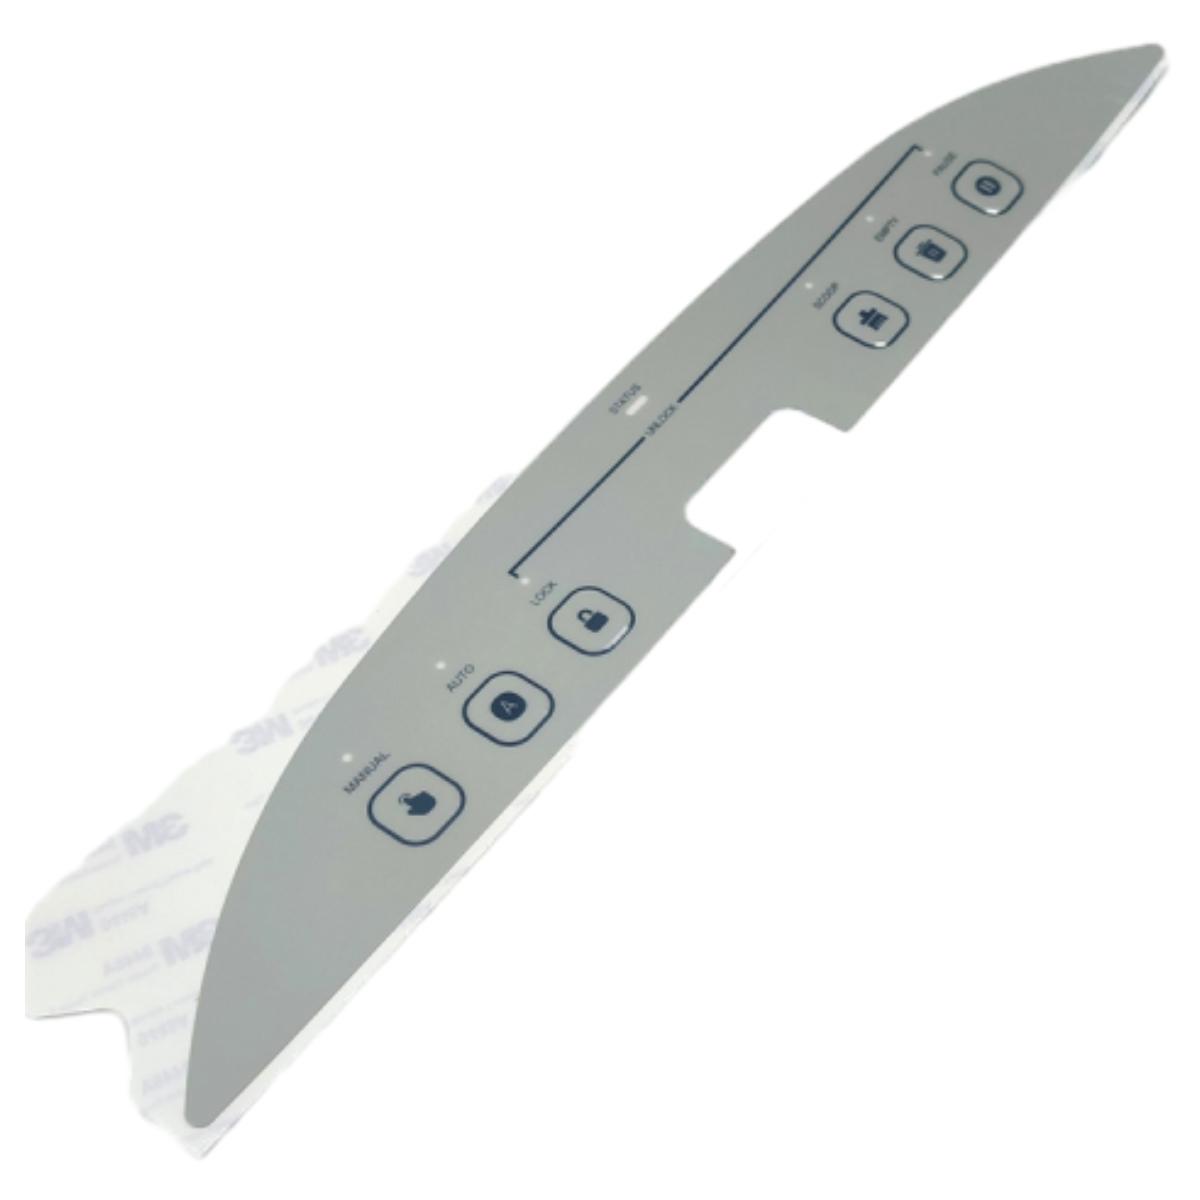
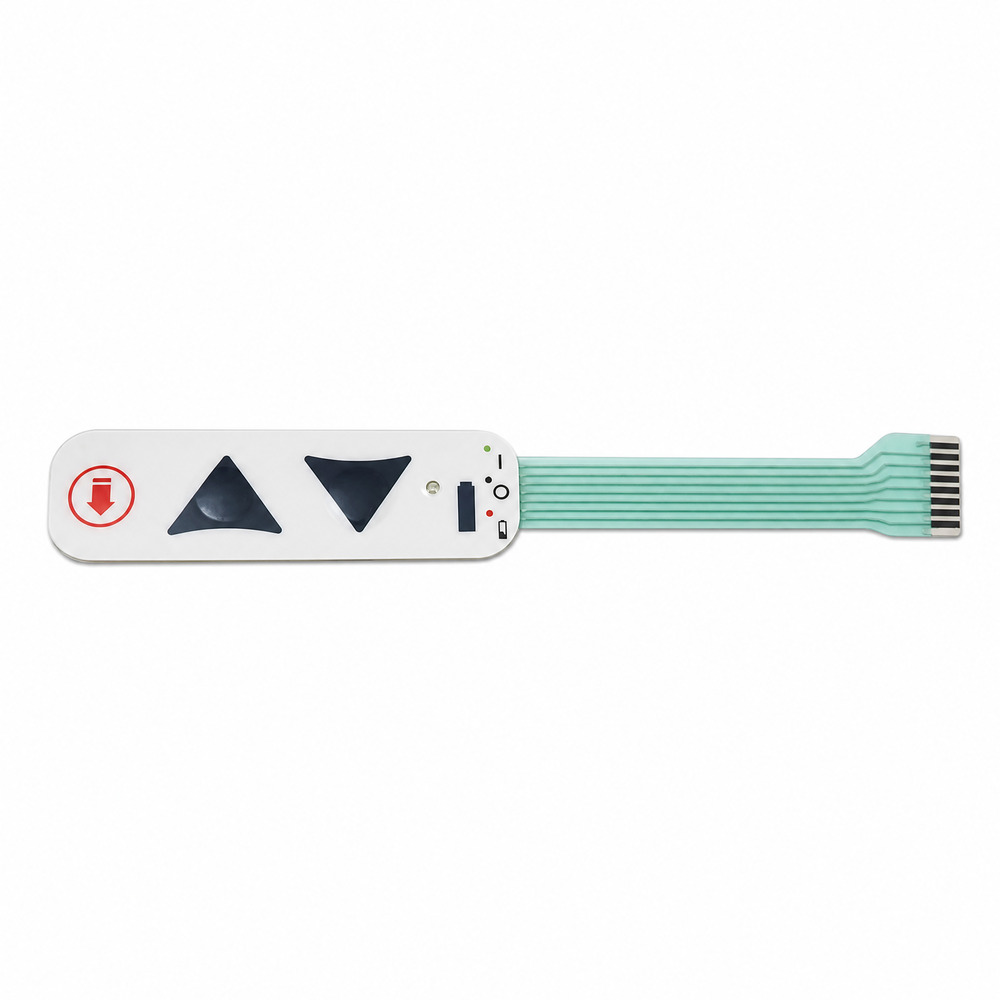
A custom membrane switch is a precision multi-layer assembly that combines functional aesthetic graphic overlays, flexible printed circuits, tactile feedback elements, and pressure-sensitive structural adhesives into a low-profile interface. Understanding the physical layer stack-up is essential for procurement managers and design engineers seeking maximum reliability in the Colón regional trade hub.
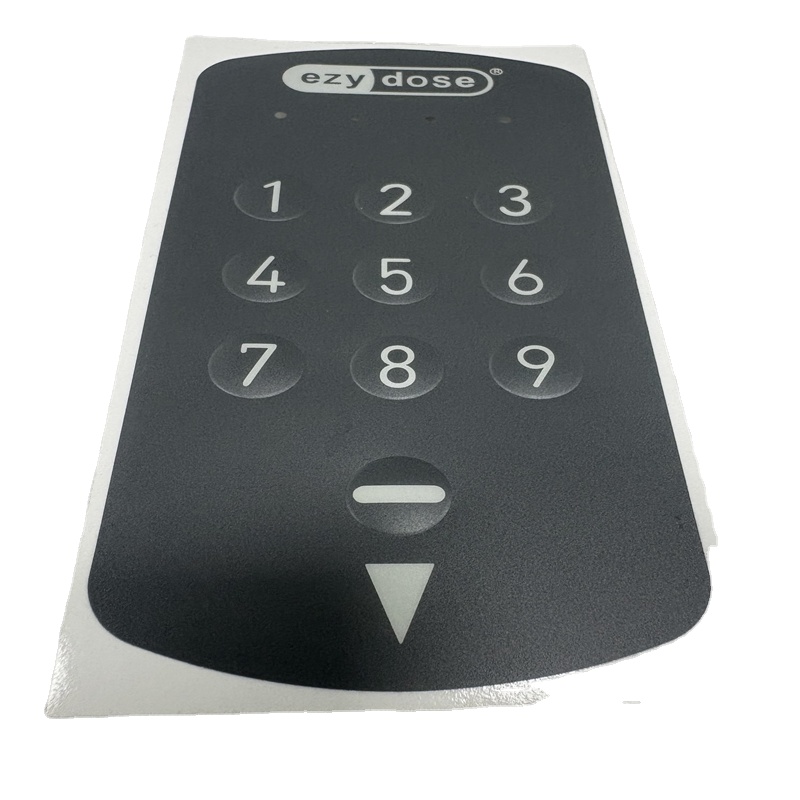
Utilizing premium Autotex XE UV-resistant polyester (PET) and hard-coated polycarbonate (PC) materials ranging from 0.125mm to 0.25mm. Reverse screen-printed or high-resolution digital UV printed to guarantee complete scratch, chemical, and saltwater resistance under tropical marine exposure.
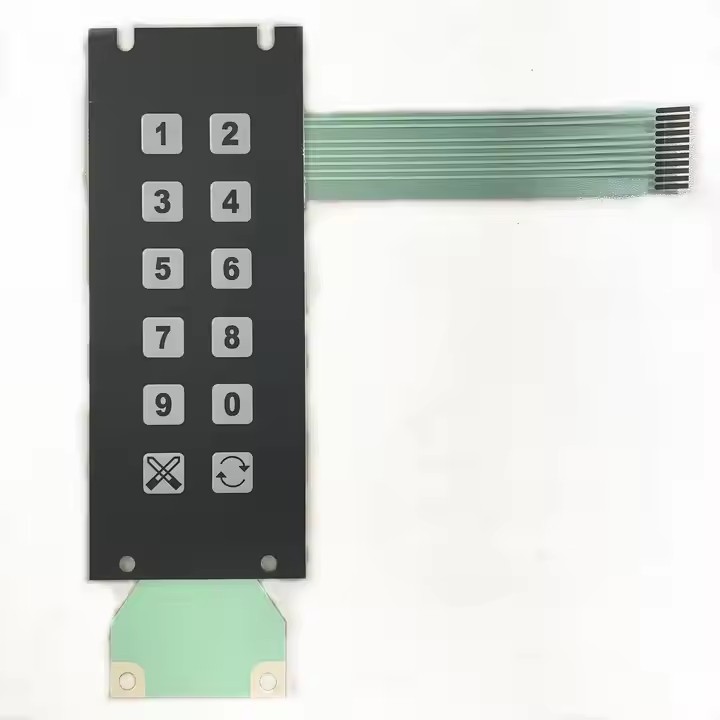
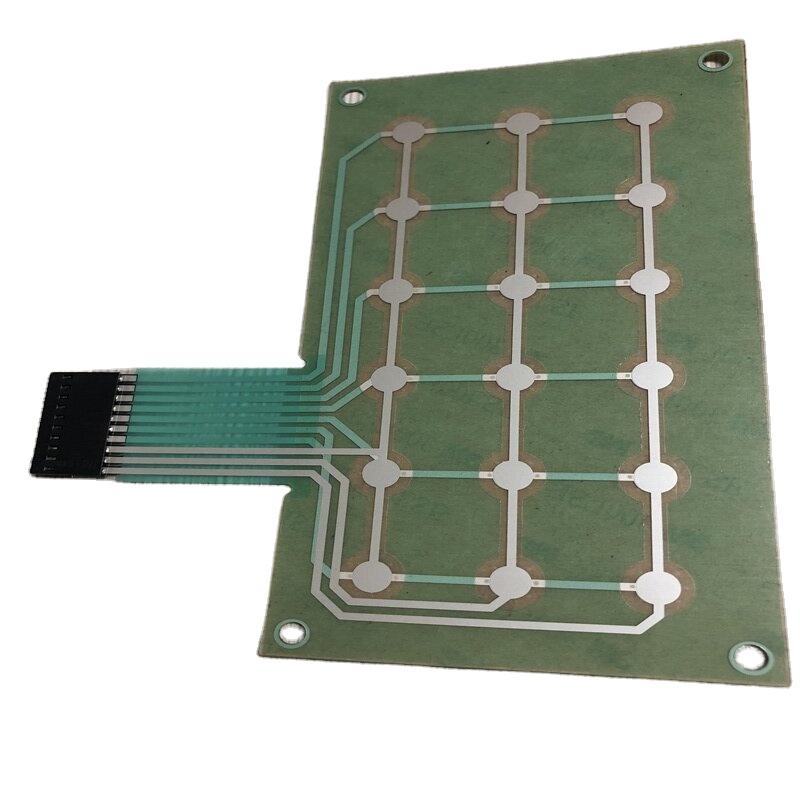
Engineered with conductive silver ink or copper-clad polyimide flexible printed circuits (FPC). For heavy industrial applications, rigid FR-4 PCB backers allow direct surface-mount technology (SMD) integration of LEDs, resistors, microcontrollers, and locking connectors.
Incorporating stainless-steel metal domes (180g to 350g snap force) or thermoformed polydomes for distinct tactile actuation. Sealed with 3M 467MP, 468MP, or 300LSE acrylic adhesives, establishing IP67 water, dust, and anti-fungal barrier protection.
Our custom membrane keypads and control panel overlays are tailored to power critical infrastructure, commercial hubs, and re-export manufacturing lines operating throughout Panama and Central America.
Colón’s world-famous port terminals rely heavily on heavy-duty crane controllers, vessel bunkering automation systems, and terminal tractor HMI screens. Our waterproof membrane keypads utilize UV-hardened polyester overlays and sealed metal-dome contacts to withstand constant salt spray, diesel fumes, and 24/7 high-impact outdoor usage without button fatigue.
As the largest free trade zone in the Western Hemisphere, ZLC houses thousands of commercial display hubs, automated warehouse terminals, and customs verification kiosks. Non-tactile flat keyboards and smooth, wipe-clean capacitive touch keypads provide an elegant, anti-microbial, easy-to-sanitize surface for continuous public and warehouse operation.
Along the Panama Canal bunkering routes, petroleum and chemical fuel dispensers require intrinsically safe, explosion-resistant control interfaces. Reverse-printed polycarbonate overlays backed with 3M 468MP high-tack adhesive resist hydrocarbon splashes, solvent cleanings, and extreme heat, ensuring legibility and safety over decades.
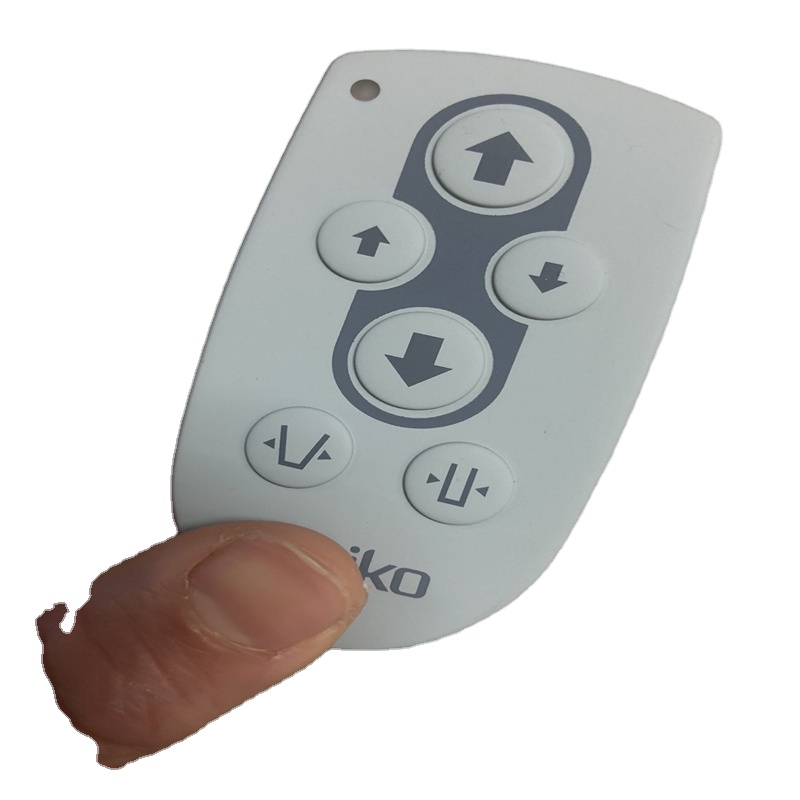
Panama serves as a central redistribution channel for diagnostic healthcare devices across Latin America. Our silicone rubber keypads with backlit LED indicators and tactile metal domes meet rigid medical-grade biocompatibility standards, offering sealed liquid resistance against aggressive clinical disinfectants and fluids.
Procurement patterns within the Colón market reflect broader global supply chain transformations. Key industry trends driving the adoption of custom membrane keypads include:
Global manufacturing realignments have elevated Colón as a high-value light assembly and customization hub. Local assembly teams require fast-turnaround modular HMI keypads that can be easily mounted onto localized equipment housings.
Industrial gear in logistics parks is rapidly adopting smart monitoring. Hybrid membrane switches featuring embedded SMD LEDs, dead-front illuminated windows, and flexible tail connectors seamlessly interface with modern IoT telemetry boards.
High operational efficiency demands long-life switches. By replacing mechanical switches with 1,000,000+ cycle rated membrane keypads utilizing zero-power capacitive or silver circuit layers, equipment downtime and electronic waste are drastically minimized.
Compare key design options to optimize your membrane switch design for the Colón region’s tropical marine environment.
| Feature Parameter | Autotex XE Polyester (PET) | Hard-Coated Polycarbonate (PC) | Silicone Rubber Keypad Integration |
|---|---|---|---|
| UV & Weathering Resistance | Outstanding (Designed for Outdoors) | Moderate (Requires UV Coating) | Excellent Elastomeric Resistance |
| Chemical & Solvent Protection | Resists Acids, Alcohols, Fuels | Resists Mild Cleaners, Oils | High Chemical Stability |
| Actuation Lifecycle | > 5,000,000 Cycles | > 1,000,000 Cycles | > 2,000,000 Cycles |
| Flexural Fatigue Life | Extremely High Resistance | Moderate Resistance | N/A (3D Molded Keys) |
| Ingress Sealing Capabilities | IP67 / IP68 Perimeter Sealed | IP65 / IP67 Sealed | IP68 Full 3D Enclosure Gasket |
| Best Colón Application | Port Cranes, Outdoor Fuel Pumps | Indoor POS Kiosks, Medical Overlays | Rugged Handhelds, Heavy Machinery |
Established in 2003, Dongguan Ravo Electronics Co., Ltd. is a premier custom membrane switch manufacturer based in Dongguan, China. Combining advanced cleanroom engineering, in-house silk-screen printing, CNC die-cutting, and 100% automated electrical testing, we deliver precision HMI solutions to over 50 countries.
Our dedicated DFM (Design for Manufacturability) engineering team analyzes your CAD drawings, Pantone artwork, and circuit schematics within 2 hours, offering optimized stack-up solutions to eliminate costly production delays.
Whether you need a single prototype unit for initial testing or 100,000 units for mass production, our flexible tooling and digital laser cutting capabilities support rapid prototyping without high initial setup costs.
All production processes operate under strict ISO 9001 quality management systems. Materials used—including 3M adhesive tapes, Autotex PET films, and conductive inks—are fully RoHS and REACH certified for seamless import into Central and South America.
Get immediate technical and logistical answers regarding custom membrane switch procurement, customs entry through Panama, and engineering specifications.
Partner with Dongguan Ravo Electronics Co., Ltd. for engineering excellence, rapid DFM feedback within 2 hours, and high-reliability HMI keypads tailored to your exact operational environment.
Get Catalog