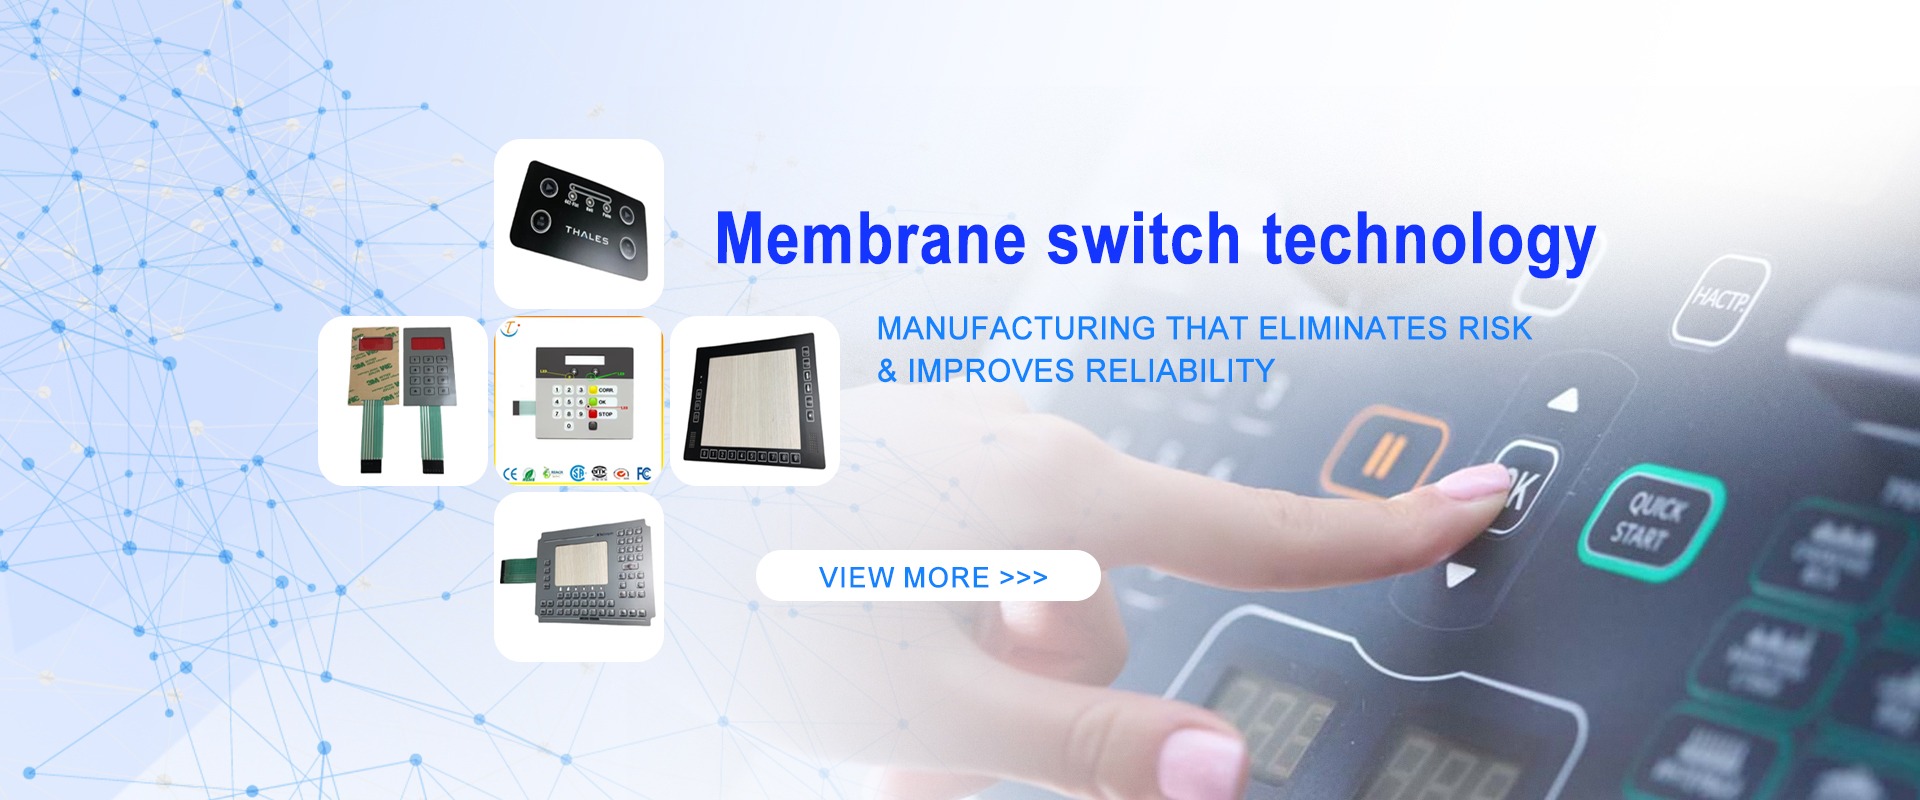
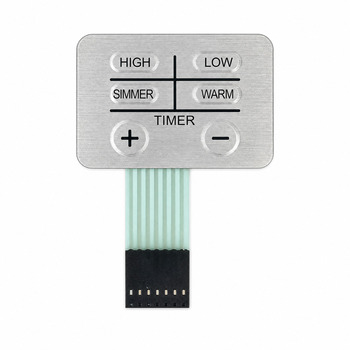
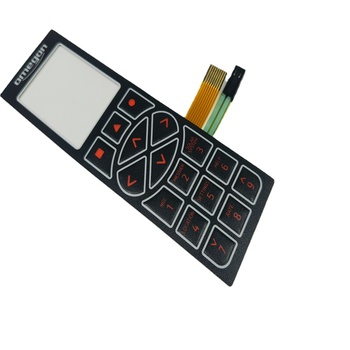
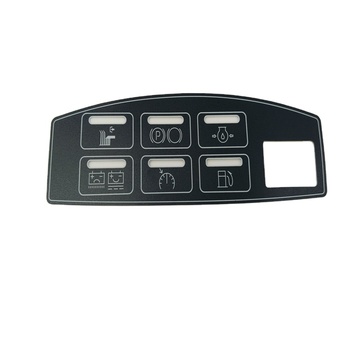
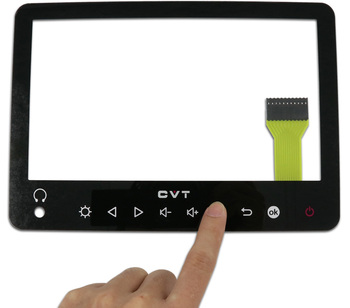
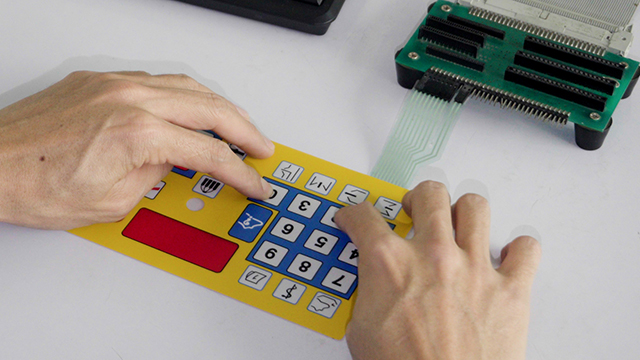
When mission-critical human-machine interfaces encounter corrosive saline mists, aggressive medical chemical sterilizations, torrential outdoor rainstorms, or high-pressure food-processing washdowns, standard off-the-shelf control panels fail catastrophically. As global industrial designers, biomedical engineers, and procurement directors evaluate human-machine interface (HMI) hardware, the Waterproof Membrane Keyboard has emerged as the definitive benchmark for impenetrable liquid resistance, ergonomic precision, and extended cyclic durability.
Engineered by Dongguan Ravo Electronics Co., Ltd. (operating from Fenggang Town, Dongguan since 2003), our sealed membrane interface solutions unify advanced high-barrier polymer films, perimeter pressure-sensitive adhesive barriers (3M 200MP / 300LSE), hermetically encapsulated tactile metal domes, and potted tail terminations. Whether your system mandates IP65 splash resistance, IP67 temporary submersion, or IP68 continuous immersion endurance, Ravo brings 20+ years of vertical manufacturing prowess to transform your 2D/3D CAD specifications into field-proven, zero-defect hardware.
Rapid Engineering DFM Review • 14 Years Verified International Export
Engineering Mechanics
How an Industrial Waterproof Membrane Keyboard Achieves Hermetic Sealing
A deep dive into layer stacks, adhesive bonding chemistry, hydrophobic pressure equalization, and tail potting mechanics.
1. Non-Permeable Overlays
Utilizing high-grade biaxially oriented PET (Autotex XE / Autotype) or hard-coated PC (Lexan HP92W) with chemical-resistant, UV-stabilized, and antimicrobial surfaces that withstand alcohol wipes, fuels, and acidic industrial sprays.
2. Perimeter Gasket Isolation
Unlike commercial keyboards that breathe ambient moisture, our waterproof keyboards utilize continuous boundary gaskets die-cut from high-shear 3M acrylic transfer tapes, forming an impenetrable ring around the circuit envelope.
3. Hermetic Tail Waterproofing
Moisture capillary entry via the connector tail is completely nullified through rear potting, UV-cured urethane gaskets, flexible printed circuit (FPC) polyimide terminations, or ultrasonic weld collars.
In standard consumer keyboards, fluid ingress occurs through switch gaps, capillary seams, or ambient venting channels necessary for key actuation. In contrast, an industrial Waterproof Membrane Keyboard manufactured by Dongguan Ravo Electronics Co., Ltd. treats ingress protection as a total structural paradigm. Below is the anatomy of a genuine IP67/IP68 sealed multi-layer interface:
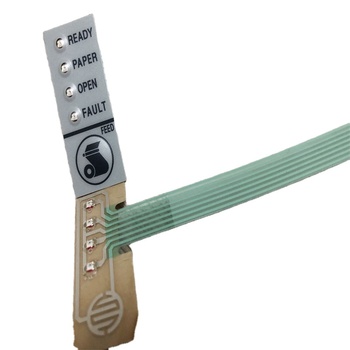
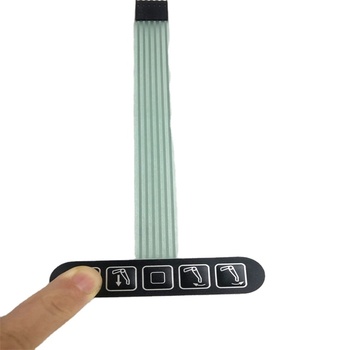
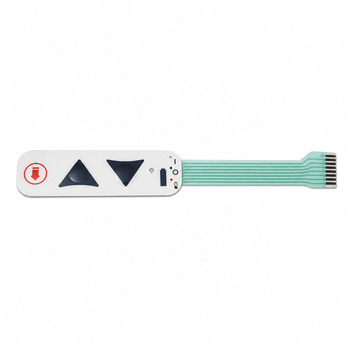
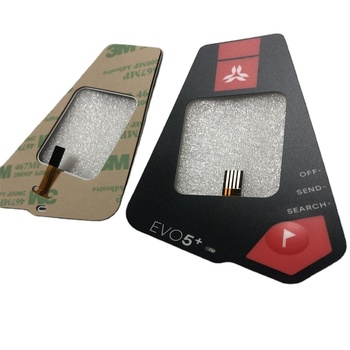
Explore our most trusted production architectures built for demanding industrial automation, harsh weather outdoor environments, medical instrumentation, and high-pressure food processing machinery.
Emerging Technology Trends in Waterproof Membrane Keyboards
How the convergence of smart materials, capacitive sensing, and optical integration is redefining modern waterproof HMI hardware.
1. Hybrid Capacitive-Membrane Surface Convergence
Traditional tactile domes are increasingly paired with seamlessly printed capacitive touch sliders, gesture fields, and zero-force touch keys beneath unified waterproof graphic foils. This eliminates mechanical switch fatigue while maintaining full IP68 water sealing without physical seams or crevices where bacteria and fluids collect.
Modern defense, marine, and medical equipment require dynamic display-overlay assemblies. The integration of optically clear adhesives (OCA) directly binding waterproof PET overlays to TFT LCD displays prevents internal condensation, fogging, and refractive washouts under direct sunlight.
3. Self-Equalizing Micro-Venting Membranes
As equipment transitions between sub-zero refrigerated chambers and humid outdoor worksites, rapid thermal shifts cause internal air expansion, causing false triggering or dome suction. The next-generation waterproof membrane switches utilize hydrophobic, oleophobic PTFE venting membranes allowing vapor venting without letting a single droplet of moisture penetrate.
4. FPC Copper Circuits Replacing Silver-Ink in Harsh Sites
While screen-printed silver ink remains cost-effective for standard indoor controls, the rapid expansion of electric vehicle charging stations, mining controllers, and maritime panels is accelerating the adoption of polyimide Flexible Printed Circuits (FPC). Copper tracks completely eliminate silver electromigration under persistent electrical bias in high-humidity zones.
Strategic Sourcing Insights
Future Global Procurement Trends: Sourcing Resilient Waterproof Keyboards
What international supply chain leaders and OEM buyers must prepare for over the next 3 to 5 years.
1. Total Cost of Ownership (TCO) vs. Initial Unit Price
Procurement departments are moving away from evaluating membrane keyboards purely on BOM cost. A field failure caused by water ingress costs orders of magnitude more in warranty recalls and client reputation. Investing in high-grade 3M adhesive gaskets, Autotex XE films, and 100% electrical/continuity testing during factory production delivers massive long-term ROI.
2. Agile Tooling & Rapid Micro-Lot Prototyping
Global electronics OEMs demand faster time-to-market. Factory partners who offer in-house laser cutting, digital proofing, and prototype runs from as few as 1 to 10 pieces—without charging thousands of dollars in permanent hard tooling upfront—are winning long-term OEM contracts. Dongguan Ravo Electronics excels at this agile NPI (New Product Introduction) workflow.
3. Stricter Environmental & Chemical Compliance (RoHS 3, REACH, Halogen-Free)
Regulatory scrutiny across Europe and North America requires end-to-end trace documentation. Buyers demand full declaration that conductive inks, dielectric spacers, transfer adhesives, and plasticizers are free of PFOS/PFOA, heavy metals, and restricted phthalates. Sourcing from verified manufacturers with certified raw material pipelines is non-negotiable.
4. Direct Factory Engineering Alignment via AI & Real-Time DFM
Overseas procurement teams are bypassing intermediate trading agents in favor of direct engineering access. With engineering response turnaround times benchmarked at ≤2 hours, buyers work directly with manufacturing technicians in Dongguan to optimize trace routing, dome actuation forces, and tail exits before steel cutting dies are fabricated.
Dongguan Ravo Electronics Co., Ltd. — Two Decades of Precision HMI Excellence
Dongguan Ravo Electronics Co., Ltd. is a leading professional manufacturer of custom waterproof membrane switches, PC/PET panels, flexible circuit boards (FPC), aluminum nameplates, copper panels, dimensional signs, silicone keypads, and silicone rubber gifts. Located in Fenggang Town, Dongguan City, Guangdong Province, our enterprise was established in 2003 as the premier subsidiary of Tianjin Industry (HK) Co., Ltd. In addition, our sister company Shenzhen Jingzhicheng Electronics Co., Ltd. is specialized in the production of high-performance conductive buttons, Zebra connector stripes, mobile phone components, and engineered waterproof rings.
Through more than two decades of focused industrial expansion, Dongguan Ravo Electronics Co., Ltd. has developed from an initial technical workshop of 8 people into a vertically integrated manufacturing powerhouse with over 300 skilled employees and an expansive plant area exceeding 12,000 square meters.
Our company possesses formidable R&D technology, automated high-precision screen-printing equipment, class-1,000 cleanroom assembly lines, advanced CNC laser cutting systems, and an uncompromising ISO 9001 certified quality management system. With the tireless dedication of our engineering staff, our products are widely exported and enthusiastically trusted throughout Europe, North America, Australia, and East Asia.
Trusted by Global Leaders:LINAKFLEXTRONICSLGCASIOEARLY LIGHT
From graphic prepress, color-matching, and screen printing to CNC die-cutting, metal dome pick-and-place, and final ultrasonic testing, all stages are kept in-house under controlled atmospheric conditions.
Fast ≤2h Engineering Response & DFM
Our senior mechanical and electrical engineers review your technical drawings (CAD, DWG, DXF, Gerber, STEP, AI) and furnish optimization proposals within two hours, cutting project lead times by weeks.
End-to-End Waterproof Sealing Expertise
Leveraging deep R&D with sister enterprise Shenzhen Jingzhicheng Electronics Co., Ltd. (specialized in silicone waterproof rings & conductive keys), we craft customized hermetic sealing rings and waterproof gaskets.
Strict 100% Electrical & Life Cycle Testing
Every single keyboard undergoing shipment is subjected to automated continuity testing, contact resistance checks (<100Ω standard), loop short checks, and sample actuation life cycle stress testing.
14 Years Verified International Exporting
Consistently maintaining a 98.59% customer response rate, robust export logistics packaging, and RoHS/REACH compliance documentation across Europe and North America.
Frequently Asked Questions on Waterproof Membrane Keyboards
Comprehensive answers addressing the key design parameters, testing standards, sealing mechanisms, and procurement requirements frequently queried by global hardware engineers and international sourcing directors.
What is the technical difference between an IP65, IP67, and IP68 waterproof membrane keyboard?
IP65: Certified protection against total dust ingress and low-pressure water jets (6.3mm nozzle) projected from any direction. It features standard continuous perimeter adhesive seals and is ideal for equipment subjected to occasional hose sprays and dust storms.
IP67: Withstands complete immersion in water up to 1 meter depth for 30 minutes. Achieved via continuous acrylic transfer gaskets (e.g., 3M 300LSE/468MP), hermetically sealed internal venting channels, and epoxy/polyurethane potted tail exit ports.
IP68: Designed for continuous submersion beyond 1 meter under specified hydraulic pressure. This demanding build incorporates flexible printed circuits (FPC), welded perimeter seams, compression-molded silicone outer gaskets, and hydrophobic micro-vent equalizers.
How do you prevent the tail (flexible cable) exit from leaking water into the keyboard or host enclosure?
The tail transition represents the single highest risk zone for capillary water leakage in membrane switches. At Dongguan Ravo Electronics Co., Ltd., we mitigate this through several proven engineering methodologies:
Bottom-Exit Sealed Apertures: Routing the tail through a die-cut hole within the mounting baseplate rather than exiting the perimeter edge, completely encapsulated under continuous 3M adhesive gaskets.
UV-Cured Epoxy / Polyurethane Potting: Encapsulating the exit neck in high-adhesion urethane resin that bonds directly to the PET/FPC tail and enclosure walls.
Co-Molded Silicone Gasket Boots: Pairing the membrane switch with a silicone keypad bezel featuring integrated O-rings or compression lips that form a watertight barrier when bolted down.
How is internal air pressure equalized during rapid temperature drops without drawing in moisture?
When a membrane switch is keyed, air must compress or shift. If a completely airtight keyboard experiences rapid ambient temperature drops (e.g., equipment transferred from a heated truck into a sub-zero shipping freezer), the internal air volume contracts. Without proper venting, this vacuum can suck moisture through microscopic weaknesses or cause tactile domes to collapse spontaneously.
To prevent this, Ravo utilizes two solutions: (1) Internal key-to-key matrix venting channels, circulating air displacement only between sealed dome chambers without external atmosphere exchange; and (2) Hydrophobic/Oleophobic PTFE micro-porous breathable membrane patches (similar to Gore-Tex). These vents allow free bidirectional airflow for barometric balance while blocking liquid water droplets and oil mists up to 3 bar hydrostatic pressure.
Which mounting adhesives are selected for textured plastics vs. powder-coated metals?
The integrity of a waterproof membrane keyboard depends directly on its surface energy adhesion to the host chassis:
High Surface Energy (HSE) Substrates (Aluminum, Stainless Steel, Polycarbonate): We employ 3M 467MP (0.05mm) or 3M 468MP (0.13mm) 200MP acrylic adhesives. They offer exceptional chemical resistance, high shear strength, and thermal resilience up to 200°C.
Low Surface Energy (LSE) Substrates (Polypropylene, Polyethylene, Powder-Coated Metal Enclosures): We select 3M 300LSE high-tack laminating adhesives. 3M 300LSE is explicitly formulated to grip oily, rough, or powder-coated surfaces, preventing edge peel and water creep under humid environments.
Can our custom waterproof keyboard incorporate tactile clicks and LED backlighting simultaneously?
Yes. We routinely engineer hybrid stackups incorporating four-legged stainless steel tactile metal domes (providing 250g to 450g tactile snap feedback and 1,000,000+ cycle life) with surface-mount 0603 or 0805 low-profile LEDs.
To preserve waterproof integrity, the LEDs are either mounted directly onto an internal FPC polyimide layer with conductive silver epoxy and encapsulated in clear dome potting, or back-illuminated through an ultra-thin Light Guide Film (LGF). The graphic overlay features translucent windows and opaque printed ink masks for zero light bleed.
How does Ravo test and certify the waterproof performance before dispatching orders?
Quality control at Dongguan Ravo Electronics Co., Ltd. follows rigorous, standardized verification protocols:
Vacuum Decay Leak Testing: Verifying airtight perimeter integrity on sample units to ensure zero micro-porosities.
Submersion Tank Testing: 1-meter immersion testing for 30 minutes in accordance with IEC 60529 (IPX7/IPX8 validation).
100% Automated Electrical Continuity: Contact resistance (≤100Ω), insulation resistance (≥100MΩ at 100V DC), and dielectric withstand tests ensuring zero conductive bridging.
What are the prototyping MOQs and production lead times at Dongguan Ravo Electronics?
To support agile prototyping and fast-track NPI cycles for international engineers, our minimum order quantity for rapid prototypes starts at just 1 to 10 pieces. Standard prototypes are engineered, laser-cut, and dispatched within 5 to 10 working days following 2D CAD signoff.
Mass production volumes typically range from 100 to 50,000+ pieces, with delivery turnaround times spanning 15 to 22 working days. Our engineering department operates with a verified average response time of ≤2 hours for RFQs and technical questions.
Ready to Engineer Your Custom Waterproof Membrane Keyboard?
Send your drawings, dimensional requirements, or target IP rating to our senior technical team. Receive a complete DFM manufacturability analysis, layer stack proposal, and transparent factory direct quotation within 2 hours.
 EN
 DE
 FR
 ES
 RU
 JA