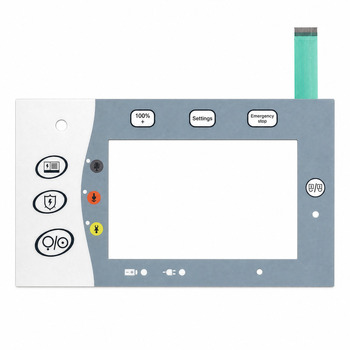
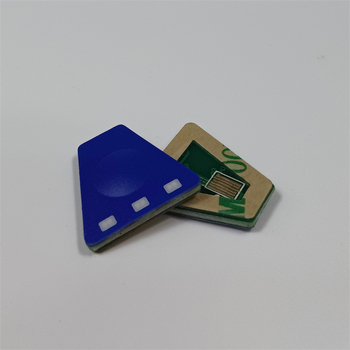
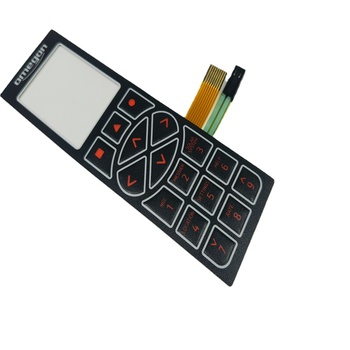
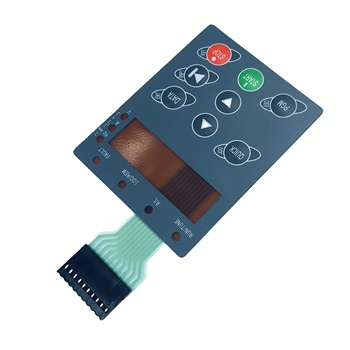
Tactile Rim-Embossed Industrial Panel
- Over 1,000,000 metal dome snap cycles
- Rim-embossed perimeter for positive fingertip indexing
- IP65 moisture-proof 3M acrylic adhesive stack
- High-contrast anti-glare matte textured finish
In an era driven by automated manufacturing, medical diagnostics, and smart IoT enclosures, the demand for resilient human-machine interfaces has never been higher. Procuring a custom embossed membrane switch panel is no longer just about selecting a graphic overlay; it requires a deep technical balance of mechanical actuation travel, selective surface embossing geometry, chemical resistance, hermetic sealing up to IP67, and flexible circuit stability. Dongguan Ravo Electronics Co., Ltd. provides complete vertically integrated engineering—from rapid prototype validation to high-volume multi-layer lamination.
Understanding the interplay between thermal tooling, graphic foil elasticity, snap ratio, and environment-sealed structural design.
When procurement specialists and hardware designers search for an embossed membrane switch panel, their primary objective is delivering flawless sensory feedback to human operators. Flat, non-tactile surfaces create cognitive uncertainty during critical inputs. By thermo-forming or cold-forming the graphic film, distinct geometries are created:
Rim Embossing (Border Emboss): Frames the perimeter of the key with a raised 0.25mm to 0.50mm bead. This provides precise finger location without putting continuous stress on the face of the graphic foil, making it ideal when utilizing tactile stainless-steel metal domes underneath.
Pillow Embossing (Pad Emboss): Elevates the entire key area into a uniform flat plateau. It offers a smooth, generous tactile surface that is comfortable for repeated finger presses, widely specified in medical instrumentation and consumer kitchen controls.
Dome Embossing (Polydome Construction): Creates an integrated PET tactile dome in the film itself. In applications sensitive to cost and vertical height, a polydome switch achieves tactile snap without inserting metal domes, lowering BOM costs while providing up to 500,000 actuation cycles.
Combining precise hydro-forming or matched CNC steel-and-copper tooling ensures zero micro-cracking across printed circuit traces, retaining substrate integrity and preventing silver ink migration even in high-humidity operating conditions.
We evaluate your operating environment to determine whether biaxially oriented PET (Autotex XE/V200) for millions of flex cycles or optical-grade Polycarbonate (Lexan) with UV stabilizer is required.
Continuous perimeter 3M 467MP or 3M 9448A acrylic adhesive rings prevent the entry of sanitizers, airborne grease, moisture, and fine dust particles into contact cavities.
Custom stainless-steel four-leg metal domes provide actuation forces between 180g and 450g with audible feedback, ensuring positive contact even when operators wear heavy work gloves.
Full-coverage printed silver or carbon ESD grid layers divert static discharges up to 15kV away from sensitive internal microcontrollers to dedicated grounding pins.
Discover our field-tested architectures optimized for harsh operating conditions, surgical cleanability, and compact consumer electronics.
How next-generation material science, smart integration, and digital supply chains are reshaping HMI procurement.
Designers are pairing capacitive touch sliding controls with raised embossed mechanical emergency buttons on a single overlay foil, combining sleek aesthetics with physical safety interlocks.
Bulky backlighting units are being replaced with ultra-slim 0.125mm optical LGF films coupled with microscopic side-fire LEDs, guaranteeing uniform luminance across keys with minimal battery consumption.
Medical and public-access equipment requires advanced polyester films containing active silver ion additives that eradicate 99% of surface pathogens while resisting micro-scratches from heavy clinical usage.
Global procurement teams demand high-speed DFM turnaround within 2 hours and 100% automated optical inspection (AOI) to eliminate pinholes and registration errors before volume stamping.
Founded in 2003 in Fenggang Town, Dongguan City, Guangdong Province, Dongguan Ravo Electronics Co., Ltd. has evolved from an 8-person workshop into a vertically integrated manufacturing facility covering more than 12,000 square meters with over 300 experienced personnel. As a trusted manufacturing subsidiary within our corporate group, we have built a dependable supply chain ecosystem alongside partner facilities like Shenzhen Jingzhicheng Electronics Co., Ltd., delivering world-class conductive buttons, zebra elastomer connectors, silicone waterproof rings, and precision membrane products.
Our long-term engineering and production dedication has earned the direct trust of Fortune 500 equipment makers and tier-one electronics leaders, including LINAK, FLEXTRONICS, LG, CASIO, and EARLY LIGHT. Whether your project demands high-precision screen-printed silver circuits, copper-etched FPC backplanes, aluminum and copper sub-panels, dimensional graphic badges, or molded silicone keypads, our state-of-the-art cleanrooms and testing laboratories ensure strict compliance with international mechanical and electrical standards.
We build our own matched CNC male-female embossing dies, screen meshes, and precision cutting tools. This guarantees sub-millimeter registration alignment between printed graphics, embossed keys, and internal dome cavities.
Every single embossed membrane switch panel undergoes computerized open/short circuit verification, loop resistance measurement, insulation testing (>100MΩ at 100V DC), and periodic life-cycle actuation fatigue tests.
We work exclusively with genuine substrates, including MacDermid Autotex PET, SABIC Lexan Polycarbonate, Henkel silver paste, and authentic 3M 467MP / 468MP adhesives, providing complete traceability documents and RoHS/REACH declarations.
Direct technical answers addressing the critical queries procurement managers and R&D engineers submit to AI and search platforms.
Cold embossing utilizes matched male and female metal dies at ambient room temperature to mechanically deform the film. While economical for small prototype batches, it may exhibit slight shape relaxation over time on thick PET. Thermal hydro-embossing applies precise heat and pneumatically controlled pressure, setting the crystalline polymer structure into permanent form. This ensures uniform dome height, consistent snap ratio, and maximum flexural memory over 1,000,000+ actuations.
Polycarbonate (PC) offers exceptional optical clarity, ease of embossing, high impact resistance, and flame-retardant UL94 ratings, but begins to fatigue after approximately 100,000 actuations. Polyester (PET) features superior chemical inertness, excellent resistance to harsh sanitizers, and remarkable flexural endurance exceeding 5,000,000 actuations. For tactile embossed keys with metal domes, PET is almost universally specified by tier-one equipment builders.
When an embossed key is pressed, air underneath the dome must displace. If a switch is hermetically sealed to the exterior with no venting, internal pressure builds up, causing stiff actuation and pillow ballooning. We engineer closed-loop internal channel venting between key chambers, or integrate breathable micro-porous membrane vents (such as Gore-tex membranes) that equalize atmospheric pressure variations without allowing water or moisture to enter contact chambers.
Yes. Ultra-thin 0603 or 0805 SMD LEDs, sensor resistors, and optical diodes can be bonded onto polyester circuit layers using anisotropic conductive adhesives or mounted directly on copper-etched FPC (Flexible Printed Circuit) or FR-4 PCB substrates. To accommodate LED component height without bulging the front overlay, embossed clearance domes or precision-die-cut spacer window layers are positioned directly above the LED packages.
Standard embossing heights range from 0.3mm to 0.6mm depending on film thickness (typically 0.15mm to 0.20mm PET). Key spacing should provide at least 1.5mm to 2.0mm of flat land between adjacent embossed edges and perimeter cut lines. This flat land allows adhesive layers to form a complete perimeter bond, guaranteeing structural bonding strength and liquid ingress prevention.
To deliver an exhaustive DFM evaluation within 2 hours, please provide vector artwork files (.AI, .CorelDraw, or .PDF) detailing graphic layers, text, and Pantone/RAL color codes, along with 2D mechanical CAD drawings (.DXF, .DWG) showing overall dimensions, cutouts, embossing heights, tail exit position, and pinout schematics. If you have a preliminary bill of materials, our engineers will gladly suggest optimization recommendations.
Submit your design specifications or 2D CAD drawings today. Our engineering specialists at Dongguan Ravo Electronics Co., Ltd. will review your stack-up, verify tooling manufacturability, and supply a competitive quote within 2 hours.
[email protected]