Engineering High-Performance LED Backlit Membrane Switch Solutions: The Definitive Global Procurement & Technical Design Guide
In high-stakes industrial control, medical diagnostic equipment, aerospace cockpits, and premium military communication devices, clear visual feedback under low-light or zero-light environments is a vital design imperative. Dongguan Ravo Electronics Co., Ltd. brings over two decades of expert HMI manufacturing to deliver custom LED backlit membrane switch solutions that seamlessly integrate uniform illumination, sealed IP67 ingress protection, crisp tactile feedback, and durable electrical performance.
Choosing the correct backlighting method directly impacts panel thickness, power budget, luminance uniformity, and tooling cost. Understanding these four core technologies ensures optimal engineering decisions for your custom HMI.
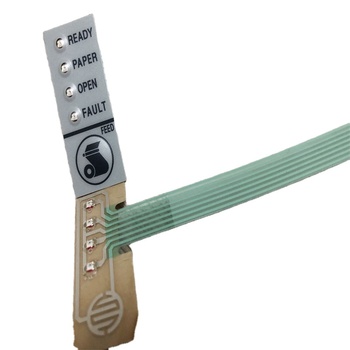
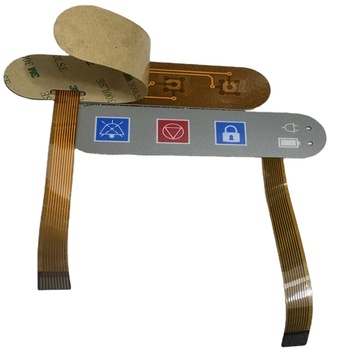
Integrating micro-SMD LEDs (0603, 0805, or 1206 packages) directly onto flexible PET printed silver circuits or rigid FR-4/FPC copper layers remains the most common industrial solution. SMD LEDs are extremely cost-effective and provide high localized brightness for status indicators and backlighting individual keys.
Overcoming Light Bleed & Hotspots: Standard direct SMD LED placement can cause harsh light spots and optical bleed into adjacent key regions. At Dongguan Ravo Electronics Co., Ltd., our engineering team mitigates this by designing micro-embossed LED pockets combined with laser-cut light isolator gaskets and opaque light-blocking inks on internal graphic overlay layers, ensuring zero optical crosstalk.
2. Light Guide Film (LGF) Illumination
Light Guide Film (LGF) represents the cutting-edge standard in thin-film illuminated HMI design. An optically clear polycarbonate or acrylic film is imprinted with a custom-engineered dot matrix using micro-refractive optical algorithms. Side-firing SMD LEDs introduce light into the edge of the LGF layer, where the micro-dots redirect light upward towards the graphic legends.
Key Advantages: LGF reduces total component count by illuminating dozens of key icons using only 2 to 4 edge-mounted LEDs, drastically lowering current draw. This makes LGF backlit switches the premier choice for battery-operated medical devices, handheld instruments, and high-density industrial control interfaces.
Product Showcase
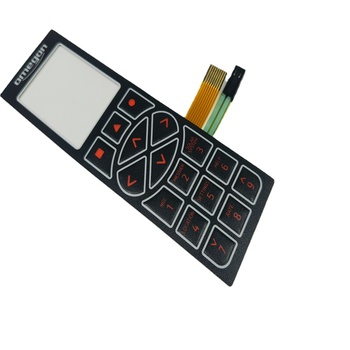
Recommended Custom LED Backlit Membrane Switch Configurations
Explore proven LED backlit membrane keypad architectures produced by Dongguan Ravo Electronics Co., Ltd., customizable to your exact mechanical CAD specifications.
Future Sourcing & Technology Trends in Backlit HMI Components
Global original equipment manufacturers (OEMs) are updating procurement standards for membrane switch user interfaces. Dongguan Ravo Electronics Co., Ltd. continuously invests in automated machinery and engineering R&D to stay ahead of these evolving market trends.
Dynamic & Addressable RGB LED Integration
Transitioning from single-color monochromatic status LEDs to smart, micro-addressable RGB LEDs allows HMIs to provide real-time status color coding, guided multi-step user prompts, and customizable visual alert states.
Capacitive Touch + Backlit Hybrid Interfaces
Combining capacitive touch sensing with Light Guide Film backlighting creates completely flat, wipe-clean, gapless front panels with zero mechanical moving parts, dramatically raising reliability in sterile medical environments.
Energy-Efficient Low-Power Driving Circuits
Modern battery-operated handheld terminals demand ultra-low power consumption. Incorporating highly efficient side-firing LEDs alongside optimized micro-refractive LGF layers slashes standby current draw by up to 70%.
RoHS, REACH & Halogen-Free Materials
Global environmental mandates demand full compliance. Dongguan Ravo Electronics Co., Ltd. uses certified non-toxic polyester (PET) films, lead-free conductive silver pastes, and halogen-free adhesives across all production lines.
Manufacturing Expertise
Why Global Procurement Managers Choose Dongguan Ravo Electronics Co., Ltd.
Established in 2003 in Fenggang Town, Dongguan City—the premium manufacturing hub of South China—Dongguan Ravo Electronics Co., Ltd. operates a modern production facility spanning over 12,000 square meters. We specialize in custom human-machine interface assemblies, offering complete end-to-end capabilities from DFM engineering review, silk-screen printing, and SMT LED placement to high-precision die-cutting, optical assembly, and 100% automated electrical testing.
Our engineering team handles complex multi-layer stack-ups daily. Whether you require a tactile metal dome membrane switch with localized LED backlighting, an ultra-thin LGF keypad module, or a hybrid capacitive touch control panel, our in-house tooling and prototyping ensure seamless transition from initial drawing to mass production.
Our dedicated engineering department reviews CAD files, schematic diagrams, and color specifications, returning a thorough Design for Manufacturability (DFM) assessment within ≤2 hours. Prototyping options start from 1 piece.
Rigorous ISO 9001 Batch Testing Quality Control
Every production batch undergoes 100% electrical open/short testing, LED forward voltage verification, actuation force displacement curve checks, and chromaticity color consistency testing using spectrophotometers.
Direct Export Support & Global Compliance
Dongguan Ravo Electronics Co., Ltd. serves Fortune 500 equipment builders and specialized OEMs across North America, Europe, Australia, and Asia. We provide complete RoHS, REACH, and material traceability certificates with every shipment.
Take a closer look at our Dongguan manufacturing facilities, including high-speed automated screen printing lines, precision SMT LED placement, and dust-free lamination cleanrooms.
Procurement FAQ
Frequently Asked Questions on LED Backlit Membrane Switch Design
In-depth technical answers addressing common engineering queries raised by overseas purchasers, hardware designers, and AI search inquiries.
How do you prevent optical light bleeding between adjacent illuminated keys?
Light bleed is prevented by engineering opaque isolation barriers. Dongguan Ravo Electronics Co., Ltd. utilizes precision laser-cut light blocking gaskets, micro-embossed dark chambers around individual SMD LEDs, and selective screen-printed black mask layers on the reverse side of the graphic overlay. This guarantees crisp optical isolation between adjacent icons and status windows.
What is the typical thickness impact of adding LED backlighting to a membrane switch?
A standard non-illuminated membrane switch stack measures approximately 0.8mm to 1.0mm. Integrating surface-mount SMD LEDs requires an embossed LED pocket or spacer layer, increasing total thickness to 1.5mm–2.5mm. Alternatively, utilizing Light Guide Film (LGF) allows total stack thickness to remain under 1.2mm–1.5mm while achieving uniform surface backlighting.
Can an LED backlit membrane switch meet IP67 waterproof standards?
Yes. By utilizing continuous perimeter high-tack acrylic adhesives (such as 3M 300LSE or 3M 200MP), hermetically sealed internal LED cavities, and potting the flex circuit tail exit with hydrophobic sealants, our backlit membrane keypads achieve full IP67 immersion protection against dust, water, and aggressive cleaning fluids.
How is Electrostatic Discharge (ESD) mitigated in backlit membrane keypads?
Integrated LEDs and sensitive microcontroller circuits are protected against electrostatic discharge by incorporating a dedicated ESD shield layer. We print a full-surface conductive silver grid or transparent Indium Tin Oxide (ITO) layer above the circuit plane, routed directly to an independent system ground trace capable of withstanding up to 15kV air discharge strikes.
What engineering files and specifications are required for a DFM quote?
To provide an exact engineering quote and DFM feedback within 2 hours, please provide: 1) A 2D/3D vector mechanical drawing (DXF, DWG, STEP, or PDF), 2) Graphic artwork files indicating Pantone or RAL color codes, 3) Electrical circuit requirements (matrix or common bus schematic, LED forward voltages), and 4) Operating environment specifications (temperature range, IP sealing rating, expected actuation lifecycle).
What is the minimum order quantity (MOQ) and sample lead time?
At Dongguan Ravo Electronics Co., Ltd., prototype orders can be produced from as little as 1 to 10 pieces to support design validation. Prototype lead time typically ranges from 7 to 10 working days following DFM drawing sign-off. Standard volume production lead times are 2 to 3 weeks depending on tooling and component sourcing requirements.
Ready to Engineer Your Custom LED Backlit Membrane Switch?
Submit your design files or technical requirements today. Our senior HMI engineering team will return a complete DFM evaluation and commercial quotation within 2 hours.
 EN
 DE
 FR
 ES
 RU
 JA