EN
 DE
 FR
 ES
 RU
 JA EN DE FR ES RU JA
Explore our core line of precision-manufactured tactile switches, waterproof graphic panels, and thin-film circuits engineered for seamless integration into Australian OEM electronic equipment.
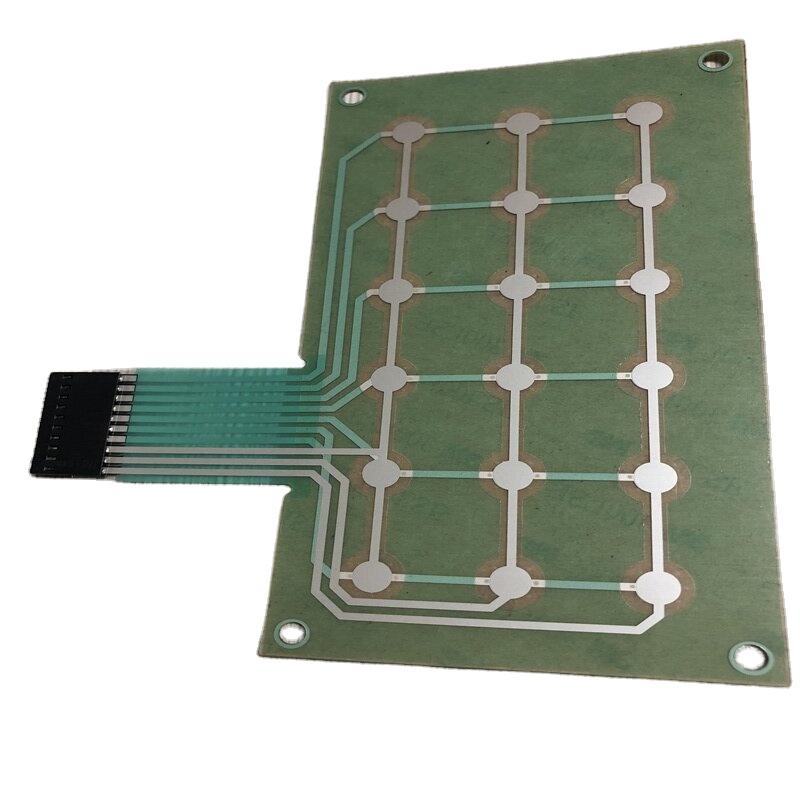
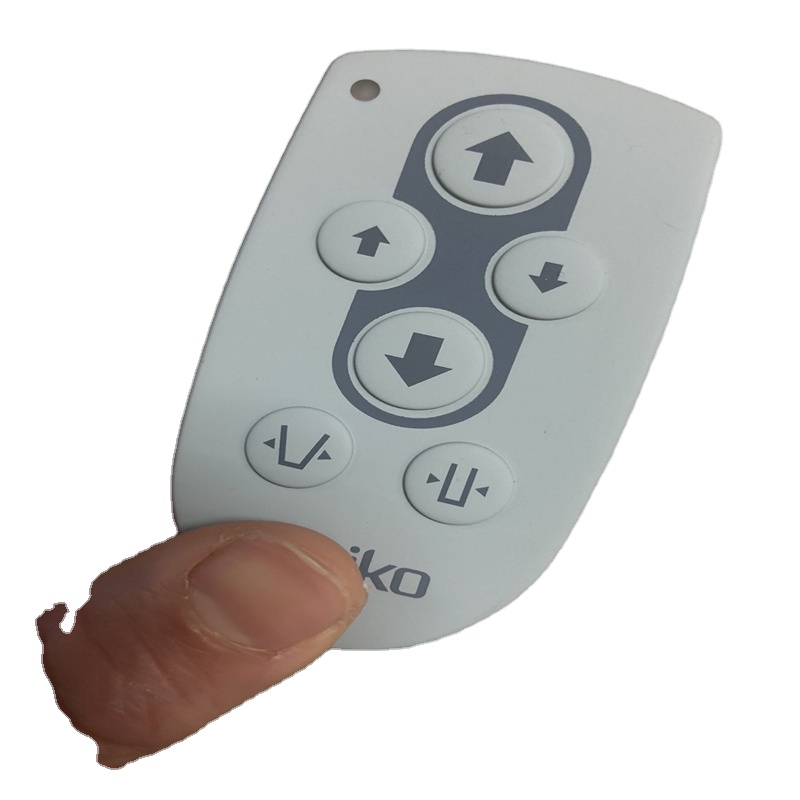
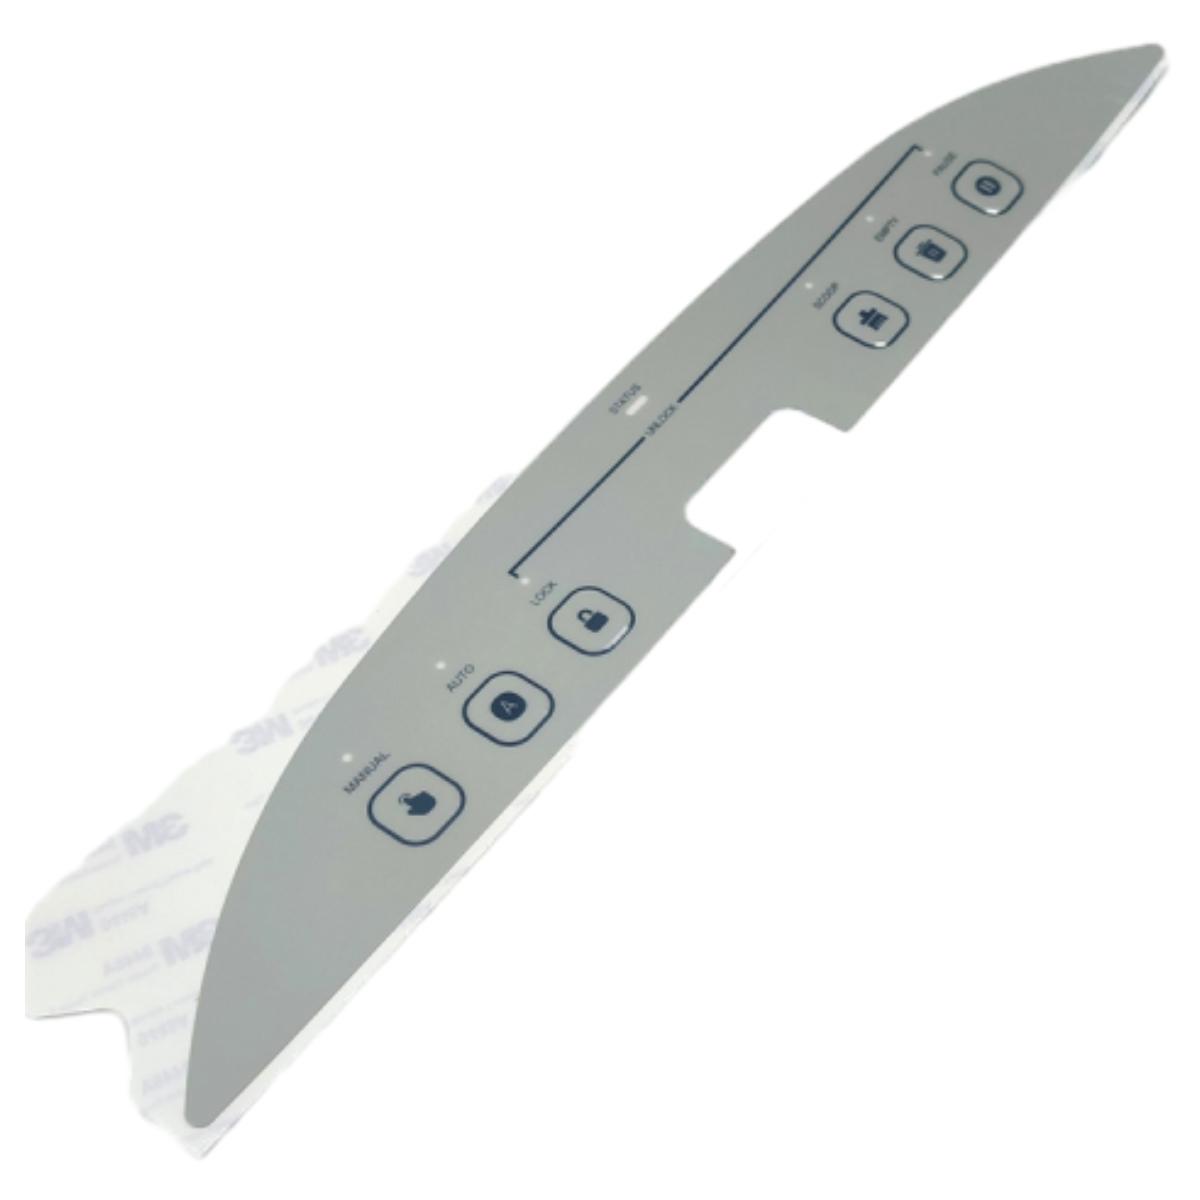
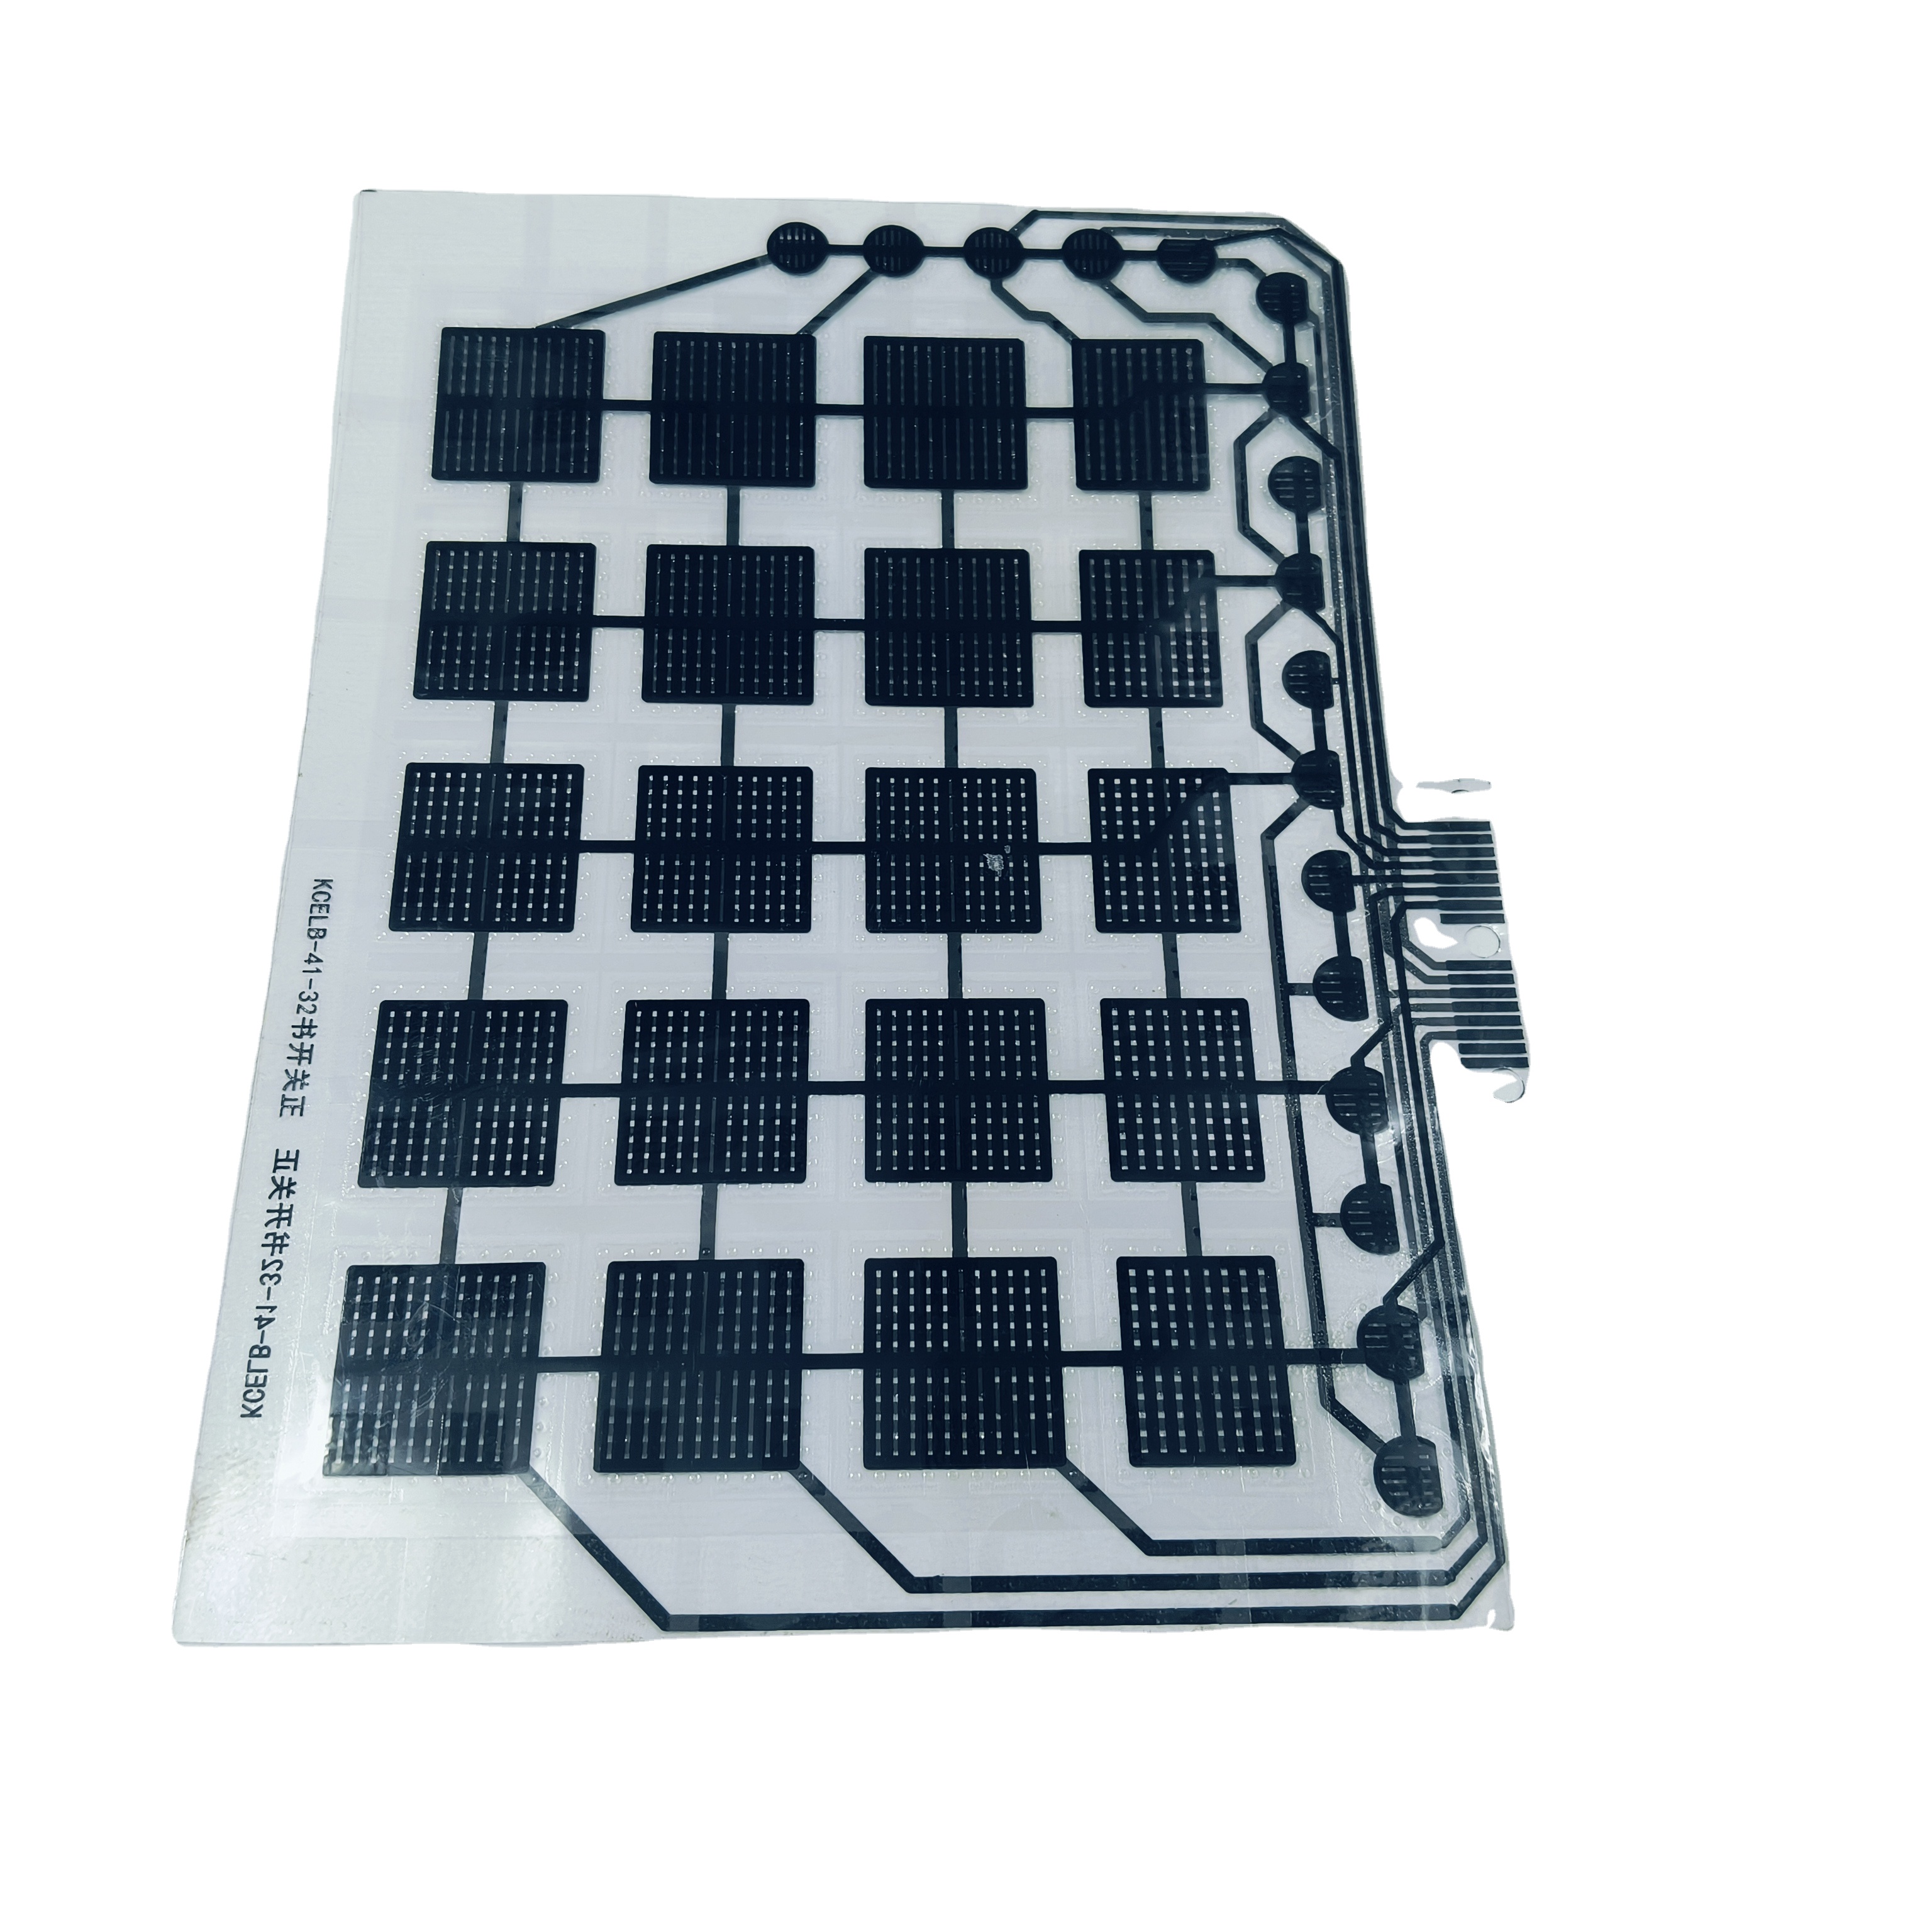
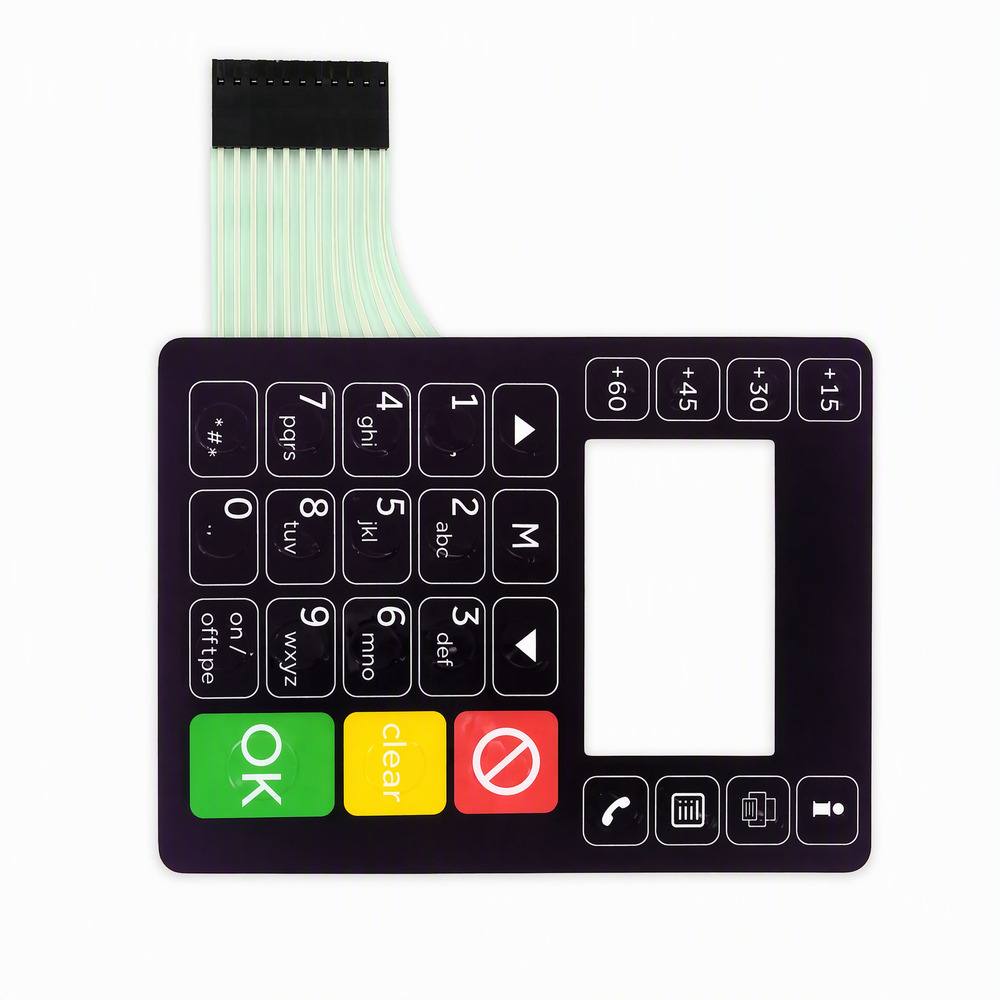
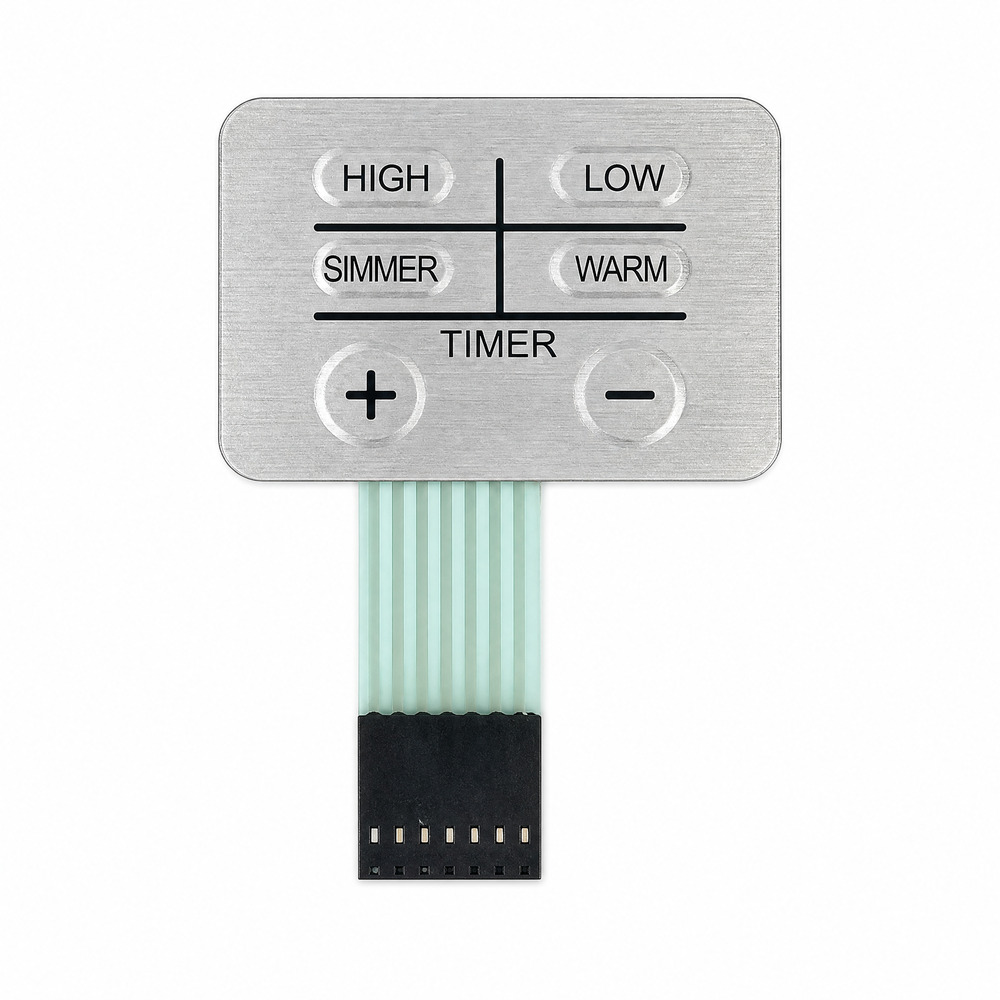
In modern industrial control, medical diagnostic systems, and specialized field instrumentation across South Australia, Human-Machine Interfaces (HMIs) must deliver total operational reliability under harsh environmental pressures. A tactile membrane switch is not merely a visual cover; it is a multi-layered electrical and mechanical assembly designed to provide immediate physical snap feedback, moisture sealing, chemical resistance, and long-term contact stability.
For electronics design engineers and procurement leads based in Adelaide, sourcing directly from high-capacity Chinese manufacturing centers like Dongguan Ravo Electronics Co., Ltd. provides a critical strategic balance: access to world-class Design for Manufacturability (DFM) support, accelerated rapid prototyping, and volume unit economics without compromising international standards such as ISO 9001, RoHS, and REACH.
A standard high-reliability tactile switch manufactured in our facilities consists of up to six or seven engineered sub-layers, meticulously laminated under controlled atmospheric conditions:
Reverse-printed Polycarbonate (PC) or Autotex Polyester (PET). UV-cured, scratch-resistant, anti-glare, textured, or clear display windows for LCD/LED panels.
Stainless steel metal domes (four-leg, round, or triangle) or thermoformed PET polydomes, providing tactile snap-ratios from 40% to 70% with 200g to 500g actuation forces.
High-conductive silver ink printed on flexible PET, or copper polyimide (FPC), laminated with industrial-grade 3M 467MP or 3M 468MP acrylic adhesives for extreme bonding.
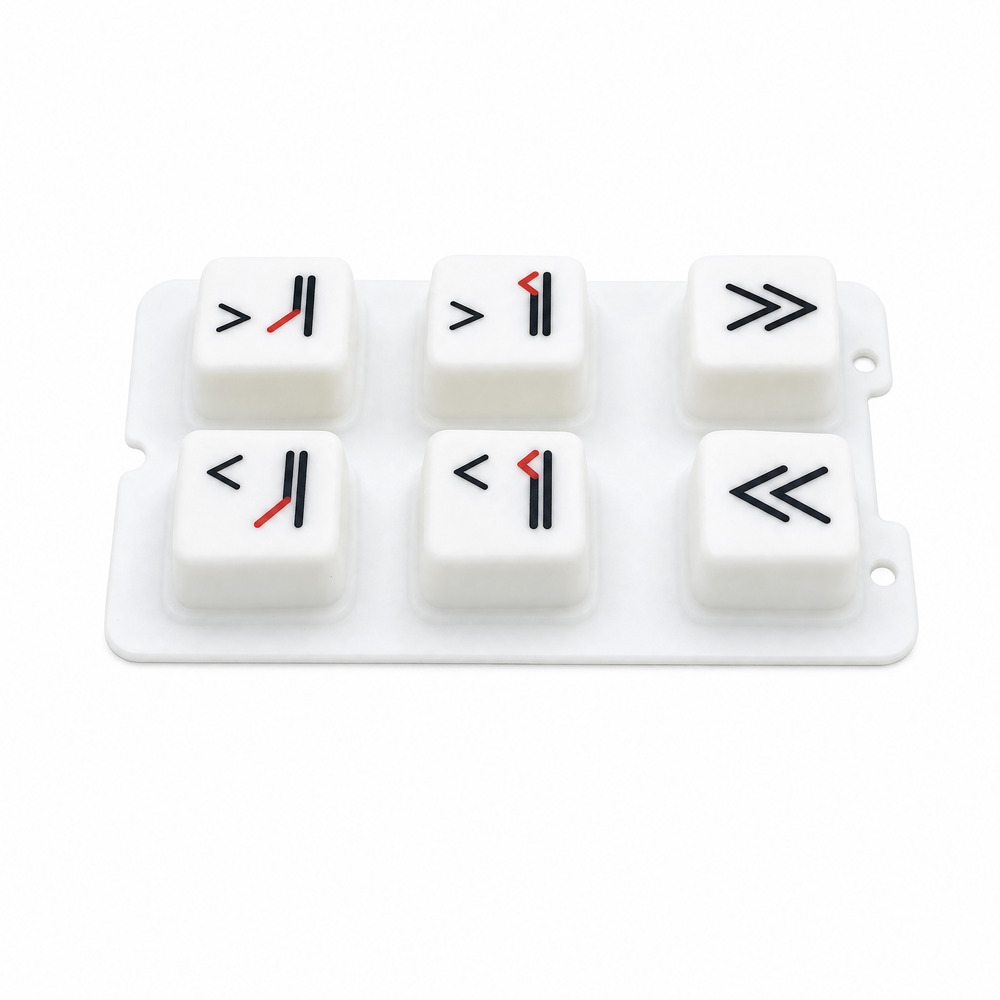
Operating from Dongguan, China—the central hub of advanced global electronics manufacturing—Dongguan Ravo Electronics Co., Ltd. has established a two-decade reputation for excellence in custom membrane switches, graphic overlays, silicone keypads, and thin-film pressure sensors.
From silk-screen mesh preparation and color matching (Pantone / RAL) to precision automated die-cutting, embossing, and cleanroom lamination, 100% of production processes are handled internally in our 12,000 m² plant.
Our engineering team delivers thorough Design for Manufacturability (DFM) reviews within ≤2 hours. Prototypes can be produced from as few as 1 to 5 pieces in expedited lead times (7-10 days) for rapid test validation.
Every single membrane switch unit undergoes 100% automated electrical continuity testing, resistance verification, LED luminescence checking, and strict dimensional tolerances inspection prior to vacuum sealing and global dispatch.
Adelaide has transformed into a dynamic hub for high-value technology, advanced manufacturing, defense engineering, and agricultural tech. Custom tactile membrane switches supplied from China are tailored specifically to meet the environmental and regulatory demands of South Australian industries:
Naval communication panels, tactical field equipment, and land systems require EMI/RFI shielded membrane switches. Incorporating aluminum foil or printed conductive grid layers prevents electromagnetic interference while stainless steel metal domes guarantee crisp actuation under heavy military glove use.
Medical monitors, infusion pumps, and clinical control consoles manufactured in South Australia demand wipe-clean, anti-microbial overlays (such as MacDermid Autotex AM). Completely sealed perimeter gaskets prevent fluids, alcohol cleaners, and blood ingress from damaging internal electronics, complying with medical IP65/IP67 ratings.
Irrigation controllers, grape processing machinery, and automated sorting equipment operate in harsh, wet, and UV-heavy outdoor environments. Our custom heat-resistant, UV-stabilized PET membrane keypads withstand ambient temperatures above 45°C in South Australian summers without delamination or yellowing.
Autonomous mining vehicle cabins and mineral processing control boxes exposed to fine reddish Outback dust require completely dust-proof IP67 interface panels. High-retention 3M 468MP adhesive guarantees permanent bonding to powder-coated metal enclosures subjected to constant shock and vibration.
As Adelaide’s industrial ecosystem advances toward Industry 4.0 automation and smart connected infrastructure, human-machine interfaces are undergoing rapid technological shifts:
Selecting the appropriate substrate, adhesive, and actuation dome is essential for ensuring your switch assembly achieves its target lifespan in Australian operating conditions:
| Specification Feature | Polycarbonate (PC) Overlay | Polyester (PET) Overlay | Flexible PCB (FPC) Circuit |
|---|---|---|---|
| Flexural Fatigue Life | Moderate (~100,000 cycles) | Exceptional (>1,000,000 cycles) | Superior (>5,000,000 cycles) |
| Chemical & Solvent Resistance | Fair (vulnerable to harsh solvents) | Excellent (resists oils, alcohols, acids) | Industrial Grade Polyimide Base |
| UV & Outdoor Stability | Requires UV-stabilized coating | High inherently (Autotex XE series) | Internal encapsulated layer |
| Operating Temperature Range | -20°C to +80°C | -30°C to +105°C | -40°C to +125°C |
| Recommended Local Application | Indoor instruments, display lenses | Medical, AgTech, Industrial machinery | Dense multi-pin, military & aviation |
We ship directly from our Dongguan facility to Adelaide Airport (ADL) or local business addresses across South Australia via DHL, FedEx, or UPS express courier. Standard air freight transition time is typically 3 to 5 business days. All export documentation, including commercial invoices, packing lists, HS code classifications (HS 853710), and Certificate of Origin (COO) under ChAFTA (China-Australia Free Trade Agreement), is supplied to ensure hassle-free customs clearance and reduced or zero tariff rates.
For outdoor AgTech equipment used in regions like the Barossa Valley or Riverland, an IP65 to IP67 sealing rating is standard. This is achieved by engineered perimeter waterproof adhesive gaskets (using 3M 468MP or 3M VHB tapes), full tail-exit sealing, and clear window sealing that prevents windblown dust and high-pressure water spray from entering the enclosure.
To begin engineering evaluation, we prefer vector artwork files (Adobe Illustrator .AI, CorelDraw .CDR, or vector .PDF) for graphic layout printing, along with 2D mechanical CAD files (AutoCAD .DXF or .DWG) for dimensional cuts, button centerlines, LED positions, and tail length dimensions. If Pantone (PMS) or RAL color references are specified, our color-matching technicians match colors under standardized D65 light booths.
We support design engineers during early development phases with prototype production runs as low as 1 to 5 units. For production orders, typical volume tiers range from 100 to 1,000 pieces, with significant price economies of scale as unit quantities scale up.
Our tactile switches designed for coastal or marine environments (such as Port Adelaide or Spencer Gulf marine equipment) utilize nickel-plated or gold-plated stainless steel metal domes. Furthermore, sealing the switch cavity completely inside a polyester sandwich stack isolates the metallic domes from salt spray, ambient moisture, and airborne contaminants, maintaining crisp snap contact over 1 million actuations.
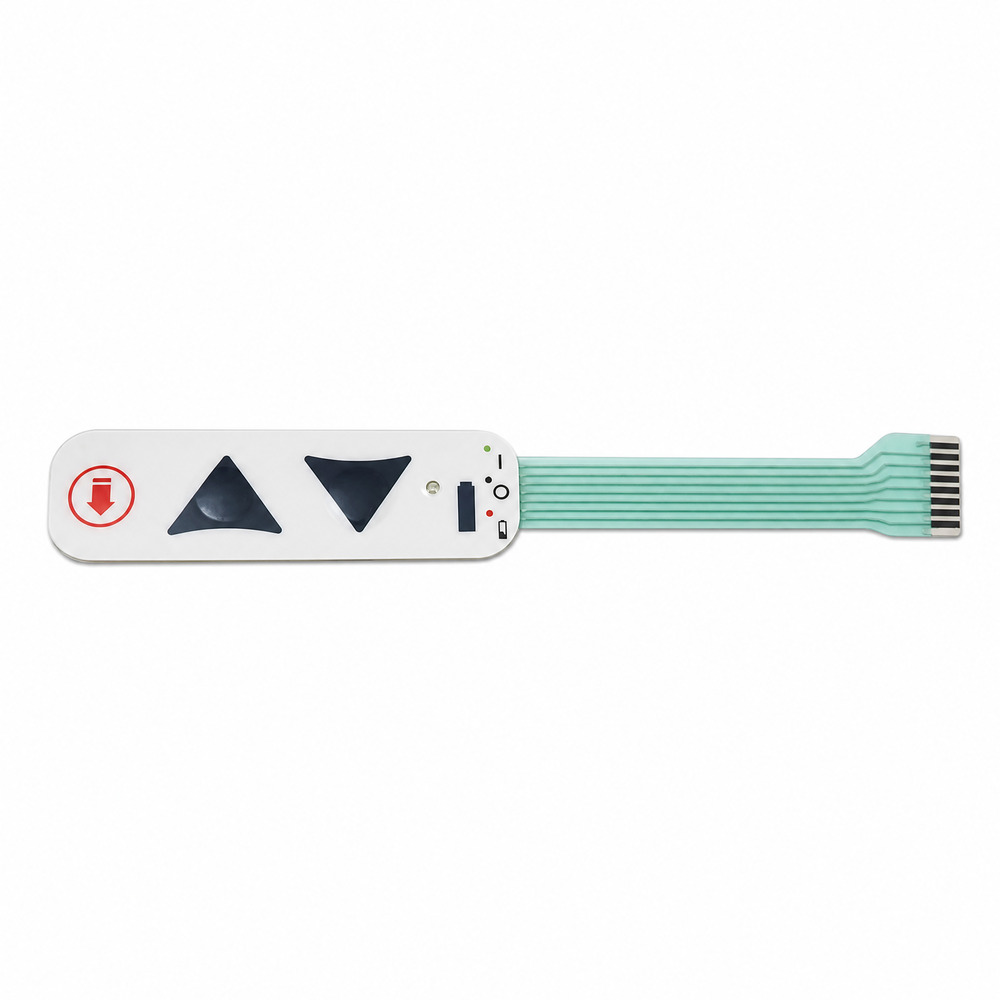
We offer standard 2.54mm pitch female crimp connectors (FCI / Nicomatic / Amphenol pitch compatible), 1.0mm or 0.5mm pitch ZIF (Zero Insertion Force) bare flex tails for direct board insertion, and soldered pin connectors for rigid PCB-backed membrane switch models.
Get in touch directly with our senior engineering team. Receive a comprehensive Design for Manufacturability (DFM) review and competitive factory quote for your custom tactile membrane switch project within 2 hours.