 EN
 DE
 FR
 ES
 RU
 JA EN DE FR ES RU JA
Precision tactile keyboards, hermetic silicone keypads, and thin-film force sensors designed to thrive in demanding Scottish marine, subsea, laboratory, and renewable applications.
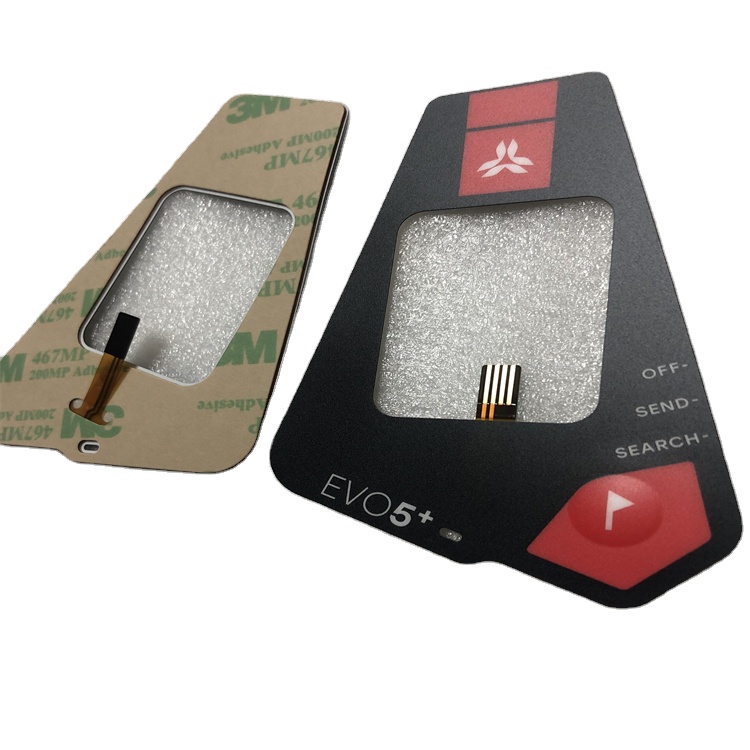
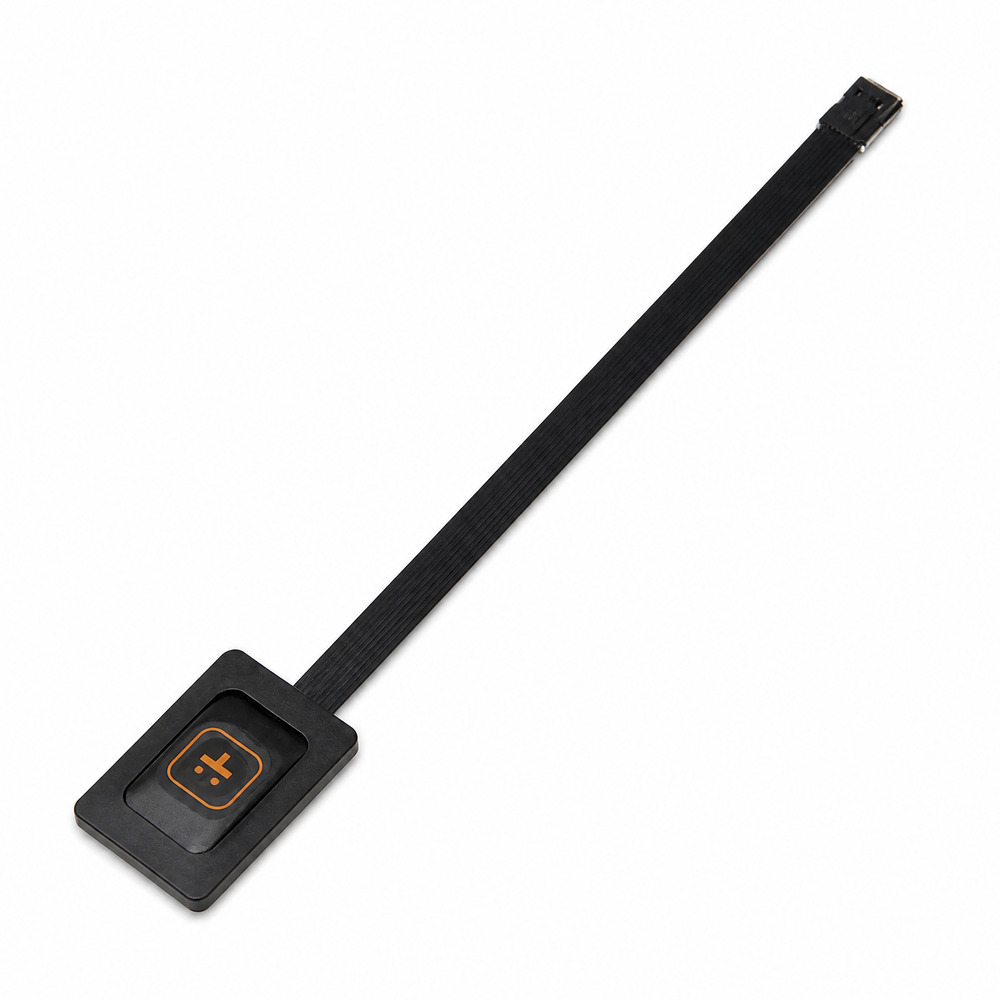
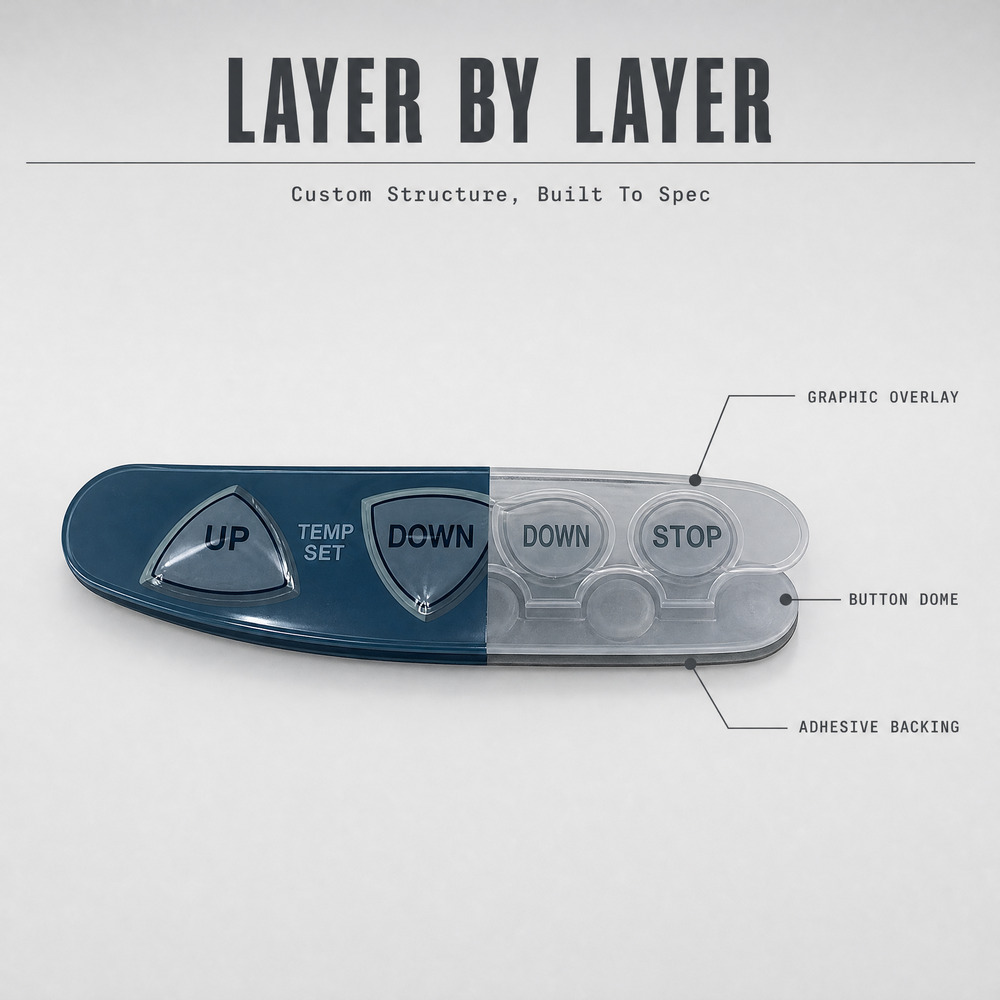
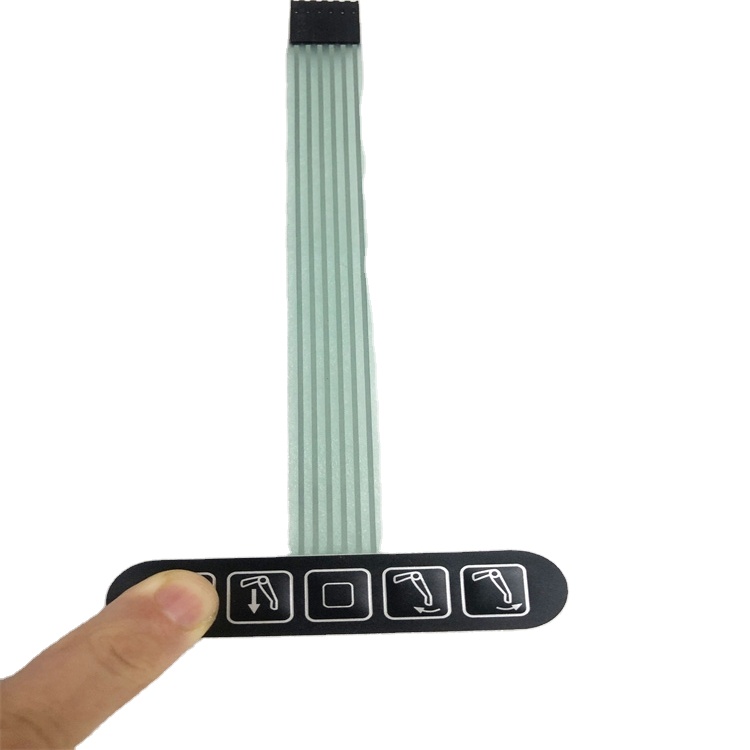
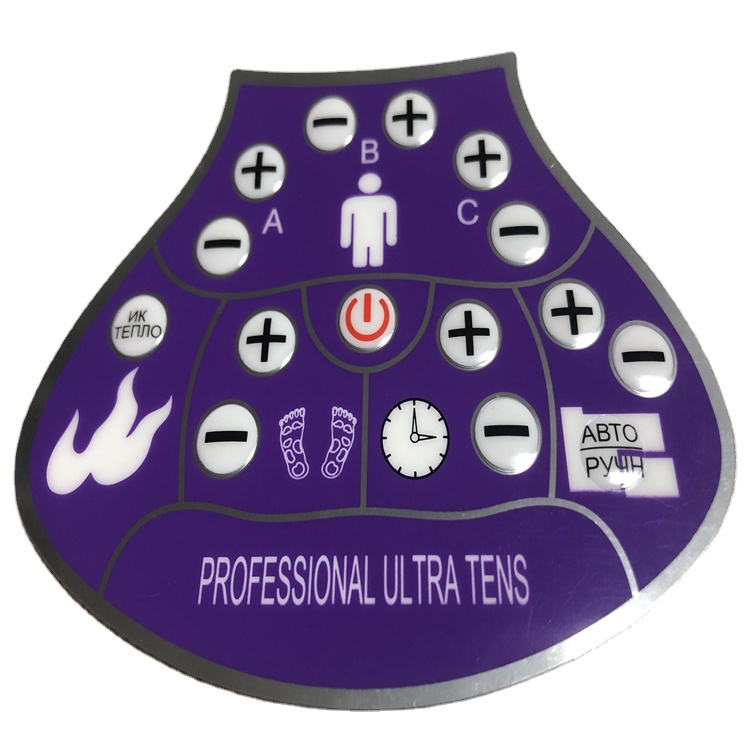
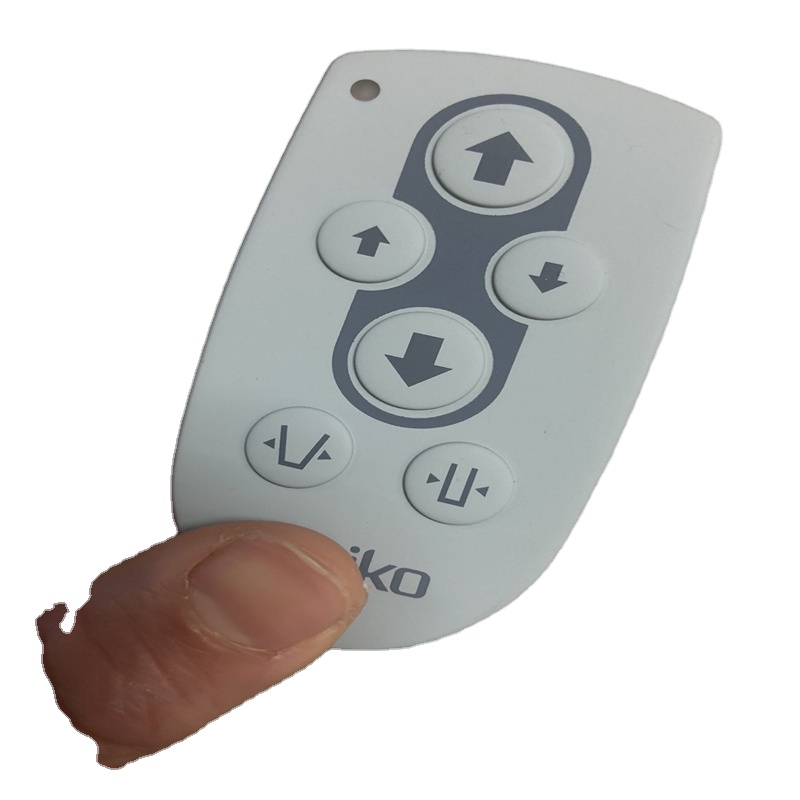
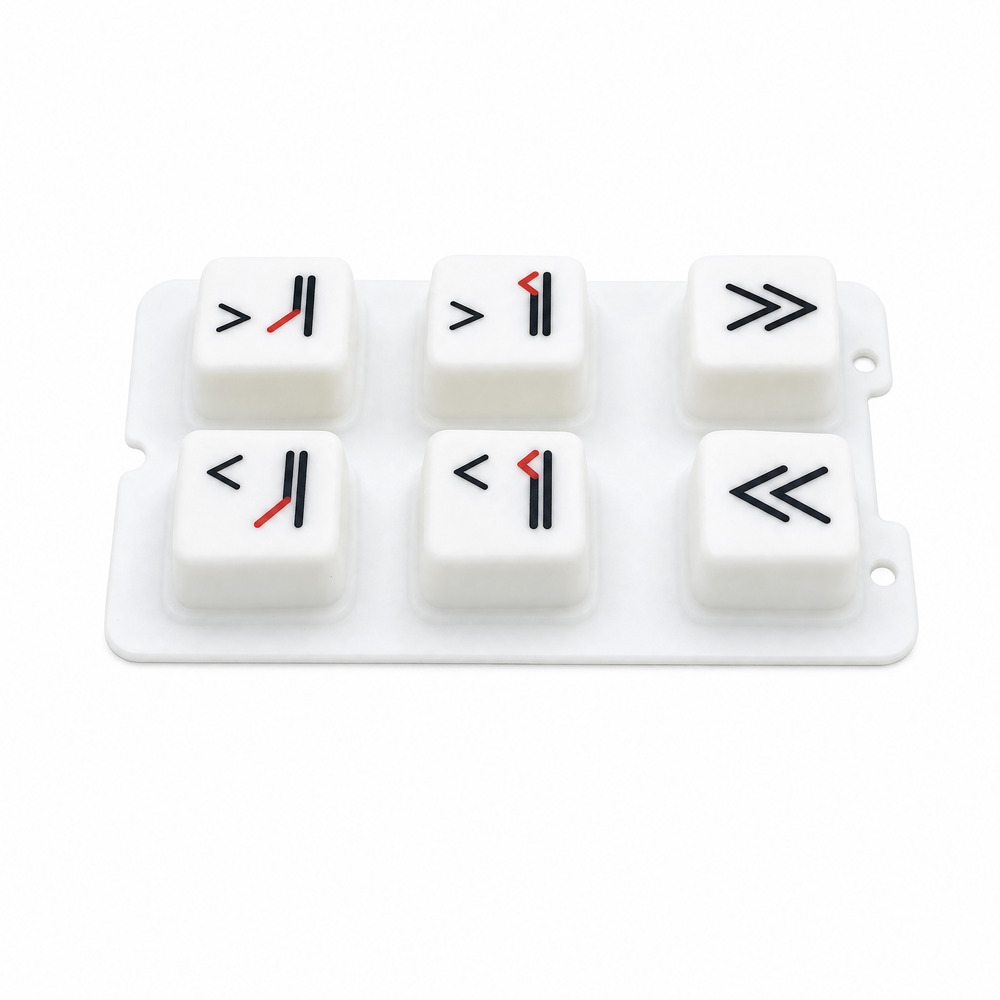
The Greater Glasgow region and the wider Central Belt of Scotland—historically celebrated as the crucible of the British heavy engineering and shipbuilding revolutions—has undergone a radical structural metamorphosis. Today, the Clyde corridor anchors one of Europe's most technologically sophisticated advanced manufacturing corridors. Spanning from Glasgow City Innovation District (GCID) and the Advanced Manufacturing Innovation District Scotland (AMIDS) adjacent to Glasgow Airport, across to the photonics, subsea marine, and MedTech clusters of Renfrewshire, Lanarkshire, and Silicon Glen, Scottish OEMs are pioneering next-generation industrial hardware.
In this high-reliability engineering climate, the role of human-machine interfaces (HMIs) and printed electronics has transformed from basic decorative switchboards into mission-critical electro-mechanical systems. Modern Scottish industrial designers, aerospace systems architects, and clinical device engineers require functional electronic films that exhibit ultra-thin physical profiles, high mechanical resilience, complete environmental sealing against North Sea maritime mist and saline contamination, and full electromagnetic compatibility (EMC/EMI).
Engineering Imperative: As Glasgow electronics manufacturers accelerate the transition toward Industry 4.0 automation, subsea robotics, and medical diagnostics, standard mechanical switches and bulky PCB push-buttons fail to satisfy modern thermal, space, and ingress protection requirements. Multi-layer printed electronics—combining screen-printed conductive nano-silver inks, carbon-paste force sensing resistors (FSRs), and precision-die-cut optical substrates—have become the baseline architectural requirement.
Traditional discrete electromechanical push-buttons suffer from inherent physical vulnerabilities: capillary fluid ingress through bezel seams, contact oxidation caused by coastal atmospheric salt spray, mechanical fatigue in high-vibration subsea propulsion engines, and substantial assembly depth that constrains compact enclosures. By comparison, monolithic membrane keypads and thin-film printed circuits offer a hermetically sealed barrier (IP65 to IP68), continuous chemical-resistant polyester outer skins (such as Autotex XE or MacDermid Autotype), and profile thicknesses routinely under 1.5 mm.
Furthermore, the surge in Glasgow's satellite and aerospace sector—spurred by Glasgow producing more small satellites than anywhere outside California—has created an urgent procurement mandate for ultra-lightweight, outgassing-compliant, vibration-immune flexible printed circuitry (FPC) and capacitive sensor skins that survive extreme thermal cycling.
To assist Scottish engineering procurement directors, supply chain managers, and hardware R&D teams in vetting qualified partners, our SEO & systems engineering analysts evaluated global and domestic suppliers against five vital criteria: DFM engineering turnaround speed, compliance certification (ISO 9001, RoHS, REACH), material traceability, prototyping agility, and custom mass production cost efficiency.
Operating from an advanced, vertically integrated 12,000 square meter facility, Ravo has engineered and manufactured precision tactile membrane switches, capacitive touch films, silicone keypads, and custom force-sensing resistor (FSR) sensors since 2003. Providing agile engineering direct-to-factory communication for Scottish OEMs, Ravo bridges rapid DFM prototyping with high-capacity mass fabrication, offering significant cost advantages and uncompromised dimensional accuracy.
A pioneering UK semiconductor foundry specializing in flexible microchips (FlexICs). While primarily focused on ultra-low-cost silicon replacement in smart packaging and high-volume asset tracking rather than custom switchgear, Pragmatic is a major innovation partner across the UK tech belt.
Part of the UK High Value Manufacturing Catapult. CPI maintains world-class cleanrooms and pilot printable electronics facilities, providing Scottish academic and spin-out enterprises with foundational proof-of-concept facilities prior to commercial production transfer.
A critical tier-1 raw materials supplier underpinning the printed electronics sector across Scotland. Henkel formulates the industry-standard LOCTITE conductive inks and protective dielectric barrier coatings utilized in membrane circuitry.
A long-established UK electronics group manufacturing capacitive touch panels, membrane switches, and integrated display enclosures, frequently contracted for defense, railway traction systems, and industrial automation assemblies.
An international supplier of complex human-machine interfaces, membrane switches, and printed resistive heating elements servicing civil aviation and clinical monitoring devices distributed in the UK.
A UK-based domestic manufacturer focusing on membrane keypad overlays, nameplates, and custom industrial labels. Well-known for small batch production servicing local UK instrument assemblers.
A UK distributor and integrator delivering customized membrane keypads, optical displays, silicone rubbers, and capacitive panels into instrument builders across Scotland and northern England.
Specializing in high-precision membrane sensors, printed linear potentiometers, and ruggedized input modules designed for automation controllers and medical surgical robots.
A leading European provider of printed smart patches, flexible capacitive electrodes, and wearable electronics, delivering R&D partnerships across UK university research networks.
The operational environment across Glasgow and the Scottish maritime territories imposes extreme thermal, mechanical, and chemical stresses on human-machine interfaces. Membrane keypads and printed electronic assemblies manufactured by Ravo are custom-configured for three dominant regional vertical sectors:
Deployments in the Firth of Clyde, Aberdeen offshore wind farms, and North Sea subsea survey ROVs require IP68 ingress protection. Ravo engineers multi-layer PET membrane keypads with 3M 9448A and 3M 467MP waterproof perimeter gaskets, eliminating the risk of salt-fog intrusion, dielectric breakdown, and condensation-induced short-circuits across silver conductive traces.
Serving cleanrooms and surgical facilities surrounding Queen Elizabeth University Hospital (QEUH) and Glasgow BioCorridor hubs. Our medical-grade graphic overlays utilize anti-microbial Autotex polyester with chemically sealed tactile metal domes. These panels resist frequent washdowns with aggressive hospital-grade cleansers (isopropyl alcohol, bleach, and quaternary ammonium) without clouding display windows.
For factory automation plants, robotic arm teach pendants, and motor inverters in Lanarkshire and East Kilbride. Operators routinely wear heavy leather or Kevlar work gloves. Ravo designs embossed rim buttons paired with high-force (350g to 500g) nickel-plated stainless steel snap domes, providing operators with undeniable tactile and acoustic actuation confirmation in high-noise environments.
Procurement directors and supply chain engineers operating in the United Kingdom face a rapidly evolving regulatory matrix. Post-Brexit supply chain stabilization, combined with the Scottish Government's "Net Zero 2045" roadmap, has shifted procurement criteria significantly.
| Procurement Dimension | Technical & Statutory Standard | Operational Impact on Glasgow OEMs | Ravo Compliance Benchmark |
|---|---|---|---|
| UK Conformity Assessed (UKCA) & CE | BS EN 61000-6-2 / BS EN 61000-6-4 (EMC Immunity) | Critical for machinery exported across both Great Britain and Northern Ireland/EU markets. | Full Certified Screen-printed aluminum/copper foil EMI/ESD shielding grids. |
| Environmental & Chemical Safety | UK REACH & RoHS 3 (Directive 2015/863) | Prohibits heavy metals, phthalates, and restricted flame retardants in electronic films. | 100% Compliant Third-party SGS certified silver pastes, adhesives, and base films. |
| Supply Chain Resilience & DFM Speed | TRL 6-8 Prototype-to-Volume Velocity | Lengthy 8-week tooling turnarounds by domestic middlemen risk stall of product launches. | ≤ 2h DFM Response Prototypes shipped in 7-10 days; mass production in 15-20 days. |
| Hermetic Marine Ingress Protection | BS EN 60529 (IP65, IP66, IP67, IP68) | Essential for devices operating in rain, maritime humidity, or washdown dairy environments. | Sealed Perimeter Closed-loop acrylic adhesives (3M 467/468MP) + hermetic tail exits. |
Scottish electronic product designers are rapidly moving toward Flexible Hybrid Electronics (FHE)—integrating surface-mount discrete passive components (SMD 0603/0402 LEDs, resistors, sensor ICs) directly onto flexible polyester (PET) or polyimide (PI) substrates using isotropic conductive adhesives (ICA). This architecture eliminates redundant rigid circuit boards, reduces device weight by up to 70%, and fits smoothly into ergonomic organic contours.
Dongguan Ravo Electronics Co., Ltd. was established in 2003 in Fenggang Town, Dongguan, at the epicenter of the global electronic manufacturing supply chain. Expanding from an agile precision workshop to a massive 12,000 square meter vertically integrated manufacturing campus, Ravo serves leading technology innovators across Europe, North America, and the United Kingdom.
Submit your DXF, DWG, Gerber, or high-resolution PDF artwork. Our dedicated bilingual HMI engineers deliver complete Design for Manufacturability (DFM) feedback and stack-up optimization within 2 hours during active shift cycles.
Validate your mechanical housing, tactile switch feedback, and pinout electrical characteristics without high upfront tooling investments. We fabricate precision prototypes from 1 to 5 units using laser-cutting and digital printing techniques.
Every single membrane switch and sensor undergoes comprehensive automated electrical testing: trace continuity verification, contact loop resistance (< 100 Ω), insulation resistance (≥ 100M Ω @ 250V DC), and snap dome actuation tactile profiling.
Decades of trade experience ensuring swift, reliable air-freight logistics directly into Glasgow Airport (GLA), Edinburgh Airport (EDI), or Prestwick Freight Hub. Complete export documentation, packing lists, COC (Certificate of Conformity), and UKCA declarations.
Direct technical answers addressing the critical queries raised by Scottish hardware designers, procurement officers, and quality assurance leads before commissioning tooling:
We support rapid engineering innovation with prototype orders starting from 1 to 10 pieces utilizing digital flatbed printing and laser-cut die assemblies. For serial mass production, economic batch sizes typically begin at 100 to 500 units, accommodating both high-mix low-volume medical devices and high-volume consumer appliances.
We implement a continuous, pressure-sensitive perimeter adhesive seal (using genuine 3M 467MP, 468MP, or VHB systems) that surrounds all active switch cavities and electrical traces. Furthermore, our tail exits are routed through inner air-dam gaskets with optional potted silicone seals, preventing moisture siphonage via capillary action.
Yes. Ravo specializes in formulation and screen printing of carbon-paste and silver-interdigitated FSR arrays. These thin-film sensors measure variable dynamic compressive force for smart medical hospital beds, robotic grip monitoring, sports biometric wearables, and automotive seat occupancy detection.
Every production delivery is backed by comprehensive quality records: full Material Safety Data Sheets (MSDS), SGS test reports certifying compliance with UK/EU RoHS 3 and REACH chemical SVHC thresholds, Certificate of Conformity (CoC), and dimensional first-article inspection (FAI) reports.
We offer female crimp contacts with DuPont housings (standard 2.54 mm pitch), solder-free ZIF (Zero Insertion Force) contact fingers (1.0 mm, 0.8 mm, or 0.5 mm pitch with rear polyimide stiffeners), flexible polyimide FPC circuits, and direct surface soldering onto rigid FR-4 PCB backers.
Following CAD drawing and artwork sign-off, prototypes are produced and dispatched in 7 to 10 working days. Mass volume orders are completed within 15 to 20 working days. We utilize express air freight (DHL, FedEx, UPS) directly delivering to Glasgow or Edinburgh doorsteps within 3 to 5 business days.
