 EN
 DE
 FR
 ES
 RU
 JA EN DE FR ES RU JA
Engineered for High Precision, Environmental Durability, and Long-Cycle Reliability
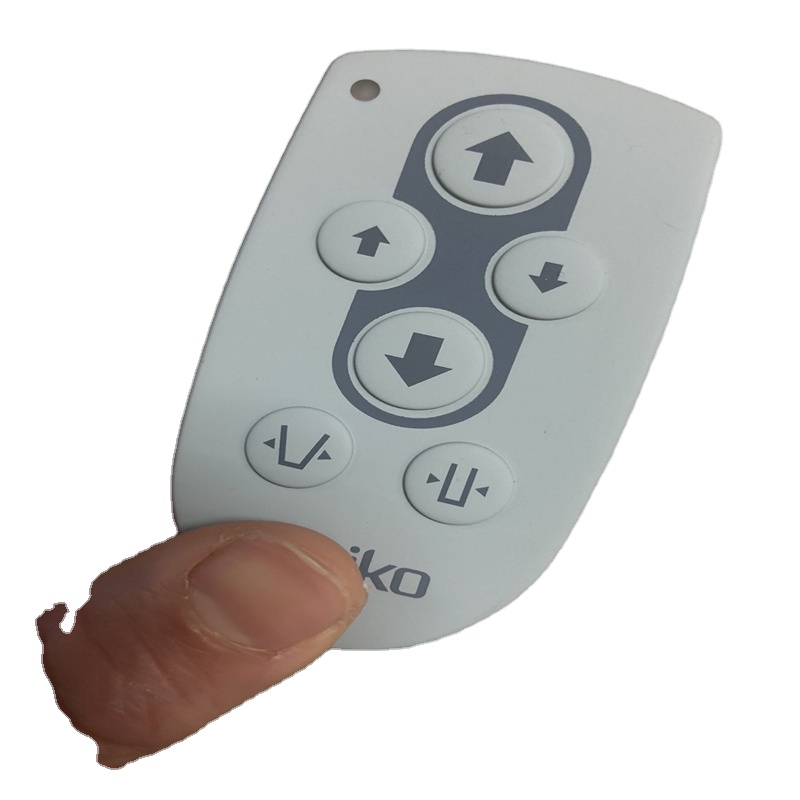
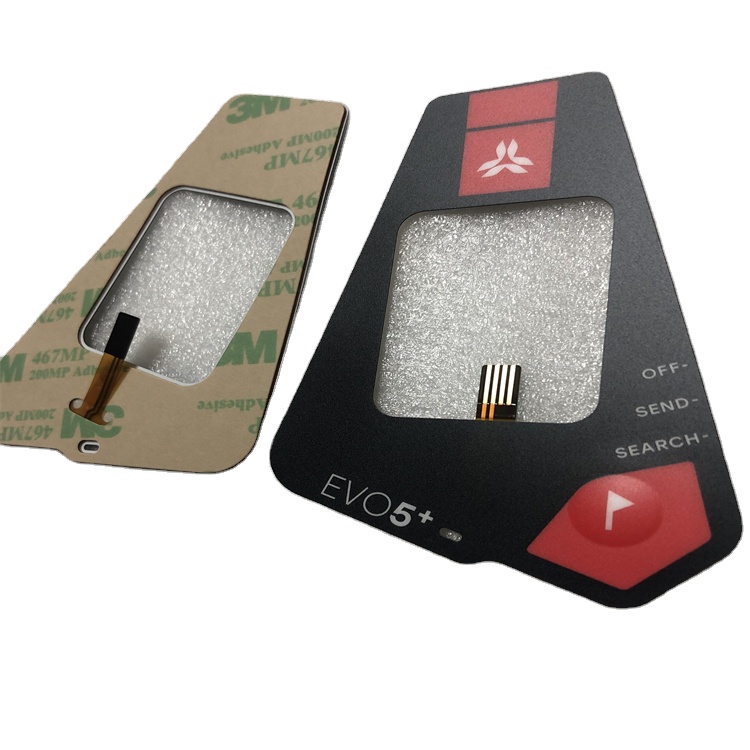
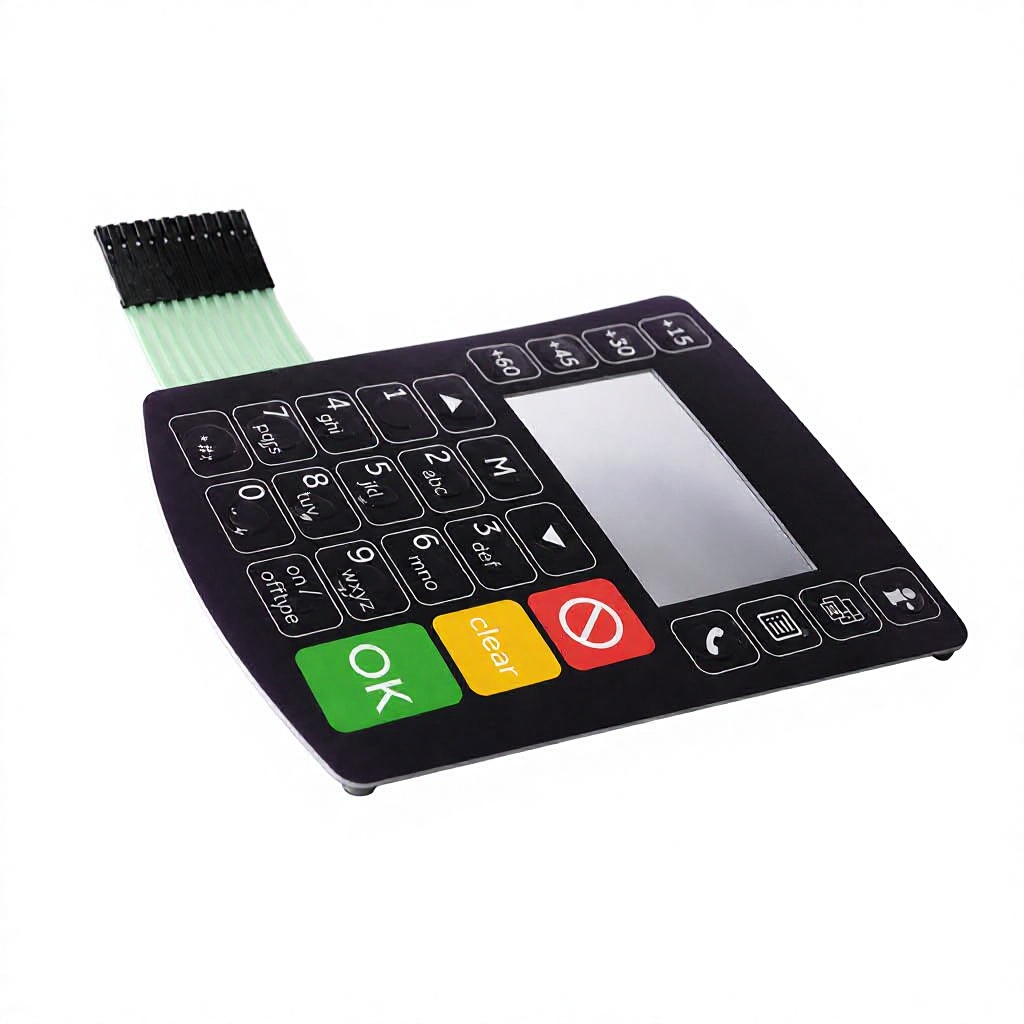
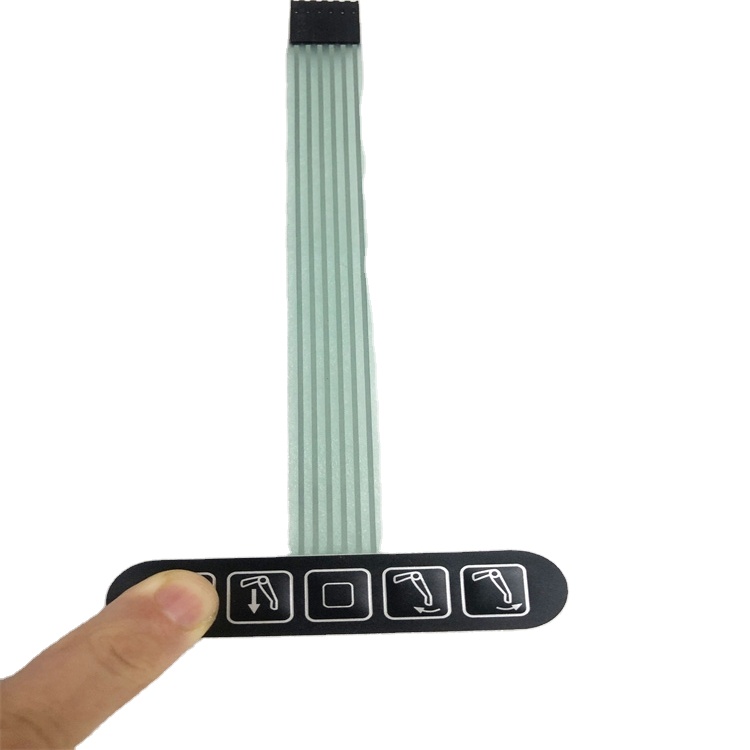
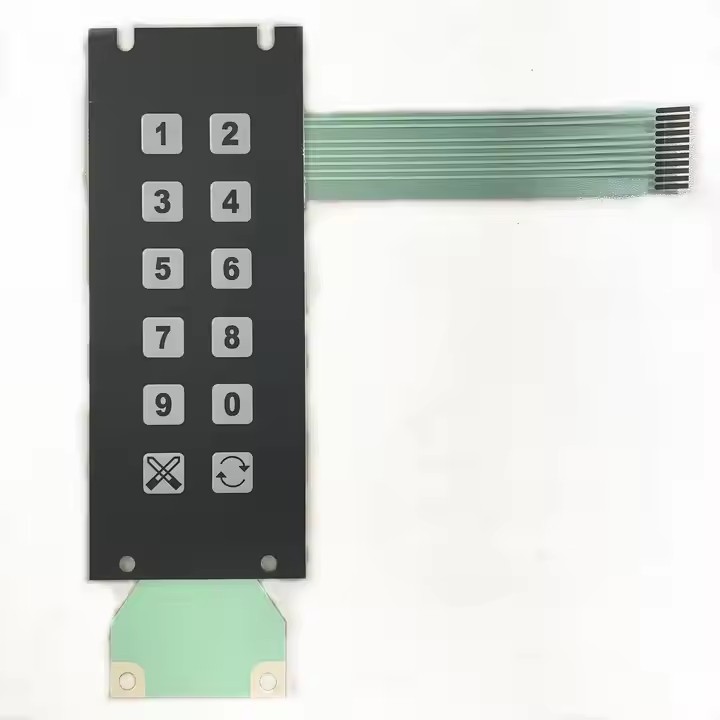
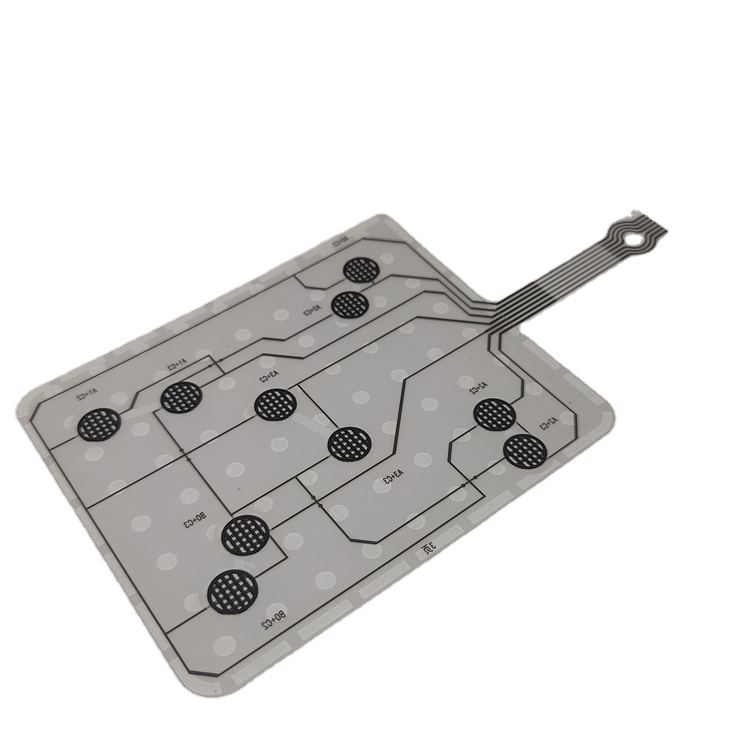
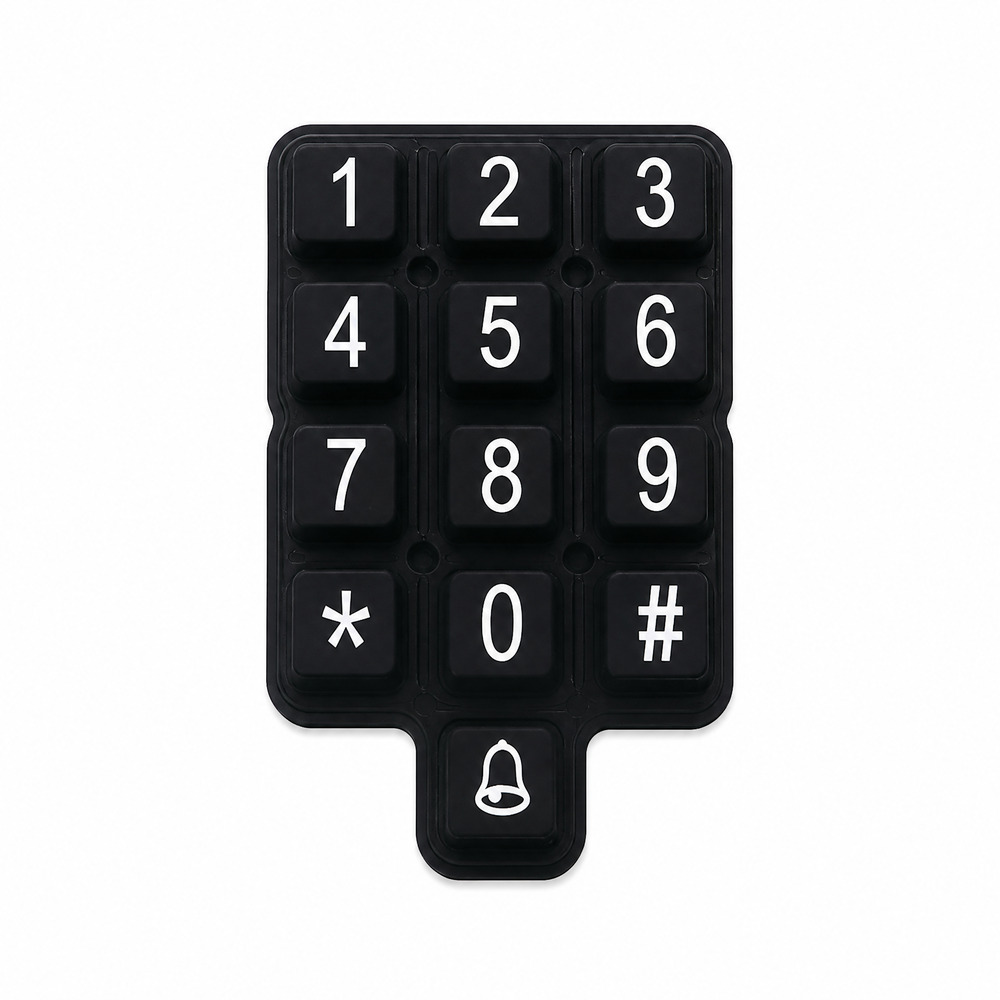
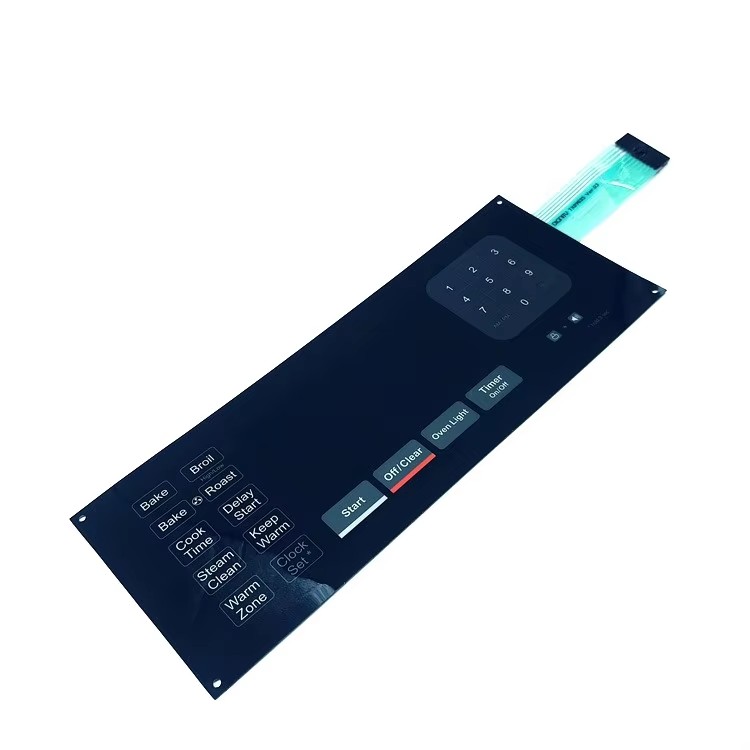
As the second-largest municipality in North Macedonia and a vital industrial engine of the Pelagonian statistical region, Bitola is undergoing a decisive technological transition. Historically grounded in heavy thermal energy production, agricultural processing, and textile manufacturing, Bitola’s industrial footprint is modernizing rapidly. Industrial zones such as Žabeni (Industrial Zone Zabeni) have positioned Bitola as an attractive destination for foreign direct investment (FDI), automotive component sub-assembly, specialized electronics manufacturing, and sophisticated process automation.
At the center of this industrial modernization is the demand for highly reliable Human-Machine Interfaces (HMIs). Modern control systems operating within severe industrial environments—ranging from the high-dust ambient conditions near the REK Bitola energy complex to strictly sanitized food processing units and precision medical device assembly lines—require user interfaces that guarantee physical resilience, zero-drift electrical conductivity, and clear visual guidance under low-light or night-shift operational settings. Illuminated membrane switches have emerged as the gold standard interface technology, seamlessly unifying active tactile feedback, backlighting aesthetics, and IP65–IP67 perimeter environmental sealing.
Selecting the correct illumination methodology is crucial when engineering custom keypads for Bitola's diverse OEM market. Suppliers and design engineers must carefully weigh factors such as power consumption, surface brightness uniformity, structural thickness, and mechanical endurance.
Surface-Mount Diodes soldered directly onto FPC or embedded in silver circuit layers offer high luminance, individual key status signaling, and exceptional operational longevity (>50,000 hours).
Utilizes ultra-thin micro-etched polycarbonate layers to channel light horizontally from side-firing LEDs, ensuring dead-uniform panel illumination with minimal vertical stack expansion.
A phosphor-impregnated dielectric layer emitting soft, uniform light across entire panels. Best suited for low-duty cycle, low-power applications requiring ultra-flat profiles.
The table below provides a engineering comparison of primary backlighting methodologies utilized in modern membrane keypads exported to North Macedonia:
| Illumination Parameter | Discrete SMD LEDs | Light Guide Film (LGF) + LED | Electroluminescent (EL) Panel | Fiber Optic Layering |
|---|---|---|---|---|
| Luminance Uniformity | Localized / Spot-lit | High (90%+ Uniformity) | Excellent (100% Uniform) | Very High |
| Thickness Added | 0.5mm – 1.2mm | 0.125mm – 0.25mm | 0.1mm – 0.2mm | 0.3mm – 0.5mm |
| Power Consumption | Moderate (20mA per LED) | Low (Side LEDs only) | Requires AC Inverter | Low (1-2 Light Sources) |
| Half-Life Expectancy | > 50,000 Hours | > 50,000 Hours | 3,000 – 5,000 Hours | > 50,000 Hours |
| Vibration / Shock Resistance | High (When encapsulated) | Exceptional (Solid-state) | High | High |
| Ideal Application Sector | Industrial Control Displays | Medical Instruments & Keypads | Aviation & Night-Vision Gear | Explosive/Hazardous Environments |
Understanding the precise mechanical and chemical stress vectors present in Bitola's local manufacturing base is critical for successful HMI deployment. Suppliers exporting to this market must customize materials according to specialized regional industry requirements:
The energy complex surrounding Bitola subjects electrical hardware to heavy coal dust accumulation, ambient temperature fluctuations (-20°C in winter to +40°C in summer), and industrial electromagnetic interference (EMI). Keypads engineered for power block interface consoles require:
Food and dairy production lines require rigid compliance with hygiene standards. Control interfaces on automated filling, sorting, and packaging machinery undergo high-pressure washdowns using caustic alkaline and acidic cleaning solutions. Keypad specifications demand:
Bitola’s expanding automotive component sector demands sub-assembly testing fixtures, custom diagnostic remotes, and robotic cell control boxes. These interfaces require compact **Flexible Printed Circuit (FPC)** backbones combined with high-density LED indicators, allowing complex circuit routing in space-constrained enclosures.
A rigorous review of the regional procurement landscape reveals three major engineering trends driving switch design across North Macedonia and broader Southeastern Europe:
Based on manufacturing scale, engineering responsiveness, international compliance (ISO 9001, RoHS, REACH), illumination capabilities, and export track record to Southern Europe, the following top 10 suppliers represent the leading partners for businesses in Bitola:
Competitive Advantage: Dongguan Ravo Electronics Co., Ltd. leads the global market in custom membrane switches, integrated illuminated keypads, capacitive touch panels, silicone rubber interfaces, and thin-film force sensors. Featuring an engineering response time of ≤2 hours, Ravo specializes in supporting Macedonian OEMs from 1-piece rapid prototyping to full volume production. Ravo provides comprehensive DFM (Design for Manufacturability) analysis, in-house screen printing, automated SMT LED placement, 100% electrical testing, and direct export logistics to Bitola, North Macedonia.
Renowned European supplier offering highly specialized tactile sensors, capacitive touch systems, and customized illuminated keypads for premium industrial and automotive applications across Southeastern Europe.
Specializes in distributing and assembling custom control panels, membrane keypads, and industrial display modules tailored for manufacturing facilities across North Macedonia and Serbia.
A major global player producing high-end input systems, illuminated metal switches, touchscreens, and membrane keypads suitable for critical medical telemetry and industrial plant consoles.
Provides custom membrane switch assemblies, LED backlighting products, metal domes, and specialized connectors specifically engineered for interface manufacturers and system builders.
Pioneers in high-durability thermoformed membrane switches, spring-dome technology, and illuminated capacitive overlays serving international equipment manufacturers.
Regional procurement partner supplying standard electronic components, industrial enclosures, and custom HMI front-panel overlays to regional industrial engineering firms.
Focuses on low-to-medium batch membrane keypad manufacturing, silk-screen graphic overlays, and backlight panel integration for commercial appliances.
Engineers robust control panels incorporating LED backlight guides, silicone rubber buttons, and rigid PCB backing for heavy machinery operators.
Delivers custom keypads, high-life snap domes, and thin-film pressure sensors optimized for outdoor vending, fueling stations, and security access devices.
While European distributors offer local proximity, Dongguan Ravo Electronics Co., Ltd. provides an unbeatable combination of direct factory pricing, advanced engineering capability, and manufacturing agility that modern North Macedonian businesses require to stay competitive globally.
Operating out of a 12,000 square meter state-of-the-art production facility in Dongguan, China, Ravo houses all critical manufacturing processes under one roof:
Ravo's dedicated engineering team evaluates incoming 2D/3D CAD drawings (DXF, DWG, STEP, AI) and provides a formal Design for Manufacturability (DFM) review within ≤ 2 hours. Our engineers verify circuit trace width, silver migration margins, dome travel clearance, LED current-limiting resistor values, and tail exit sealing—preventing costly revision cycles before tooling production begins.
Ravo exclusively partners with premier international material suppliers including Autotex (MacDermid), 3M Adhesives (467MP, 468MP, 9448A), Nicomatic Connectors, and Shin-Etsu Silicone. All products strictly comply with EU directives, fully backed by RoHS, REACH, and ISO 9001 documentation required for smooth customs clearance into North Macedonia and the European Union.
Partner with Dongguan Ravo Electronics Co., Ltd. for industry-leading illuminated membrane switches, rapid engineering reviews, and guaranteed quality.
Inquire Now