 EN
 DE
 FR
 ES
 RU
 JA EN DE FR ES RU JA
Precision-engineered HMI interface products manufactured by Dongguan Ravo Electronics Co., Ltd. for global export
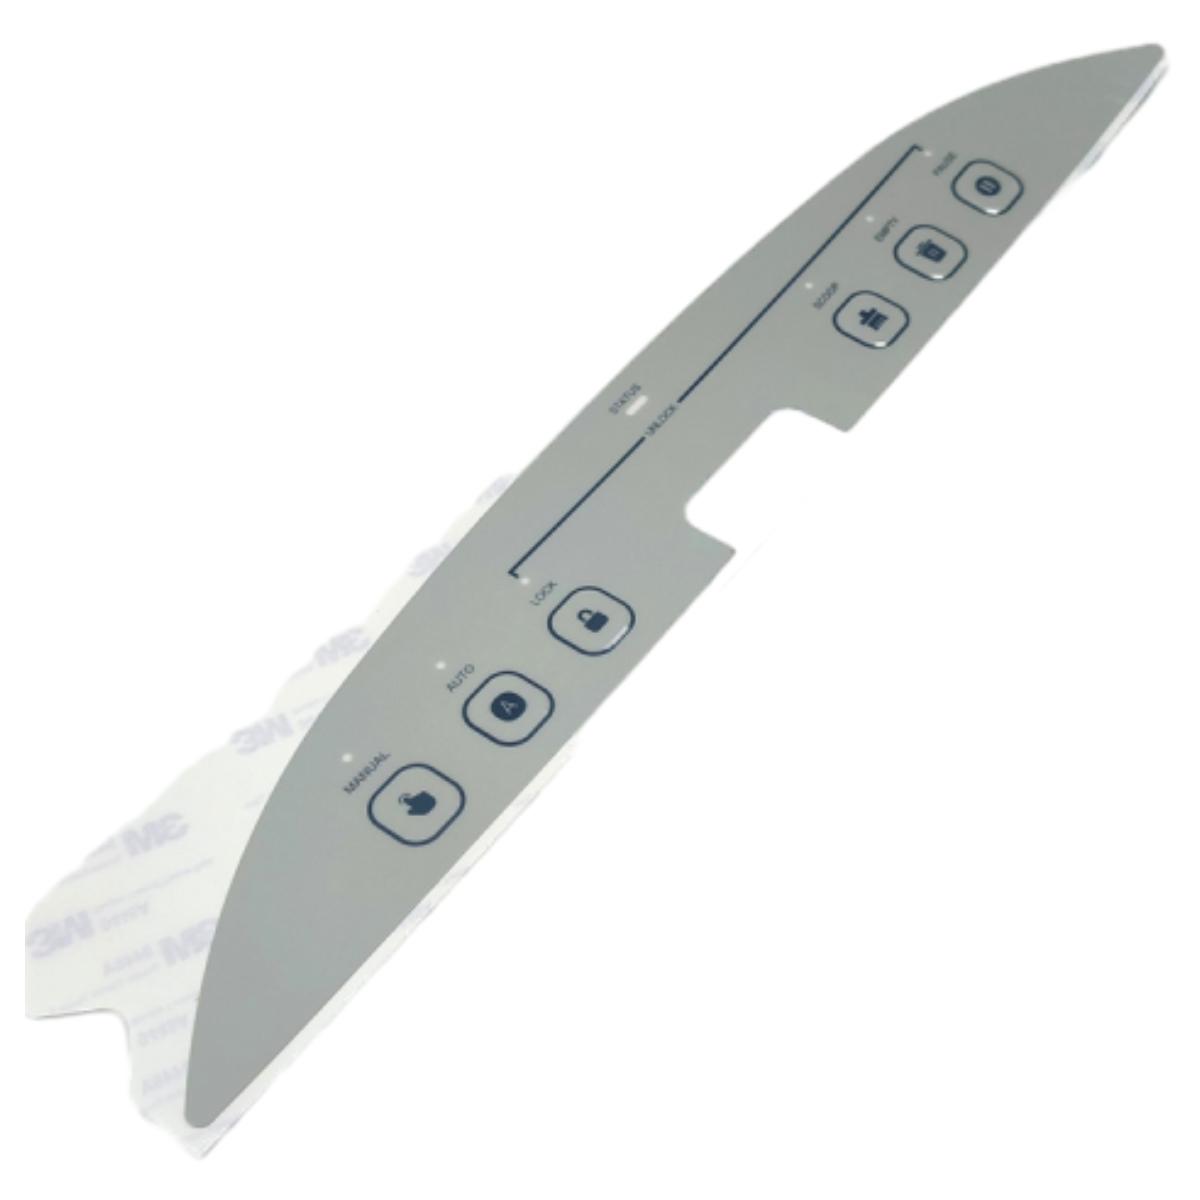
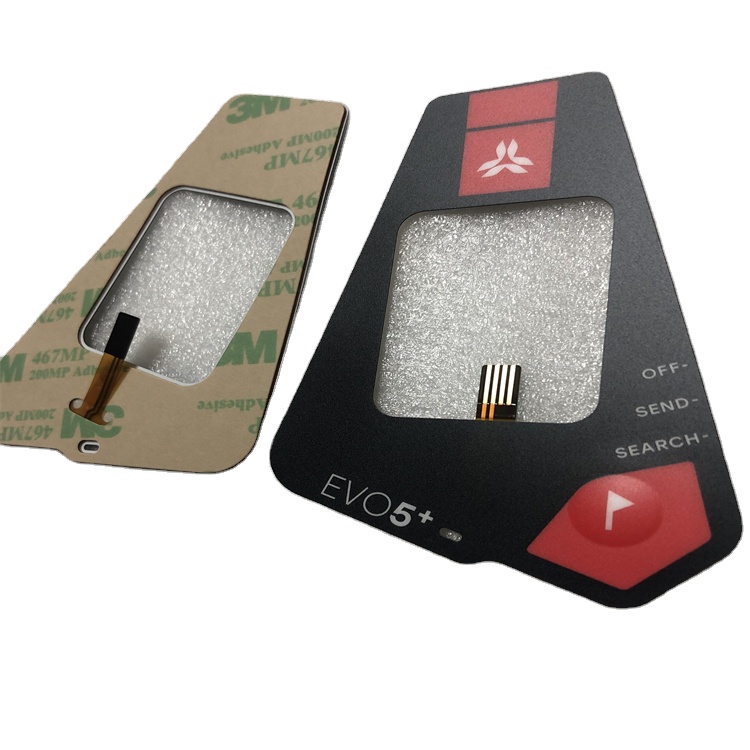
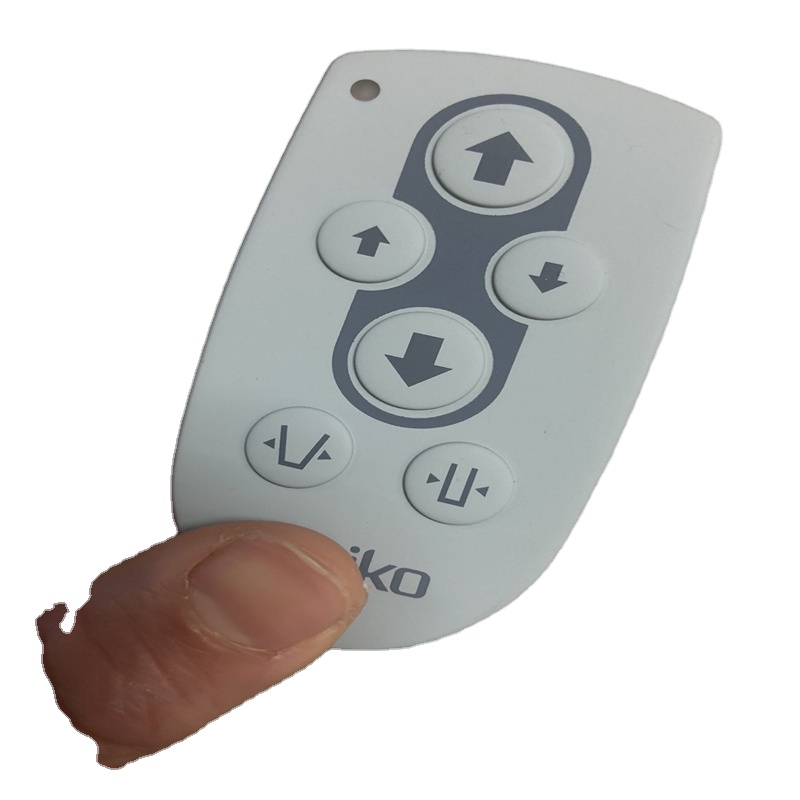
Operating electronic Human-Machine Interfaces (HMIs) in Jamaica presents a unique matrix of environmental challenges. Located in the heart of the Caribbean, Jamaican industrial, commercial, and hospitality equipment faces constant exposure to high ambient temperatures, elevated relative humidity (often exceeding 85% to 95%), airborne salt fog, and aggressive ultraviolet (UV) solar radiation. Standard electromechanical button arrays and unsealed mechanical keypads rapidly experience contact oxidation, short-circuiting from moisture ingress, tactile dome degradation, and graphic overlay yellowing under these harsh tropical conditions.
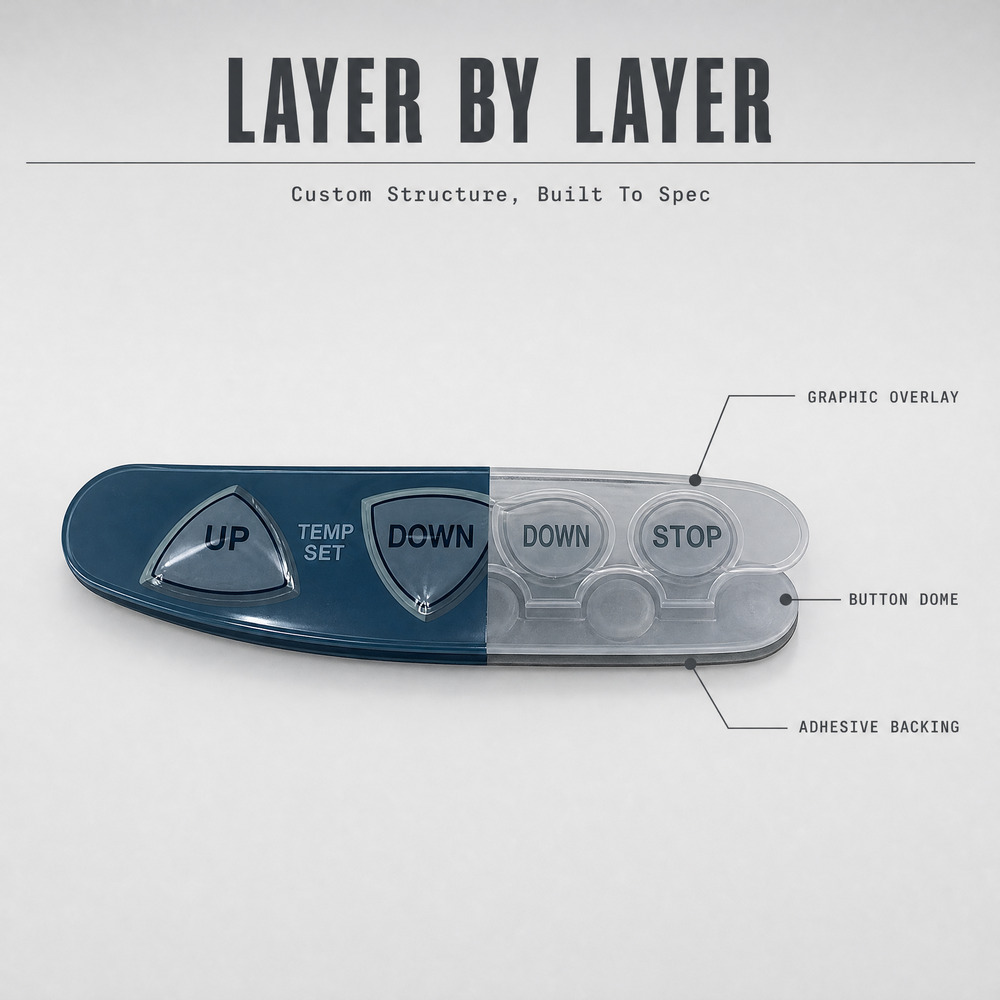
As a premier global OEM/ODM sealed membrane keyboard manufacturer and factory supplying Jamaica, Dongguan Ravo Electronics Co., Ltd. provides advanced, fully customized thin-film membrane switch assemblies engineered specifically to withstand Caribbean atmospheric stress. By combining multi-layer polyester (PET) or polycarbonate (PC) graphic overlays with full perimeter gas-gaskets, hydrophobic venting filters, conductive silver/carbon ink circuitry, and high-tack acrylic adhesives from 3M, our sealed keyboards deliver complete IP65, IP67, and IP68 ingress protection against fluid, dust, and corrosive aerosols.
Achieving reliable long-term performance in tropical industrial environments requires a meticulously designed multi-layer substrate architecture. Each layer serves a dedicated electrical, mechanical, or protective function:
Jamaica’s expanding economy demands custom HMI hardware built to local industrial standards. Our custom sealed membrane keyboards and control overlays are actively deployed across primary Caribbean sectors:
Deployable in regional hospitals and health centers across St. Andrew and St. James. Antimicrobial PET overlays allow seamless wipe-downs with harsh chlorine bleach and isopropyl alcohol sanitizers without damaging display windows or graphic legends.
Custom waterproof membrane keypads designed for outdoor resort equipment, spa controllers, commercial laundry units, and poolside digital kiosks in Negril, Montego Bay, and Ocho Rios, built to withstand chemical splashes and intense solar UV exposure.
Ideal for Jamaica's rum distilleries, sugar refineries, and beverage bottling plants. Sealed IP67 keypads prevent washdown fluid ingress during hot high-pressure cleaning cycles while resisting organic sugars and acidic wash chemicals.
Navigational instruments, crane control pendants, and cargo terminal interfaces operated around Kingston Port and Montego Bay Freeport. Features full salt-fog protection (tested per ASTM B117 standards) and integrated LED backlighting for night visibility.
As Jamaica expands renewable solar energy installations, our wide-temperature membrane switches (-40°C to +85°C operating range) protect solar microgrid inverters, battery management systems, and outdoor metering enclosures from thermal stress.
Vandal-resistant, high-actuation polydome or metal-dome membrane keyboards built for ticket dispensers, fuel pumps, and self-service retail kiosks operating under constant high-traffic usage throughout Kingston.
The manufacturing and commercial electronics landscape across Jamaica and the wider Caribbean Community (CARICOM) is undergoing rapid modernization. Key market trends accelerating the transition toward custom OEM sealed membrane keyboards include:
In the wake of global health consciousness and heightened sanitation standards in Jamaican tourism and medical facilities, physical push-buttons with open crevices are being replaced by completely flush, wipe-clean graphic overlays. Membrane keyboards offer flat or embossed surfaces that eliminate dirt traps, enabling 100% surface sterilization in seconds.
Jamaica’s agricultural processing initiatives—ranging from coffee bean processing in the Blue Mountains to automated poultry and produce packaging facilities—require reliable automation controls. Machinery operators working in dusty or humid packaging environments require tactile feedback with gloves on, driving high demand for custom embossed keypads with stainless steel metal domes.
Modern equipment designers in Jamaica are adopting hybrid membrane switches featuring integrated surface-mount LEDs (SMD LEDs), dead-front optical display windows, capacitive touch channels, and flexible copper FPC tails. This allows sleek aesthetic design combined with robust industrial reliability.
When specifying a custom OEM/ODM sealed membrane keyboard for Jamaican industrial projects, selecting the appropriate substrate, circuit layer, and adhesive formulation is critical. Below is our engineering material comparison table:
| Parameter / Feature | Autotex PET Overlay (Recommended) | Lexan PC Overlay | Silicone Rubber Keypad Overlay |
|---|---|---|---|
| UV & Outdoor Resistance | Excellent (Autotex XE Grade) | Moderate (Requires UV coating) | High (Inherent weatherability) |
| Flexural Fatigue Life | > 5 Million Actuations | > 100,000 Actuations | > 1 Million Actuations |
| Chemical / Solvent Resistance | Resists alcohols, bleaches, fuels | Susceptible to aromatic solvents | High resistance to oils & fluids |
| Sealing Ingress Protection | IP65 / IP67 / IP68 Gas-Sealed | IP65 / IP67 Sealed | IP67 / IP68 Molded Seal |
| Circuit Substrate Options | Silver Ink PET / FPC Polyimide | Silver Ink PET / Rigid PCB | FPC / PCB / Conductive Carbon Pills |
| Backlighting Integration | SMD LED / LGF Light Guide Film | SMD LED Window Illumination | Laser-Etched Backlit Characters |
| Operating Temperature | -40°C to +85°C | -30°C to +75°C | -50°C to +180°C |
Established in 2003 in Fenggang Town, Dongguan, China, Dongguan Ravo Electronics Co., Ltd. has grown over two decades into an industry-leading manufacturer specializing in custom membrane switches, graphic overlays, silicone keypads, flexible printed circuits (FPC), and thin-film force-sensitive resistor (FSR) pressure sensors.
Founded in 2003, operating a state-of-the-art 12,000 m² facility staffed by over 300 skilled technicians and senior HMI engineers dedicated to precision fabrication.
Our engineering team provides comprehensive Design for Manufacturability (DFM) reviews and CAD drawing feedback within ≤ 2 hours, dramatically accelerating project lead times.
We support product designers and equipment engineers from initial concept to full production. Prototype sample orders are supported starting from 1 piece.
Strict quality assurance protocols utilizing 100% automated optical inspection (AOI), circuit continuity testing, actuation life cycle testing, and fully RoHS/REACH compliant raw materials.
In-house precision screen printing, automated laser cutting, CNC die-cutting, cleanroom assembly, silicone molding, and SMT surface-mount component placement under one roof.
14+ years of direct export experience supplying clients across North America, Europe, and the Caribbean, with specialized anti-static protective packaging and air/sea freight routing to Kingston and Montego Bay.
We ship custom membrane keyboards and keypads regularly to Kingston (Port of Kingston) and Montego Bay. Express air courier shipments (via DHL, FedEx, or UPS) typically arrive in Jamaica within 4 to 7 business days following production completion. For high-volume mass production orders, sea freight options are arranged via international logistics partners.
Our tropicalized membrane switches utilize closed-cell perimeter gaskets, non-hygroscopic Autotex PET overlays, and 3M LSE acrylic adhesives. All internal silver conductive circuit traces are encapsulated with a protective carbon overcoat to eliminate silver migration caused by atmospheric moisture and salt ions.
To begin a project DFM review, simply provide your 2D engineering drawings (Vector PDF, AutoCAD DXF or DWG, Adobe Illustrator .AI) along with artwork color specifications (Pantone color codes). If your design includes surface-mount components or embedded circuit tails, 3D STEP files or Gerber files are also welcomed.
Yes. We utilize high-precision color matching systems (Pantone Matching System PMS and RAL color standards) for both screen-printed and digitally printed PET/PC graphic overlays. Translucent or dead-front display windows, filter tints, and embossed company logos are fully supported.
We understand that custom industrial design requires validation. Ravo supports prototype sample builds starting from just 1 to 10 pieces. Mass production MOQs start flexibly at 100 to 500 units depending on layout complexity, circuit type, and backlighting requirements.
All raw materials used in our factory—including PET films, inks, stainless steel domes, and 3M adhesives—are fully compliant with RoHS and REACH regulations. Our IP67/IP68 sealed assemblies meet non-sparking low-voltage requirements suitable for intrinsic safety applications in industrial gas, beverage processing, and medical control panels.
Contact our senior HMI engineering team today for immediate DFM feedback, material recommendations, and competitive direct-from-factory pricing.
