EN
 DE
 FR
 ES
 RU
 JA EN DE FR ES RU JA
High-reliability tactile switches, waterproof overlays, and flexible pressure sensors customized for industrial deployment in Noro and regional maritime operational environments.
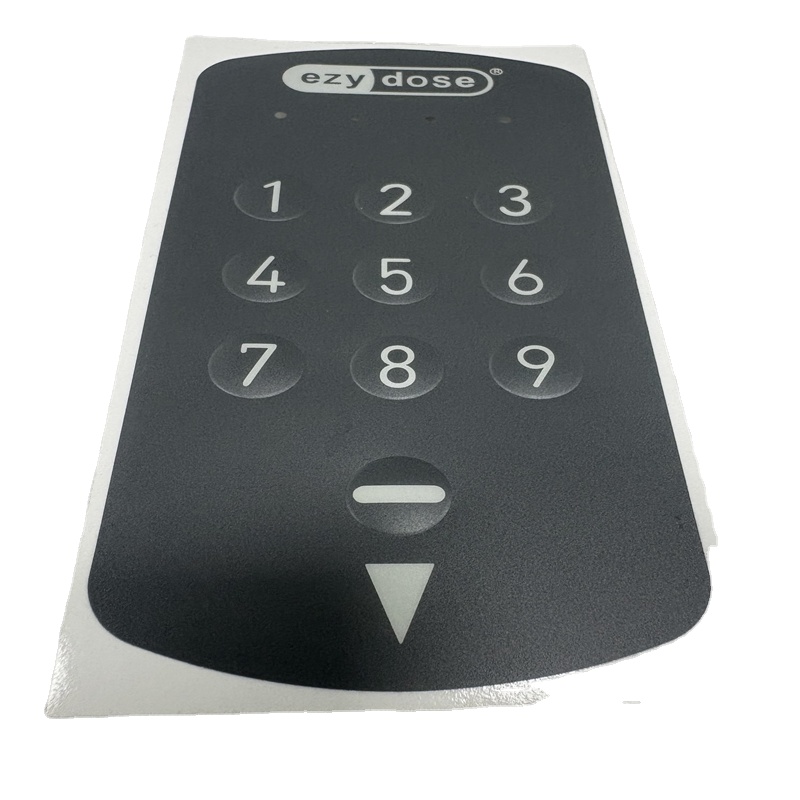
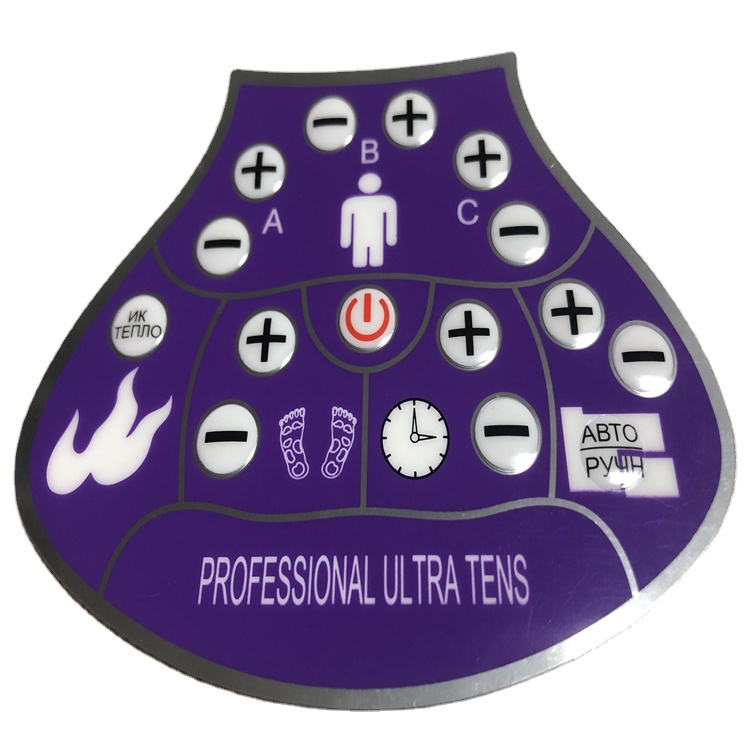
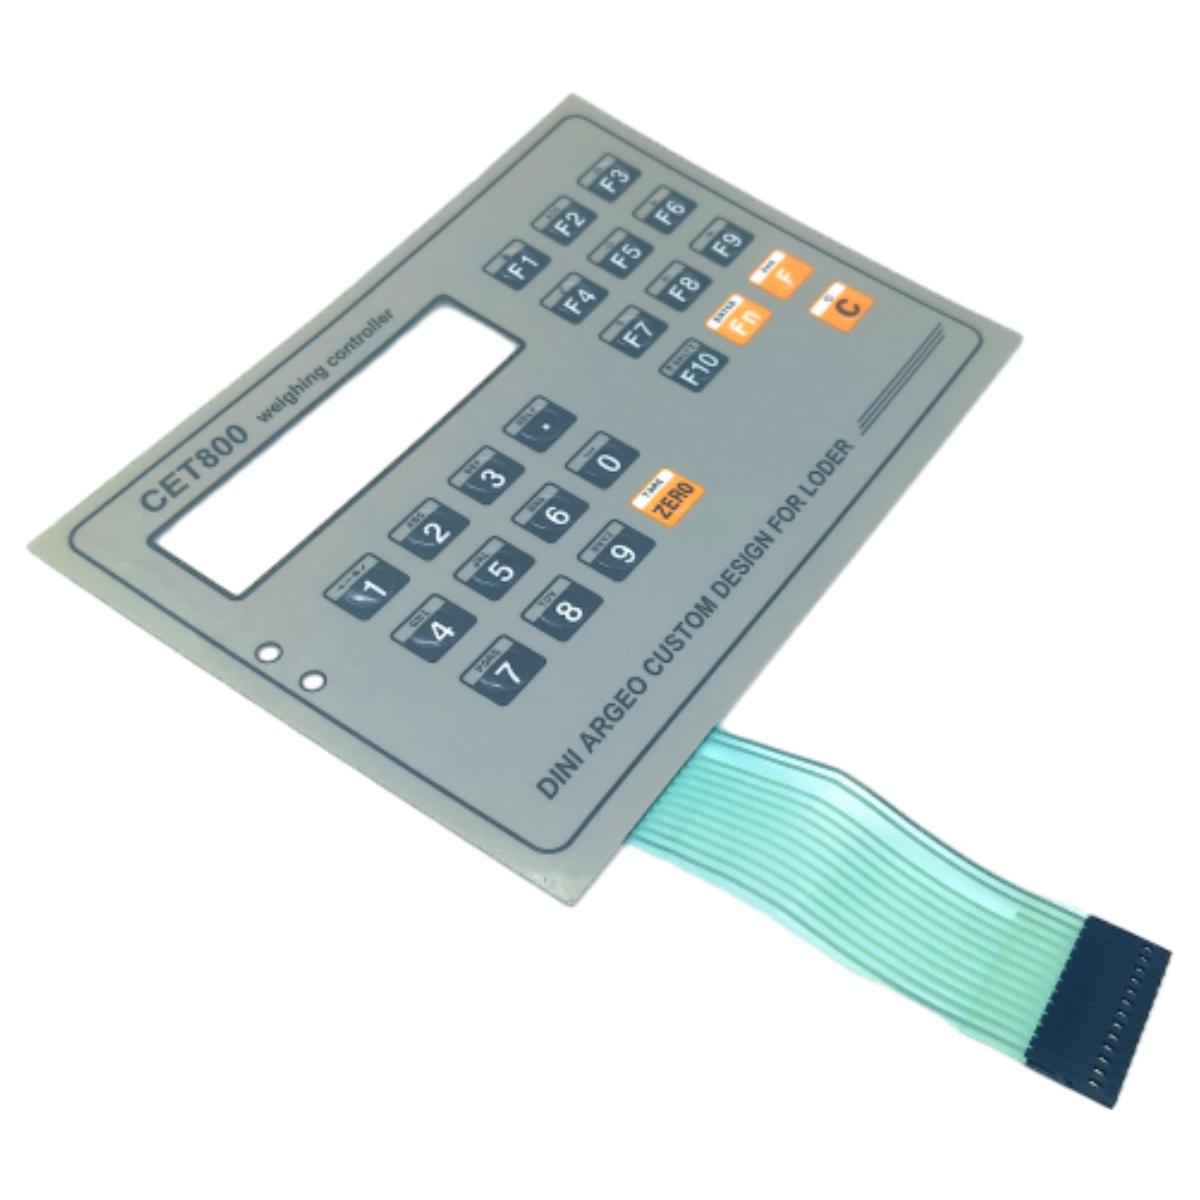
In modern industrial automation, marine port facilities, processing terminals, and severe climate environments—such as those encountered in Noro and surrounding tropical coastal zones—Human-Machine Interface (HMI) keypad panels represent the critical operational bridge between physical machinery and electronic control units. Delivering an optimal HMI switch assembly requires rigorous material science selection, multilayer planar stackup optimization, precise actuation force calibration, and total environmental sealing against ingress factors including high humidity, direct saltwater fog spray, petroleum distillates, and intense UV degradation.
Dongguan Ravo Electronics Co., Ltd. (established in 2003) engineers high-performance custom membrane switches, capacitive touch interfaces, silicone rubber keypads, reverse-printed graphic overlays, and thin-film pressure sensors designed to withstand extreme operational stresses. As an industry-leading OEM/ODM manufacturer, Ravo manages the complete production lifecycle within our 12,000 square-meter vertically integrated manufacturing facility in Dongguan, China, delivering engineered solutions that meet stringent global quality frameworks including ISO 9001 quality management, RoHS, REACH, and environmental ingress protection up to IP67 and IP68.
A resilient HMI keypad panel relies on a precision engineered, multilayer laminated construction. Each functional layer is selected based on chemical compatibility, mechanical shear resistance, surface energy, and thermal stability. The primary architecture typically comprises five to eight functional sub-layers:
Noro, located in the Western Province of the Solomon Islands, serves as a pivotal commercial port, deep-water maritime hub, and industrial fisheries processing center. Equipment deployed in and around Noro operates under demanding environmental conditions: continuous high humidity (>85% RH), ambient exposure to tropical heat, constant salt-fog mist, marine engine exhaust, and frequent high-pressure washdowns in food-grade processing facilities. Standard off-the-shelf mechanical switches quickly suffer from contact oxidation, seal breakdown, and mechanical failure under these conditions. Custom engineered HMI keypad panels supplied by Ravo directly address these localized technical challenges.
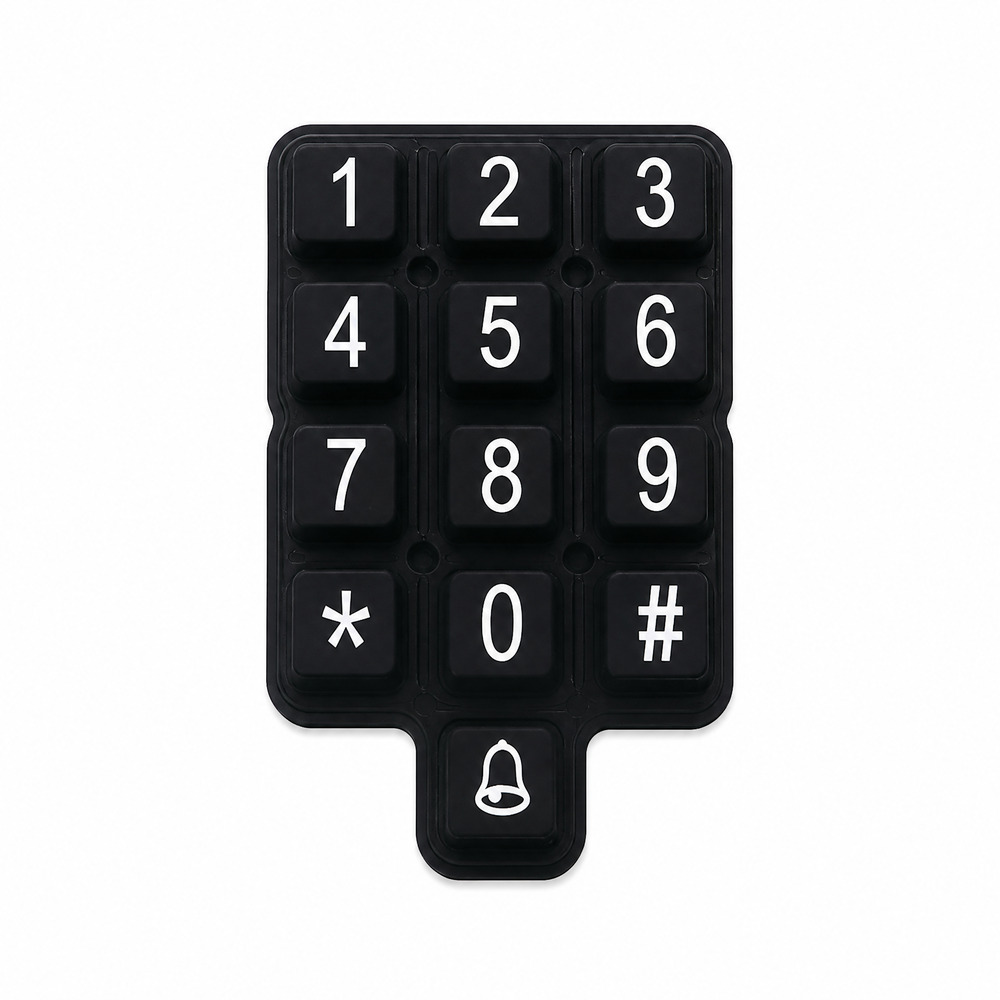
In maritime navigation units, cargo handling equipment, winch controls, and port cranes operating around Noro Harbor, HMI keypads must maintain absolute contact reliability despite salt-spray fog and tropical sun exposure. Ravo supplies custom silicone rubber keypads combined with hard-coated Autotex fine-matte PET overlays. The overlay features UV-blocking surface treatments that prevent yellowing and embrittlement under prolonged equatorial sunlight, while silicone boot surrounds form hermetic seals around the panel cutouts, completely preventing corrosive saltwater ingress into engine control modules.
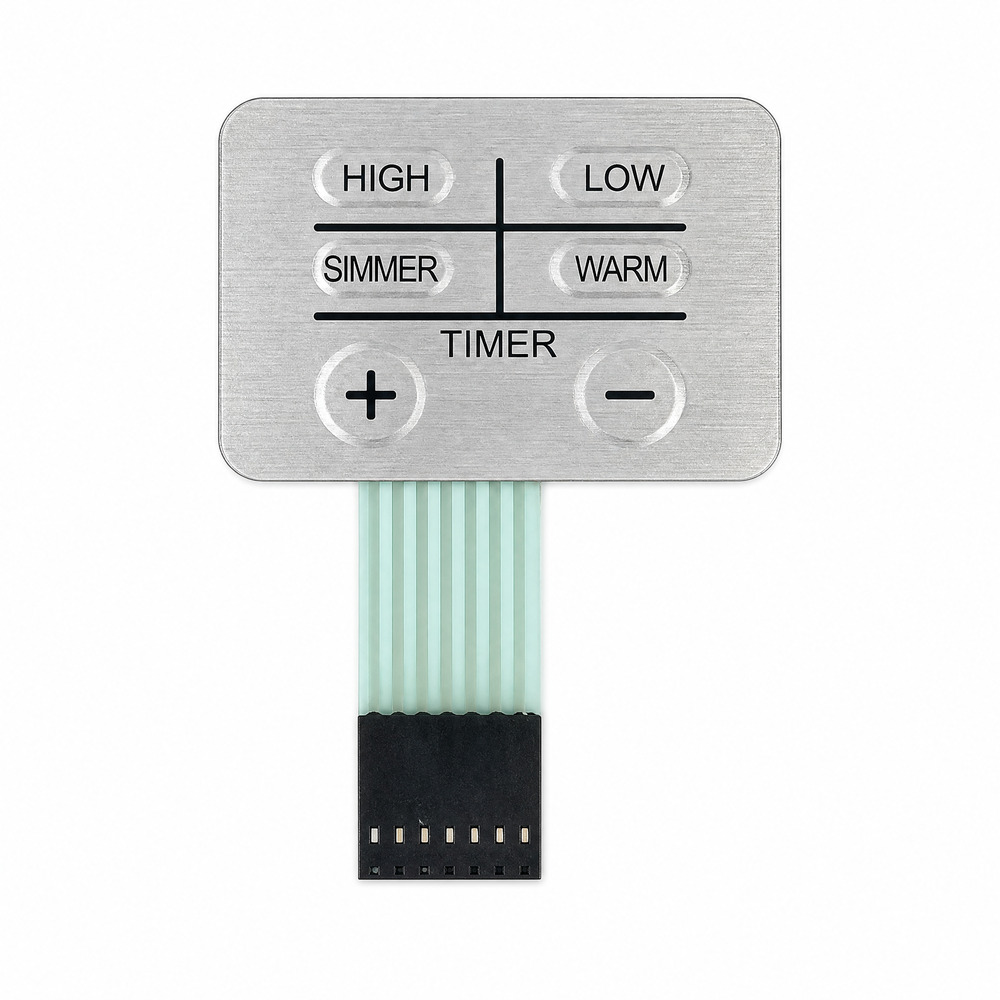
As home to major tuna processing and cold-storage operations, industrial facilities in Noro require HMI interfaces installed on automated fish-canning machinery, deep-freeze temperature loggers, and hygienic conveyor sorting lines. These panels must endure daily washdowns using high-temperature caustic chemical sanitizers. Ravo's reverse-printed, non-porous polycarbonate and polyester graphic overlays provide a completely flat, wipe-clean surface. With zero gaps or crevices, bacteria and organic matter cannot accumulate, while chemical-resistant 3M 467MP adhesive gaskets ensure zero delamination even under continuous thermal cycling from -40°C in blast freezers to +65°C during sanitation cleaning.
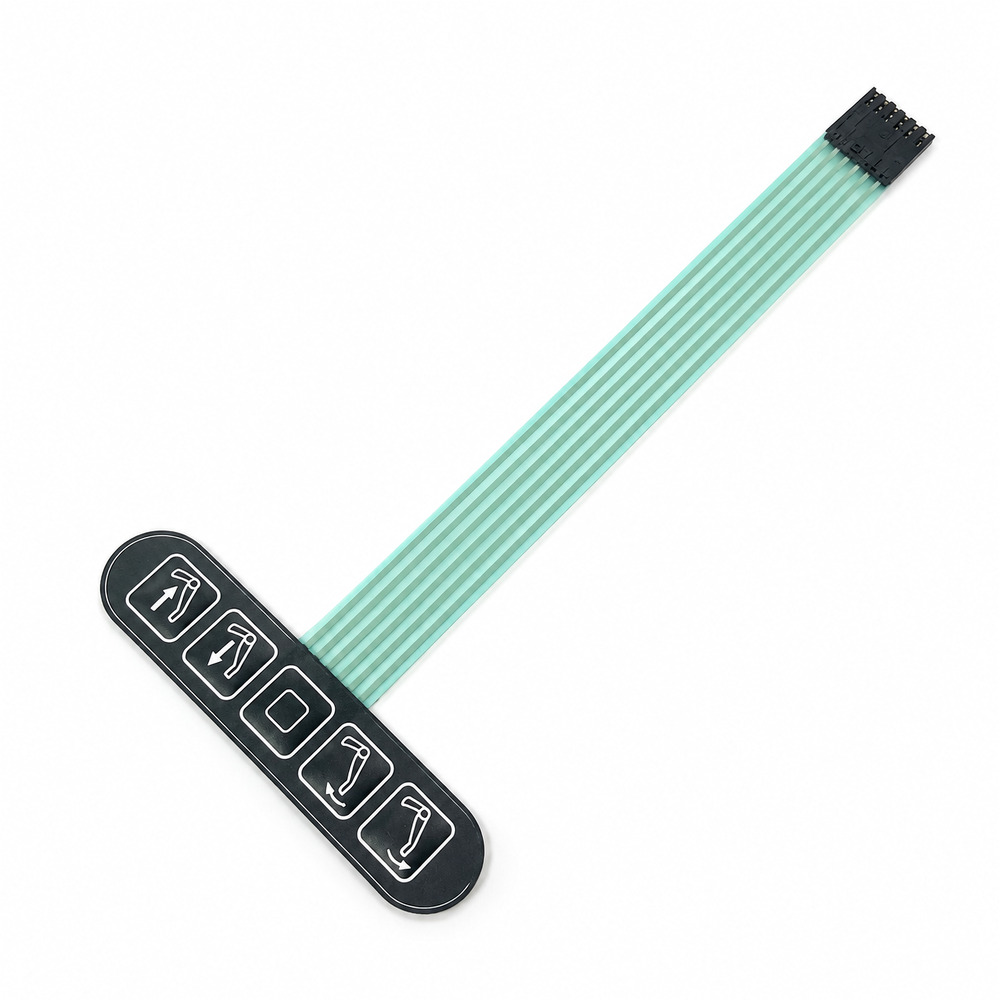
Infrastructure in island environments relies heavily on ruggedized power generation, diesel generator sets, and hybrid solar energy storage systems. Control panels for these power units require clear visual display windows, backlighting for nighttime emergency monitoring, and reliable tactile key switches. Ravo manufactures PCB-backed and FPC-integrated membrane switches featuring integrated SMD LEDs, light guide film (LGF) backlighting, and optically clear display windows with anti-glare anti-reflective hardcoats. These panels enable clear parameter reading under bright direct sunlight while guaranteeing operational responsiveness during utility outages.
Engineers and procurement teams serving Noro can evaluate key mechanical, electrical, and environmental characteristics using Ravo's design selection matrix below:
| Performance Parameter | Polyester (PET) Overlay Switch | Polycarbonate (PC) Overlay Switch | Silicone Rubber Keypad Assembly | Capacitive Touch HMI Panel |
|---|---|---|---|---|
| Actuation Life (Cycles) | > 5,000,000 flex cycles | > 1,000,000 flex cycles | > 2,000,000 button presses | Solid-state (Infinite) |
| Chemical Resistance | Outstanding (Alcohols, Acids, Solvents) | Moderate (Vulnerable to aromatic hydrocarbons) | Excellent (Oils, UV, Ozone, Saltwater) | Superior (Glass / Hardcoat PET face) |
| Tactile Operator Feedback | Crisp metal dome tactile click (200g-500g) | Thermoformed polydome or metal dome | Tactile snap dome effect (60g-300g) | Audible/Visual signal or Haptic motor |
| Ingress Sealing Rating | IP65 to IP67 perimeter sealed | IP65 to IP67 perimeter sealed | IP67 to IP68 full enclosure boot | IP68 / IP69K smooth wipe-down surface |
| UV / Solar Stability | High (with Autotex UV-treated grade) | Moderate (Requires UV hardcoat) | Excellent natural UV resistance | Superior (UV resistant glass cover) |
| Operating Temp. Range | -40°C to +85°C (-40°F to 185°F) | -30°C to +75°C (-22°F to 167°F) | -50°C to +200°C (-58°F to 392°F) | -20°C to +70°C (-4°F to 158°F) |
As industrial automation advances across developing port hubs in the Pacific Rim, local machinery operators and original equipment manufacturers (OEMs) servicing Noro are shifting away from legacy, un-sealed mechanical toggle switches toward fully sealed, integrated HMI keypads. Key market trends driving this transition include:
Traditional mechanical switches with open contact gaps are prone to swift corrosion due to ambient humidity and airborne sea salt in Noro. The industrial market is increasingly migrating toward solid-state capacitive touch membrane keypads. Capacitive touch interfaces eliminate moving mechanical parts entirely. Covered by an unbroken layer of heavy-duty glass, PMMA, or hard-coated polyester, capacitive touch panels are completely impermeable to fluid ingress, offer zero mechanical wear, and allow effortless surface disinfection in medical and food processing applications.
Nighttime port operations and low-light marine engine rooms require intuitive key illumination. Modern HMI panels designed for Noro increasingly incorporate Light Guide Film (LGF) or ultra-thin surface-mount LED backlighting coupled with "dead-front" graphic printing. Icons and text indicators remain completely invisible (blacked out) when unlit, illuminating sharply only when activated by the controller circuit. This prevents operator confusion during complex night operations and enhances panel aesthetic appeal.
With localized machinery maintenance requiring specialized, low-volume replacement panels or custom OEM upgrades, procurement managers in Noro cannot afford multi-month lead times or high minimum order quantities (MOQs). Ravo fulfills this critical industry demand by offering rapid Design for Manufacturing (DFM) engineering reviews within 2 hours, flexible prototyping starting from as few as 1 to 5 pieces, and rapid laser-cut tooling options that bypass expensive steel die investments during early-stage prototyping.
Dongguan Ravo Electronics Co., Ltd. brings over two decades of specialized manufacturing authority to the global HMI industry. Operating from our state-of-the-art 12,000 square meter production facility in Fenggang Town, Dongguan, China, Ravo provides end-to-end quality control, advanced manufacturing equipment, and direct-from-factory pricing advantages.
Unlike trading intermediaries, Ravo maintains full vertical integration under one roof. Our facility houses dust-free Class 10,000 screen printing cleanrooms, automated screen printing presses, high-precision laser cutting machinery, semi-automatic embossing presses, CNC die-cutting equipment, compression silicone molding equipment, and automated SMT pick-and-place lines for LED/resistor component placement.
Every single HMI keypad panel produced by Ravo undergoes rigorous testing before international export packaging. Our quality control architecture includes:
For custom prototyping and initial engineering verification, Ravo offers ultra-flexible MOQs starting from 1 to 10 pieces. For volume mass production runs, standard MOQs typically range from 100 to 500 pieces depending on the layer stackup complexity, circuit material (PET silver paste vs. FPC copper), and backlighting requirements. Small-batch custom production is fully supported to accommodate repair and maintenance schedules for local equipment in Noro.
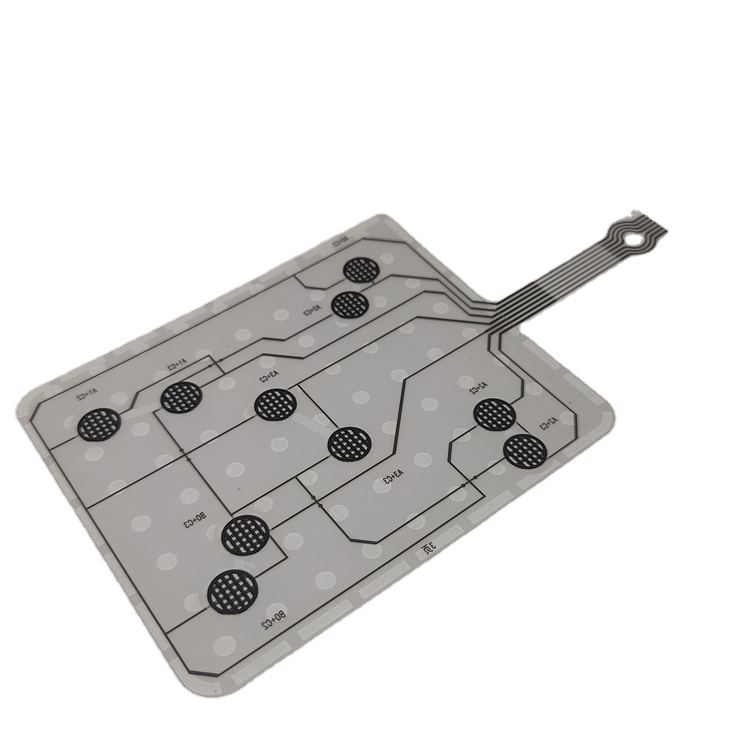
Silver migration occurs when moisture condenses on silver ink traces under DC voltage bias, causing silver ions to dendritically grow across traces and create electrical shorts. Ravo eliminates this risk by screen printing a protective, non-conductive carbon paste overcoat over all silver contact traces, utilizing anti-migration silver inks, incorporating full perimeter adhesive moisture seals (3M 467MP/468MP), and offering optional Flexible Printed Circuits (FPC) with polyimide coverlay protection for extreme high-humidity applications in tropical environments like Noro.
To provide an accurate quote and Design for Manufacturability (DFM) review, our engineering team requires: 1) Vector artwork files for the graphic overlay (Adobe Illustrator .AI, CorelDraw .CDR, Vector .PDF, or .DXF) with specified Pantone or RAL color codes; 2) Mechanical 2D/3D dimension drawings (.DXF, .DWG, .STEP); 3) Circuit schematic or pinout table; 4) Desired tactile feedback type (metal dome, polydome, or non-tactile); and 5) Operating environment parameters. Our engineers evaluate your files and return a complete DFM proposal within 2 hours during business hours.
Yes. For equipment operators in Noro working on fishing vessels, docks, or processing plants with heavy rubber or leather industrial gloves, Ravo designs keypads featuring large key target areas (minimum 12mm x 12mm), embossed key outlines (pillow or rim embossing raised 0.3mm to 0.5mm), and high-force stainless steel metal domes (350g to 500g tactile force). This combination guarantees that operators feel a distinctive, unmistakable tactile click even through thick protective gloves.
Ravo offers a wide array of tail connector options to suit your PCB header interface. For standard flex tails printed with conductive silver paste, we supply 2.54mm pitch female crimp connectors (FCI/Berg connectors with plain or latching housings) and 1.0mm, 1.25mm, or 2.54mm pitch bare-lead flexible tails for ZIF (Zero Insertion Force) socket insertion. For polyimide FPC circuits, fine-pitch surface-mount board-to-board connectors or soldered pin headers are integrated per engineering specifications.
Following design approval and drawing sign-off, prototype samples ship within 7 to 12 working days. Standard mass production orders ship in 2 to 3 weeks depending on quantity and material complexity. Ravo provides full export packaging, anti-static vacuum sealing, and express international air freight (DHL, FedEx, UPS) directly to destinations serving Noro, Western Province, and the Solomon Islands, complete with commercial invoices, customs documentation, and certificates of origin.
Connect with Dongguan Ravo Electronics' senior engineering team today. Get expert DFM feedback, complete technical material specs, and a fast direct-factory quote for your project serving Noro.