EN
 DE
 FR
 ES
 RU
 JA EN DE FR ES RU JA
Explore our factory-direct, high-durability interface assemblies custom engineered for medical, industrial, and commercial equipment operating in demanding climates.
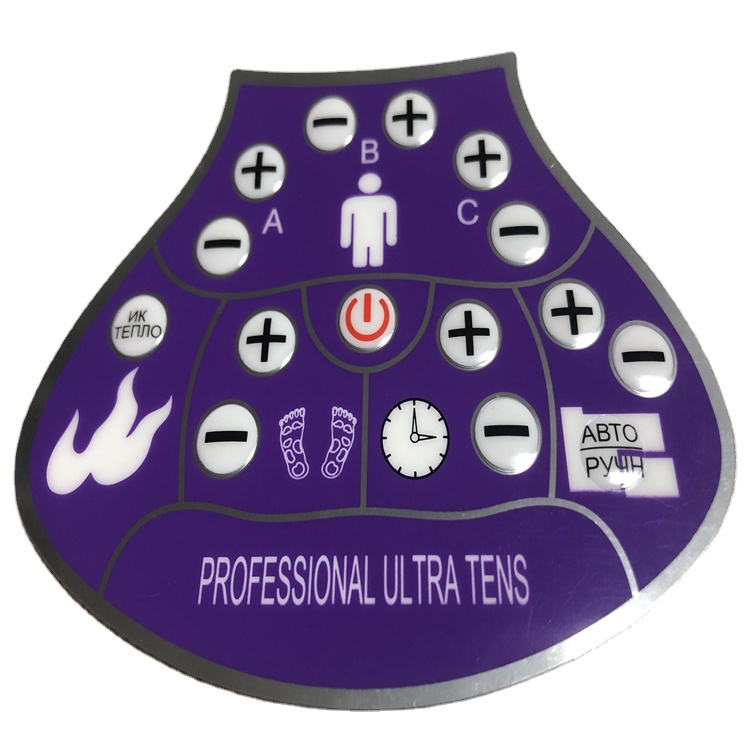
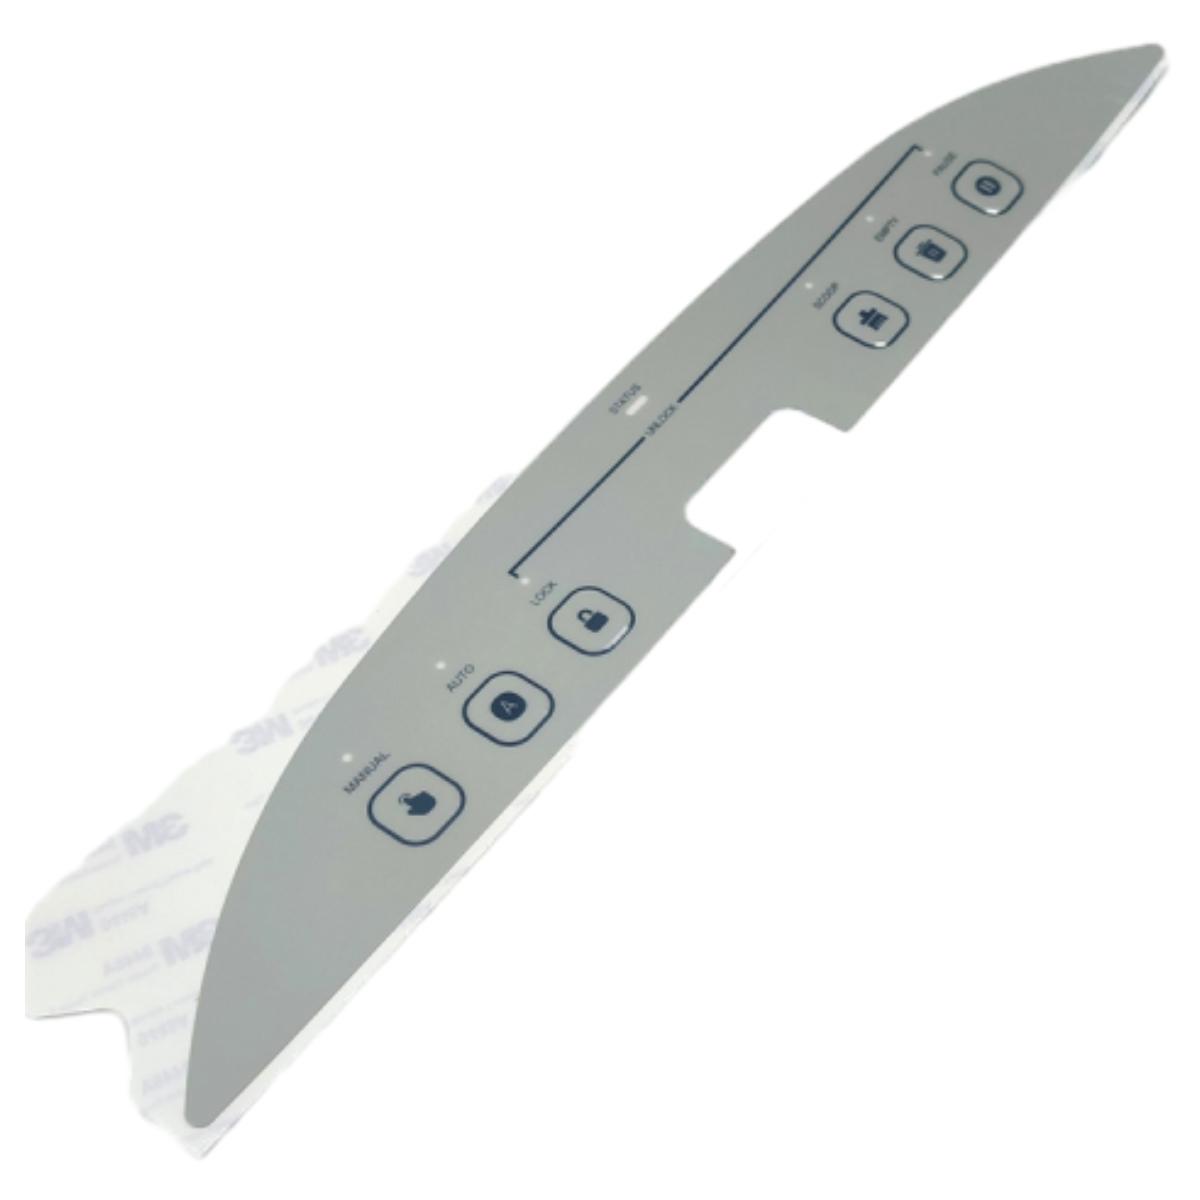
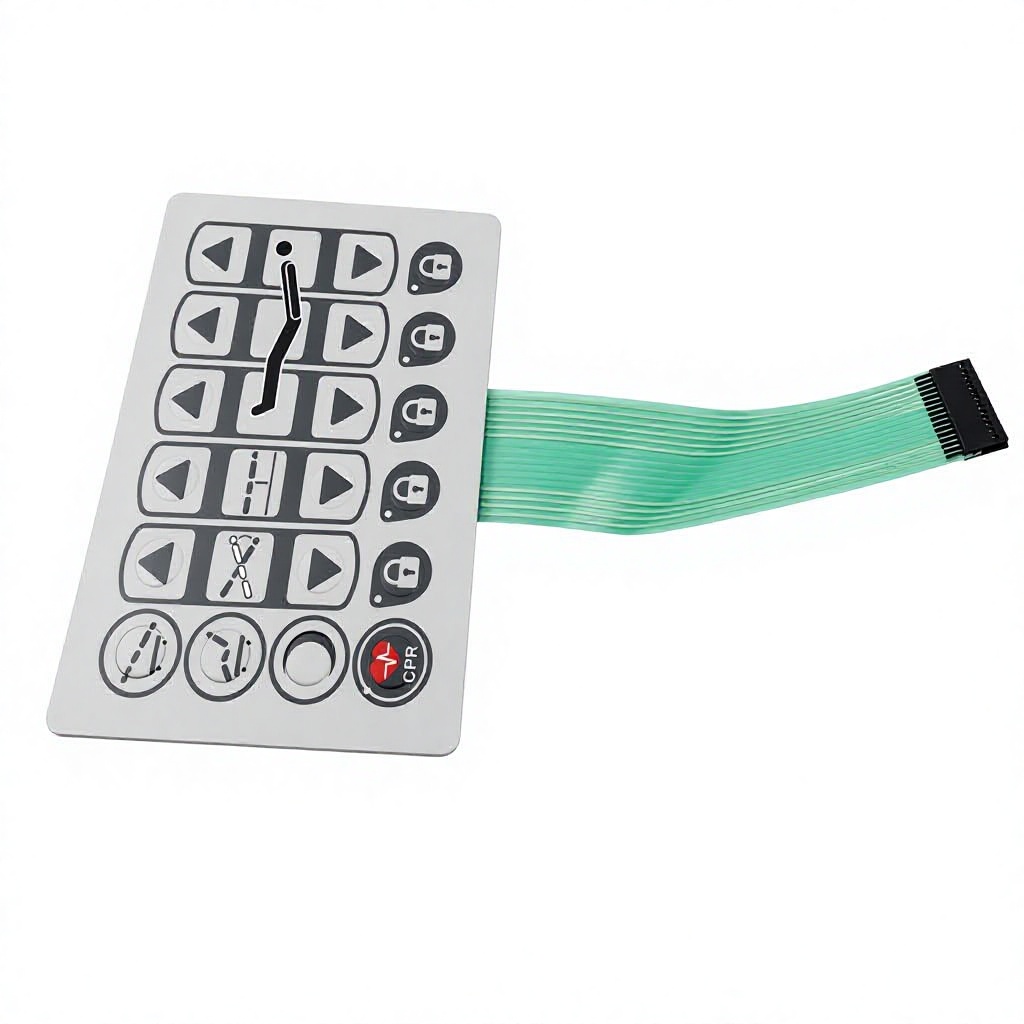
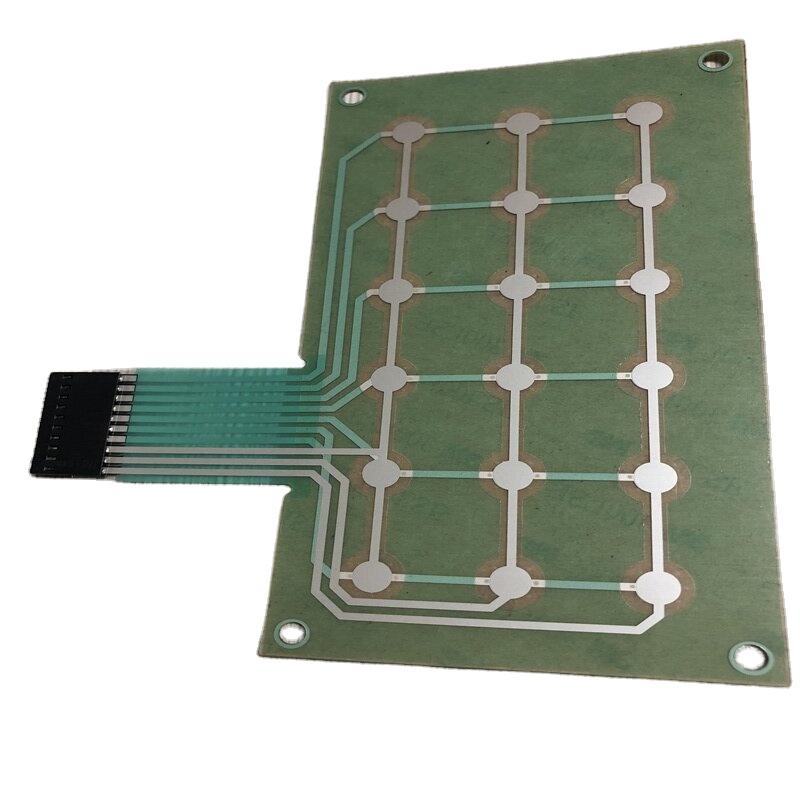
In the rapidly evolving industrial landscape of Eastern Cuba—anchored by the vital port city, manufacturing centers, and regional healthcare hubs of Santiago de Cuba—the demand for high-performance Human-Machine Interfaces (HMI) has expanded exponentially. Industrial machinery, agricultural processing lines, medical facilities, rum distilleries, and maritime control stations require custom control panel overlays and membrane keypads that deliver uncompromised operational safety, structural integrity, and long-term aesthetic fidelity.
As an established OEM/ODM pioneer, Dongguan Ravo Electronics Co., Ltd. (operating from our 12,000 square meter specialized manufacturing complex in Dongguan, China) supplies fully custom, CE-certified control panel overlays, capacitive touch keypads, graphic foil stickers, and flexible circuit switches explicitly engineered to thrive under harsh environmental constraints. This whitepaper details the engineering parameters, material selection frameworks, and localized applications critical for electrical engineers, system integrators, and procurement directors sourcing HMI assemblies for Santiago de Cuba and the broader Caribbean trade ecosystem.
Custom HMI Engineering Tailored to Key Regional Sector Demands
Santiago de Cuba serves as a regional medical center housing major institutions like the Hospital Provincial Saturnino Lora. Our CE-certified tactile membrane keypads and antimicrobial PET graphic overlays are integrated into patient beds, surgical tables, diagnostic analyzers, and lifters. Features include wipe-clean chemical resistance to isopropyl alcohol and bleach, IP65 perimeter water sealing, and embossed tactile buttons for error-free clinician input under high-stress conditions.
Home to world-renowned rum production and beverage bottling plants, local facilities require control interfaces immune to organic solvents, high atmospheric humidity, and frequent washdown cycles. Ravo manufactures custom acrylic, polycarbonate, and 3M adhesive-backed overlays resistant to alcohol vapor delamination, thermal spikes, and splash contact, guaranteeing long-term legibility and circuit reliability on automated bottling lines.
Operating along the Port of Santiago de Cuba demands interface hardware capable of enduring coastal marine atmospheric corrosion. Our waterproof silicone rubber keypads and UV-stabilized Autotex PET graphic overlays resist salt fog degradation, intense solar radiation, and mechanical abrasion on cargo cranes, marine engine room consoles, and municipal transport dispatch terminals.
Processing facilities across the Santiago region face fine airborne particulate dust, bagasse fibers, and continuous mechanical vibration. Ravo’s polydome and metal dome membrane switches utilize 3M 467MP high-cohesion adhesives and full perimeter gaskets to prevent dust ingress, delivering key actuation lifespans exceeding 1,000,000 cycles without contact degradation.
With Cuba expanding solar photovoltaic arrays to bolster energy resilience, local power inverter enclosures demand heat-resistant control panels. Ravo designs custom PCB-backed membrane switches and LED backlit front foils capable of continuous operation from -20°C up to +85°C, ensuring UV stability and anti-glare window clarity for outdoor monitoring panels.
As commercial tourism and automated retail expand across Santiago’s historic urban zones, public-facing vending keyboards require vandalism-resistant, splash-proof design. Our 0.125mm glossy PET membrane switches feature silver paste circuitry, tactile metal domes, and scratch-resistant hardcoats for effortless maintenance and high operational uptime.
Exporting control panel overlays to Santiago de Cuba requires an in-depth understanding of the region's distinct ambient stressors and regulatory compliance parameters. Unlike equipment deployed in temperate inland industrial sectors, HMI hardware installed along the Caribbean coastline faces a continuous combined attack of tropical atmospheric moisture (RH exceeding 85% year-round), salt-laden sea breeze, high ambient heat cycling, and elevated ultraviolet exposure.
In high-humidity coastal zones, standard screen-printed silver ink circuits are prone to micro-voiding and silver ion migration under continuous DC voltage bias, leading to short circuits. To counteract this failure mechanism, Ravo employs high-density conductive silver paste encapsulated with a dielectric protective overcoat. For critical applications, we utilize Flexible Printed Circuits (FPC) or Polyimide copper trace substrates with gold/nickel plating, delivering total immunity to atmospheric moisture penetration.
Standard grade Polycarbonate (PC) overlays degrade under direct sunlight, suffering from yellowing, embrittlement, and micro-cracking within months of Caribbean exposure. Ravo specifies textured polyester films—such as MacDermid Autotex XE (Extra Environment) PET—which incorporate built-in UV blocking chemistry. This material withstands prolonged tropical solar exposure without discolouration, loss of flexibility, or key actuation failure.
For equipment entering international markets or certified medical/industrial projects, CE compliance is mandatory. Ravo integrates full Electro-Static Discharge (ESD) shielding layers—utilizing printed carbon grids or continuous aluminum foil planes linked to ground tails—capable of shielding delicate microprocessor electronics from ESD events up to 15kV. All raw materials (inks, adhesives, PET films, domes) conform strictly to RoHS and REACH environmental standards.
| Substrate Material | Chemical & Solvent Resistance | UV / Outdoor Stability | Flexural Life (Actuations) | Recommended Application |
|---|---|---|---|---|
| Autotex XE Polyester (PET) | Excellent (Alcohols, Acids, Detergents) | Superior (Built-in UV Block) | > 5,000,000 cycles | Outdoor industrial control, Marine, Distilleries |
| Standard Polycarbonate (PC) | Moderate (Vulnerable to Aromatics) | Fair (Requires UV Hardcoat) | > 1,000,000 cycles | Indoor medical devices, Home appliances |
| PMMA / Optical Acrylic | Good (High surface hardness) | Good (Excellent clarity) | Rigid (Non-tactile overlay) | Instrument display windows, Touchscreen bezels |
| Silicone Rubber (Compression Molded) | Excellent (Hydrophobic, Washable) | Excellent (Wide temp range) | > 2,000,000 cycles | Surgical equipment, Heavy machinery keypads |
Founded in 2003, Dongguan Ravo Electronics Co., Ltd. has spent over two decades developing world-class HMI manufacturing systems. Our integrated facility in Dongguan, China combines precision tooling development, high-speed automated screen printing, clean-room surface assembly, embossing, laser die-cutting, and 100% electrical inspection under one rigorous ISO 9001 quality system.
Our engineering department delivers comprehensive Design for Manufacturability (DFM) reviews within 2 hours of receiving your DXF, STEP, or AI artwork files. Prototype builds are supported from as low as 1 piece to accelerate your product development cycle.
Every membrane switch and control overlay undergoes rigorous functional verification, including circuit resistance testing, insulation impedance checks, key actuation force mapping, and optical window clarity inspection before export packing.
Equipped with 14+ years of direct export experience, Ravo coordinates robust anti-static export packaging, custom documentation, and reliable air/ocean shipping options tailored for Caribbean ports and regional duty frameworks.
Essential Technical and Logistic Insights for Purchasing Managers and Engineers
All our custom control panel overlays and membrane keypads are manufactured under ISO 9001 certified quality management systems and strictly comply with CE marking mandates. We provide complete material declaration reports confirming compliance with RoHS, REACH, and UL94 flame retardancy standards upon request.
We specify premium tropicalized substrates, such as Autotex XE polyester, paired with high-cohesion acrylic pressure-sensitive adhesives (e.g., 3M 467MP, 3M 300LSE). Furthermore, we offer complete perimeter hydrophobic gaskets and dielectric-sealed silver traces to prevent moisture ingress and dielectric breakdown.
We support engineering development and field test trials with prototype MOQs starting from 1 to 10 pieces. Mass production minimums typically range from 100 to 500 pieces depending on stack-up complexity, selective embossing, and backlighting requirements.
Yes. We integrate surface-mount (SMD) LEDs directly onto flexible silver or FPC circuit layers for illuminated status indicators. Overlay display windows can be finished with transparent gloss, anti-glare, or dead-front (hidden-until-lit) selective tints for optimal LCD/LED display integration.
Our engineering team accepts vector graphic and CAD files including DXF, DWG, STEP, Vector PDF, and Adobe Illustrator (.AI). Please specify Pantone color codes, key embossing profiles, and tail connector pitch (e.g., 2.54mm or 1.0mm pitch).
Standard prototype samples ship within 7 to 12 working days following DFM drawing approval. Full volume production runs are completed within 2 to 3 weeks, followed by express air freight or consolidated ocean container logistics.
Request a comprehensive engineering evaluation, material sample kit, or instant quotation for your Santiago de Cuba projects. Our technical team responds within 2 hours with DFM optimization insights.
Send an Inquiry