Waterproof Membrane Switch Factory & Supplier serving Mixco

Engineering IP67 & IP68 Sealed Human-Machine Interfaces (HMI) for Industrial, Medical, and Outdoor Electronics across Guatemala and Central America

Featured Waterproof Membrane Switches & Custom Interfaces

Precision-engineered HMI solutions tailored for Mixco's manufacturing, commercial, and healthcare sectors
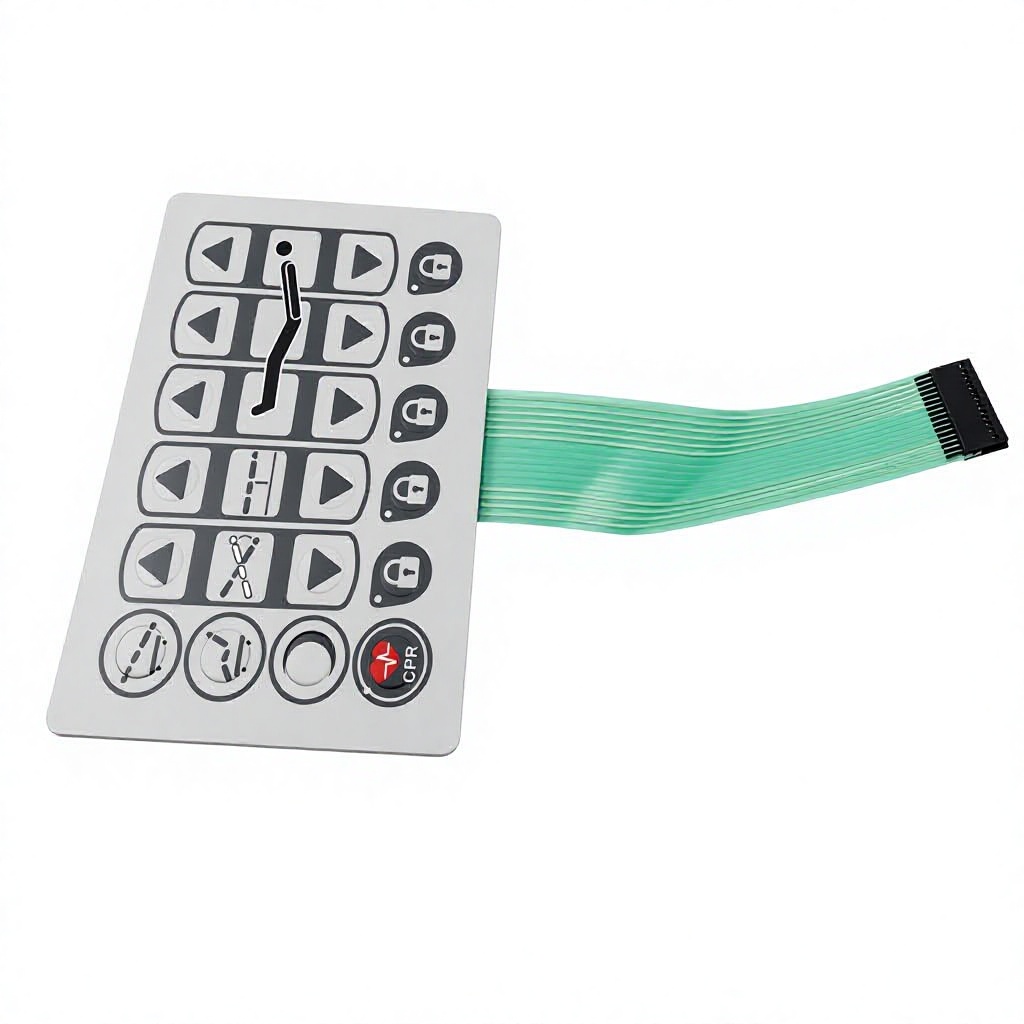
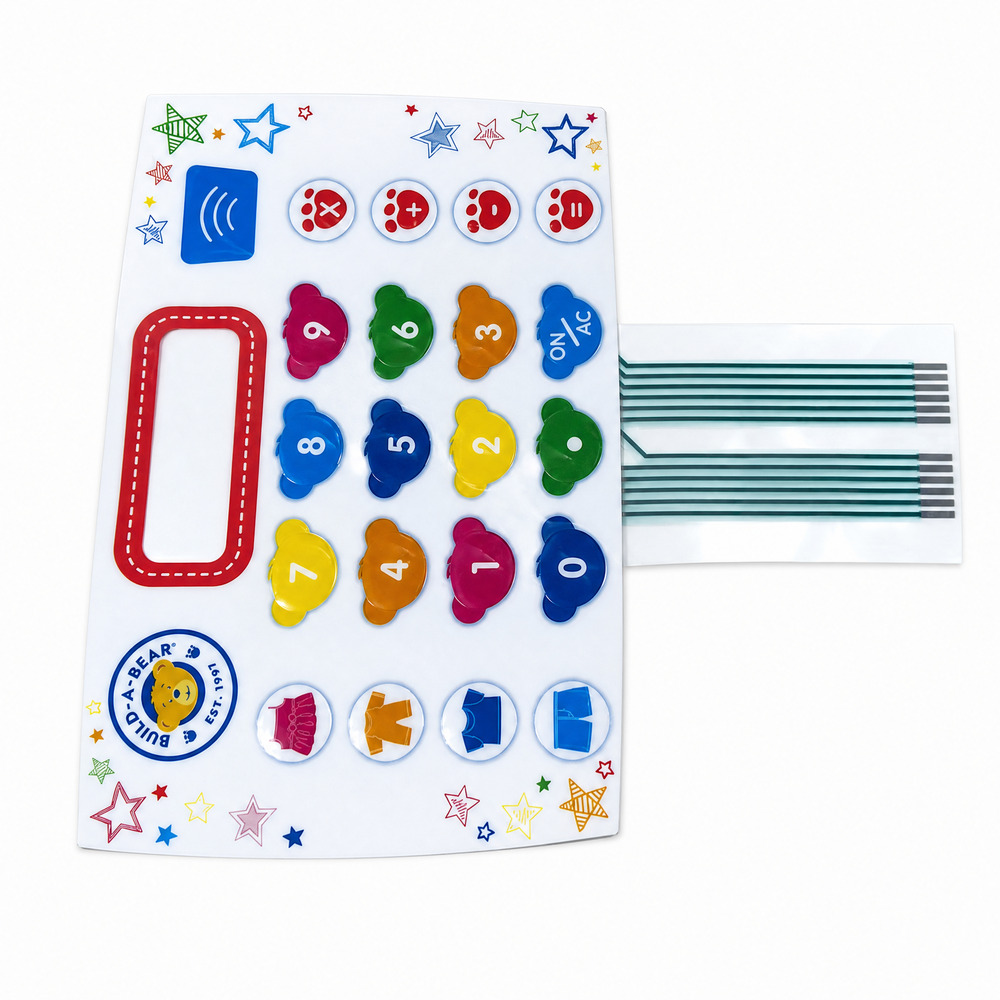
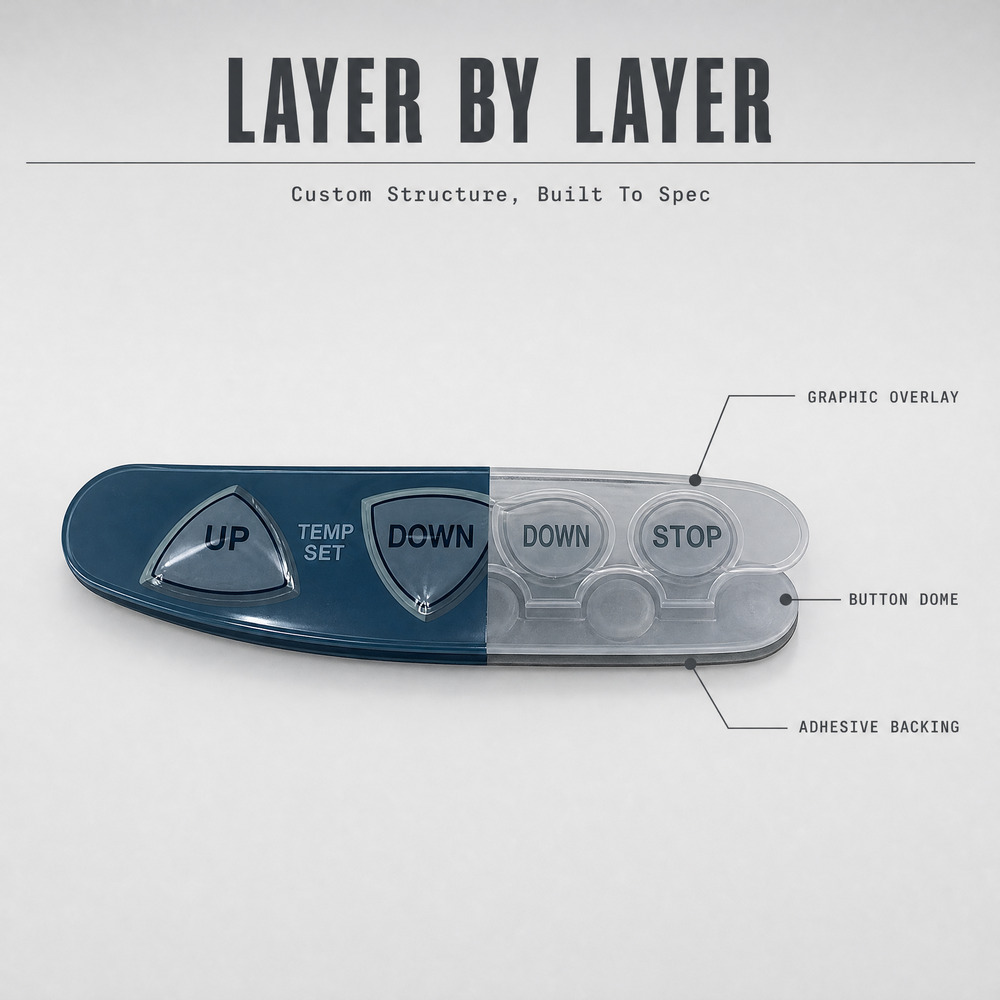
Medical Bed Membrane Keypad Tactile Switch
Antimicrobial overlay, tactile metal dome actuation, and IP67 perimeter moisture sealing designed for hospital beds, patient lifters, and clinical sterilizable tables.
View Product Details
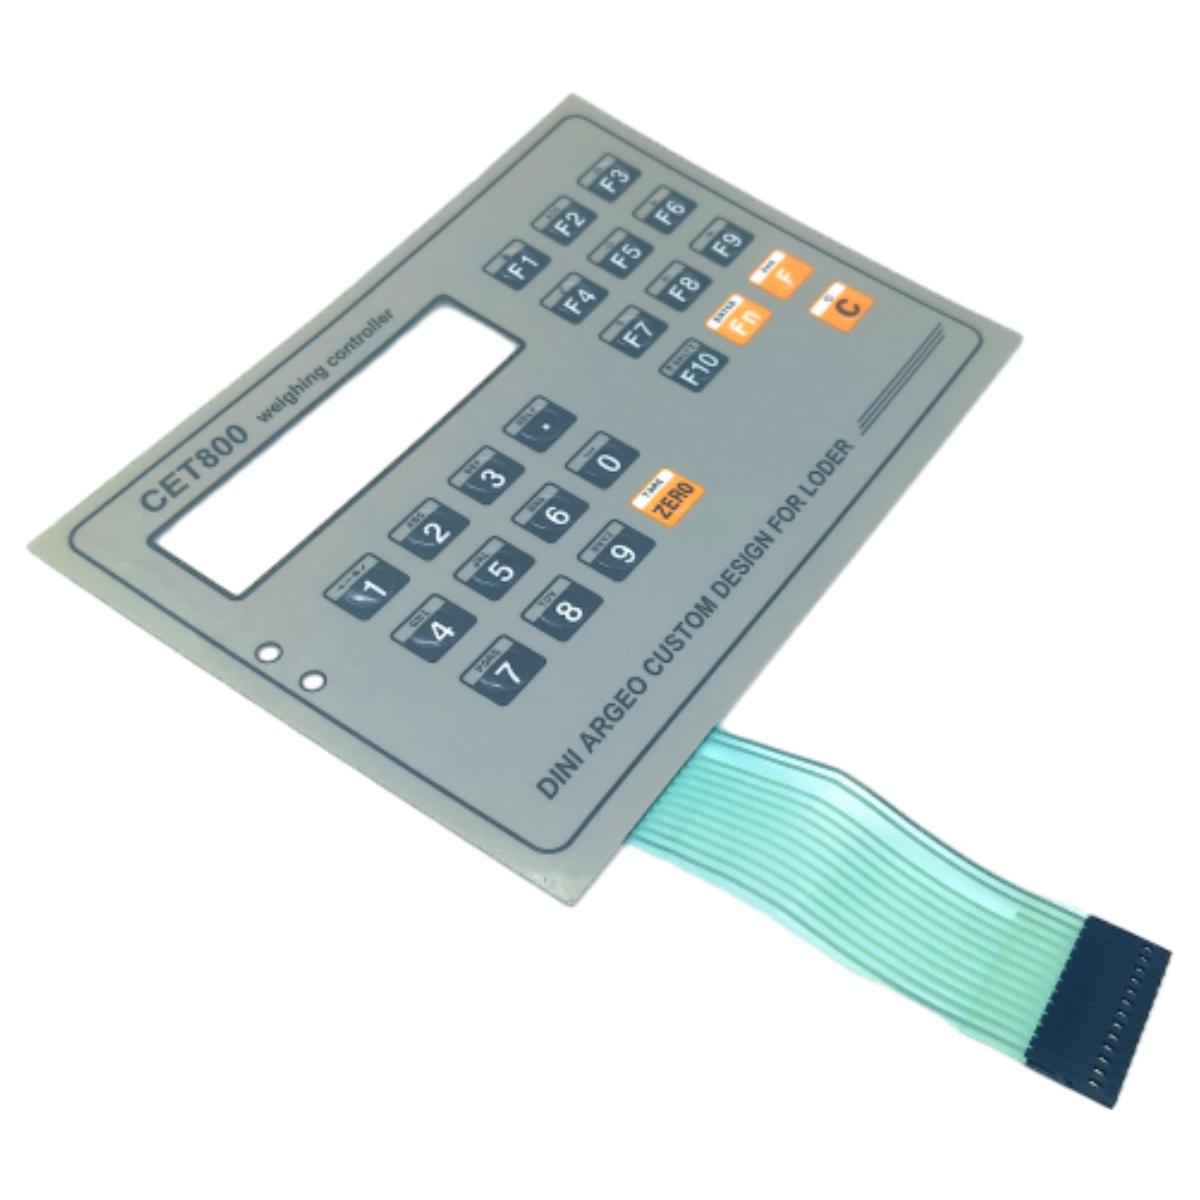
High Sensitivity Non-Tactile Membrane Switch
Ultra-thin conductive silver circuit with high touch responsiveness, customizable color graphic overlay, and robust long-life mechanical flexibility.
View Product Details
DIY Non-tactile Membrane Switch
Rapid prototyping flat panel layout with versatile connector tails, 3M adhesive backing, ideal for early-stage engineering validation in Mixco factories.
View Product Details
Custom Silicone Membrane Switch Overlay
Ergonomic compression-molded silicone rubber keys combined with membrane circuit layers, offering smooth tactile feedback and extreme temperature tolerance.
View Product Details
Prototype Silicone Membrane Keypads
Custom PET/Polycarbonate front graphics backed by 3M 467MP adhesive. Engineered for rapid turnarounds and low-volume custom production runs.
View Product Details
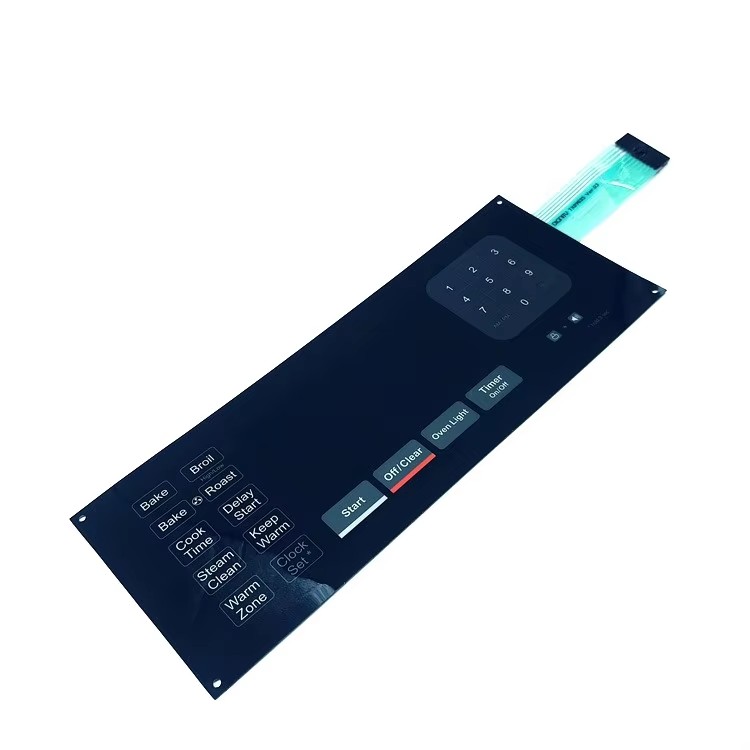
Matte Polycarbonate Reverse Printed Overlay
Scratch-resistant velvet matte Lexan overlay featuring sub-surface reverse silk-screen printing and crystal-clear LED/LCD display viewing windows.
View Product Details
Custom Membrane Switches & Silicone Parts
Full turn-key interface assembly combining flexible circuits, rigid PCB backers, molded rubber elements, and tailored surface finishes.
View Product Details
OEM Custom Tactile Waterproof Keypad
Industrial-grade waterproof control panel switch with stainless steel metal domes, IP67 environmental sealing, built for heavy machinery in humid outdoor settings.
View Product Details

Whitepaper: Engineering Waterproof & Tropicalized HMI Membrane Switches for Mixco's Operating Climate

Mixco, located in the Department of Guatemala, stands as one of the region's primary industrial and manufacturing hubs. Characterized by a subtropical highland climate with distinct rainy seasons, high ambient humidity levels, and varied industrial operating conditions—ranging from food and beverage processing plants in San Cristóbal to high-precision pharmaceutical labs and agricultural equipment assembly lines—the operational durability of Human-Machine Interfaces (HMIs) is under constant stress. Conventional mechanical keypads frequently fail in Mixco due to moisture ingress, oxidation of copper traces, dust particle accumulation, and aggressive surface sanitation regimes.

This technical whitepaper details the material science, structural engineering, and sealing architectures necessary to manufacture industrial-grade, waterproof, and chemically resilient membrane switches capable of delivering over 1,000,000 flawless actuations under high-humidity and washdown conditions.

IP67/68
Ingress Protection Rating
1M+
Actuation Cycle Expectancy
≤ 2 Hours
Engineering DFM Review
ISO 9001
Certified Manufacturing

1. Waterproof Sealing Architectures: Overcoming Humidity & Washdown Ingress

The core vulnerability of standard membrane keypads in tropical and washdown environments is the perimeter adhesive stack and the tail exit zone. Standard pressure-sensitive adhesives (PSAs) can degrade over time when exposed to persistent atmospheric humidity or liquid ingress during high-pressure equipment cleaning. Our factory employs a multi-tiered sealing protocol:

  • Full Perimeter Gasket Enclosure: Utilizing specialized closed-cell acrylic foam tapes or high-tack 3M 467MP / 3M 468MP adhesives die-cut into continuous, unbroken outer rings. This forms an impermeable barrier around the active electrical switch cavity.
  • Encapsulated Flexible Tail Exit: The flex circuit tail where electrical contacts exit the keypad housing represents a primary leak path. We implement UV-curable polymer potting, silicone boot potting, or internal labyrinth tail exits that redirect fluid away from internal silver traces.
  • Hydrophobic Venting Membranes: To prevent internal condensation caused by temperature changes within sealed equipment enclosures in Mixco, integrated micro-porous PTFE vents equalize internal and external pressure while repelling liquid water completely.

Substrate Selection: PET vs. PC

Polyester (PET, such as MacDermid Autotex) offers superior flexural fatigue resistance (over 5M flexes) and chemical resistance against alcohol and chlorine disinfectants, outperforming Polycarbonate (PC) in humid and sterile medical settings.

Silver Ink vs. FPC Circuits

While screen-printed conductive silver ink on PET provides an economical solution for most applications, Flexible Printed Circuits (FPC) with gold-plated copper traces eliminate silver migration risks under high voltage and constant humidity.

Tactile Feedback Mechanics

Stainless steel metal domes (four-leg or round configuration) supply a clear, audible snap with 250g to 450g actuation force—essential for machine operators working with heavy industrial gloves.

2. Technical Specifications & Material Performance Standards

Our manufacturing facility, Dongguan Ravo Electronics Co., Ltd., operates under strict ISO 9001 guidelines to maintain uniform electrical and mechanical integrity across all production batches shipped to Guatemala.

Parameter Silver Ink Circuit on PET Polyimide Copper FPC Circuit Rigid PCB Backer Switch
Operating Voltage / Current 30V DC / 100mA max 50V DC / 500mA max 100V DC / 1A max
Contact Resistance < 100 Ω (varies by tail length) < 10 Ω < 1 Ω
Insulation Resistance ≥ 100M Ω at 100V DC ≥ 500M Ω at 500V DC ≥ 500M Ω at 500V DC
Dielectric Withstand 250V RMS (50-60Hz 1 min) 500V RMS (50-60Hz 1 min) 1000V RMS
Operating Temperature -20°C to +70°C -40°C to +85°C -40°C to +105°C
Sealing Capability IP65 – IP67 IP67 – IP68 IP67 – IP68
ESD Shielding Printed Carbon or Aluminum Foil Solid Copper Plane Layer Multi-layer Ground Plane

Engineering Insight for Mixco Equipment Designers

When engineering interfaces destined for humid or unconditioned industrial plants in Central America, silver migration represents a primary cause of short circuits in silver-printed flex circuits. To eliminate this issue, our engineers specify minimum trace gaps of 0.5mm, apply dielectric overcoats over all conductive lines, and offer solid copper FPC layers for high-reliability applications.

Localized Application Scenarios in Mixco & Regional Guatemala Industry

Custom membrane switches and silicone rubber keypads manufactured by Ravo serve critical interface functions across specialized industry clusters within Mixco and surrounding industrial parks in Guatemala:

Medical Beds & Hospital Operating Tables

Deploying antimicrobial Autotex PET graphic overlays with metal dome actuation for bedside control units, surgical tables, and patient transfer lifters used in clinical facilities across Mixco and Guatemala City. Easy to wipe clean without graphic degradation.

Food & Beverage Processing Plants

Heavy washdown requirements in local bottling and food packaging lines demand IP67 sealed membrane keyboards equipped with 3M 468MP high-tack mounting adhesive. Prevents water and sanitizer ingress during daily line cleaning routines.

Agricultural Processing & Grain Sorters

Industrial machinery deployed in sorting coffee, sugar cane, and agricultural produce requires dustproof, scratch-resistant control panels. Matte velvet polycarbonate panels with reverse-printed graphics remain fully legible under harsh usage.

Commercial Vending & Ticket Kiosks

High-cycle non-tactile or polydome membrane keyboards with integrated LED backlighting and clear display windows, engineered to withstand constant public interaction and ambient solar exposure in municipal transport hubs.

Smart Home Appliances & HVAC Systems

Sleek capacitive touch switches and silicone rubber keypad overlays designed for modern residential control units, offering smooth capacitive touch control and dead-front backlighting effects.

Educational Toys & Remote Controllers

High-sensitivity non-tactile conductive circuits for interactive learning tablets and specialized wireless remotes, combining low unit cost with long-term mechanical flexibility.

Localized Development Trends in Mixco & Central American Manufacturing

The industrial market in Guatemala is undergoing rapid modernizations driven by international nearshoring investments, automated production lines, and strict hygiene protocols post-global pandemic. Several key technological trends are influencing HMI product sourcing across Mixco:

  • Shift from Mechanical Switches to Sealed Membrane Panels: Traditional push-button switches with mechanical crevices are increasingly replaced by smooth, flush membrane keypads or capacitive touch panels that eliminate particulate trap zones and simplify surface sterilization.
  • Integration of Backlighting & Status LEDs: Modern equipment design emphasizes clear visual indicators. Surface-mount LEDs embedded directly within the membrane circuit stack—illuminating embossed keys or status windows—allow intuitive operation in low-light factory environments.
  • Demand for Hybrid Input Interfaces: Combining silicone rubber keypads with flexible membrane circuits or rigid PCB backers provides operators with deep-travel tactile key feel while preserving the multi-layer environmental sealing underneath.
  • Rapid Prototyping & Fast DFM Turnarounds: Local original equipment manufacturers (OEMs) in Mixco require agile supplier responses. Ravo’s ability to conduct Design for Manufacturability (DFM) reviews in under 2 hours and produce functional prototypes from 1 piece accelerates regional product release timelines.

Enterprise Advantages: Dongguan Ravo Electronics Co., Ltd.

Established in 2003 in Dongguan, China, Dongguan Ravo Electronics Co., Ltd. has established itself as an authoritative global manufacturer of custom membrane switches, graphic overlays, silicone rubber keypads, and thin-film force sensors.

12,000 m² Integrated Production Facility

Vertically integrated manufacturing including automatic screen-printing lines, precision laser cutting, CNC die-cutting, high-speed SMT LED placement, and dust-free cleanroom lamination suites.

Rigorous Quality Assurance & ISO Certification

ISO 9001 quality management compliance. Every production run undergoes 100% automated electrical continuity testing, resistance verification, actuation force profiling, and visual inspection.

Direct Engineering Support & Fast DFM

Our experienced HMI engineering team evaluates CAD files (DXF, DWG, STEP, AI) and delivers thorough Design for Manufacturability (DFM) feedback and stack-up proposals within 2 hours.

Frequently Asked Questions for Sourcing Membrane Switches to Mixco

What is the typical minimum order quantity (MOQ) for custom membrane switches delivered to Mixco?
We support product development with prototype quantities starting from 1 to 10 pieces. For volume production orders bound for Guatemala, standard production MOQs range from 100 to 500 pieces depending on the complexity of the material stack, tooling requirements, and integrated backlighting components.
How do you ensure your membrane keypads remain waterproof in humid outdoor settings?
We implement continuous die-cut 3M acrylic adhesive rings (such as 3M 467MP or 3M 468MP) around the outer switch frame, pot the flex circuit exit zone with UV-cured resin, and integrate waterproof venting membranes. This enables our assemblies to achieve IP65, IP67, or IP68 protection levels.
What graphic overlay materials are recommended for equipment subjected to frequent chemical cleaning?
For medical devices, sterilizable clinical tables, and food processing machinery, we strongly recommend hard-coated Polyester film (MacDermid Autotex PET). PET exhibits superior resistance to isopropyl alcohol, bleaching agents, sanitizers, and chemical solvents compared to standard Polycarbonate (PC).
What files are required to initiate a custom quotation and engineering DFM review?
To generate a detailed technical quotation and layer stack proposal, please provide vector artwork files (AI, PDF, EPS with Pantone color specifications) alongside 2D/3D mechanical drawings (DXF, DWG, STEP) indicating key dimensions, tail exit location, connector pitch, and tactile dome requirements.
What shipping options and lead times apply for delivery to Mixco, Guatemala?
Prototype orders are manufactured in 7 to 12 working days and dispatched via express air freight (DHL/FedEx/UPS), reaching Guatemala in approximately 4 to 6 transit days. Mass production orders can ship via express air cargo or ocean freight to Puerto Quetzal, accompanied by full commercial invoices and customs documentation.

Ready to Build Custom Waterproof Membrane Switches for Your Equipment?

Contact our engineering specialists today to receive a complete DFM evaluation, custom material layer stack-up recommendation, and direct factory price quote within 2 hours.

Contact Us