EN
 DE
 FR
 ES
 RU
 JA EN DE FR ES RU JA
Engineered for extreme durability, chemical resistance, and tactile precision. Select a solution below or contact our engineering team for custom stack-up designs.
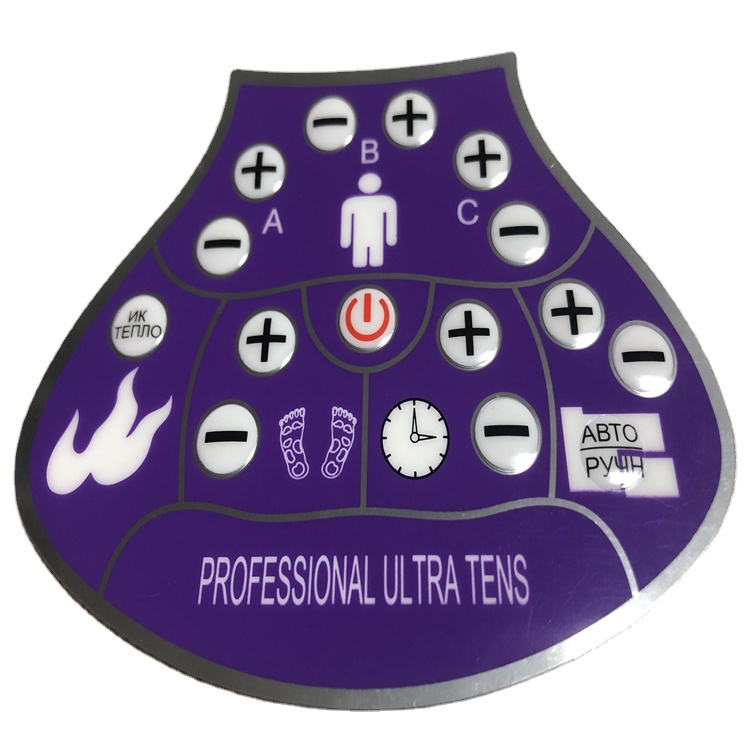
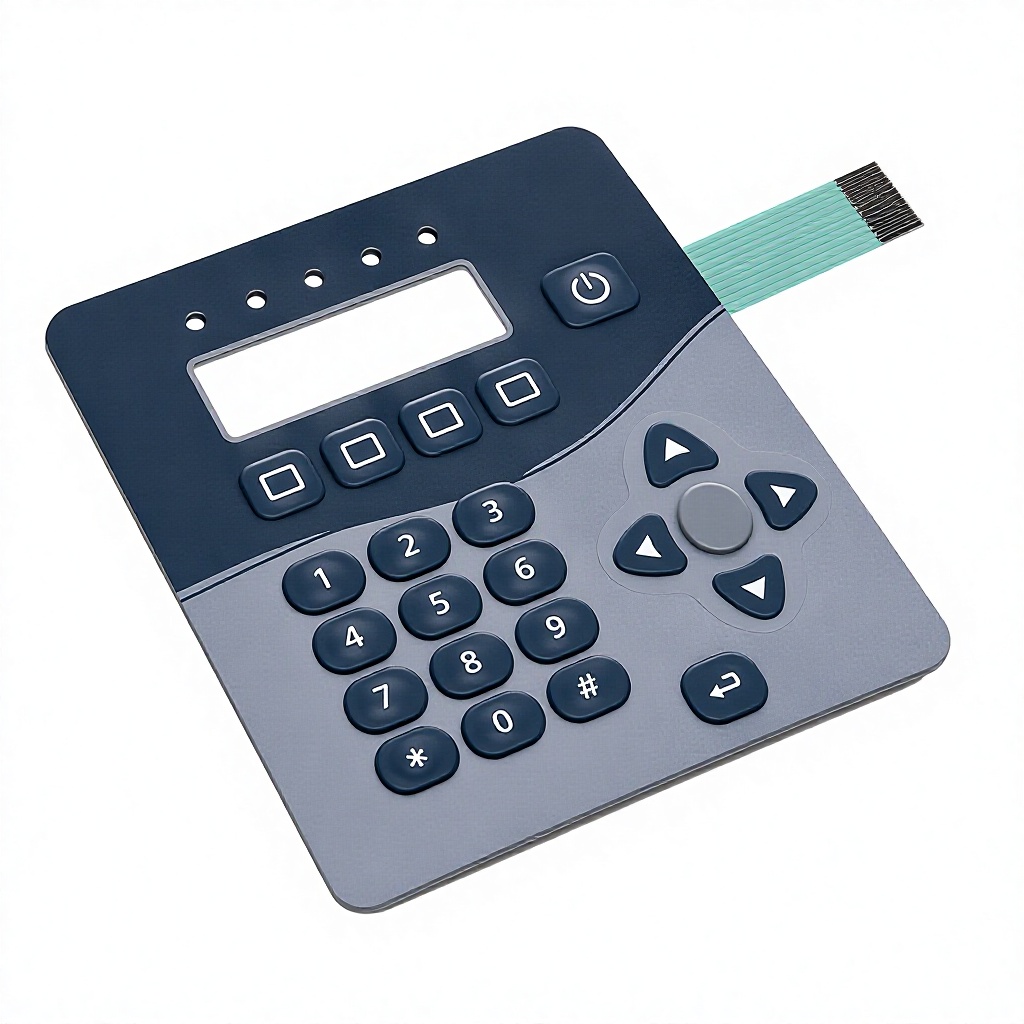
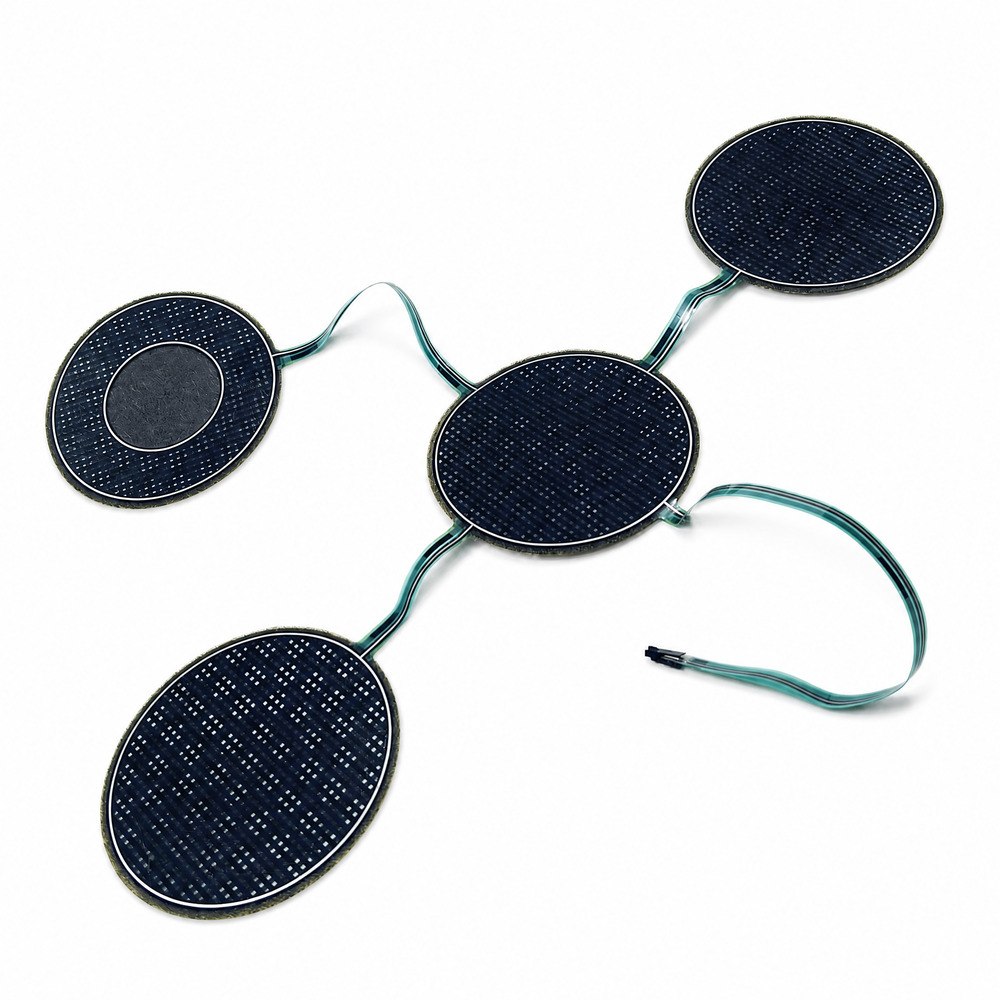
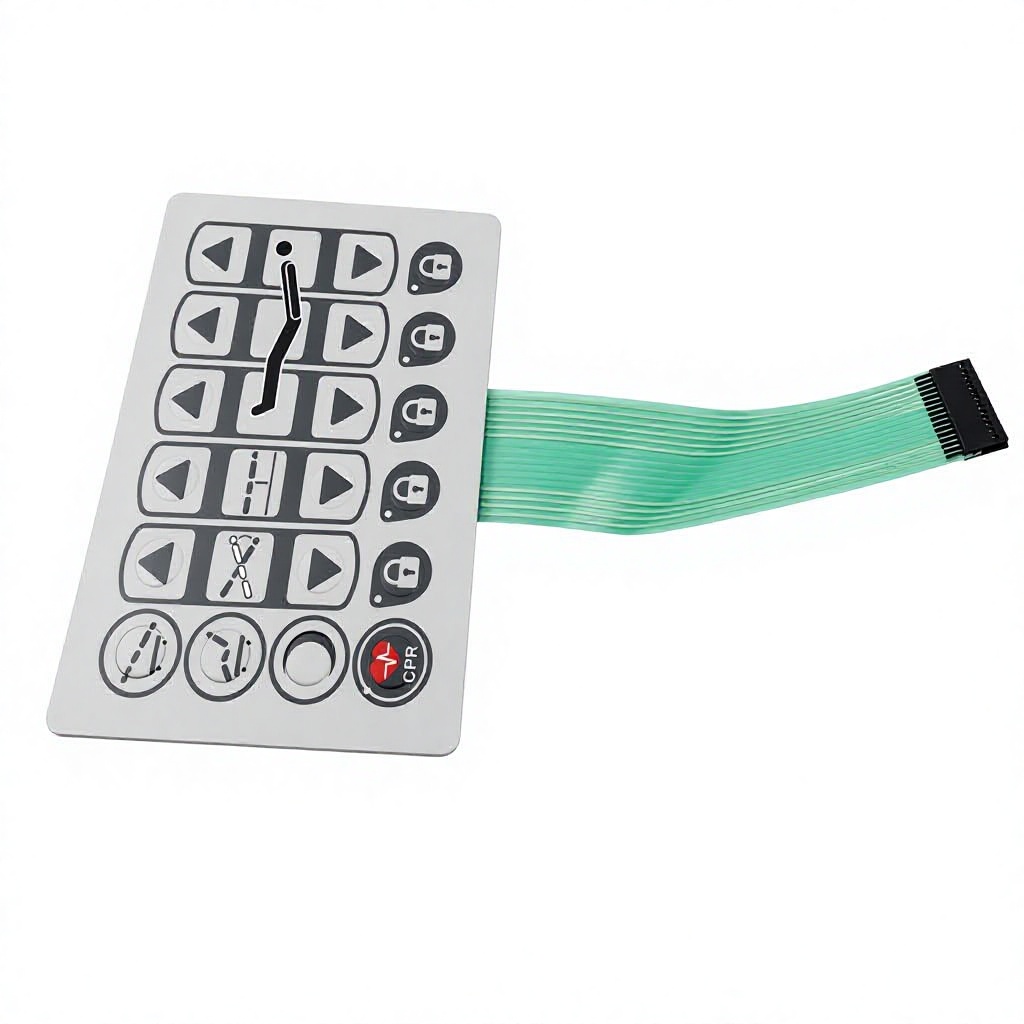
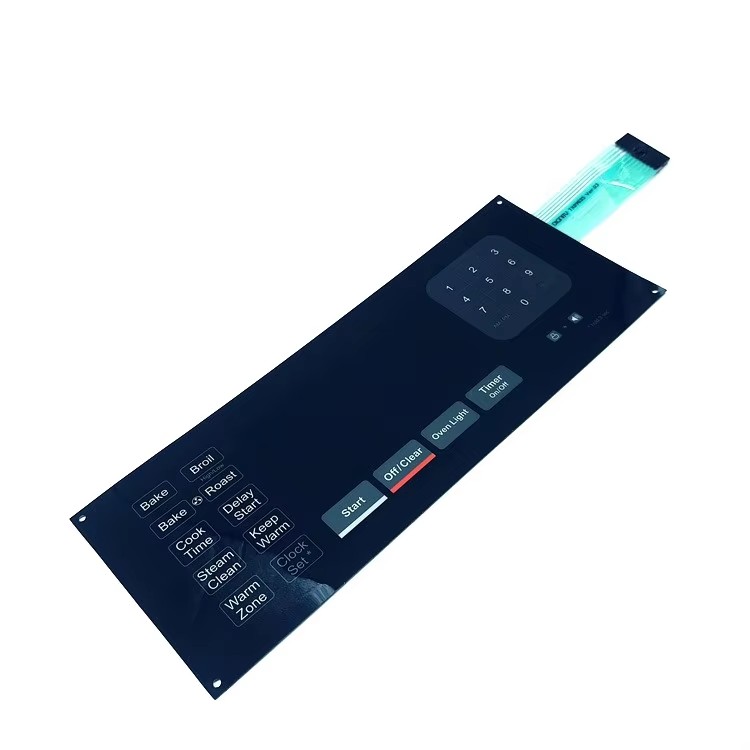
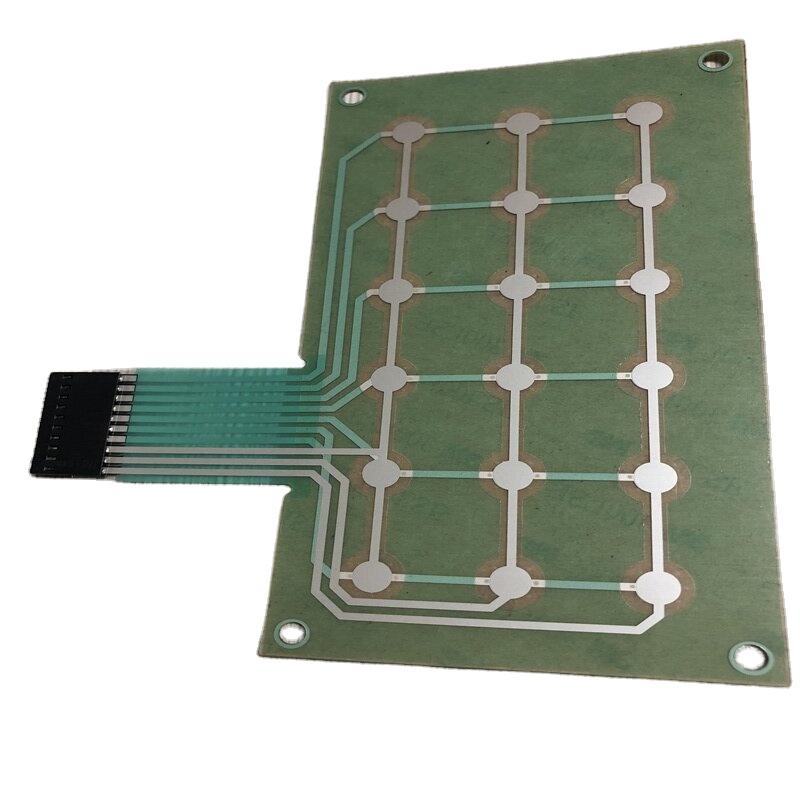
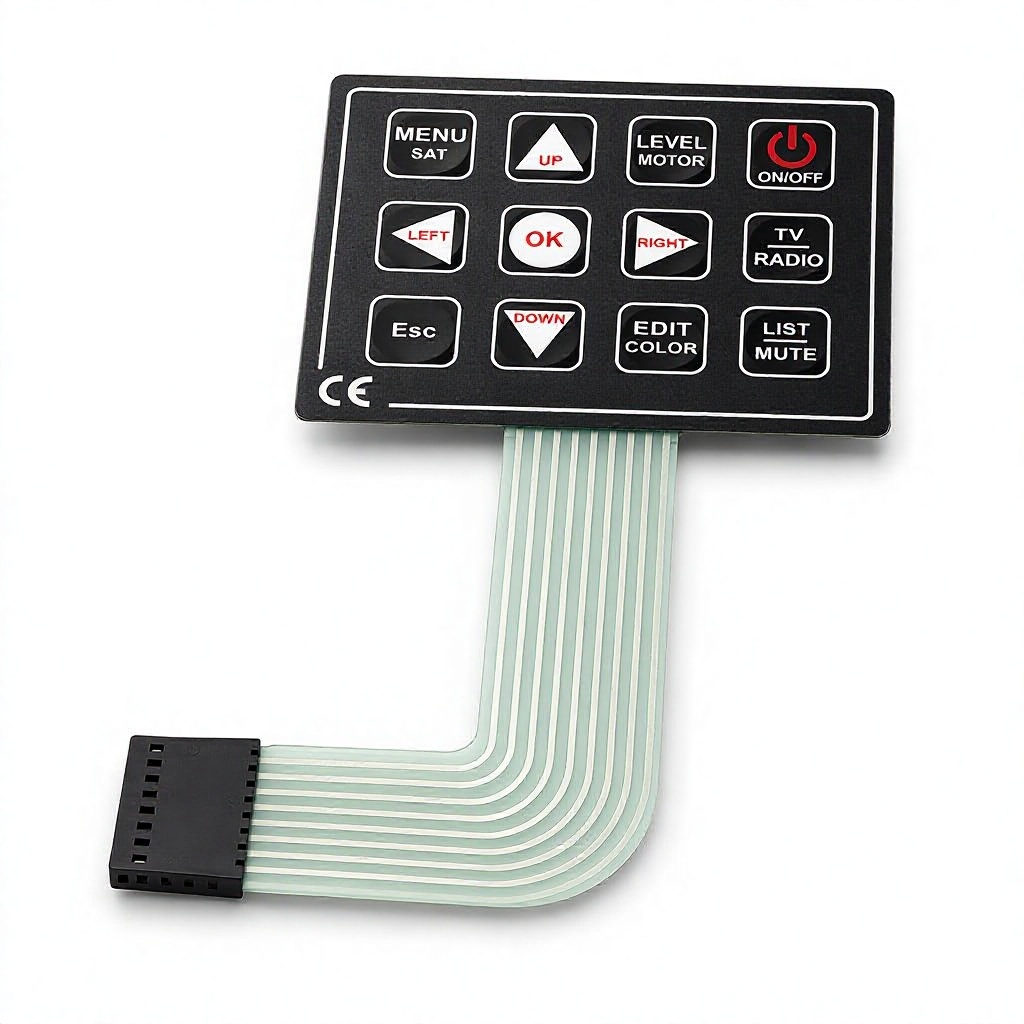
The Charlestown industrial corridor—spanning biotech manufacturing hubs, regional medical technology clusters, maritime research installations, and precision defense contractors—demands exceptional reliability in Human-Machine Interfaces (HMI). Electromechanical switches and conventional touchscreens often fail when subjected to harsh environmental variables such as salt spray, chemical sterilizers, hydraulic fluid exposure, high tactile actuation frequency, and severe ESD (Electrostatic Discharge) events.
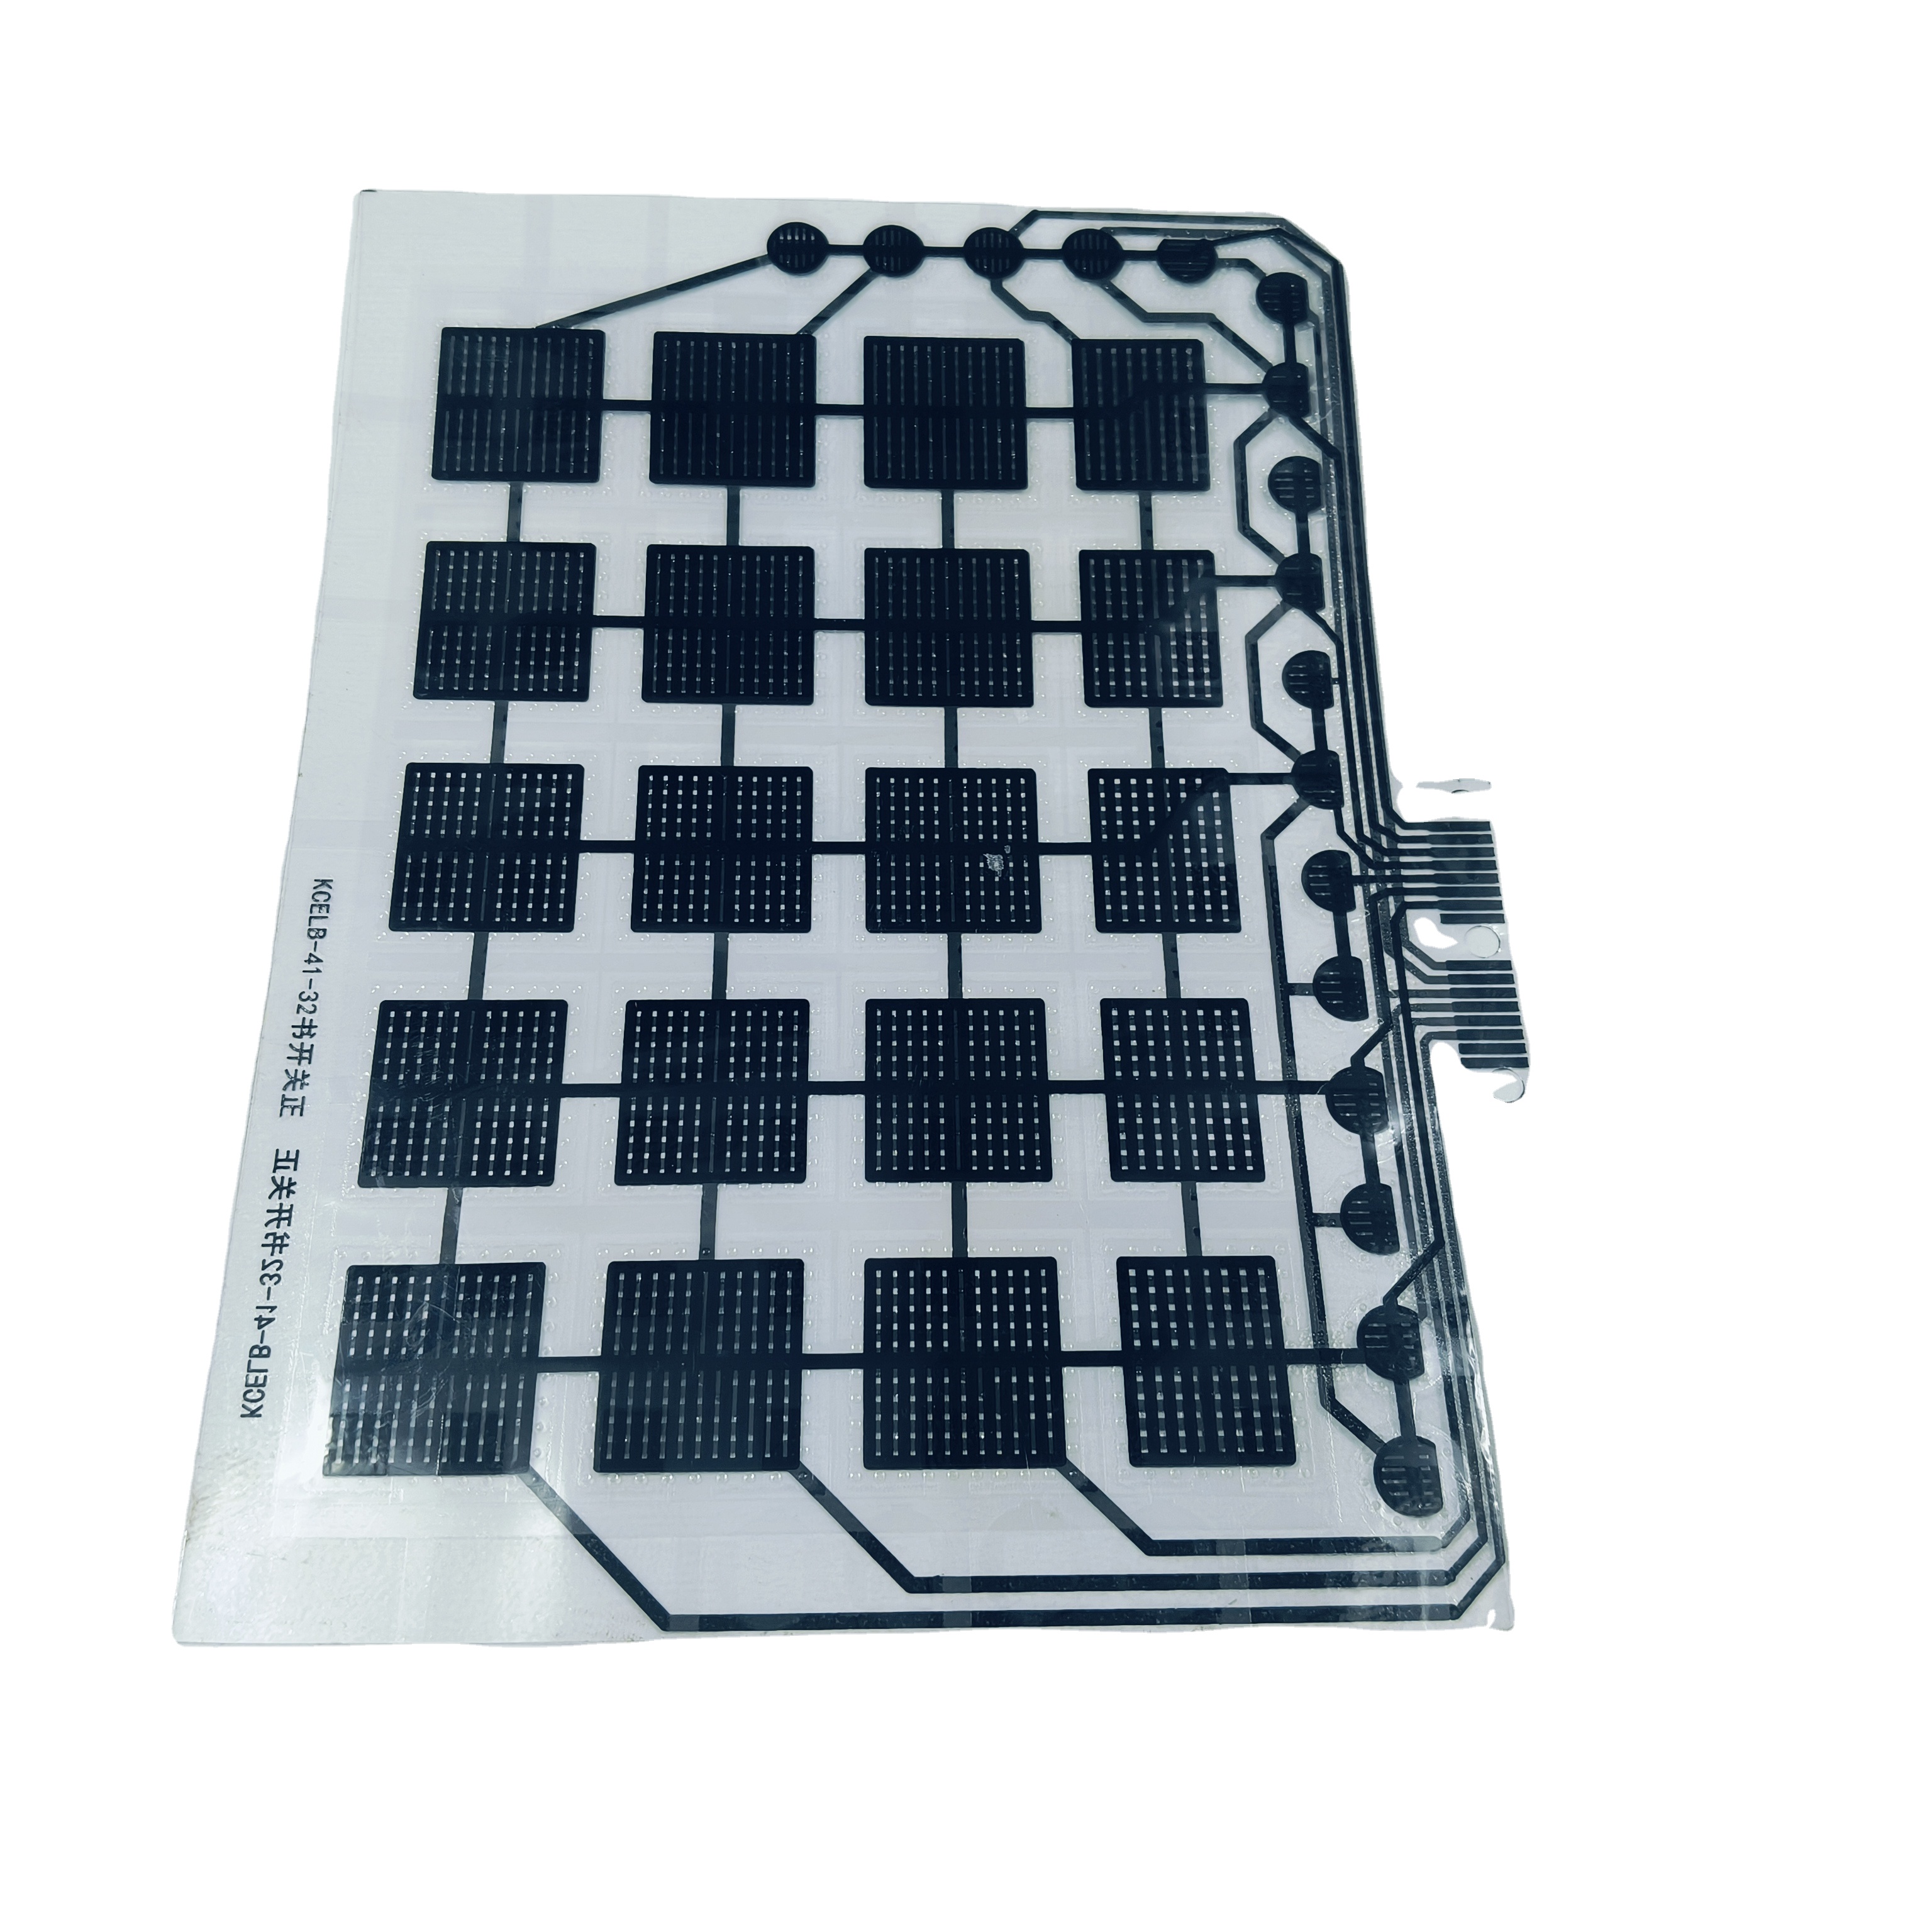
Custom membrane keypads engineered by Dongguan Ravo Electronics Co., Ltd. bridge the critical gap between complex internal circuit architecture and human operation. By utilizing precision multi-layer thin-film constructions—integrating MacDermid Autotex® polyester foils, Bayer Bayfol® polycarbonate films, 3M™ high-tack acrylic adhesives, stainless steel tactile domes, and screen-printed silver ink circuits—we supply Charlestown manufacturers with sealed, low-profile interface solutions rated for over 1,000,000 actuation cycles.
Understanding the structural layers that enable IP67 waterproofing, crisp tactile feedback, and ESD attenuation in severe operating environments.
Autotex® PET or Lexan™ PC (0.125mm to 0.25mm) with sub-surface reverse silk-screen printing. Offers extreme UV resistance, anti-glare finishes, scratch resistance, and chemical immunity against bleach, alcohol, and industrial detergents.
Utilizes 3M™ 467MP or 468MP high-performance acrylic adhesive. Holds Four-Legged Stainless Steel 304 Domes (12mm to 20mm, 280g to 450g actuation force) precisely over contact pads, delivering tactile feedback with clear sensory click sound.
Screen-printed conductive silver ink (<0.05 Ω/sq/mil) blended with graphite anti-migration traces on stabilized heat-treated PET or polyimide FPC substrate. Features pitch configurations down to 1.0mm ZIF connectors or 2.54mm female crimp housings.
Integrated full-surface printed carbon ESD ground planes or aluminum foil EMI shielding, grounded through a dedicated tail conductor to discharge up to 15kV static surges. Backed with 3M™ 9448A or VHB™ adhesives for immediate bezel assembly.
| Substrate Type | Tactile Feel / Mechanism | Sealing Rating | Actuation Life | Optimal Charlestown Application |
|---|---|---|---|---|
| Metal Dome PET Circuit | Crisp tactile snap (280g - 350g force) | IP65 - IP67 Sealed | 1,000,000+ Cycles | Medical Bed Controllers, Patient Monitoring, Diagnostic Gear |
| Polydome Thermoformed PET | Soft cushion tactile response | IP65 Perimeter Gasket | 500,000 Cycles | Commercial Appliances, Fitness Equipment, Consumer Electronics |
| Capacitive Touch PET/Glass | Non-tactile, zero travel touch sensing | IP68 Smooth Washdown | 5,000,000+ Cycles | Sterile Surgical Suites, Cleanroom Food Processing, Lab Automation |
| FPC / PCB Rigid Backer | Metal Dome / SMT LED Integration | IP67 NEMA 4X | 2,000,000+ Cycles | Maritime Navigation Systems, Military Defense Keypads, Heavy Machinery |
Tailored interface solutions designed to comply with local Charlestown manufacturing standards, medical regulations, and harsh maritime environments.
Charlestown’s expanding medical technology and research corridor requires cleanroom-compatible human-machine interfaces. Our medical-grade membrane keypads feature anti-microbial overlays (containing silver ion additives) and fully sealed perimeter gaskets that withstand harsh sterilization protocols (isopropyl alcohol, hydrogen peroxide vapor, and bleach).
Key Design Highlights: Embossed tactile metal domes for gloved operation, integrated ultra-thin SMD LEDs for status indicators, clear display windows for OLED/LCD screens, and compliance with ISO 13485 quality standards.
Located directly adjacent to coastal salt-fog environments, Charlestown maritime engineers face severe corrosion challenges. Ravo manufactures specialized marine-grade membrane switches featuring double-sided potted tail exits, UV-stabilized Autotex® hard-coat surfaces, and IP67 water-tight perimeter bonding.
Key Design Highlights: MIL-STD-810G salt fog resistance, backlit light-guide film (LGF) illumination for night vision operations, anti-glare matte texturing, and heavy-duty 450g metal domes for high vibration marine craft.
As advanced manufacturing facilities across Massachusetts modernize with automated guided vehicles (AGVs) and robotic workcells, interface keypads must endure continuous multi-shift usage. Ravo’s industrial membrane switches offer ruggedized polycarbonate graphic overlays bonded to rigid FR4 PCB backers.
Key Design Highlights: Integrated tactile directional D-pads, carbon ESD static grounding layer, high-temp 3M 468MP adhesive mounting, and custom pinouts compatible with industrial PLC controllers.
High-traffic outdoor keypads demand scratch-resistant, anti-vandalism construction. For commercial vending machines, fuel dispensers, and public access kiosks in Charlestown, Ravo supplies glossy 0.125mm PET membrane keypads with 3M 467 adhesive that endure outdoor thermal expansion from -40°C to +85°C.
Key Design Highlights: Ultra-thin non-tactile design, 2NO high-reliability silver paste contact matrix, cost-effective high-volume screen printing, and UV non-yellowing protective layers.
Hardware development in the Charlestown market is undergoing a rapid evolution toward sleeker, smarter, and more environmentally compliant interfaces. As local OEM design teams reduce enclosure depths and demand seamless wipe-clean control panels, several engineering trends have emerged:
Answers to common technical questions regarding custom prototyping, material selection, environmental sealing, and export logistics.
Founded in 2003 in Fenggang Town, Dongguan, Ravo Electronics has expanded into a premier 12,000 square meter vertically integrated manufacturer of custom human-machine interfaces, thin-film pressure sensors, silicone rubber keypads, and graphic overlays.
By maintaining complete in-house control over graphic screen printing, laser cutting, automated dome placement, SMD LED soldering, precision lamination, and final electrical testing, we eliminate middleman overhead and enforce rigorous quality standards. Our dedicated international engineering support team bridges time zone differences with ≤2 hour response times, delivering tailored DFM insights to hardware engineers across Charlestown, North America, and Western Europe.
CNC digital cutting tables and photolithography screen making allow rapid design changes without long tooling lead times.
Certified quality management systems guaranteeing batch-to-batch repeatability and rigorous material component traceability.
Send us your DXF/Gerber files, sample specs, or project requirements today. Our senior HMI application engineers will provide a complete DFM analysis and quotation within 2 hours.
Contact Us