EN
 DE
 FR
 ES
 RU
 JA EN DE FR ES RU JA
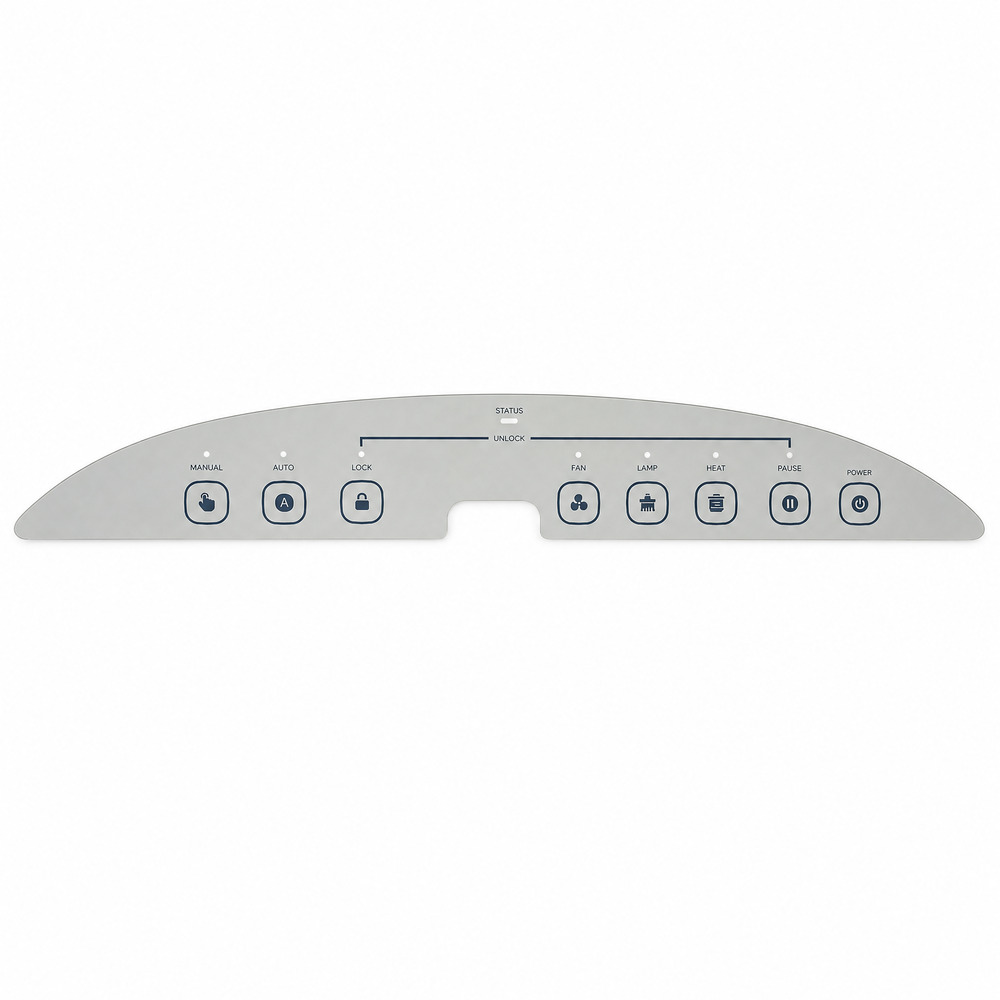
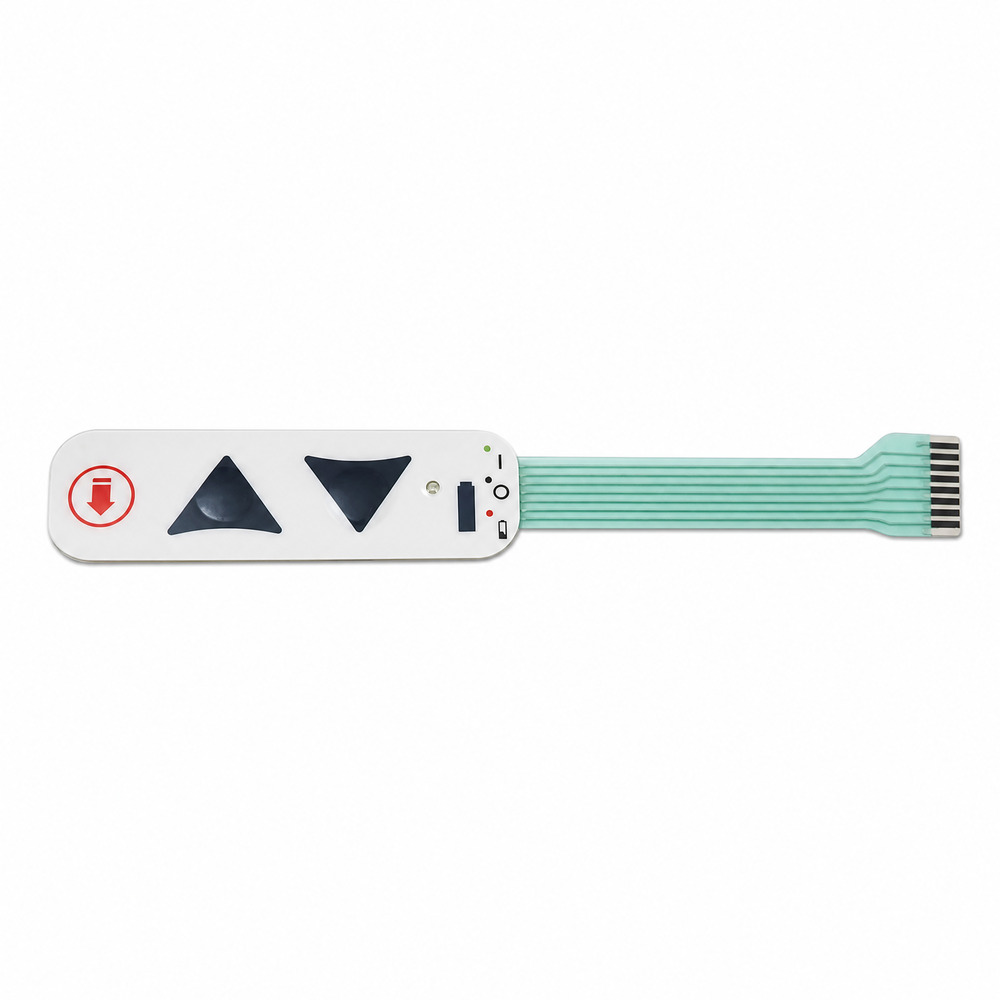
Explore our export-grade membrane switches, capacitive touch assemblies, graphic overlays, and thin-film force sensitive resistors (FSR). Designed for rigorous medical environments, surgical systems, and industrial control electronics in Lisbon and across the European Union.
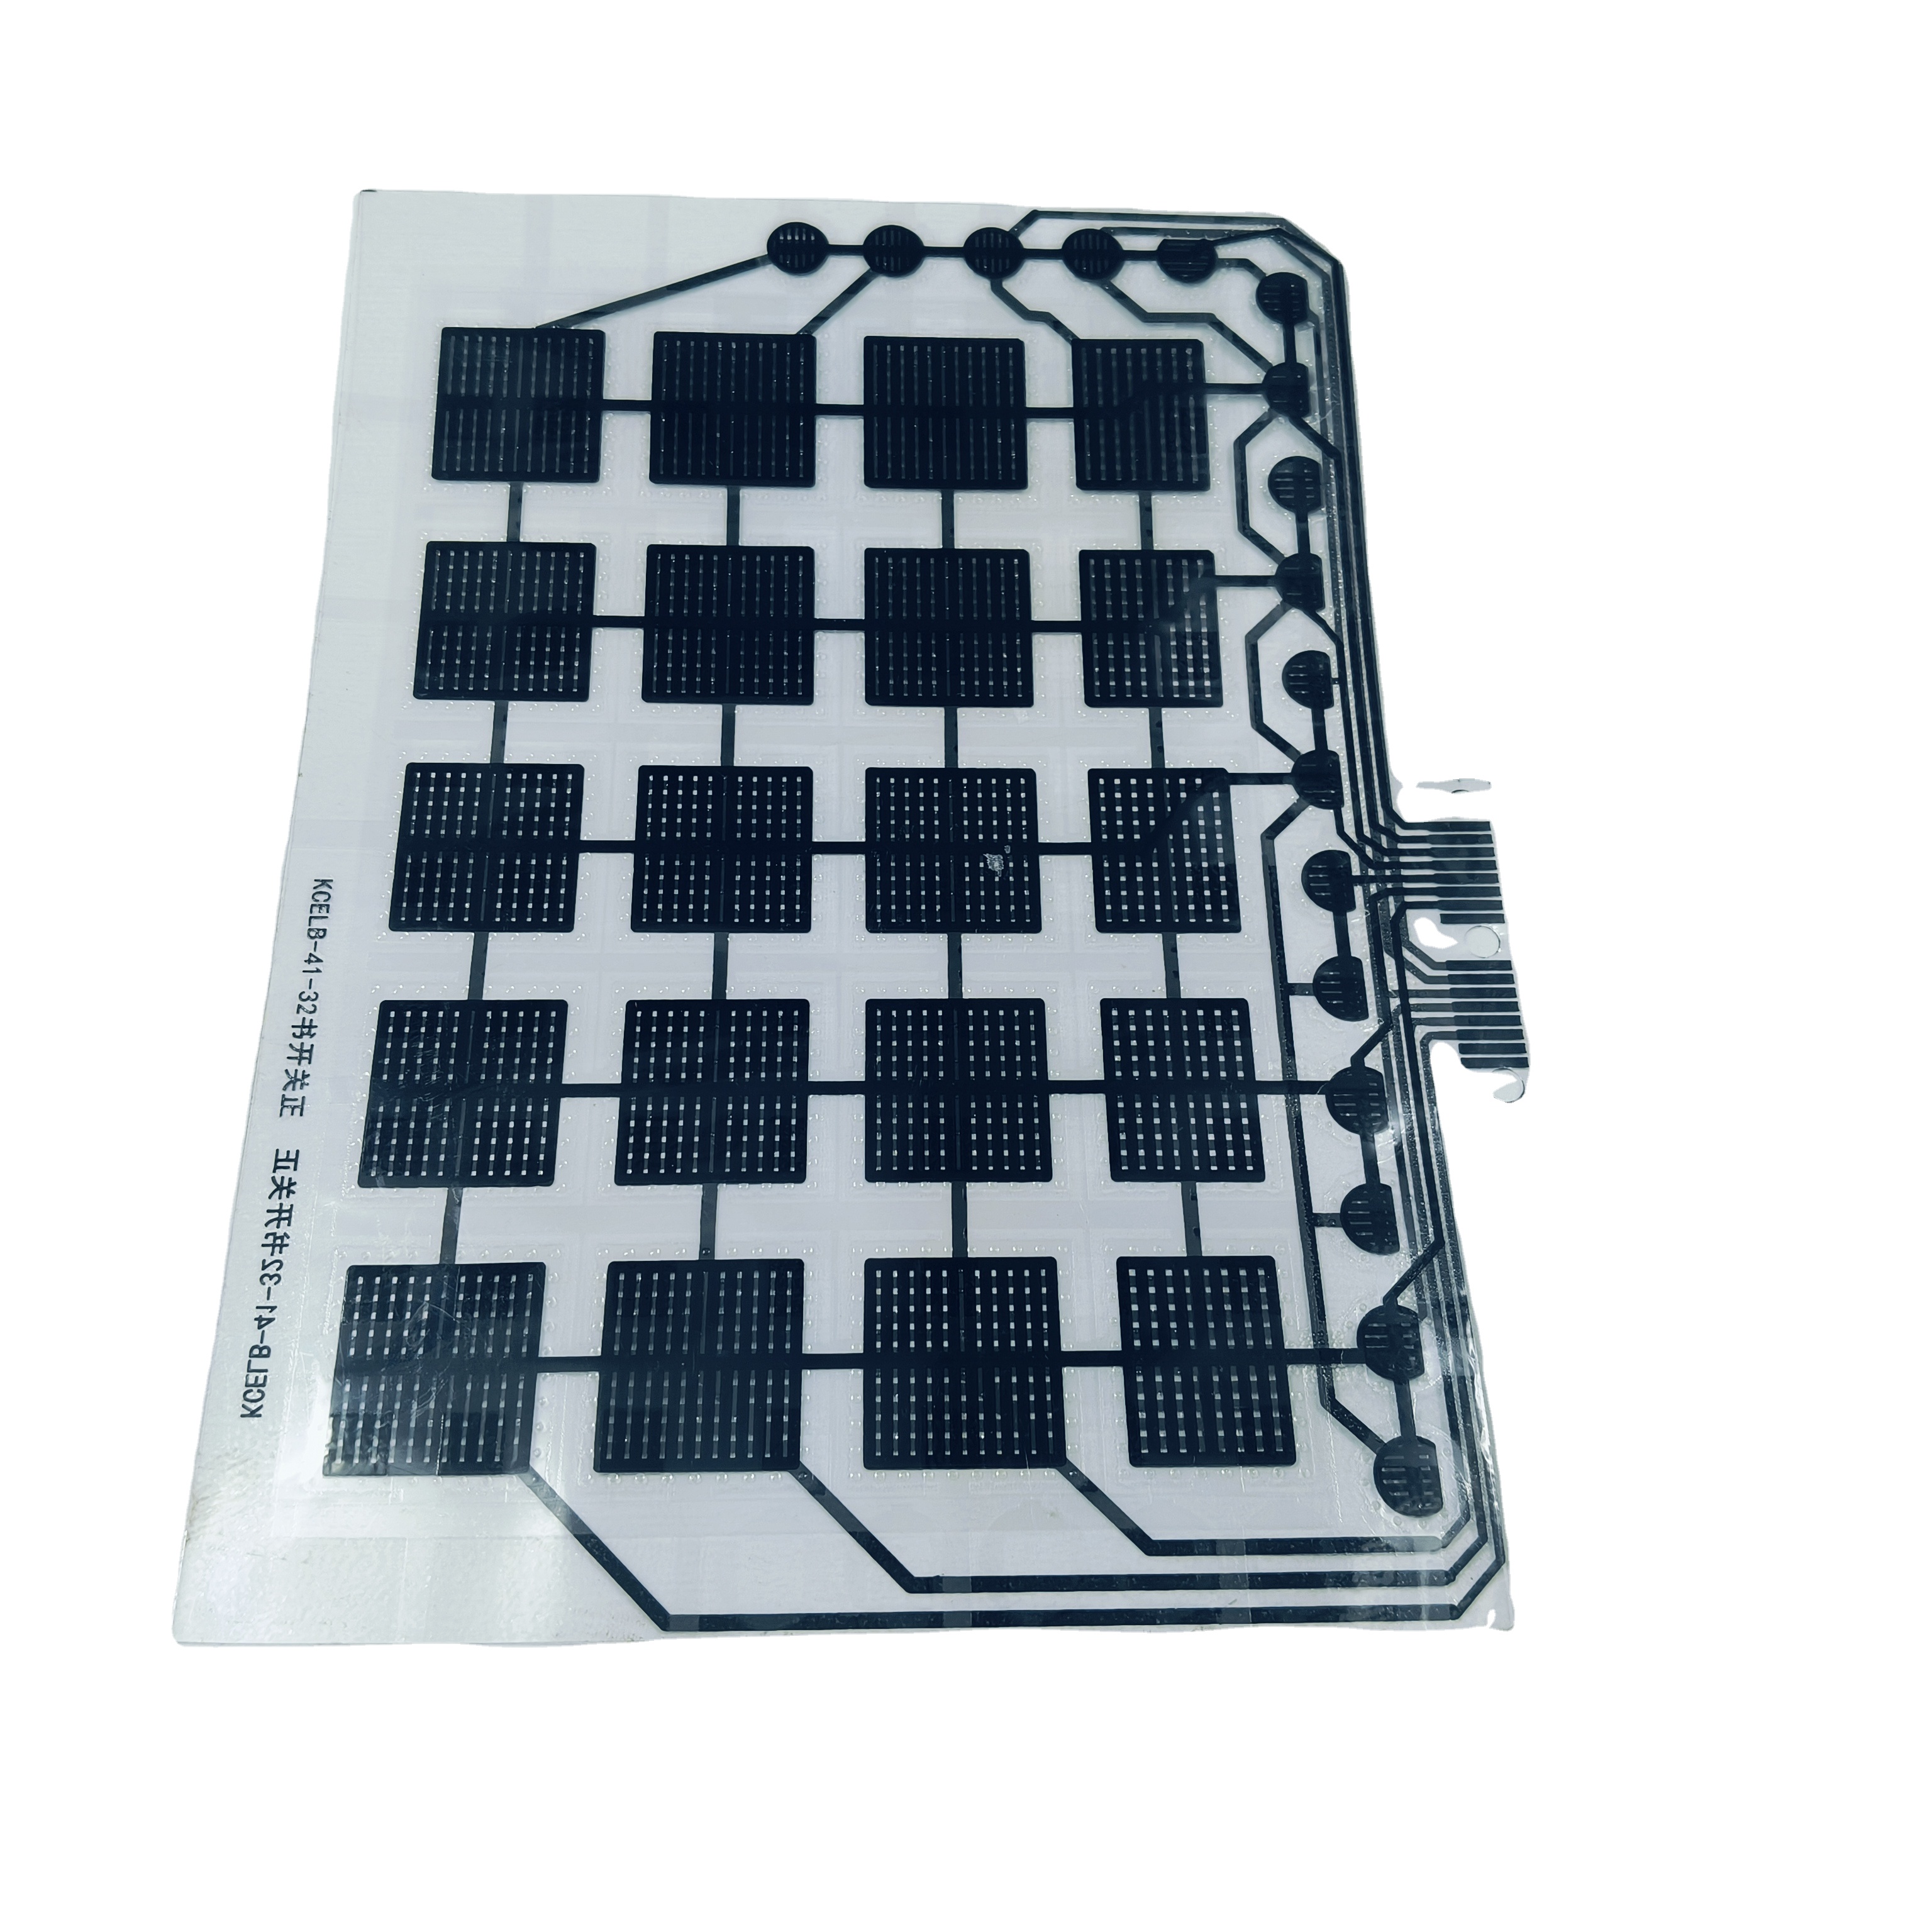
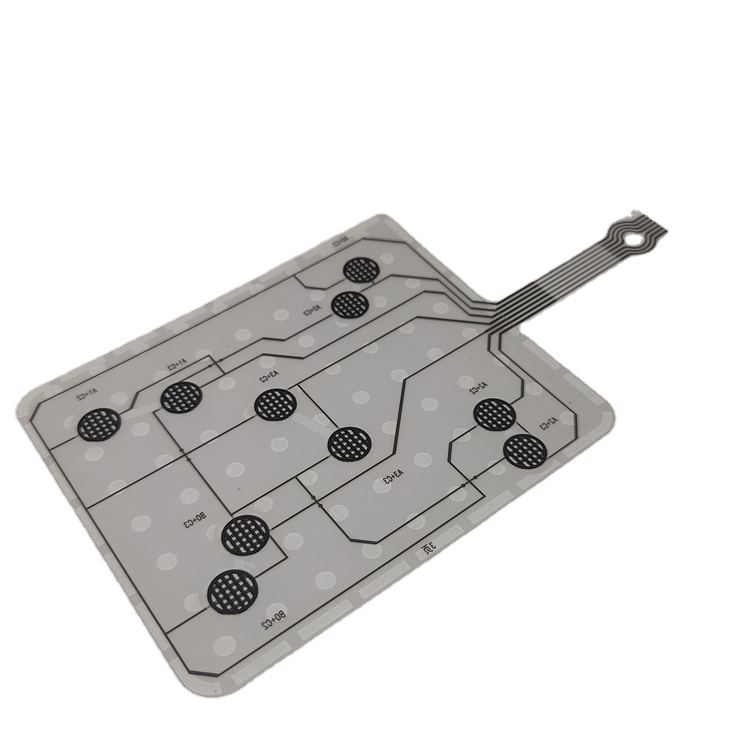
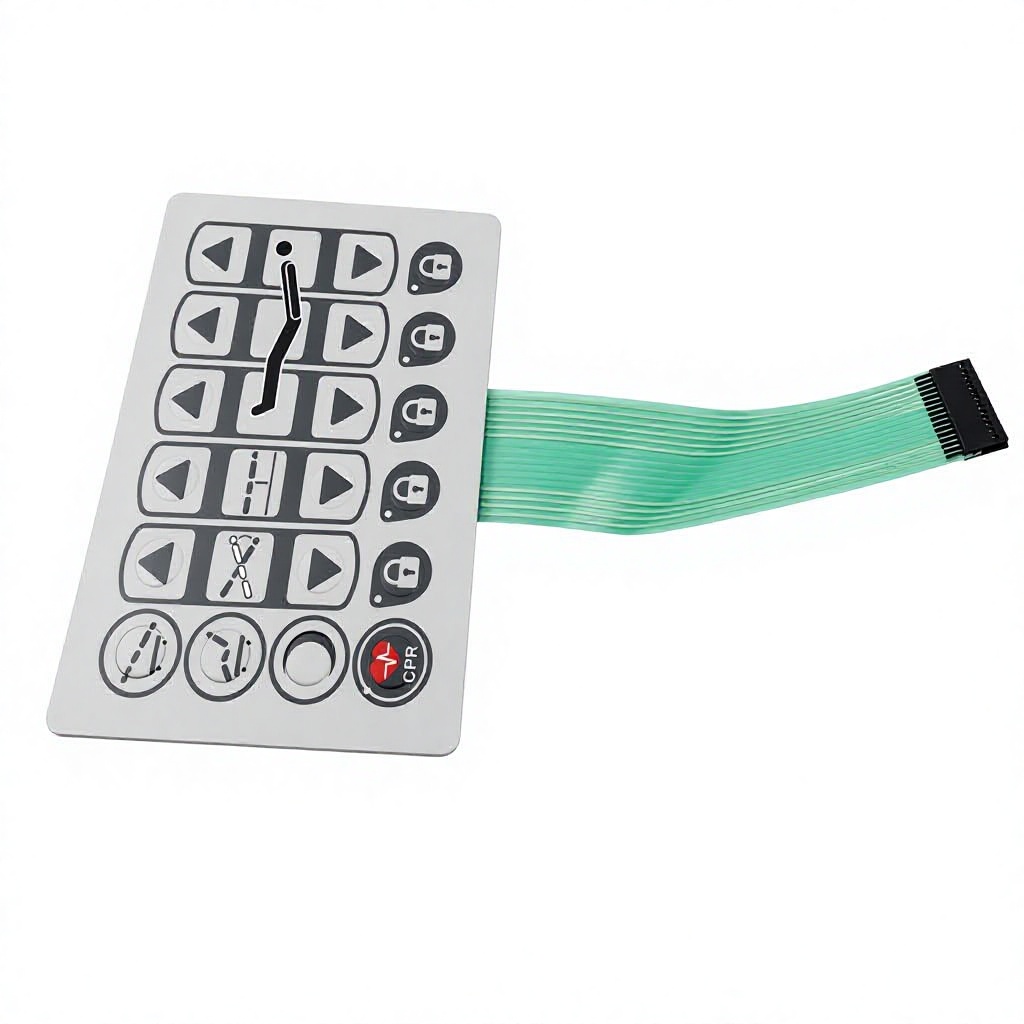
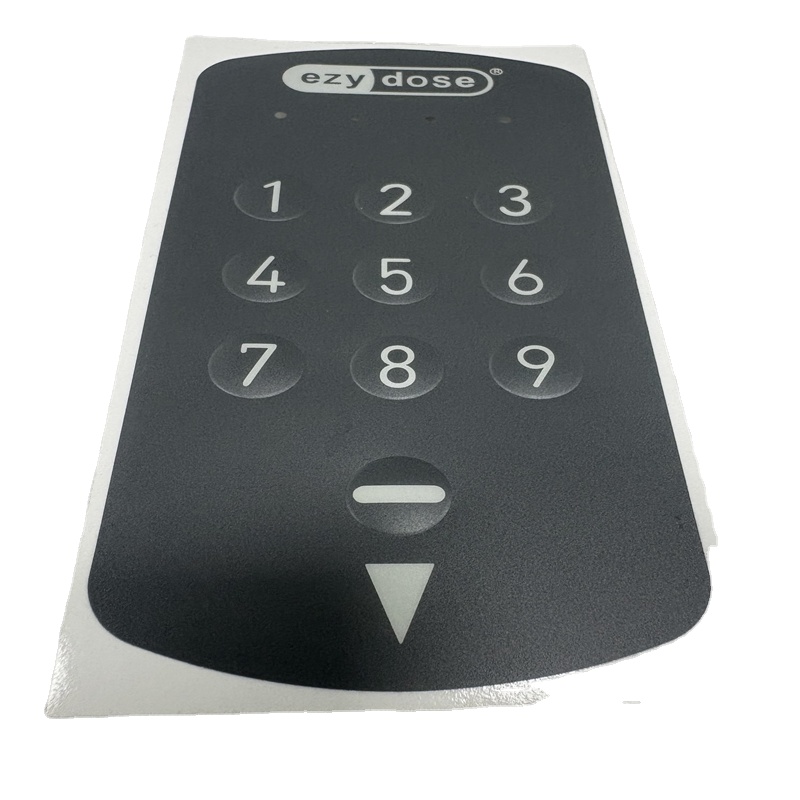
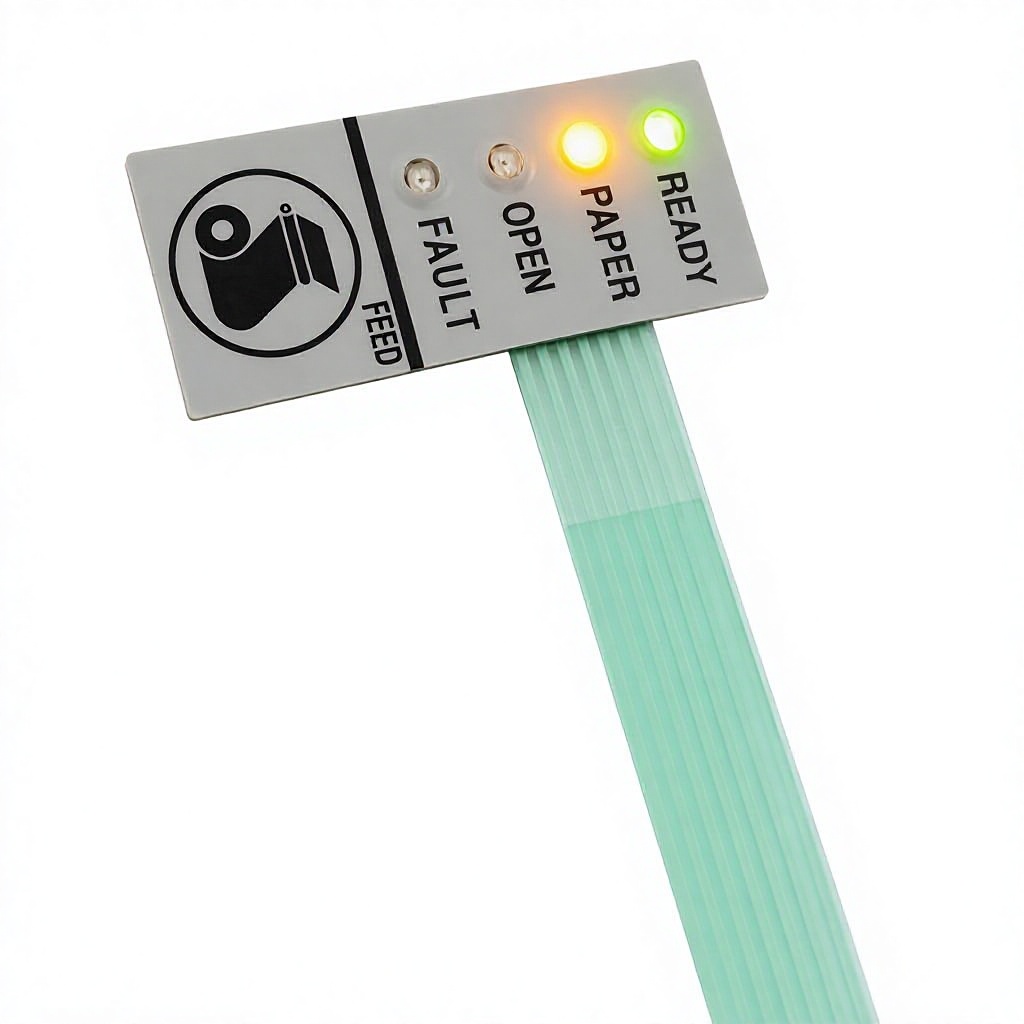
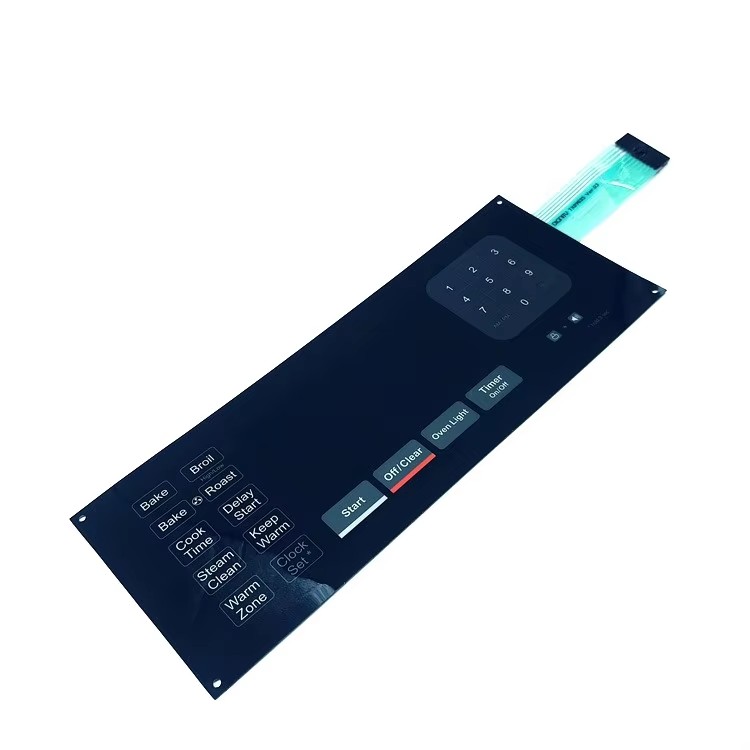
As the Greater Lisbon area—spanning technical hubs like Taguspark (Oeiras Valley), Lumiar Health Technology Parks, and academic research centers surrounding Hospital de Santa Maria—expands its medical device manufacturing footprint, the demand for high-reliability, cleanroom-manufactured Human-Machine Interfaces (HMI) has reached an all-time peak. Medical OEMs operating within Portugal and exporting across the European single market require sub-assemblies that adhere strictly to EU MDR 2017/745 and IEC 60601-1 electrical safety standards.
As a premier OEM/ODM direct manufacturer based in Dongguan, China with over two decades of specialized expertise, Dongguan Ravo Electronics Co., Ltd. serves as a trusted engineering partner to medical equipment designers and procurement leaders in Lisbon. We engineer customized medical membrane switches, non-tactile capacitive control panels, tactile metal-dome keypads, and thin-film force sensitive resistor (FSR) sensors designed specifically to survive harsh clinical decontamination protocols while guaranteeing zero operational latency.
A true medical-grade membrane switch is a highly engineered multi-layer composite. Unlike standard commercial keypads, medical interfaces must resist chemical ingress, prevent bio-burden accumulation, shield sensitive microprocessors from Electrostatic Discharge (ESD), and withstand millions of actuations under high stress.
| Layer Index | Layer Component | Material Specification | Engineering Functionality |
|---|---|---|---|
| Layer 1 | Graphic Overlay | Autotex Microban PET / MacDermid XE Film | Antimicrobial front foil, chemical-resistant matte/gloss texture, sealed display windows. |
| Layer 2 | Overlay Adhesive | 3M 200MP / 467MP / 468MP High-Performance Acrylic | Forms an airtight bond; prevents ingress of isopropyl alcohol, bleach, and fluids. |
| Layer 3 | Dome Retainer / Spacer | 0.075mm - 0.125mm Polyester (PET) Film | Secures tactile metal domes in exact alignment; provides physical travel cushion. |
| Layer 4 | Tactile Domes | Stainless Steel Domes (Four-leg or Circle, 200g-400g) | Delivers tactile snap feedback; reliable electrical connection upon compression. |
| Layer 5 | Flexible Circuitry | Silver Ink Conductive / Carbon Paste PET or Polyimide FPC | Low-resistance printed conductive trace network transferring signal to control board. |
| Layer 6 | Rear Adhesive / Stiffener | 3M 9448A Tissue or Rigid FR-4 Backer Panel | Mounts entire HMI assembly to metal or plastic equipment chassis securely. |
Lisbon’s healthcare industry ranges from public clinical centers to high-tech medical technology exporters. Ravo's custom membrane keypads and thin-film pressure sensors are built to integrate seamlessly into diverse medical equipment deployed across Portugal:
Pendant remotes and side-rail control keypads for surgical tables, hospital bed articulators, and patient lifters. Sealed to IP67 specifications with embossed tactile metal domes so medical personnel can operate adjustments intuitively through surgical gloves.
Integrated control console panels for portable X-ray units, ultrasound diagnostic systems, and MRI positioning tables. Features dead-front backlighting and optical-clear display windows for high contrast in dimmed imaging suites.
Wipe-clean capacitive touch membrane interfaces designed for fluid management devices. Features non-tactile, completely flat polyester surfaces with zero crevices, preventing chemical or fluid pooling during rapid disinfection.
Used extensively in clinical research labs around Oeiras Valley and Lisbon university hospitals. Heavy-duty PCB-backed membrane switches combined with status indicator LEDs to monitor RPM, thermal controls, and cycle safety interlocks.
Thin-film Force Sensitive Resistor (FSR) matrix pressure sensors integrated into medical bed occupancy monitors, patient fall-prevention pads, and orthotic gait analysis tools deployed in Portuguese physical therapy centers.
The Southern European healthcare technology corridor is undergoing a rapid modernization phase driven by public investment, the Plano de Recuperação e Resiliência (PRR) in Portugal, and strict European sustainability mandates. Key trends shaping procurement decisions for medical HMIs include:
Post-pandemic hospital infection protocols in Lisbon require surface interfaces that actively resist microbial growth. Ravo utilizes specialized polyester films impregnated with silver-ion technology (Autotex Microban). These films destroy 99.9% of bacterial strains (including MRSA and E. coli) on contact while withstanding harsh hospital-grade cleaning agents like quaternary ammonium, peracetic acid, and 70% isopropyl alcohol without clouding or surface degradation.
While traditional tactile metal domes remain essential for blind-location keys, medical device designers at Taguspark healthtech firms are increasingly moving toward hybrid interfaces. Combining capacitive touch zones for rapid wiping with embossed tactile emergency buttons provides the ultimate balance of hygiene and safety.
Modern intensive care units (ICUs) demand quiet, low-light operation to aid patient recovery. Integrating low-profile Surface Mount Device (SMD) LEDs and ultra-thin light guide films (LGF) into membrane keypads allows uniform backlighting of specific function keys without light leakage or excessive power draw.
Lisbon-based OEMs face tight product launch deadlines. Working with suppliers capable of providing immediate Design for Manufacturability (DFM) feedback within 2 hours, combined with 1-piece sample capability, drastically reduces prototype iteration cycles from months to days.
Dongguan Ravo Electronics Co., Ltd. operates a state-of-the-art 12,000 square meter manufacturing facility in Fenggang Town, Dongguan. Our vertically integrated factory houses dust-free cleanrooms, high-precision automated screen printing lines, CNC laser cutting, die-cutting equipment, and computerized testing suites.
100% automated optical inspection (AOI) and 100% electrical continuity testing on every batch. We conduct actuation force mapping, resistance testing, and environmental thermal chamber cycling before dispatch.
Our engineering team evaluates your 2D/3D CAD drawings (DXF, DWG, STEP, Gerber) and returns comprehensive DFM analysis, pinout optimizations, and material stack-up recommendations in 2 hours or less.
Seamless customs handling, door-to-door express air freight (DHL/FedEx/UPS) reaching Humberto Delgado Airport (LIS) within 3–5 working days, and complete DDP/DAP trade term options for hassle-free European purchasing.
Clear, direct technical answers to the most common questions raised by engineering lead and procurement directors sourcing custom medical HMIs from China:
Partner with Dongguan Ravo Electronics for precision-engineered, ISO-compliant medical membrane switches and thin-film sensors delivered directly to your facility in Lisbon or anywhere in Europe.
Send an Inquiry