Industrial
 EN
 DE
 FR
 ES
 RU
 JA
Certified turnkey manufacturing from precision film tooling and SMD component placement to complete environmental sealing and ISO 9001 quality validation.
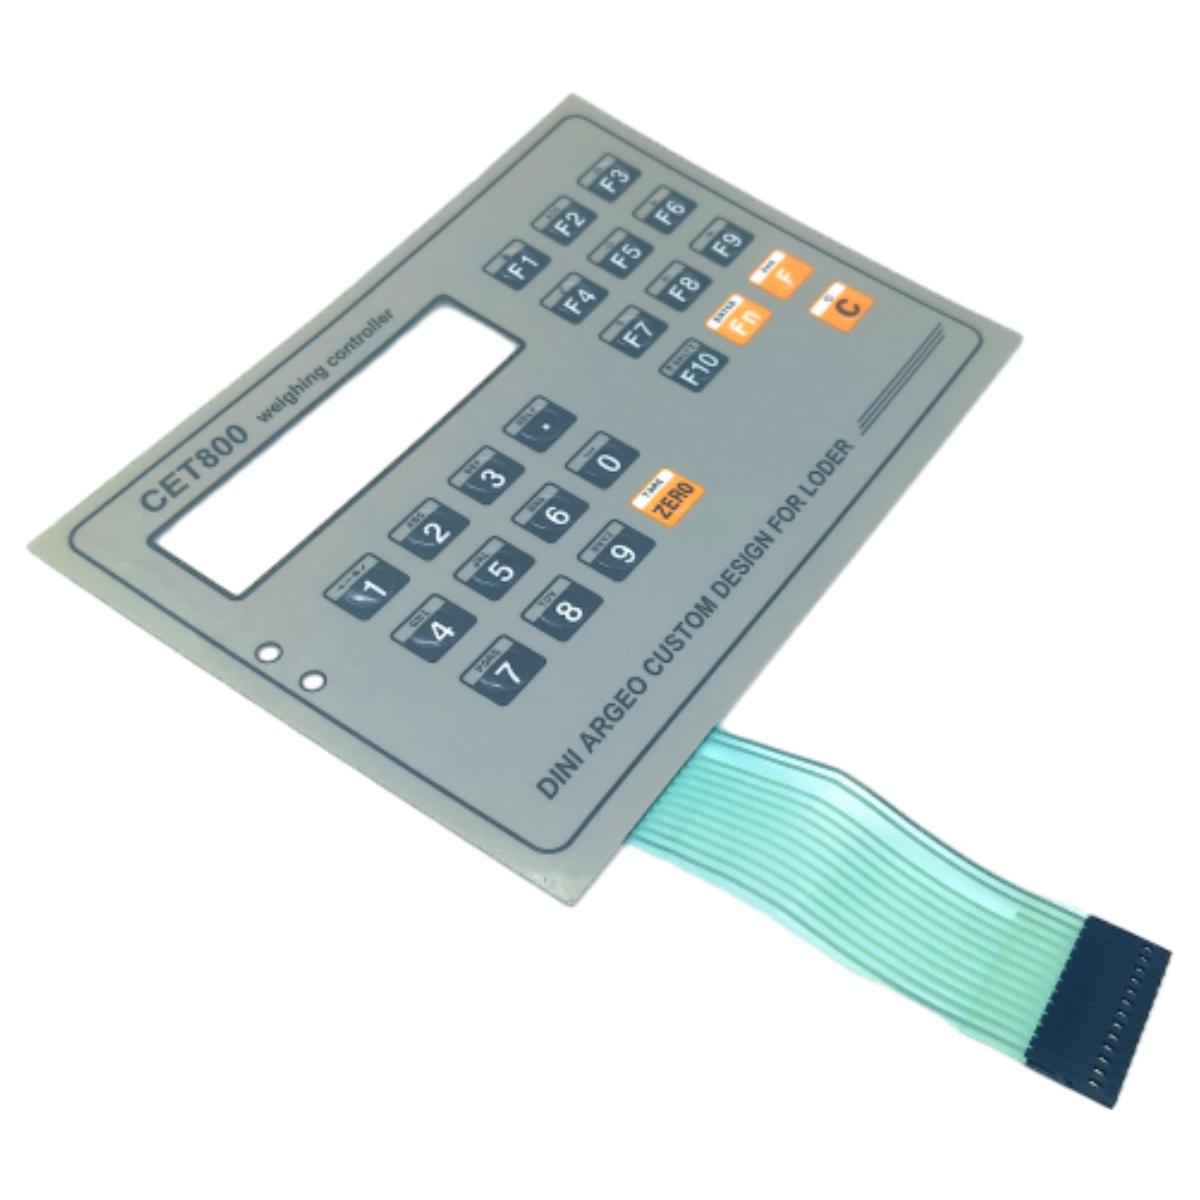
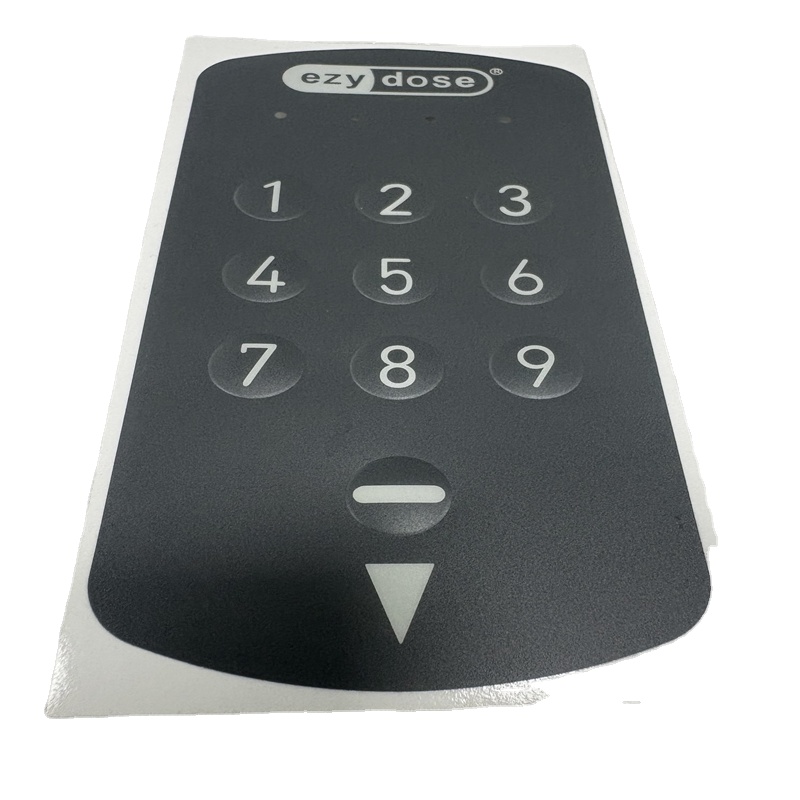
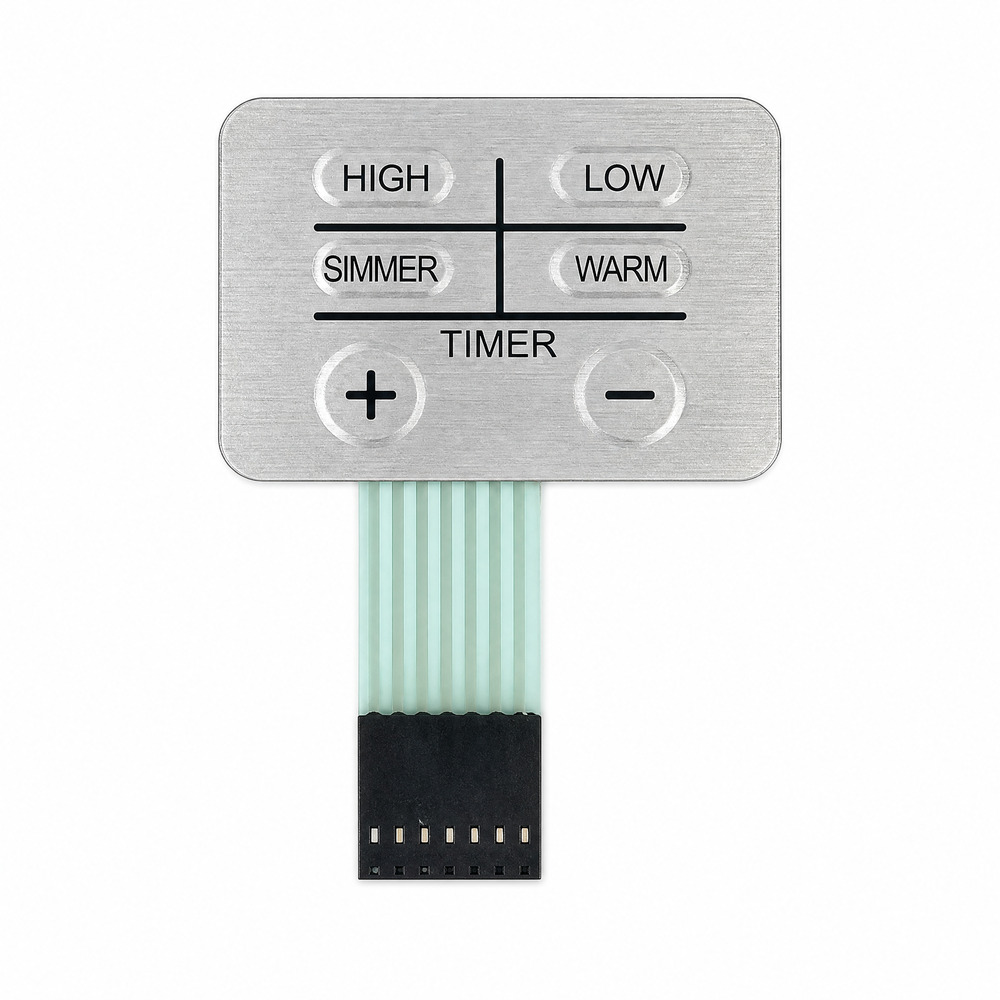
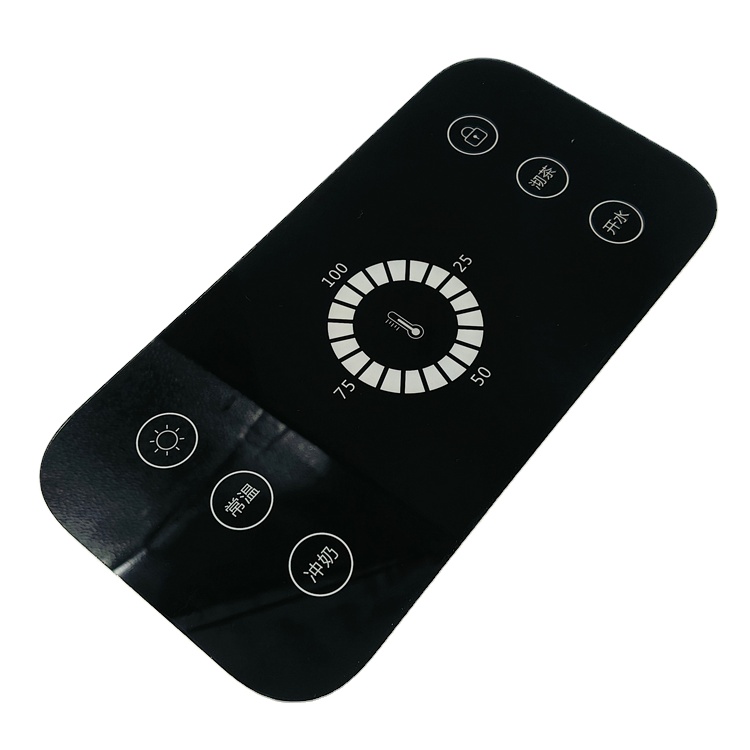
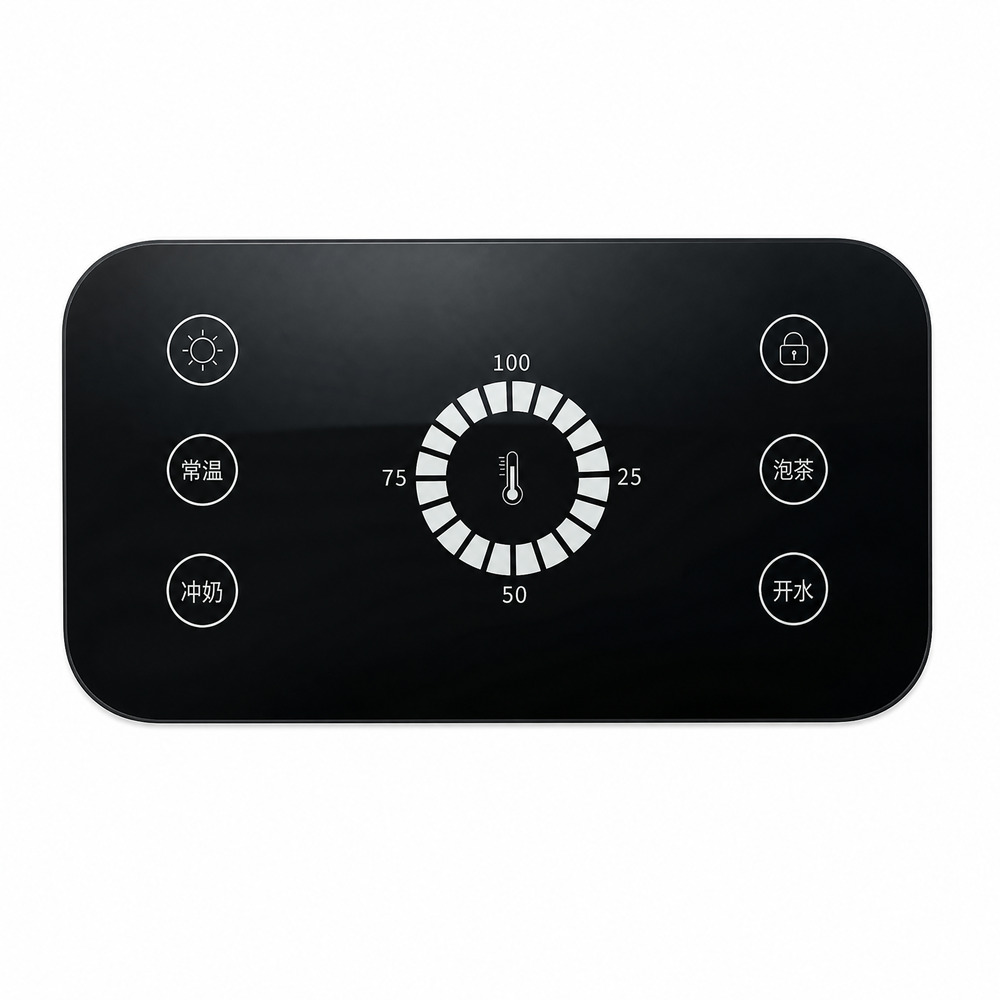
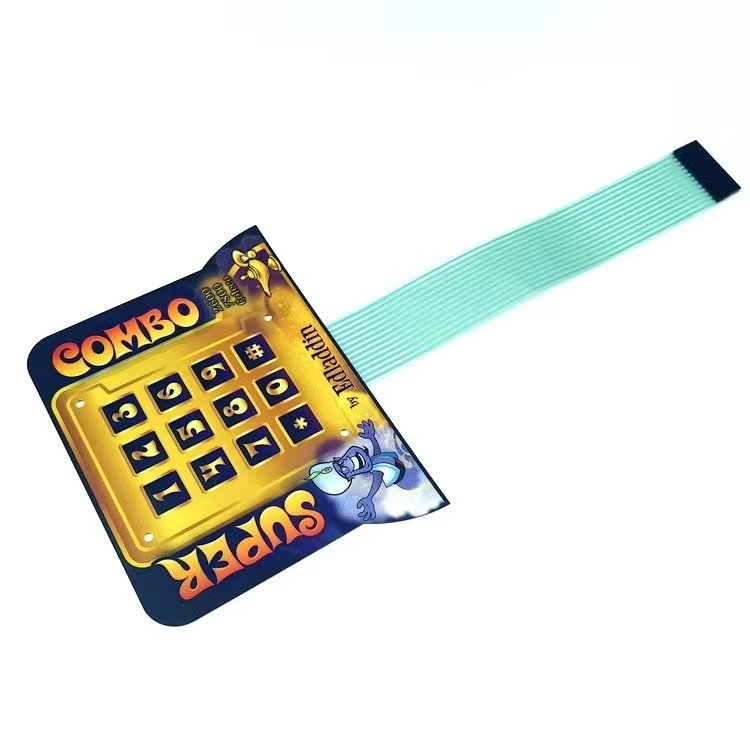
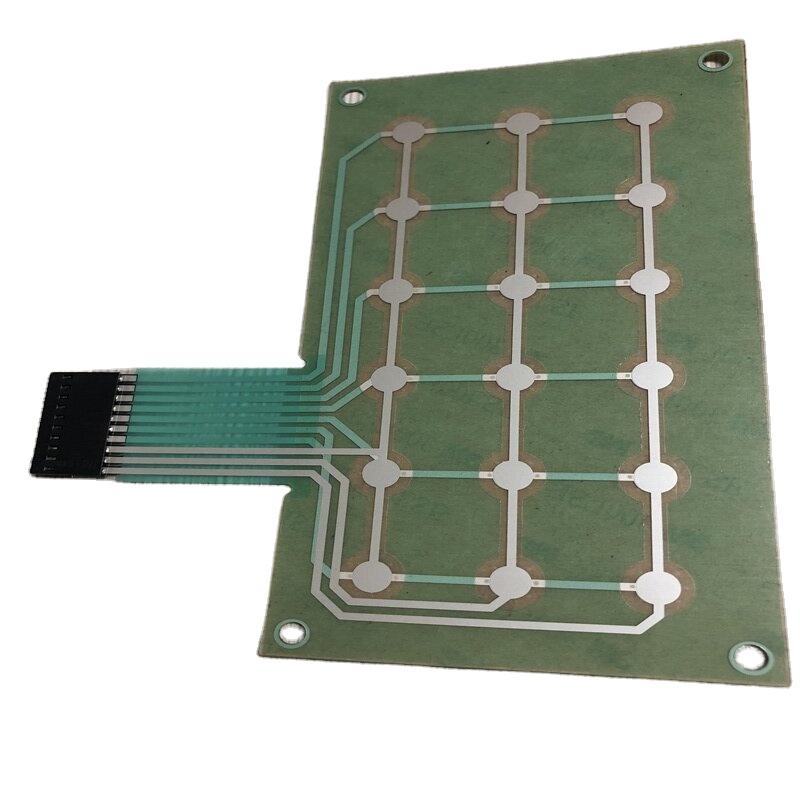
Procuring industrial electronics for deployable applications in Cuba requires direct engagement with severe environmental challenges. Unlike standardized climate-controlled environments, facilities across Havana, Mariel Special Development Zone (ZEDM), Matanzas, Cienfuegos, and Holguín subject control apparatus to elevated relative humidity (frequently exceeding 85% to 90%), persistent ambient temperatures between 30°C and 40°C, and airborne salinity blown inland from coastal coastlines. When designing customized OEM LED backlit membrane switches for such sectors, conventional adhesive grades and low-grade conductive inks rapidly experience electrochemical migration, silver dendrite development, contact failure, and graphic delamination.
Dongguan Ravo Electronics Co., Ltd. (Ravo Keypad) brings over two decades of specialized membrane switch R&D and production excellence to Caribbean purchasing authorities and engineering firms. Operating an expansive 12,000 m² modern manufacturing plant in Fenggang, Dongguan, our engineering team manufactures custom human-machine interface panels designed explicitly to survive thermal shifting, ionic corrosion, aggressive sterilization regimens, and intermittent grid stability. Through high-grade Autotype MacDermid PET overlays, genuine 3M marine-grade adhesives (such as 3M 467MP, 468MP, and 300LSE for low-surface-energy plastics), and micro-encapsulated SMD LED backlighting systems, we supply custom human-machine interface products that maintain uninterrupted uptime.
To eliminate short circuits caused by moisture infiltration, Ravo avoids generic PVC or vulnerable polycarbonate front plates in tropicalized builds unless specially coated with automotive UV blockers. Instead, we standardize on multi-layered, biaxially oriented polyethylene terephthalate (PET) films. PET provides outstanding chemical resistance to aggressive disinfectants, fuels, mild acids, and industrial solvents, while exhibiting an actuation fatigue life that surpasses polycarbonate by a factor of ten.
| Layer Component | Material Specification | Engineering Benefit for Caribbean Deployments |
|---|---|---|
| Graphic Overlay | Autotex F150 / F200 Fine Textured PET or Hardcoated Polycarbonate | Exceptional resistance against UV degradation, scratch resistance, and chemical wipes (alcohols, detergents). |
| Backlighting Layer | Ultra-thin SMD LEDs (0603/0805) embedded in Light Guide Film (LGF) or Side-lit array | Uniform luminous diffusion across dark operating consoles without hot spots; high energy efficiency under fluctuating voltages. |
| Top Circuit & Traces | DuPont / Acheson High-Grade Conductive Silver Paste with Carbon Overprint | Carbon bridging eliminates silver oxidation, electro-migration, and trace detachment in high humidity environments. |
| Tactile Elements | Nickel-plated or Gold-plated Stainless Steel Domes (12mm-16mm, 250g-400g trip force) | Crisp tactile click feedback allowing accurate operator engagement even when utilizing industrial work gloves. |
| Adhesive System | 3M 467MP / 468MP / 9448A / 300LSE High-Performance Acrylic | Shear strength remains intact across -40°C to +105°C; seals perimeter edges against salt spray and moisture penetration. |
| Sealing Perimeter | Continuous Hydrophobic Gasket Barrier (IP65 to IP67 Rated Design) | Blocks vapor ingress and direct liquid washdowns commonly required in medical and food processing environments. |
Our custom OEM LED backlit membrane switches, FPC/PCB integrated keyboards, and graphic overlays are designed directly to fulfill operational requirements across Cuba's industrial framework:
Havana's renowned pharmaceutical and medical device manufacturing nodes require IP67 sealed, anti-microbial membrane switch interfaces for centrifuges, diagnostic incubators, infusion monitors, and cleanroom consoles that resist daily sterilization with ethanol and sodium hypochlorite.
Varadero and the Cayos require reliable, backlit front control panels for heavy-use hotel automation, commercial kitchen ovens, dishwashing machinery, and water treatment dispensers. Integrated LED backlighting ensures seamless functionality during scheduled energy conservation periods.
In processing facilities across Matanzas and Villa Clara, interface consoles encounter severe dust, sugar residues, washdown cycles, and ambient vibrations. Our metal-dome tactile arrays deliver unmistakable mechanical feedback, preventing false triggers in noisy refinery spaces.
As Cuba accelerates solar farm deployments and modernizes thermoelectric infrastructure, solar inverter interfaces and petrochemical monitoring boxes need UV-stable, high-contrast, dead-front backlit indicator switches capable of operating outdoors under blistering solar irradiance.
Deployments in the Port of Mariel require salt-fog resistant membrane switches for container handling equipment, crane consoles, and dockside communications units where non-corrosive FPC tails and nickel-gold plating prevent pin galvanic decay.
Commercial transport fleets and specialized public agricultural machinery demand compact dashboard control keypads equipped with wide-angle LED night backlighting, ruggedized tactile switches, and resistance to diesel fuel, lubricants, and engine compartment thermal spillover.
The procurement landscape in Cuba is actively shifting. With state modernization programs and infrastructure projects prioritizing operational longevity, buyers are moving away from fragile mechanical micro-switches that fail prematurely due to dust and moisture exposure. Key industry shifts include:
1. Demand for Low-Power LED Backlighting Systems: Energy conservation protocols across Cuban state entities have made energy-efficient LED configurations standard. Our ultra-thin Light Guide Film (LGF) architecture achieves uniform illumination across the entire switch area with just 2 to 4 low-power SMD LEDs, reducing thermal output and power consumption substantially compared to outdated electroluminescent (EL) lamps.
2. Consolidation of PCB-Backer Modules: More system builders in the Mariel development zone are adopting rigid PCB-backed membrane assemblies. By soldering SMT connectors, microcontrollers, buzzer circuits, and LED arrays directly to a single FR-4 backing plate, OEMs eliminate redundant wiring harnesses, reduce assembly time on local production lines, and improve structural stability against physical drop shocks.
3. Transition from Domestic Retrofitting to Long-Lifecycle Turnkey OEM Parts: Industrial plant maintenance directors frequently rely on retrofitting imported machinery. Sourcing exact-fit, direct-replacement membrane switches from Ravo allows engineers to revive legacy German, Russian, Italian, and Chinese machinery controllers with improved humidity sealing, clear display windows, and updated graphic layouts.
Founded in 2003, Dongguan Ravo Electronics Co., Ltd. has established itself as an authoritative partner for high-reliability Human-Machine Interface technologies. Here is how our production infrastructure and engineering standards protect your supply chain:
• Integrated In-House Manufacturing: We run an end-to-end operation inside our 12,000 m² cleanroom-equipped plant. From CAD drawing verification, laser film cutting, precision silkscreen printing, and semi-automatic die-cutting to surface-mount soldering and hydraulic embossing, every production step is tightly controlled in Dongguan.
• Rapid Engineering Response (≤2 Hours): In an international project, slow engineering feedback creates critical bottlenecks. Our team of experienced HMI engineers typically delivers comprehensive Design-for-Manufacturability (DFM) reviews, layer stack-up proposals, and trace optimization notes within two hours of file receipt.
• Prototypes from 1 Piece & Low MOQs: We understand the prototyping stages of specialized Cuban infrastructure investments. While our high-capacity lines easily scale to hundreds of thousands of units, our rapid prototyping department supports pilot runs from 1 to 10 pieces with production-grade materials.
• 100% Electrical & Environmental Verification: Every membrane circuit leaving our facility undergoes automated electrical pin-to-pin continuity and resistance testing. Batch sampling validates actuation cycle life (tested beyond 1 million operations), thermal cycling resistance (-40°C to +85°C), and humidity threshold endurance.
• Certified Compliance: All manufactured components utilize authentic materials fully compliant with ISO 9001 quality management guidelines, RoHS directives, and REACH standards, backed by authentic certificate documentation.
We accommodate rapid prototyping from 1 to 5 pieces for proof-of-concept testing. For mass OEM production runs, our standard minimum order quantity typically ranges between 100 and 500 units depending on complexity, tool requirements, and circuit types.
We use premium conductive silver pastes overprinted with a protective carbon-ink layer. This blocks silver migration even when moisture is present. For extreme installations, we recommend our sealed polyimide FPC or rigid FR-4 PCB substrates with gold-plated contact fingers.
Please provide vector artwork or mechanical files in DXF, DWG, STEP, AI, or PDF format. Specify graphic colors (using Pantone solid coated codes), LED color assignments, key actuation forces, connector pitch (such as 2.54mm or 1.0mm ZIF), and housing surface materials.
Yes. Reverse engineering is one of our core specialties. You can send an intact or partially damaged original sample to our Dongguan factory. Our team will measure dimensions, scan circuit pathways, match Pantone colors, and fabricate direct replacements.
We supply comprehensive export documentation including Commercial Invoices, Packing Lists, Certificates of Origin (CO), RoHS material declarations, and test certificates. Parts are packed in vacuum-sealed anti-static bags with moisture-absorbing desiccant packs.
Once CAD drawings and color swatches are approved, prototypes ship within 7 to 12 working days. Full mass-production runs typically take 2 to 3 weeks depending on component availability and overall order volume.
