 EN
 DE
 FR
 ES
 RU
 JA EN DE FR ES RU JA
Precision-engineered front panel overlays, PET/PC keypads, and tactile interfaces manufactured for rigorous operating environments.
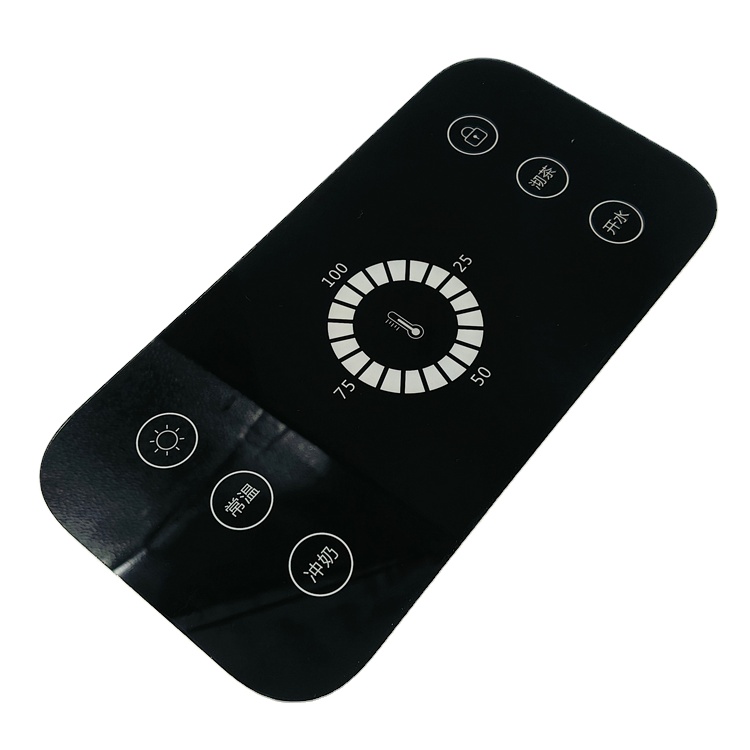
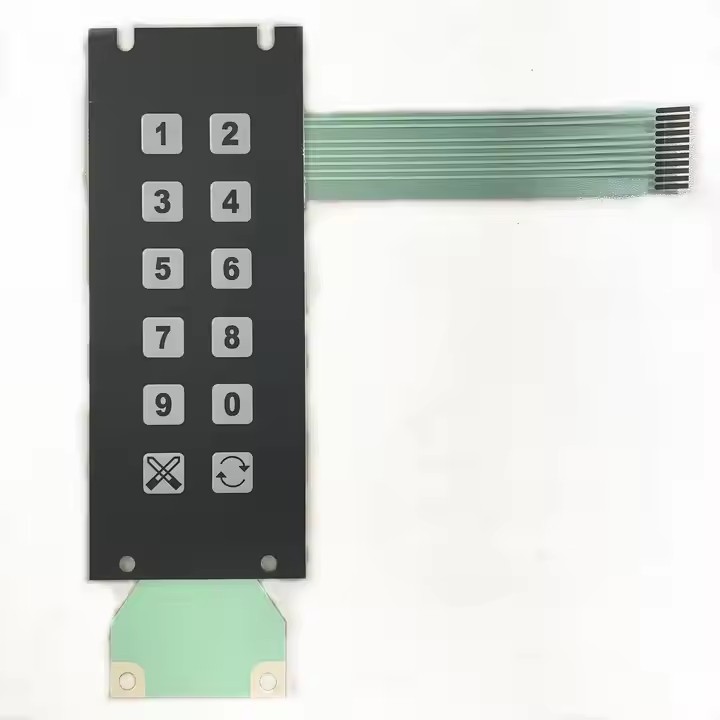
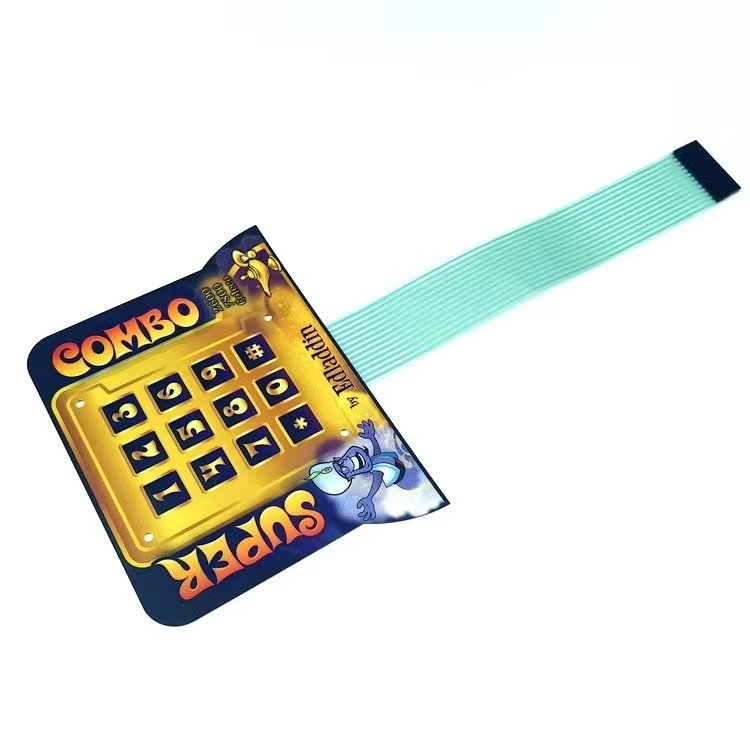
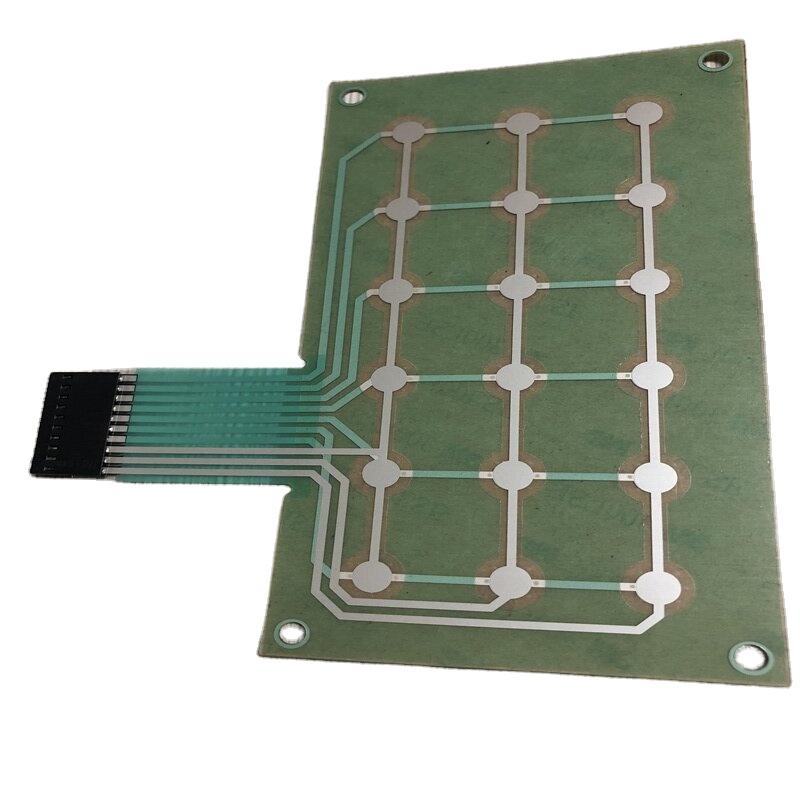
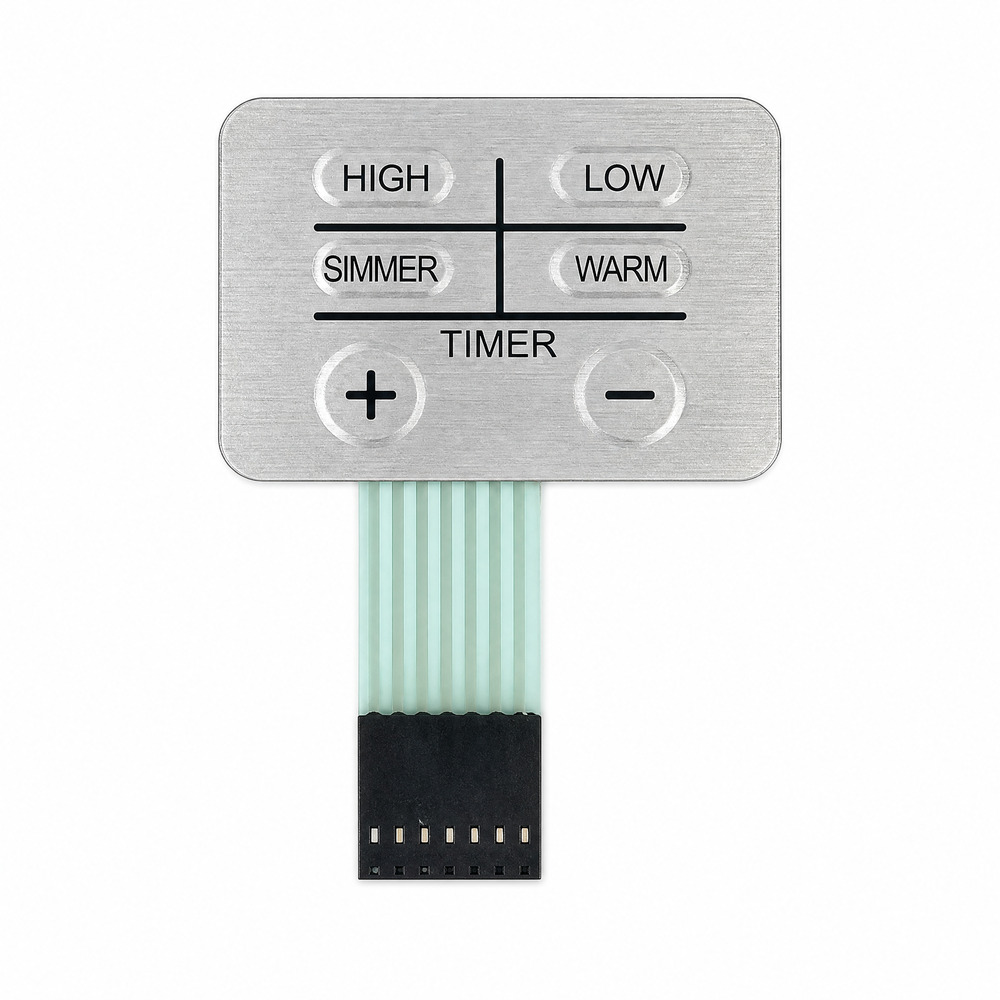
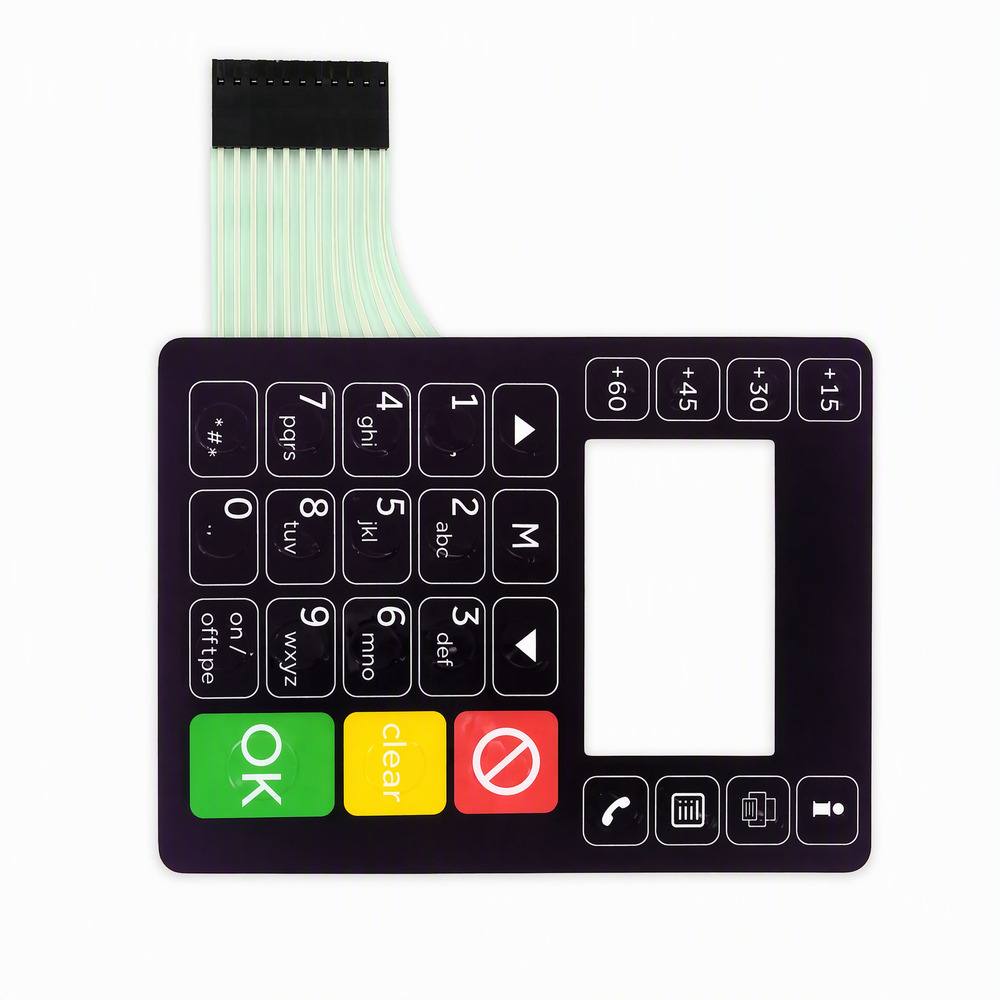
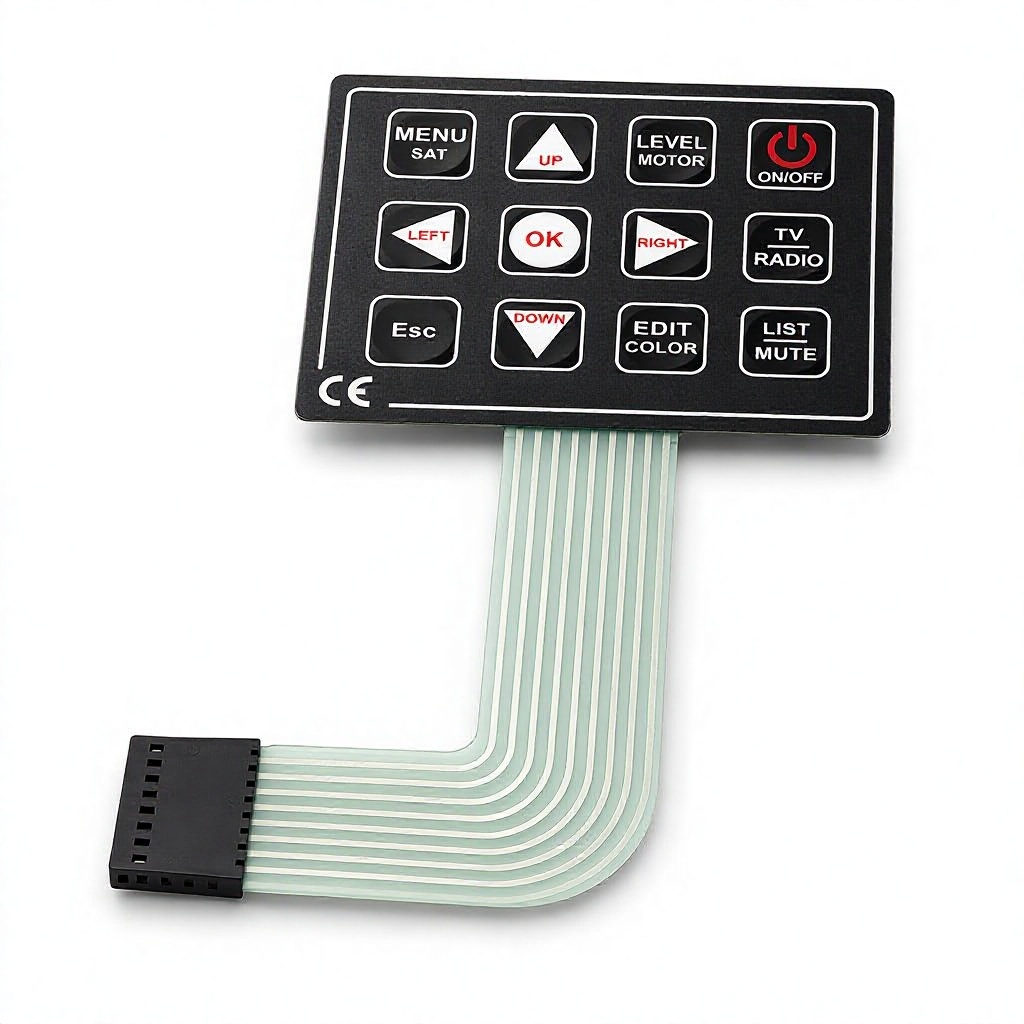
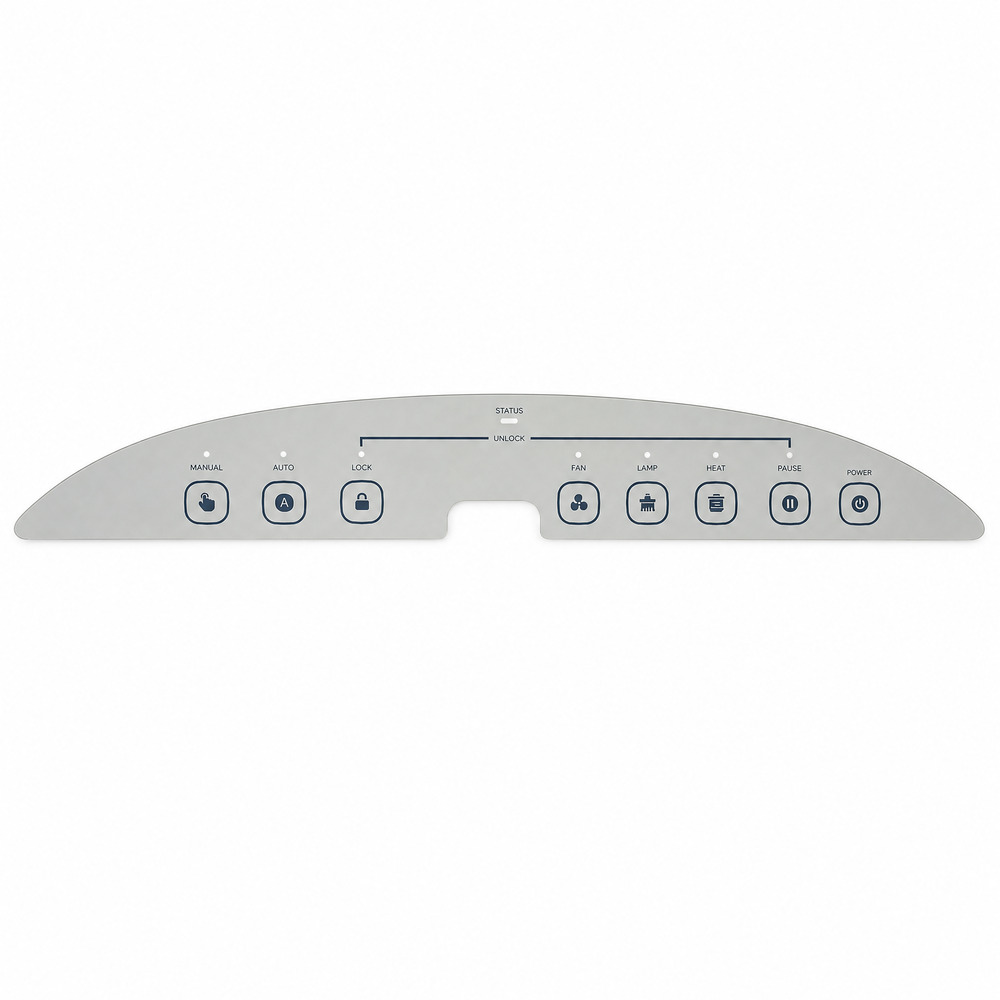
Human-Machine Interfaces (HMI) serve as the vital sensory interface between users and modern electronic systems. In the context of industrial equipment, medical instrumentation, commercial appliances, and regional agricultural automated systems, the front panel overlay is much more than a cosmetic skin. It is a highly engineered, multi-layered protective and functional membrane that shields internal electronics against moisture, dust, ultraviolet radiation, chemical solvents, and mechanical abrasion.
As original equipment manufacturers (OEMs) and contract assemblers serving the San Ignacio market and broader Central American regions expand their production of eco-tourism control systems, off-grid power management units, agricultural processing machinery, and commercial hardware, the demand for custom-built front panel overlays has experienced exponential growth. Delivering high-reliability overlays requires rigorous material science, sub-micron screen printing accuracy, chemical-resistant adhesives, and precise die-cutting execution.
A commercial-grade membrane overlay stack-up manufactured by Dongguan Ravo Electronics Co., Ltd. consists of several specialized layers, each serving a distinct engineering function:
San Ignacio, located in the Cayo District of Belize, stands as a major hub for eco-tourism infrastructure, sustainable agricultural production, renewable energy distribution, and municipal water management. Operating electronic hardware in this environment demands hardware designed specifically to withstand high ambient humidity, heavy seasonal rainfall, intense solar UV indices, and fluctuating power conditions.
Off-grid resorts, eco-lodges, and remote research stations surrounding San Ignacio rely on solar invertors, battery bank management panels, and water filtration controllers. Custom front overlays featuring IP67 perimeter sealing and dead-front backlighting allow operators to monitor power and water metrics effortlessly, even in damp jungle microclimates.
Central Belize's agricultural belt requires robust control panels for grain drying, citrus processing, and timber milling equipment. Overlays engineered with chemical-resistant PET and 3M 468MP high-cohesion adhesive prevent oil, chemical fertilizer, and grain dust ingress from short-circuiting control electronics.
Commercial fuel stations along the George Price Highway and outdoor municipal kiosks require non-tactile, high-durability keyboards. Using sub-surface silkscreen printing on UV-stabilized polycarbonate ensures key legends remain sharp despite constant exposure to gasoline fumes and heavy daily user interaction.
As international supply chains shift toward nearshoring and regional decentralization, equipment builders and repair hubs in San Ignacio and regional industrial parks are upgrading legacy mechanical switch panels to modern, sealed membrane overlays and capacitive touch keypads. Key market trends driving this shift include:
Traditional push-button switches with mechanical bezels frequently fail in tropical regions due to humidity condensation and dust accumulation behind buttons. Modern OEMs in the San Ignacio market are exclusively adopting continuous membrane overlays with fully enclosed perimeter gaskets and sealed flex tail exits, achieving IP67 wash-down performance.
Medical clinics, food processing centers, and high-end hospitality venues are increasingly opting for sleek, capacitive touch graphic overlays. By eliminating mechanical moving parts entirely, the smooth front panel can be wiped down easily with harsh disinfectant alcohol or chlorine solutions without degrading the graphics or electrical traces underneath.
Regional equipment integrators cannot afford 8-to-12-week lead times for localized custom hardware repairs or prototype builds. Factories like Dongguan Ravo Electronics Co., Ltd. fulfill this market demand by offering engineering DFM evaluations within 2 hours, digital prototype production from 1 single piece, and direct express delivery to Central America within days.
Selecting the optimal material substrate is the single most critical decision when designing a custom OEM front panel overlay. The comparative engineering matrix below illustrates the performance trade-offs:
| Engineering Property | Autotex Polyester (PET) | Lexan Polycarbonate (PC) | Cast Acrylic (PMMA) |
|---|---|---|---|
| Flexural Life (Actuation Domes) | > 5,000,000 cycles (Exceptional) | ~ 100,000 cycles (Moderate) | Rigid / Non-Flexible |
| Chemical & Solvent Resistance | Outstanding (Acids, Alcohol, Oils) | Moderate (Vulnerable to Aromatics) | High Chemical Resistance |
| Impact Resistance | High | Extremely High (Unbreakable) | Moderate / Brittle on Impact |
| Optical Window Clarity | Very High (With Clear Window Treatment) | Crystal Clear (>91% Transmission) | Optically Superior (>92%) |
| UV & Outdoor Weatherability | Excellent (UV-Hardcoated Grades) | Requires UV Inhibitor Coating | Inherent UV Resistance |
| Primary Application | Membrane Switches & Embossed Overlays | Heavy-Impact Display Panels & Lenses | Thick Structural Control Bezels |
Dongguan Ravo Electronics Co., Ltd., located in Fenggang Town, Dongguan, China, has been an industry-leading manufacturer of custom membrane switches, graphic overlays, silicone rubber keypads, flexible printed circuits (FPC), and thin-film pressure sensors since 2003. Operating from a state-of-the-art 12,000 m² cleanroom facility, Ravo seamlessly bridges the gap between high-precision Chinese manufacturing expertise and global procurement demands.
Over two decades of continuous innovation in HMI engineering. Our experienced production team has delivered over 15,000 unique overlay designs to clients across Europe, North America, and Latin America.
Our dedicated engineering department evaluates your CAD drawings (DXF, DWG, AI, PDF) and provides Design for Manufacturability (DFM) feedback and stack-up optimization within 2 hours during operational hours.
ISO 9001 certified manufacturing workflow with 100% electrical continuity testing, spectrophotometer color matching (Pantone/RAL delta E < 0.5), life cycle stroke testing, and full RoHS/REACH compliance.
Whether you require 1 to 10 prototype units for urgent field-testing in San Ignacio or volume production runs exceeding 100,000 units, Ravo offers full vertical integration: screen-printing, automated die-cutting, cleanroom lamination, surface mount LED assembly, and anti-static export packaging under one roof.
Answers to common technical, logistics, and material procurement questions regarding custom OEM front panel overlays:
