EN
 DE
 FR
 ES
 RU
 JA EN DE FR ES RU JA
Custom-engineered Human-Machine Interfaces (HMIs) built for extreme humidity, salt spray, and continuous industrial use in oceanic environments.
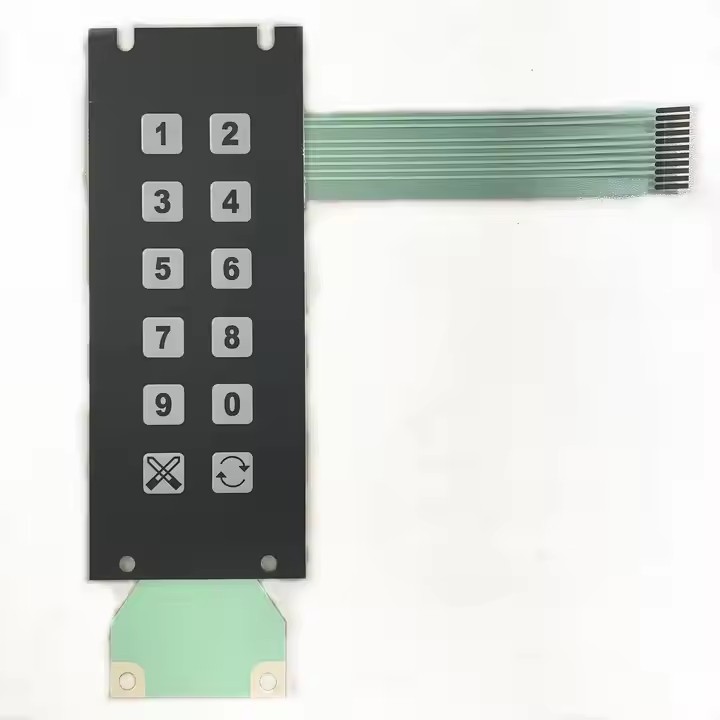
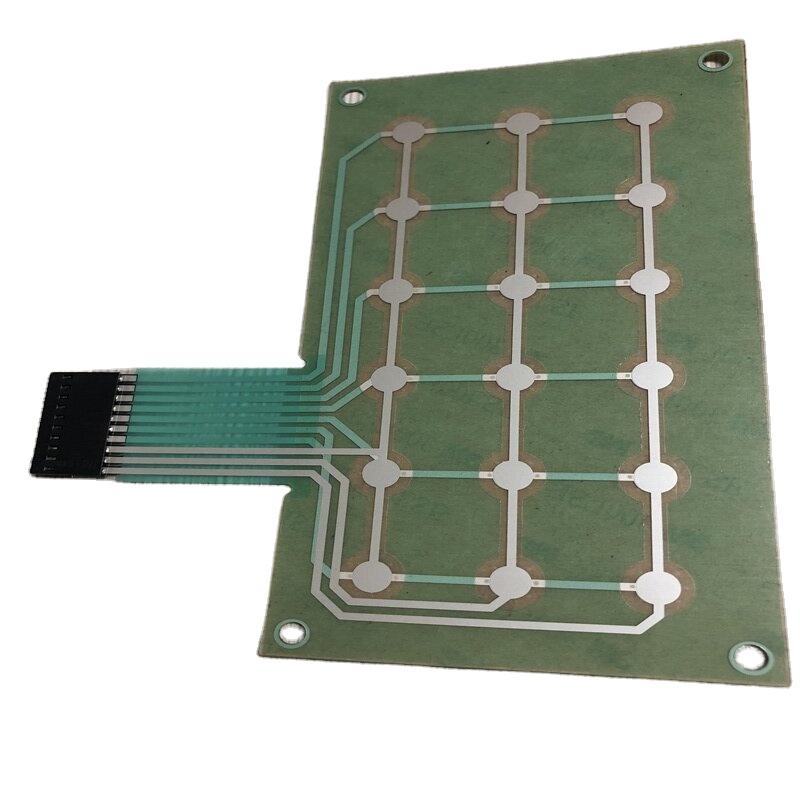
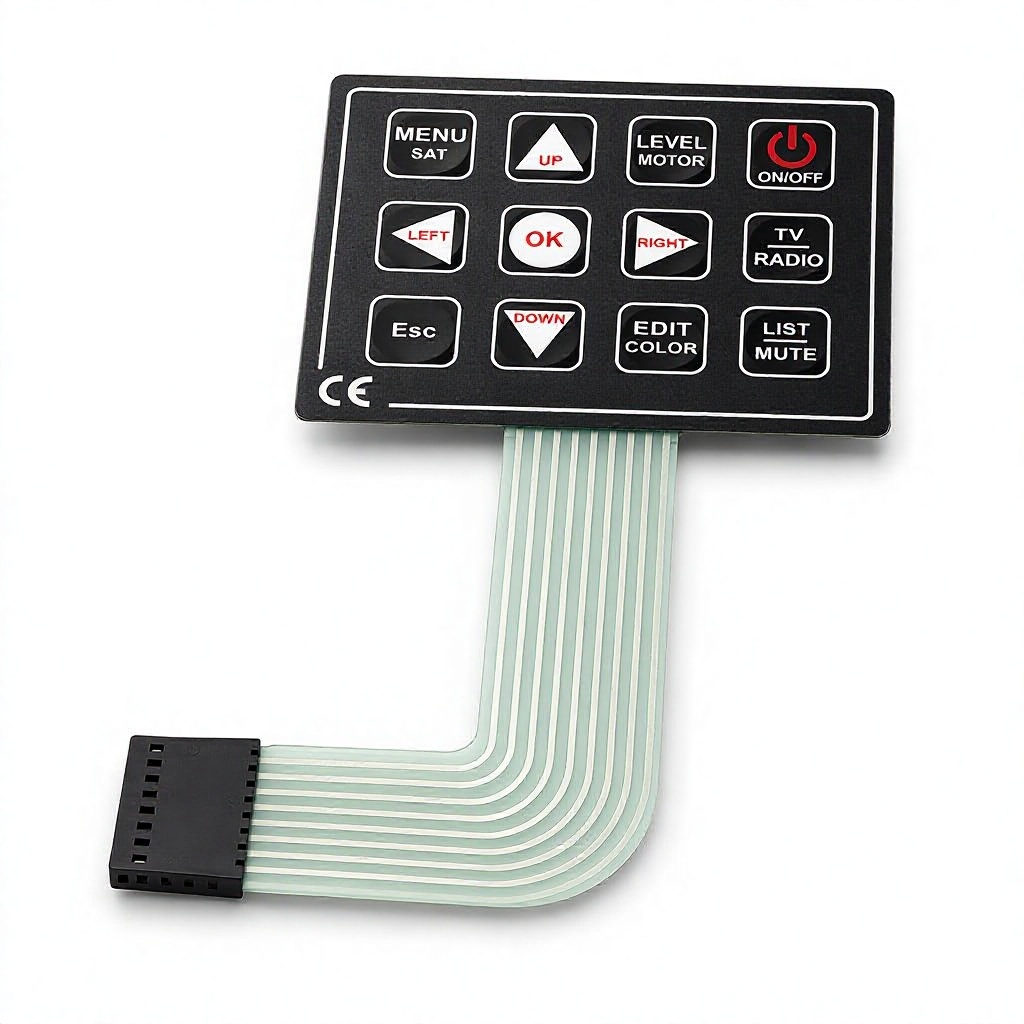
Operating human-machine interface (HMI) keypads in the Republic of the Marshall Islands (RMI)—encompassing Majuro Atoll, Ebeye, Kwajalein, and remote maritime zones—presents extraordinary environmental challenges. Situated in the equatorial Pacific, equipment installed in this region faces perpetual exposure to atmospheric salt fog, high ultraviolet radiation (UV Index > 11 year-round), and continuous relative humidity exceeding 85% to 95%. Standard commercial membrane keypads rapidly suffer from conductor migration, silver ink oxidation, overlay delamination, and LED backlighting driver short-circuits under these aggressive conditions.
Dongguan Ravo Electronics Co., Ltd. (Ravo) brings over two decades of specialized expertise as a premier CE-certified membrane switch manufacturer and exporter. To survive the Pacific atoll environment, Ravo's illuminated membrane switches are designed with multi-layer hermetic perimeter sealing, UV-stabilized Autotype XE polyester graphics, and hydrophobic venting membranes. This deep engineering focus ensures zero moisture ingress, stable contact resistance, and prolonged backlight luminance for critical infrastructure and marine controllers throughout Micronesia.
Information Gain Insight: Standard PET circuits rely on perimeter acrylic adhesives that allow moisture vapor transmission over prolonged exposure to tropical humidity. Ravo integrates specialized hydrophobic perimeter gaskets combined with 3M 9448A / 468MP high-tack adhesive systems and sulfur-resistant conductive silver ink traces to eliminate silver dendrite growth entirely.
| Engineering Parameter | Standard Commercial Grade | Ravo Ocean-Grade Marine Spec (Marshall Islands) |
|---|---|---|
| Base Overlay Material | Standard Polycarbonate (PC) / Matte PET | Autotype Polyester (PET) with Hardcoated UV-Stabilized Surface |
| Ingress Protection (IP Rating) | IP54 to IP65 | IP67 / IP68 Fully Hermetically Sealed Perimeter |
| Salt Fog Corrosion Resistance | 24 Hours (ASTM B117) | 96+ Hours Continuous Salt Spray Resistance (ASTM B117) |
| Operating Temperature Range | -10°C to +50°C | -40°C to +85°C Extreme Environmental Range |
| Circuit Backbone Options | Single-layer Silver Ink on PET | Polyimide Flex Circuit (FPC) / Rigid FR4 PCB / Silver PET with Carbon Cap |
| Illumination Options | Basic SMD LED Surface Mounted | Side-lit LGF (Light Guide Film), EL, or High-Brightness Low-Power LEDs |
| Mounting Adhesive Layer | Standard Acrylic Tape | 3M 467MP / 3M 468MP / 3M 300LSE High-Surface-Energy Adhesives |
The Marshall Islands market demands exceptionally resilient hardware tailored to island logistics, maritime transport, utility microgrids, and local processing facilities. Ravo custom-engineers illuminated keypads and graphic control overlays specifically targeting these critical sectors:
Installs directly on ocean vessels, tuna purse seiners, and dockside navigation rigs. Illuminated keys feature high-contrast night backlighting (dimmable LEDs) and tactical metal domes to allow effortless operation even when wearing heavy deck gloves under stormy marine conditions.
Majuro and Ebeye rely heavily on reverse osmosis (RO) water purification units. Ravo's chemical-resistant PMMA and PET overlays resist chlorine, saltwater splash, and cleaning solvents while maintaining crystal-clear display windows for digital sensor readouts.
Outer island electrification projects in RMI deploy solar-battery hybrid systems. Ravo supplies illuminated capacitive touch keyboards with dead-front graphics, ensuring seamless aesthetics and dustproof/waterproof sealing for remote inverter control panels.
For clinical devices in Majuro Hospital, hygienic operation is non-negotiable. Ravo’s antibacterial textured graphic overlays feature wipe-clean flat surfaces or smooth pillow embossing, fully resistant to hospital-grade disinfectants and alcohol swabs.
Outdoor terminals along Marshall Islands docks require heavy-duty keypads with UV protection. Ravo manufactures matrix switches with 0.125mm to 0.25mm thick PET/PC graphic skins that do not yellow, craze, or crack under intense equatorial sunlight.
Integrates custom thin-film Force Sensitive Resistors (FSR) for seating occupancy detection on ferries, automotive equipment, and industrial safety mats operating across Pacific island trade routes.
As the Republic of the Marshall Islands accelerates its National Strategic Plan focusing on climate resilience, sustainable blue economy expansion, and renewable energy transition, equipment importers and regional OEMs face evolving procurement standards:
To assist electronic development engineers in selecting the optimum membrane switch stack-up for tropical oceanic deployment, Ravo’s R&D engineering team recommends following this material guideline:
Polyester (PET) is universally preferred over Polycarbonate (PC) for tropical outdoor environments. While PC offers high impact resistance, it degrades under intense UV radiation and is vulnerable to chemical cracking. Autotype XE / Fine-line Polyester films provide an flex-life exceeding 5 million actuations, extreme resistance to salt fog, and zero yellowing under continuous outdoor Pacific exposure.
For marine and heavy equipment, tactile response provides operators with instant physical confirmation of switch actuation. Ravo incorporates stainless-steel metal domes (nickel or gold-plated) ranging from 6mm to 20mm with actuation forces between 160g and 400g. Gold-plated domes are explicitly specified for marine high-salinity zones to prevent contact oxidation.
Illuminating membrane keypads for night-time operation can be achieved via surface-mounted SMD LEDs or Light Guide Film (LGF) technology. LGF delivers perfectly uniform illumination across large key areas with ultra-thin profile thickness (less than 0.2mm added to stack-up) while significantly reducing overall power consumption—a vital advantage for solar-powered island equipment.
Dongguan Ravo Electronics Co., Ltd. (established in 2003 in Fenggang Town, Dongguan) operates as a vertically integrated custom HMI solutions factory. Covering over 12,000 square meters of modern cleanroom workshops, Ravo handles the entire manufacturing spectrum in-house—from precision tool making, silkscreen and digital printing, laser die-cutting, automated SMT component placement, to 100% electrical inspection.
Our dedicated engineering department reviews your 2D/3D CAD drawings (DXF, DWG, AI, PDF) and returns a complete Design for Manufacturability (DFM) assessment with stack-up recommendations in 2 hours or less.
Support your R&D stage with low-risk prototyping. We build and ship custom functional samples from 1 to 10 pieces with fast turnaround before you commit to full-scale mass production tooling.
Every single membrane switch undergoes rigorous electrical continuity testing, resistance checking, short-circuit verification, and optical color-matching under Pantone standards before export packaging.
All materials—including raw PET/PC films, conductive silver pastes, 3M adhesives, and surface-mount LEDs—comply fully with EU RoHS, REACH, and ISO9001 quality management standards.
Beyond traditional membrane switches, Ravo specializes in silicone rubber keypads, FPC flex circuits, FR4 PCB backed assemblies, graphic control panels, and custom force-sensitive pressure sensors (FSR).
Experienced export logistics team providing custom moisture-barrier, anti-static export packaging designed to endure long transit air and sea freight routes serving Majuro, Guam, and the broader Oceania market.
We implement a full perimeter hermetic seal using 3M 9448A or 3M 468MP high-tack adhesives combined with anti-sulfuration conductive silver inks and gold-plated metal domes. This blocks salt air and water vapor from contacting conductive circuit traces.
For prototype development, our MOQ is as low as 1 to 10 pieces. Mass production batch sizes typically start from 100 to 500 pieces depending on layout complexity, backlighting method, and layer stack-up.
Yes. Every batch exported by Dongguan Ravo Electronics comes with ISO9001 factory documentation, CE compliance declarations, and material test reports confirming RoHS and REACH compliance.
You can send us vector files in 2D (AUTOCAD DXF, DWG, Adobe Illustrator .AI, vector PDF) or 3D files (STEP, IGES). Please specify Pantone color codes, LED backlight colors, and mounting surface texture.
Light Guide Film (LGF) backlighting with low-current SMD LEDs is ideal. It provides uniform legend illumination across all keys while consuming up to 60% less electrical power than traditional EL wire or bulk LED arrays.
After artwork approval, sample production takes 7 to 10 working days. Mass production requires 12 to 15 working days. Air express delivery to Majuro (via Honolulu or Guam routes) typically arrives in 5 to 8 days.
Yes. We manufacture PCB-backed membrane switches where rigid FR4 circuit boards support display modules, connectors, microcontrollers, and SMD components into a single plug-and-play assembly.
We evaluate your enclosure material and specify high-surface-energy mounting adhesives like 3M 300LSE or 3M 468MP, ensuring permanent bond strength without edge peeling over years of tropical use.
Partner directly with Dongguan Ravo Electronics Co., Ltd. Get a complete DFM engineering review and competitive direct-factory pricing for your Marshall Islands or international project within 2 hours.