 EN
 DE
 FR
 ES
 RU
 JA EN DE FR ES RU JA
Explore our field-tested membrane switch assemblies engineered for medical diagnostics, ruggedized military interfaces, high-temperature kitchen equipment, and outdoor industrial automation controls.
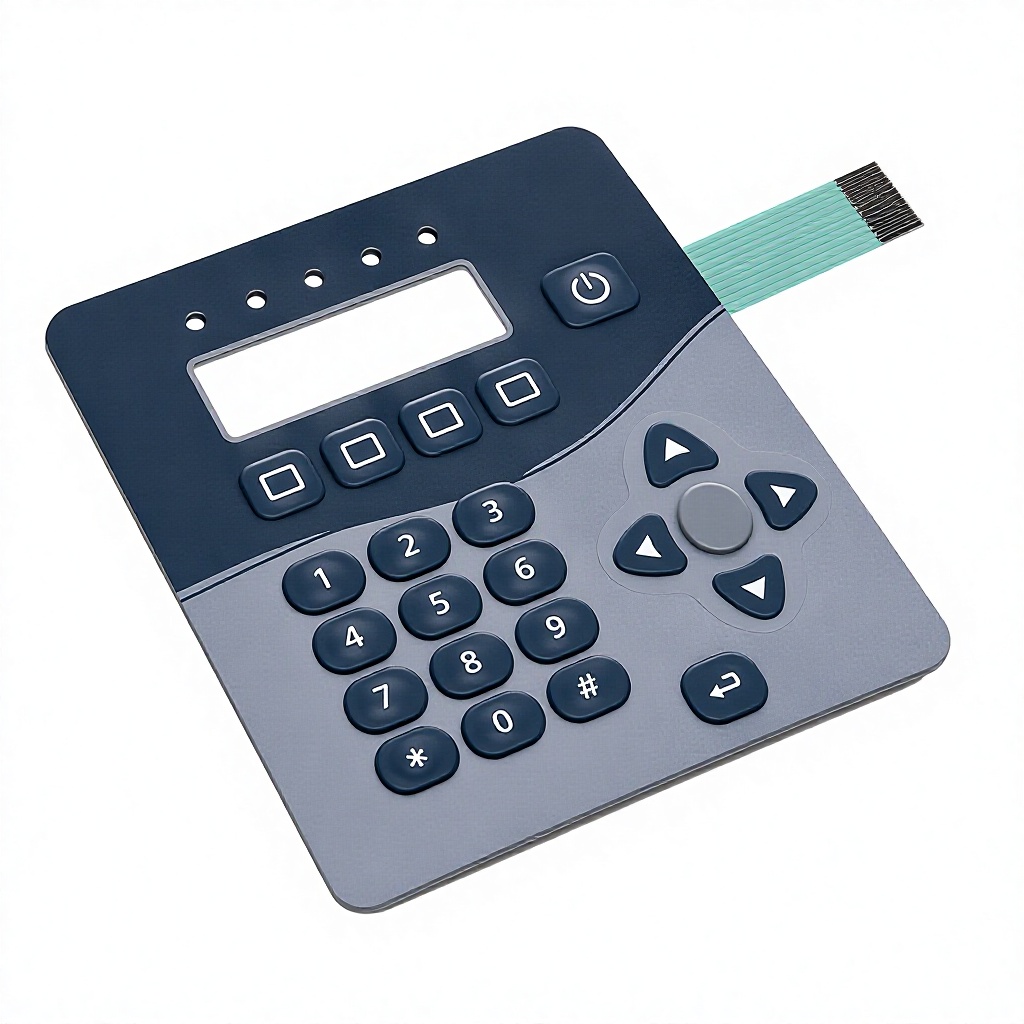
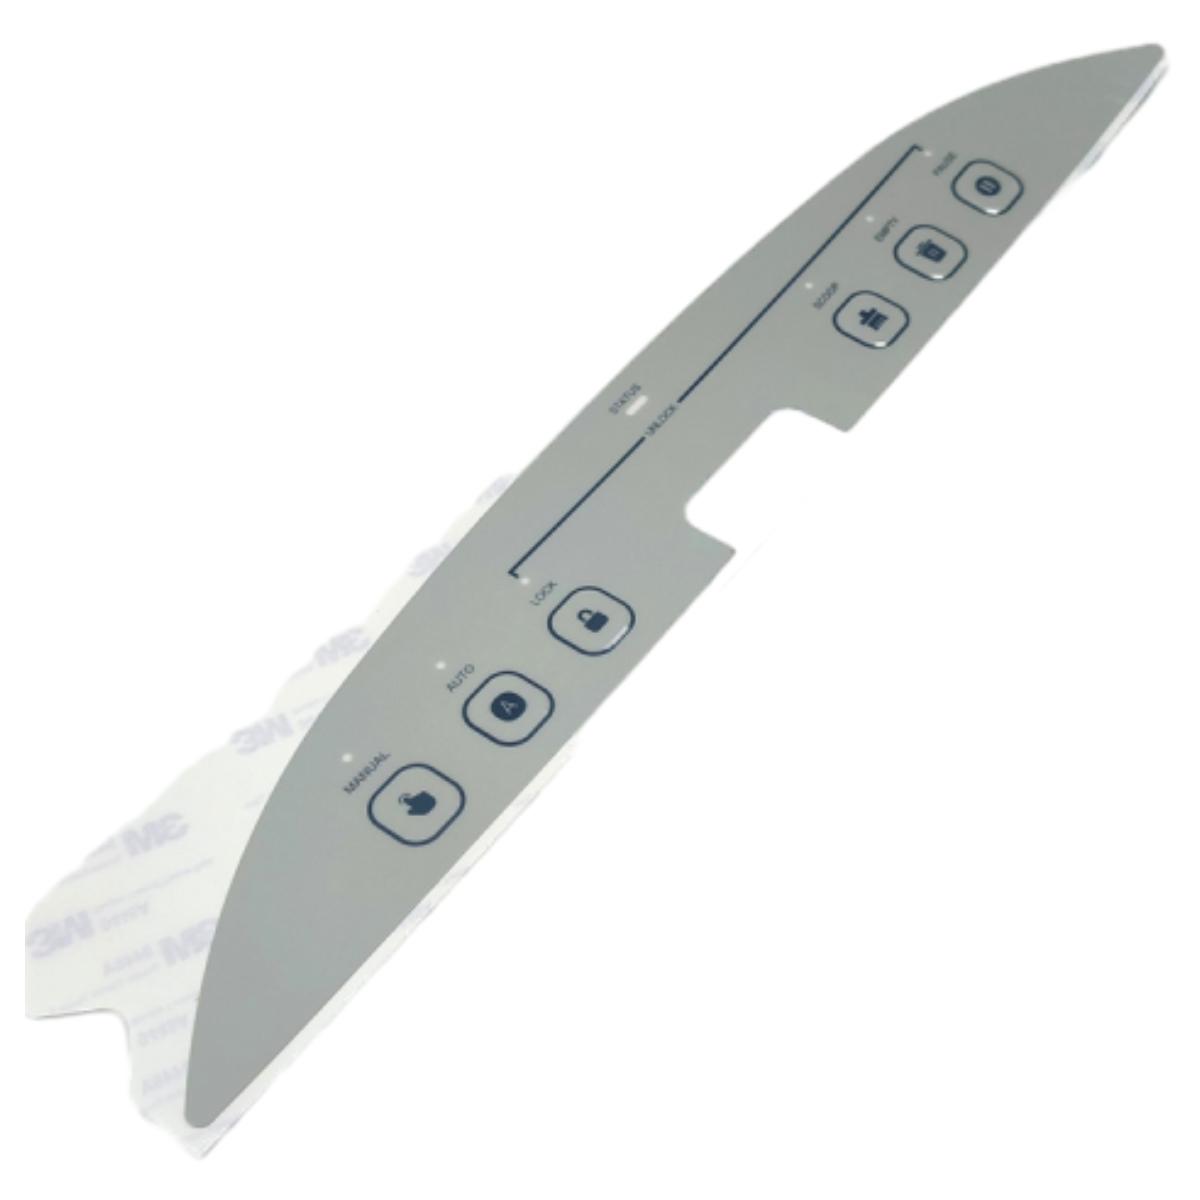
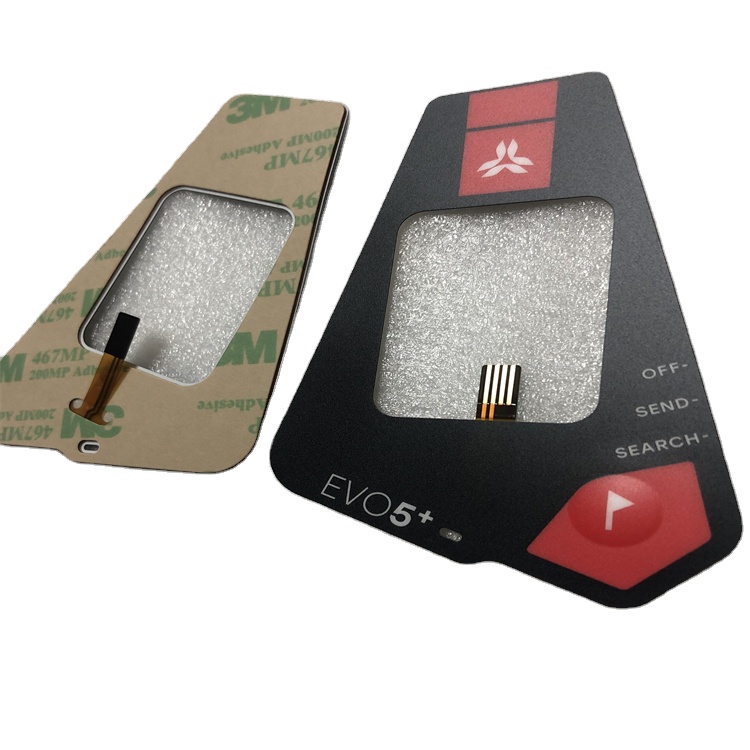
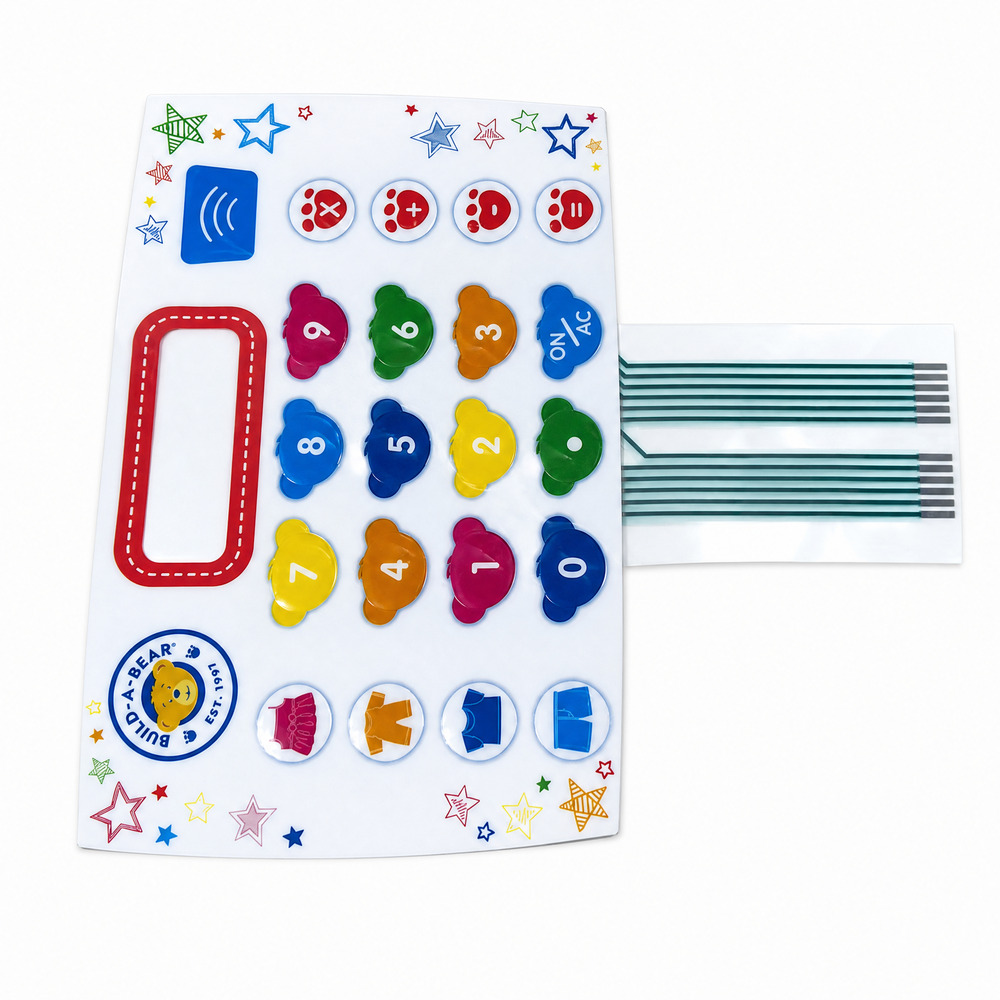
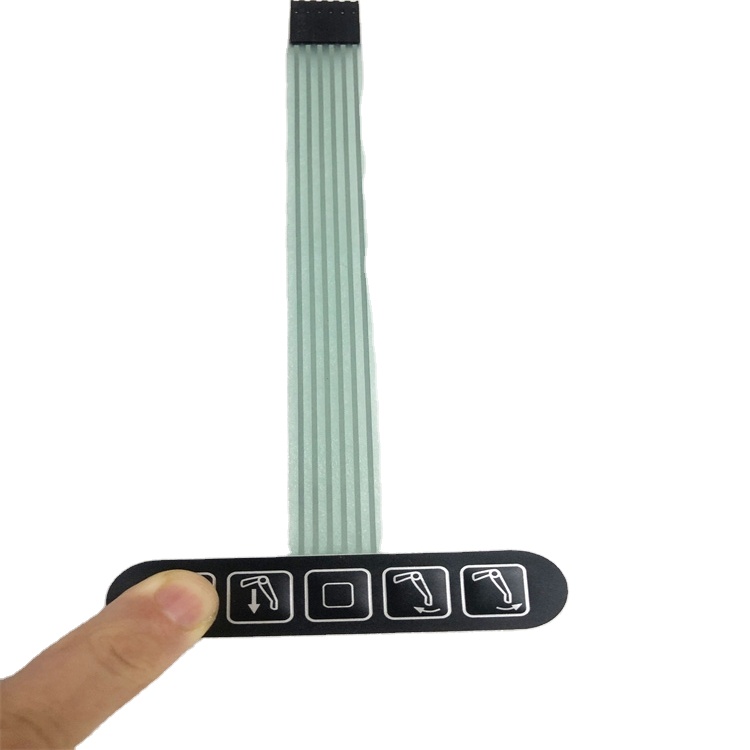
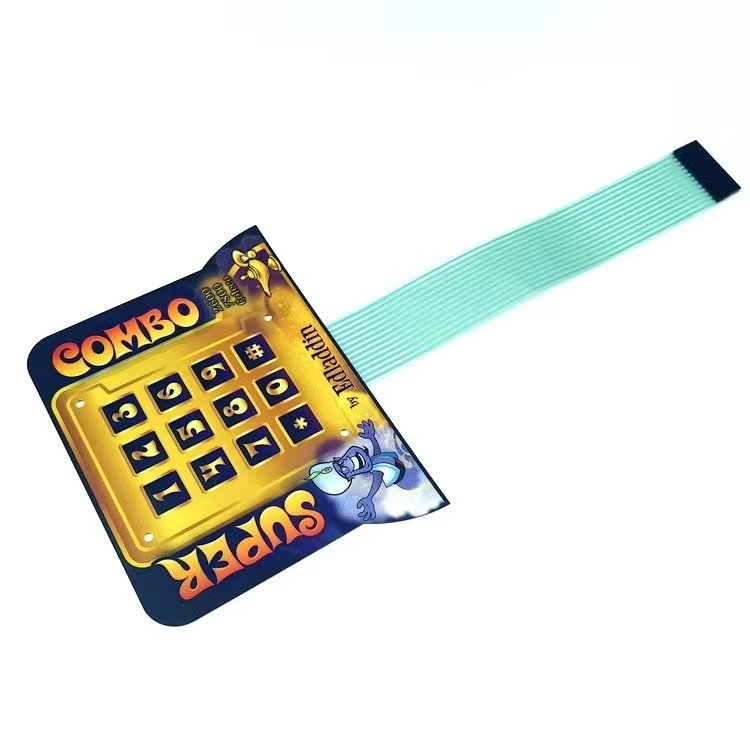
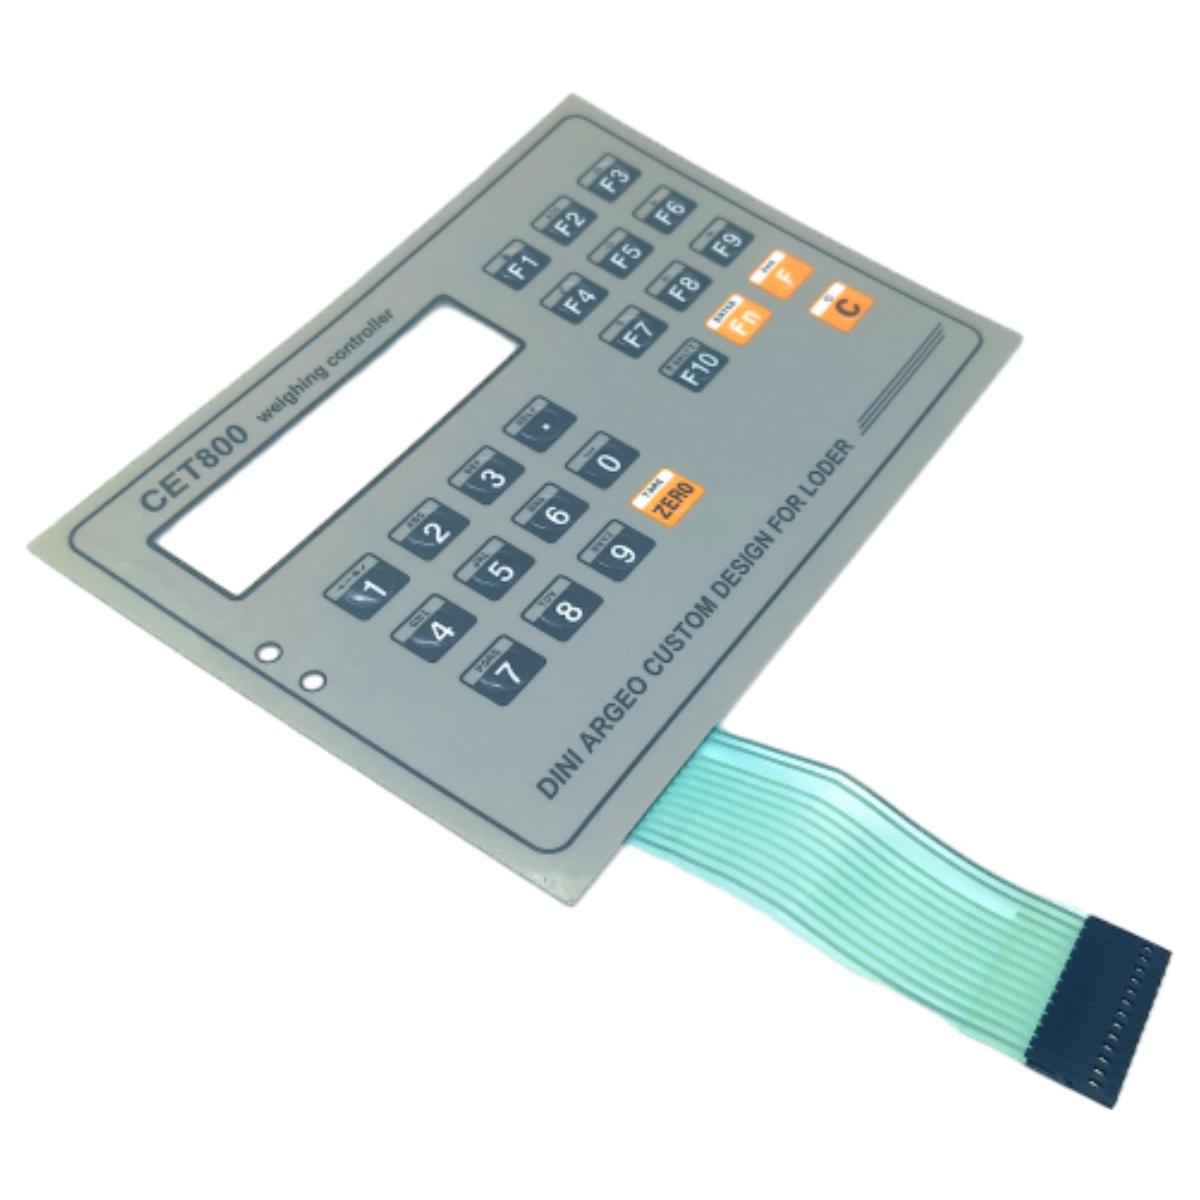
Industrial membrane switches are sophisticated multi-layer electromechanical sandwiches. Discover how our engineering choices prevent trace fracturing, resist aggressive chemical washdowns, and ensure 1,000,000+ flawless actuations.
We utilize premium biaxially oriented PET (Autotex XE/Fine/Velvet) and optical-grade Polycarbonate (Lexan). Silk-screened inks are printed in reverse on the underside of the film. This ensures that harsh cleaning chemicals, abrasive dust, and constant finger abrasion never degrade the legends, markings, or dead-front LED indicator icons.
Achieving the ideal tactile snap requires precise engineering between overlay dome embossing and metal dome selection. We utilize precision 301/304 stainless steel domes (nickel or gold-plated) available in 4-leg, round, or oblong formats, paired with retention spacer pockets designed to prevent dome migration under repetitive high-frequency cycling.
Electrochemical silver migration in humid environments is the #1 cause of field failures in low-cost membrane switches. Our factory mitigates this using selective carbon paste overcoating and UV dielectric barrier masks over all critical silver tracks, drastically lowering impedance drifts while maintaining loop resistance well below 100 ohms.
A standard 6-layer Ravo membrane switch includes: (1) Reverse-printed 0.15mm-0.20mm textured polyester overlay, (2) High-performance acrylic transfer adhesive (3M 467MP/468MP), (3) Precision die-cut dome retainer spacer with air venting channels, (4) Top circuit with conductive silver/carbon tracks or gold-plated metal dome arrays, (5) Dielectric insulating spacer, and (6) Rear mounting adhesive with custom release liner. For harsh environments, perimeter adhesive rings create hermetic IP67 water seals.
| Circuit Substrate Type | Typical Loop Resistance | Minimum Trace Pitch | Component Soldering | Actuation Durability | Optimal Application Tier |
|---|---|---|---|---|---|
| Screen-Printed PET (Silver Ink) | < 50Ω to 150Ω (geometry dependent) | 0.8mm to 1.0mm | Conductive Epoxy Bonding Only | > 1,000,000 actuations | Cost-Effective Industrial |
| Flexible Printed Circuit (FPC Copper) | < 2Ω to 10Ω (Ultra-low) | 0.3mm to 0.5mm (Ultra-dense) | Reflow / SMT Hand Soldering Compatible | > 5,000,000 actuations | Medical & Aerospace HMI |
| Rigid FR-4 PCB Backer | < 1Ω (Absolute minimum) | 0.2mm to 0.4mm | Standard Automated SMT Reflow | > 10,000,000 actuations | Heavy Duty / Structural Panel |
Founded in 2003, Dongguan Ravo Electronics Co., Ltd. has grown from a specialized technical workshop to a vertically integrated 12,000 m² smart manufacturing plant. We control the complete production chain from optical laser die-making to automated screen printing and 100% computerized electrical testing.
Our senior mechanical and electrical engineers review your CAD drawings (DWG, DXF, Gerber, STEP) and provide actionable DFM optimization within 2 hours.
Printing and optical bonding occur inside climate-controlled cleanrooms, eliminating microscopic dust inclusions behind transparent LCD/LED display windows.
We support pilot runs starting from just 1 piece without costly hard tooling by utilizing high-precision digital knife plotters and laser cutters.
Every single membrane switch undergoes computerized testing for trace continuity, open/short circuits, contact resistance, and dielectric insulation breakdown.
We strictly source genuine adhesives (3M 467MP, 468MP, 9448A) and films (MacDermid Autotype, Sabic Lexan) backed by full material test reports and RoHS compliance.
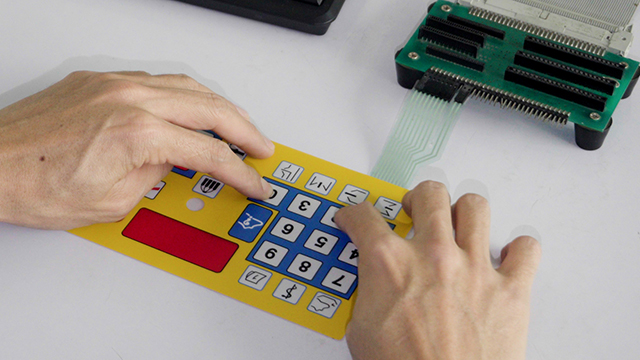
Human-Machine Interfaces (HMIs) are evolving beyond simple switches. OEM purchasers and system architects must understand upcoming paradigm shifts in tactile sensing, embedded backlighting, and smart surfaces to future-proof their hardware.
Moving from 2.5D flat stacks to 3D formed structural plastic parts. IME combines printed conductive traces with thermoformed injection-molded resins, eliminating mechanical sub-assemblies entirely.
Modern buyers demand flush wipe-clean aesthetics combined with physical tactile confirmation. Hybrid switches integrate proximity capacitive sliders with secondary mechanical metal dome confirmations.
Traditional discrete LED 'hot-spots' are obsolete. Contemporary panels integrate side-firing ultra-compact LEDs into micro-etched Light Guide Films (LGF), achieving completely uniform backlighting at 0.25mm thickness.
Post-pandemic medical procurement protocols require graphic overlays impregnated with silver-ion antimicrobial agents (such as Autotex AM) capable of actively inhibiting 99.9% of pathogen growth.
Direct factory sourcing in China offers significant cost and scale benefits, but selecting the wrong supplier risks silver migration, peeling adhesives, and inconsistent key click feel. Use this checklist during your supplier audit.
Ensure the factory can prove genuine supply chains for 3M adhesives (especially 3M 467MP, 468MP, 9448A) and films from Sabic or MacDermid. Counterfeit adhesives lead to early panel delamination under extreme summer heat or industrial chemical exposure.
Tier-1 manufacturers produce printing screens, steel rule cutting dies, and embossing tooling directly in-house. Subcontracting tooling introduces 7-10 day delays on engineering change orders (ECOs) and compromises dimensional tolerances.
Verify that the factory owns calibrated in-house testing equipment: Taber abrasion testers, automated key actuation cyclers, high/low-temperature environmental chambers (-40°C to +85°C), and ASTM cross-hatch ink adhesion testing rigs.
Direct answers to the most common technical, logistical, and commercial inquiries from overseas procurement specialists.
We require mechanical CAD drawings (DXF, DWG, or STEP) specifying external dimensions, cutout locations, embossing borders, and connector pinouts. For the graphic overlay, vector artwork (Adobe Illustrator .AI or vector PDF) with defined Pantone (PMS) or RAL color codes ensures exact color matching.
We engineer a continuous perimeter adhesive gasket completely enclosing the active switch cavities. The tail exit is channeled internally or sealed with silicone potting to prevent capillary liquid ingress. Additionally, waterproof breathable acoustic/pressure vents are integrated when air pressure equalization is needed.
Silver ink on PET is ideal for cost-sensitive standard applications with trace pitches ≥ 0.8mm. Choose Flexible Printed Circuit (FPC) copper if your design requires ultra-compact connectors (0.5mm ZIF), dense trace routing, reflow-soldered micro-controllers/sensors, or loop resistance under 5 ohms.
Prototype tooling and physical samples are completed within 7 to 10 working days. Mass production steel dies and production verification take 12 to 18 working days. Standard tooling investments range from $180 to $650 depending on complexity, embossing requirements, and hard tooling steel.
Yes. We incorporate full-coverage aluminum foil, printed carbon/silver grid matrices, or ITO (Indium Tin Oxide) conductive layers grounded directly to the chassis ground pin via the flex tail. This protects sensitive underlying logic boards from electrostatic discharge up to 15kV.
For industrial or medical applications operated with thick gloves, we recommend four-legged stainless steel metal domes with actuation forces between 350g and 500g, paired with a distinct rim or pillow embossed graphic overlay to provide positive tactile finger indexing.
Send us your technical specification, 2D/3D CAD drawing, or graphic layout. Our engineering team in Dongguan will return a comprehensive DFM manufacturability analysis and competitive factory quotation within 2 hours.
Inquire Now