IP67 Medical
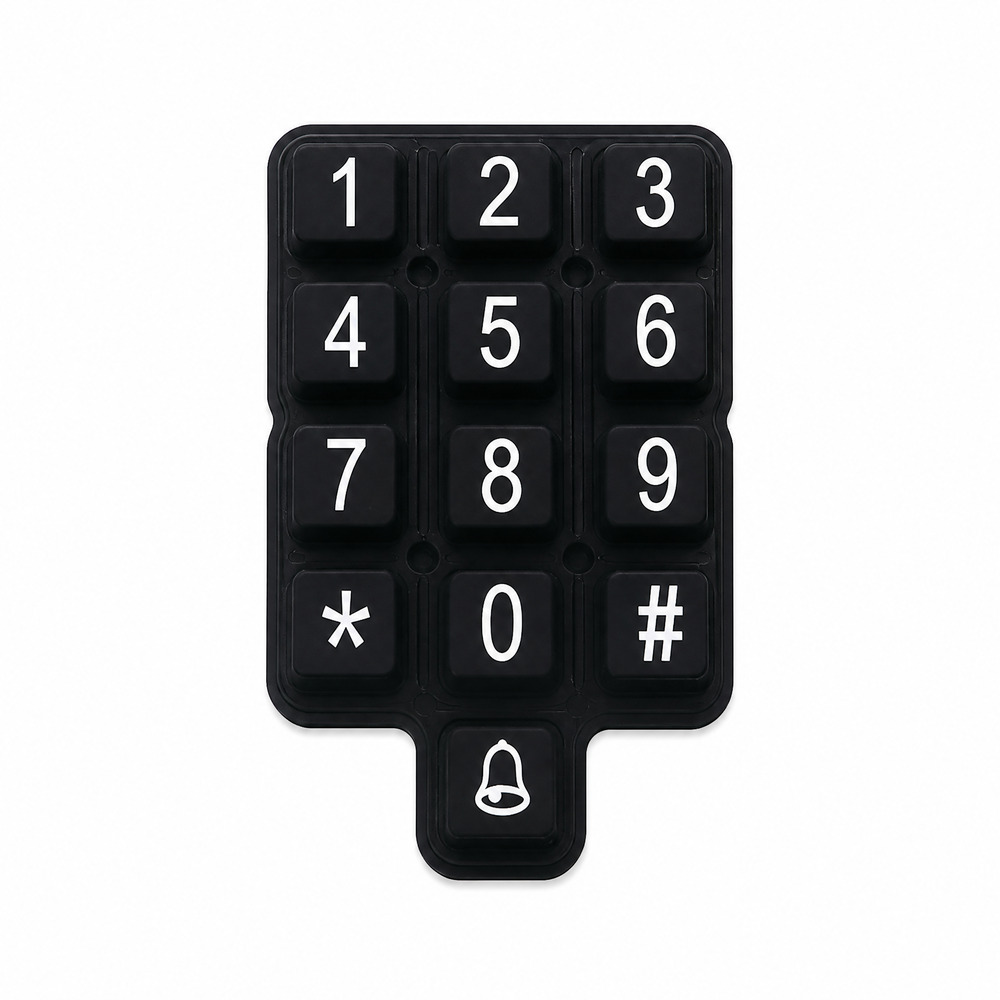
Waterproof Silicone Rubber Keypad for Medical Equipment Custom Solutions
- Biocompatible medical-grade silicone
- Hermetic perimeter seal (IP67)
- Hospital bleach & alcohol resistant
 EN
 DE
 FR
 ES
 RU
 JA
Manufactured to European CE Directives (EMC, LVD, RoHS) and international ingress standards. Explore proven configurations configured for surgical units, rugged industrial PLCs, fuel telemetry, and tactile embedded remotes.
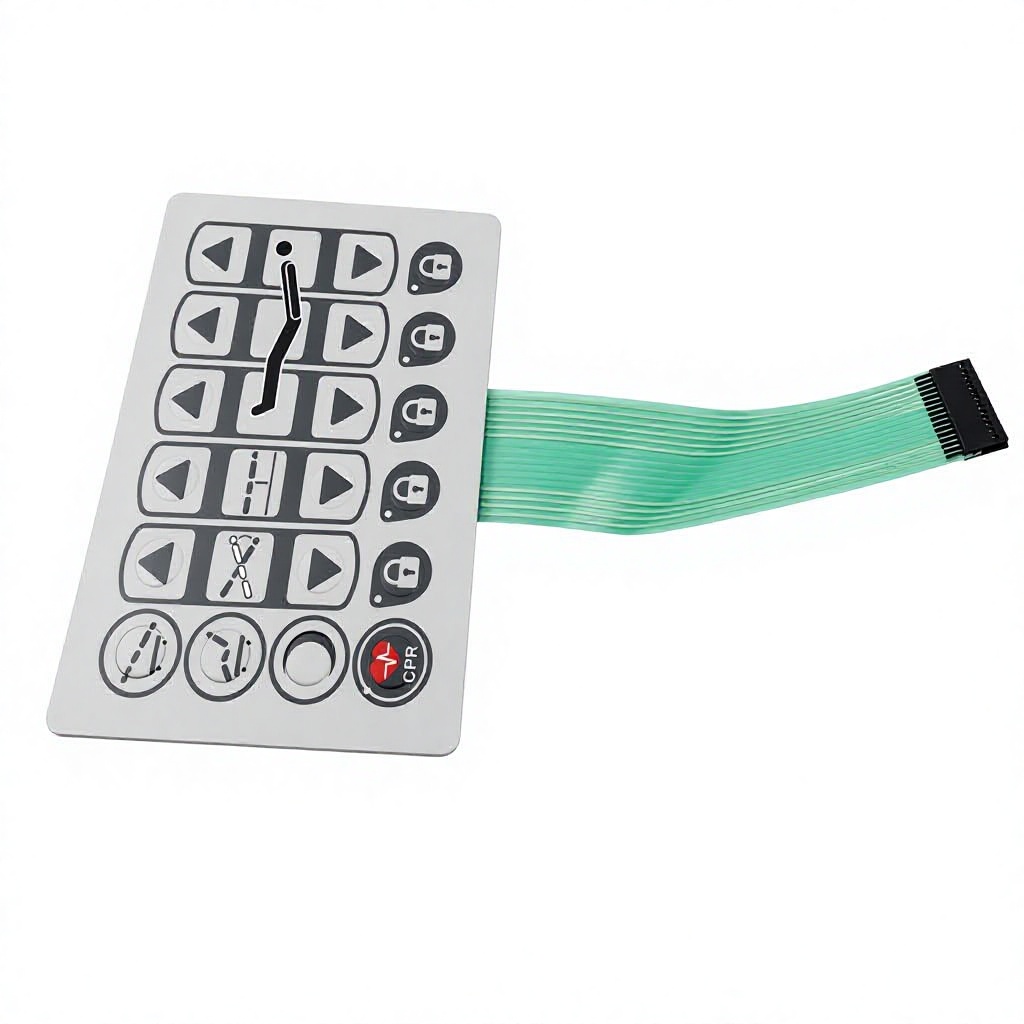
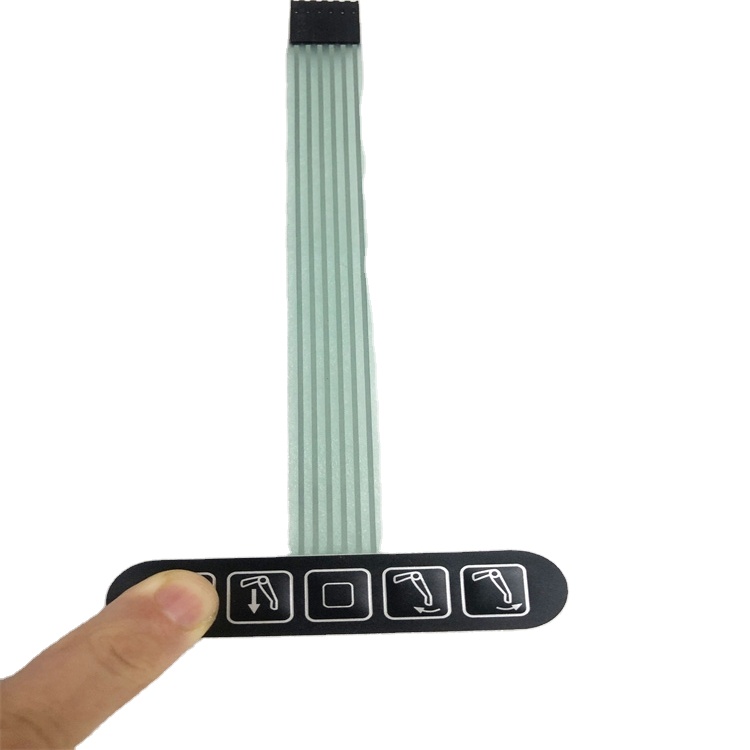
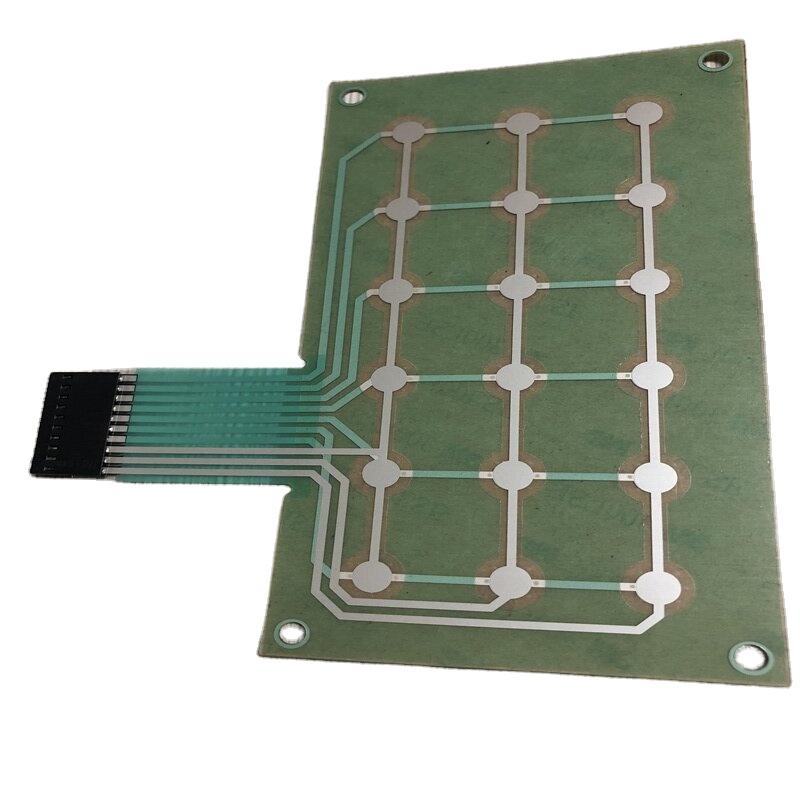
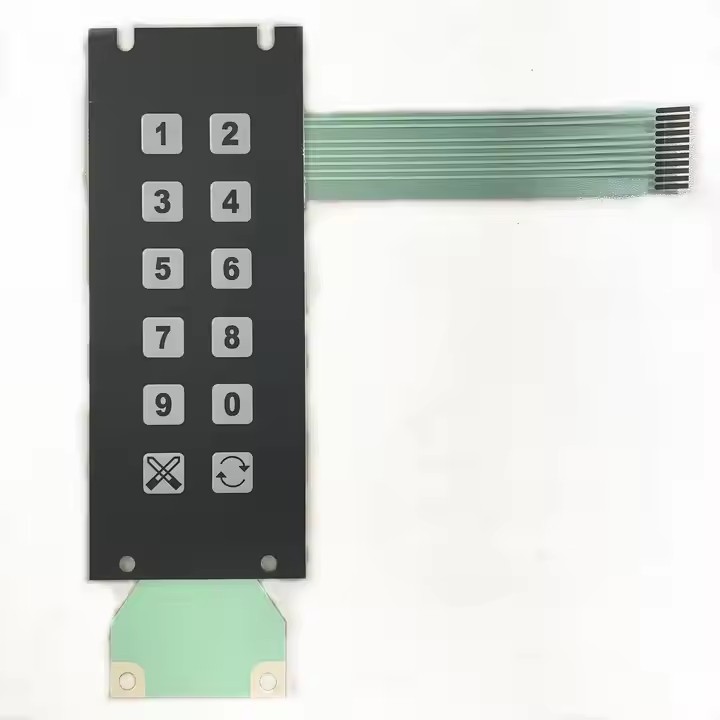
A deep technical breakdown of multi-layer hermetic sealing, dynamic ingress dissipation, and compliance engineering across demanding operating environments.
In mission-critical user interfaces, environmental ingress is the single greatest cause of field failure. A true CE certified sealed membrane keyboard requires an uninterrupted perimeter defense against high-pressure liquid impingement, sub-micron particulates, and corrosive chemical vapors.
Unlike unsealed consumer keypads that rely merely on mechanical compression, Ravo's industrial-grade sealed membrane assemblies incorporate micro-channeled perimeter gaskets precision die-cut from 3M 200MP, 300LSE, or VHB acrylic adhesive systems. These continuous perimeter boundaries prevent capillary fluid migration even when submerged at depths exceeding 1 meter (IP67/IP68 rating according to IEC 60529 standards).
Critical DFM Insight: To maintain tactile consistency across altitude and temperature shifts without allowing moisture ingress, Ravo employs semi-permeable ePTFE (expanded polytetrafluoroethylene) venting membranes integrated within internal venting channels, equalizing atmospheric pressure while remaining completely impervious to water and contaminants.
Selecting the optimal substrate-circuit stack is fundamental to balancing operational longevity, tactile response, and chemical resilience. Review the empirical performance parameters below:
| Stack Layer / Metric | Standard Screen-Printed PET | Polyimide Flex (FPC) Copper | Rigid FR-4 PCB Backed | Molded Silicone Rubber Hybrid |
|---|---|---|---|---|
| Ingress Rating Ceiling | IP65 – IP67 | IP67 – IP68 | IP66 – IP67 | IP67 – IP68 Hermetic |
| Actuation Life (MTBF) | 1,000,000 to 3,000,000 cycles | 5,000,000+ cycles | 5,000,000+ cycles | 2,000,000 to 5,000,000 cycles |
| Chemical & Solvent Barrier | Moderate (Autotype V200) | High (Encapsulated Polyimide) | High (Solder Mask + Conformal) | Exceptional (Fluorosilicone optional) |
| Operating Temp Range | -20°C to +70°C | -40°C to +105°C | -40°C to +125°C | -45°C to +150°C |
| Contact Trace Resistance | < 100 Ω (Silver Migration Protected) | < 1 Ω (Direct Pure Copper) | < 0.5 Ω (Plated Au/Ni) | < 150 Ω (Conductive Carbon Pill) |
| Component Integration | Conductive Epoxy SMD LEDs | Reflow Soldered Active ICs | Full SMT, Display Panels, Studs | Backlit Light Guides, Windows |
Global procurement teams in medical, avionics, defense, and industrial automation are transitioning away from commodity parts toward intelligent, multi-technology interface modules.
Procurement directors are increasingly specifying "hybrid keyboards" that combine completely wipeable, zero-crevice capacitive touch glass or polyester surfaces with localized tactile haptics or underlying metal snap domes. This resolves the cleanability requirements in medical isolation wards while eliminating blind user input error.
Following post-pandemic healthcare standards, global hospital procurement mandates that front-panel interfaces resist non-stop wipe-downs with accelerated quaternary ammonium compounds, isopropyl alcohol, and sodium hypochlorite without crazing, yellowing, or delaminating. Antimicrobial ion-infused texturing (ISO 22196) has become a primary sourcing specification.
Tier-1 OEMs now avoid sourcing individual membrane switches, sheet-metal brackets, displays, and wiring harnesses separately. Buyers prioritize single-source partners like Ravo capable of supplying completely assembled, tested HMI modules—integrating CNC aluminum faceplates, daughterboards, TFT display bonding, and custom cable exits.
From early mechanical contacts to micro-engineered photonic light guides and integrated thin-film force sensors.
Traditional discrete LEDs often cause hot-spots and uneven intensity across key legends. Modern designs integrate 0.1mm micro-etched Light Guide Films (LGF) powered by edge-mounted high-efficiency side-view SMD LEDs. This technology achieves uniform photometric diffusion at less than 15% of the power consumption of electroluminescent (EL) backlights.
In high-ambient light environments, marine displays, and outdoor industrial kiosks, reflection between layers degrades readability. Advancements in optically clear silicone adhesives (LOCA/OCA) allow direct bubble-free lamination of polyester or polycarbonate membrane graphic overlays directly to capacitive glass and active LCD/OLED panels.
By screen-printing quantum tunneling dynamic carbon inks in conjunction with interdigitated silver fingers, Ravo engineers integrated analog pressure sensing directly within keyboard matrices. Applications range from automotive occupant detection to industrial variable-speed motor throttling through direct key press pressure variation.
Dongguan Ravo Electronics Co., Ltd. delivers over 20 years of hands-on human-machine interface manufacturing capability from our audited Fenggang Town facility.
Our engineering division validates all products against the EU EMC Directive 2014/30/EU (immunity to high-voltage electrostatic discharge and RF interference), the Low Voltage Directive 2014/35/EU, and RoHS Directive 2011/65/EU. Complete declaration files, full-thickness material breakdowns, and XRF test reports are furnished with first-article inspections.
Our on-site engineering team conducts Design for Manufacturability (DFM) reviews within ≤2 hours during Asia business hours. We review key pitch, tail exit stress relief, dome venting corridors, and adhesive surface energy compatibility. Prototyping begins from 1 piece with short 7 to 12 day sample turnarounds.
Every switch matrix leaving our plant undergoes automated computer-controlled continuity, short, resistance, and capacitance tests. In-house verification laboratories perform ASTM F1578 dome snap-ratio actuation life testing, -40°C to +85°C thermal cycling, and IPX7 submersion verification tanks.
Direct technical answers to common questions raised by quality assurance engineers and international purchasing directors.
Passive membrane switches fall under CE requirements whenever they interface with voltage-carrying circuits (Low Voltage Directive 2014/35/EU) or function in sensitive electronic assemblies requiring electromagnetic compatibility (EMC Directive 2014/30/EU). Ravo ensures compliance by using 100% RoHS/REACH certified non-toxic films, formulating fire-retardant adhesive bonds (UL94 VTM-2 or V-0 rated), and integrating full-coverage printed carbon/silver grid Faraday shields that attenuate ESD discharges up to 25kV.
Silver migration occurs when moisture combines with DC voltage potential across adjacent silver ink conductors, causing dendritic crystal growth and short-circuits. Ravo prevents this through three standard engineering barriers: (1) Applying continuous carbon paste over-coatings over all silver circuitry; (2) Maintaining minimum trace spacing design rules (>0.5mm) based on voltage bias; and (3) Complete hermetic perimeter gasket encapsulation isolating traces from ambient humidity.
The flex tail exit is inherently the most vulnerable area in any sealed membrane keyboard. Ravo prevents ingress failures through several proven tail exit techniques: (1) Designing continuous rear-exit tails isolated within the perimeter adhesive boundaries; (2) Applying UV-curable dielectric epoxy dams at tail junctions; or (3) Transitioning to molded silicone boots or ultrasonic welded hermetic bezels that clamp around the tail with IP67/IP68 gasket compression.
The adhesive choice must match the surface energy of your substrate. For high-surface-energy (HSE) metals like smooth aluminum, stainless steel, and polycarbonate, 3M 467MP (2 mil) or 3M 468MP (5 mil) provides long-term bonding and thermal stability up to 200°C. For low-surface-energy (LSE) plastics such as textured ABS, polypropylene, powder-coated casings, or nylon, Ravo specifies 3M 300LSE or 3M 9448A high-tack modified acrylics to prevent edge peeling.
We configure three primary actuations: (1) Stainless steel metal domes (four-leg, round, or oblong), delivering a sharp audible snap with actuation forces between 180g and 450g and an MTBF exceeding 1,000,000 to 5,000,000 operations; (2) Thermoformed polydomes embossed directly into the PET film for a quieter, cost-effective snap (1,000,000 cycles); and (3) Non-tactile flat switches (5,000,000+ cycles) ideal for continuous touch or gloved swipe operation with visual display feedback.
To support agile product development, Ravo offers rapid prototyping with an MOQ starting from 1 to 10 pieces. After drawing and DFM sign-off, functional sample keyboards ship within 7 to 14 working days. Mass volume orders typically maintain a 2 to 3 week turnaround, backed by inventory safety-stock agreements for ongoing OEM series production.
Send your CAD drawings, 2D vector layouts, or schematic specifications to our senior DFM engineering team. We guarantee a detailed engineering review and comprehensive quotation within 2 business hours.
