EN
 DE
 FR
 ES
 RU
 JA EN DE FR ES RU JA
Precision-engineered human-machine interface (HMI) keypads designed for long actuation lifespans, extreme weather resilience, and seamless integration.
How advanced material science, stainless steel dome physics, and environmental sealing converge to produce high-reliability control interfaces for New Zealand's harsh operating conditions.
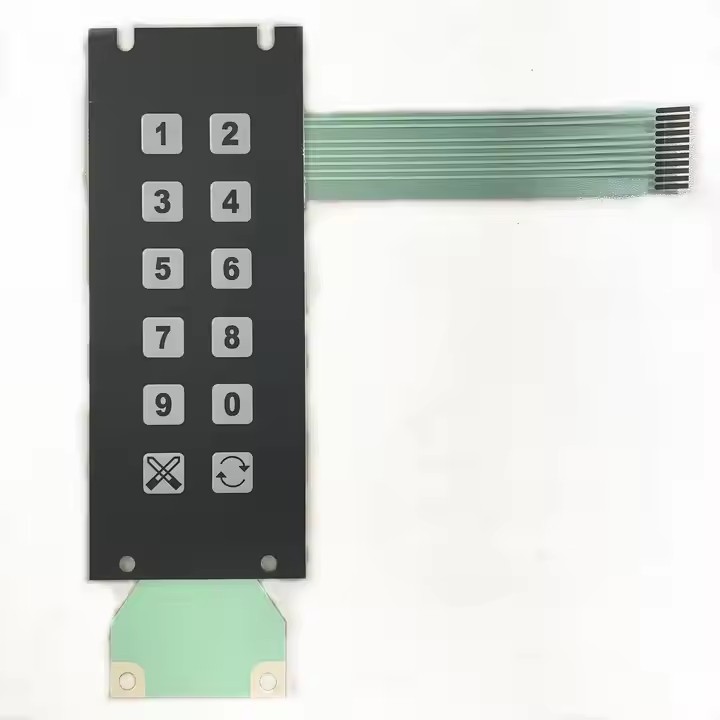
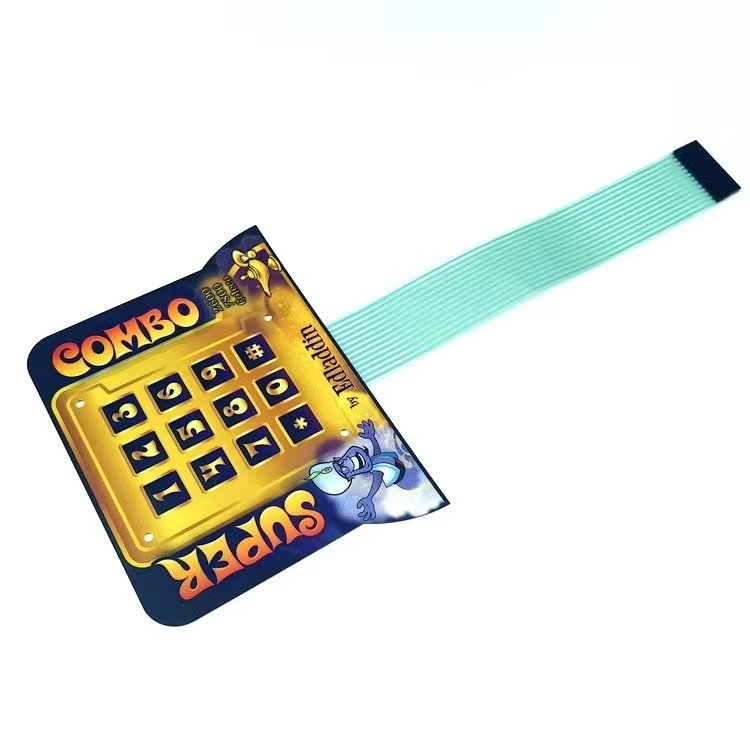
In electronic engineering, human factor ergonomics play a vital role in preventing operational errors, particularly in outdoor, industrial, or emergency equipment. A Tactile Metal Dome Membrane Switch integrates stainless steel snap domes (typically 304 or 316 grade) beneath a graphic overlay layer. When depressed, the metal dome collapses rapidly, bridging the contact gap on the silver-ink or copper-plated circuit layer below, completing the electrical loop.
The key metric governing this tactile response is the Snap Ratio (Click Ratio), expressed as:
Snap Ratio Formula: Snap Ratio (%) = [(F1 - F2) / F1] × 100
Where F1 is the peak actuation force (trip force) and F2 is the return force (contact force).
For New Zealand industrial equipment operating in cold outdoor temperatures (such as South Island forestry machinery or dairy cold-chain infrastructure), maintaining an optimal snap ratio between 40% and 65% ensures that operators wearing heavy work gloves receive clear, unambiguous physical confirmation of every keystroke without experiencing hand fatigue.
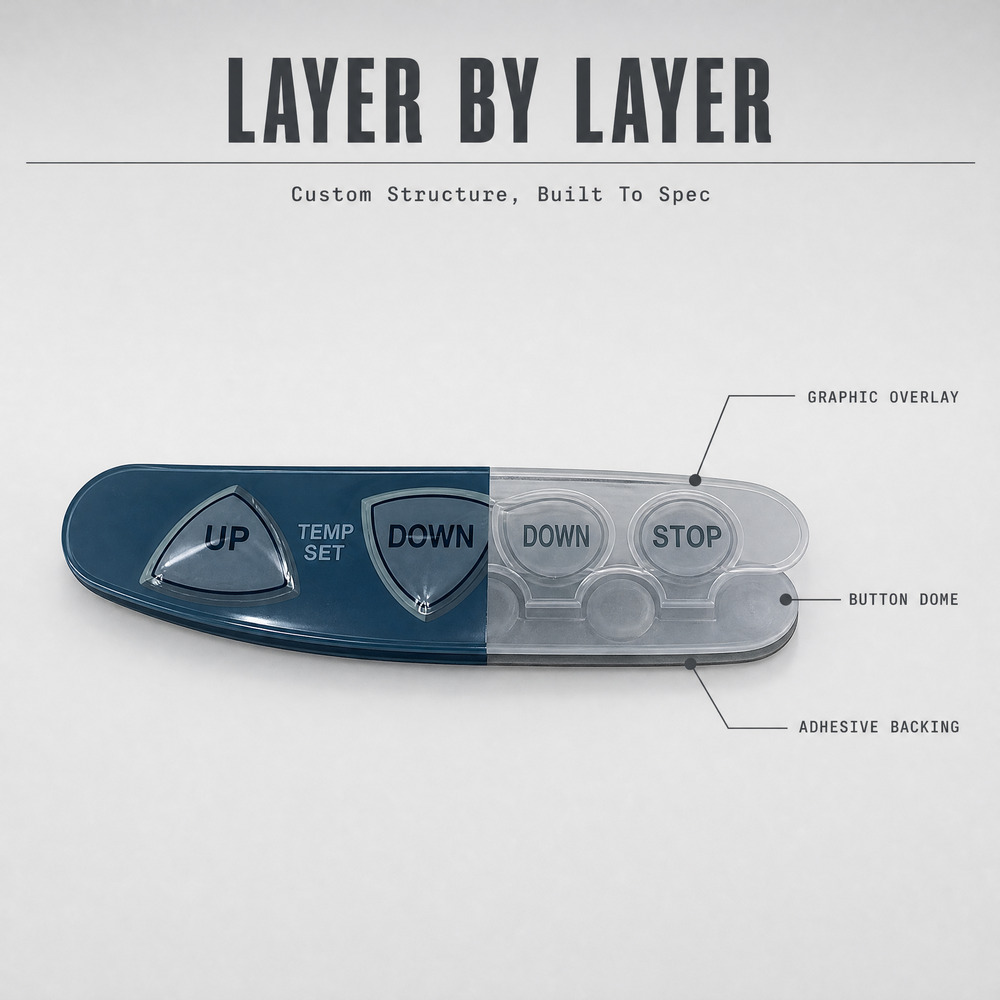
A multi-layered engineered assembly guarantees long-term conductivity, zero moisture ingress, and aesthetic brilliance. Dongguan Ravo Electronics custom-engineers each layer based on project requirements:
| Layer Component | Material Specification Options | Engineering Purpose & Performance Characteristic |
|---|---|---|
| 1. Graphic Overlay | Autotex XE Polyester (PET), Bayer Polycarbonate (PC) | Reverse silk-screen printed for permanent chemical, UV, and scratch resistance. Textured finishes eliminate glare. |
| 2. Overlay Adhesive | 3M 467MP / 3M 468MP High-Performance Acrylic | Bonds overlay to spacer layer; creates a liquid-tight seal resisting jet washdowns and petroleum exposure. |
| 3. Dome Retainer Layer | 0.075mm - 0.125mm Clear Mylar / Polyester Film | Precisely anchors stainless steel metal domes in position, preventing dome migration under intense vibration. |
| 4. Tactile Metal Domes | SUS304 Stainless Steel (Four-leg, Triangle, Round) | Delivers crisp tactile snap. Optional gold or nickel plating reduces contact resistance to <1 ohm. |
| 5. Circuit Layer | Silver-Flex Conductive Ink on PET or Flexible Polyimide FPC | Transmits electrical signals with micro-thin trace lines. FPC circuits allow pitch density down to 0.5mm. |
| 6. Rear Mounting Adhesive | 3M 9448A / 3M VHB Heavy-Duty Mounting Tape | Secures the completed switch module onto metal enclosures, powder-coated housings, or ABS plastic cases. |
From Canterbury's high-tech agritech installations to Auckland's maritime electronics hubs, our tactile switches are purpose-built for the unique microclimates and rugged demands of the Kiwi market.
New Zealand's dairy and agriculture industries demand human-machine interfaces that can endure harsh farm environments. In regions like Waikato and Canterbury, automated milking parlors, shed climate systems, and electronic irrigation controllers face constant exposure to water washdowns, mud, and agricultural chemicals. Our IP67-sealed tactile membrane keypads feature UV-stable Autotex XE polyester graphic overlays, preventing yellowing and cracking under high UV index conditions while providing reliable 1-million-cycle switch performance.
As a leading maritime nation, Auckland ('City of Sails') and Nelson harbor thriving marine engineering sectors. Electronic winch controllers, fish finders, and boat helm control panels require 100% resistance to salt spray corrosion and humidity. Ravo supplies custom silicone rubber membrane switches paired with gold-plated stainless steel domes and waterproof 3M adhesives, delivering robust seal protection (up to IP68) against ocean brine immersion.
Wellington and Auckland healthtech innovators manufacture handheld medical diagnostic tools and patient monitors. Hygiene, wipe-clean surfaces, and light-touch responsiveness are critical. Our antimicrobial graphic overlays paired with LED-backlit tactile domes allow nurses and doctors to operate panels smoothly, withstanding rigorous sterilization using hospital-grade alcohol and chemical disinfectants.
Heavy machinery operating in Rotorua logging forests or West Coast mining zones undergoes extreme mechanical shock and vibration. Conventional mechanical switches often fail due to dust intrusion or broken plastic levers. Ravo’s embossed metal dome membrane keyboards with rigid PCB backers offer self-supporting structural strength, dust-proof enclosures, and distinct physical key feel for operators wearing gloves.
With New Zealand's rapid transition toward green energy, public EV charging networks and outdoor ticketing dispensers require weather-resistant, vandalism-tolerant control interfaces. Non-tactile or embossed tactile membrane panels engineered with polycarbonate hard-coats resist impact, solar heat build-up, and rain ingress, ensuring 24/7 uptime across public infrastructure.
Key design considerations for electronic product designers exporting to or manufacturing within New Zealand.
New Zealand experiences intensely high peak UV levels during summer months. Standard polycarbonate front overlays degrade, yellow, and embrittle rapidly when installed outdoors. We explicitly specify Autotex XE UV-resistant polyester and outdoor-rated UV inks, tested under ASTM G154 accelerated weathering standards to guarantee 10+ years of outdoor colorfastness.
New Zealand importers prioritize environmental sustainability and non-toxic materials. Dongguan Ravo Electronics certifies that all silver pastes, PET films, copper FPCs, stainless steel domes, and 3M adhesives fully comply with EU RoHS 3 (Directive 2015/863) and REACH regulations, simplifying smooth clearance with New Zealand Customs.
Dry winter indoor environments or static-prone agricultural equipment can introduce Electrostatic Discharge (ESD) up to 15kV. Ravo incorporates selective aluminum foil or printed carbon grid shielding layers within the membrane switch matrix, routing static charges safely to ground before reaching sensitive microcontrollers.
Established in 2003, Ravo operates a vertically integrated 12,000m² manufacturing facility in Dongguan, China, delivering end-to-end HMI engineering for global equipment manufacturers.
Our experienced engineering team evaluates 2D/3D CAD drawings (DXF, DWG, STEP, AI, PDF) and returns comprehensive Design for Manufacturability (DFM) reviews within less than 2 hours during business hours.
We empower Kiwi startups and established R&D teams by supporting rapid prototyping from as low as 1 to 5 pieces, enabling fast physical testing before committing to high-volume production tooling.
From screen-making, CNC laser cutting, and embossing dies to silicone compression molding, our internal toolroom drastically reduces lead times and protects your proprietary design IP.
Every switch batch undergoes 100% automated optical inspection (AOI), electrical continuity & resistance testing, actuation force verification, and micro-gap short circuit detection prior to export packaging.
Everything you need to know about custom tooling, lead times, shipping options to Auckland/Wellington, and material specifications.
Our standard prototype lead time is 7 to 10 working days following drawing sign-off and color matching. For mass production orders (500–10,000+ units), production typically takes 12 to 18 days. Express air freight via DHL, FedEx, or UPS delivers directly to Auckland, Wellington, or Christchurch in 3 to 5 business days. For large production volumes, sea freight via Ports of Auckland or Tauranga is available to optimize logistics costs.
We engineer a continuous perimeter seal utilizing high-tack 3M 467MP or 3M 468MP acrylic adhesive rings surrounding the active circuit matrix. Additionally, we implement sealed tail-exit geometries (or FPC polyimide tails) that prevent moisture from wicking along trace lines into the control box, ensuring certified IP65, IP67, or IP68 protection against pressure washing and salt spray.
Yes. Every parameter is 100% customizable. You can specify metal dome diameters (from 6mm to 20mm), actuation forces (160g to 500g), and key embossing styles (pillow embossing, rim embossing, dome embossing). Color matching is conducted using the Pantone Matching System (PMS) or RAL color standards, with spectro-photometer color verification.
We support a broad range of standard industrial connectors, including 2.54mm pitch female crimp housings (Nicomatic, FCI), 1.0mm or 0.5mm pitch ZIF flex tails, direct soldering pin headers, or surface-mounted connectors on rigid PCB backplanes.
With every shipment, we can provide a Certificate of Conformance (CoC), RoHS 3 material declarations, REACH compliance statements, 100% electrical test reports, and First Article Inspection (FAI) reports upon request.
A Silver-Flex switch utilizes conductive silver ink screen-printed onto polyester (PET) film. It is highly cost-effective and suitable for most standard keypads. An FPC switch uses a polyimide substrate with chemically etched copper traces. FPC offers superior tolerance to high ambient temperatures, finer line spacing, lower trace resistance, and enables direct surface-mount soldering of SMD LEDs and active IC components.
Send your CAD vector files (DXF, DWG, AI, PDF) or prototype concepts to our senior engineering team today. Get an expert DFM feedback report and a competitive quote within 2 hours.
Get a Quote