EN
 DE
 FR
 ES
 RU
 JA EN DE FR ES RU JA
Explore our export-grade Human-Machine Interface assemblies engineered for high-cycle reliability, ingress protection, and seamless system integration. Every unit is custom-manufactured in our ISO 9001 certified facility to meet your exact mechanical, electrical, and environmental specifications.
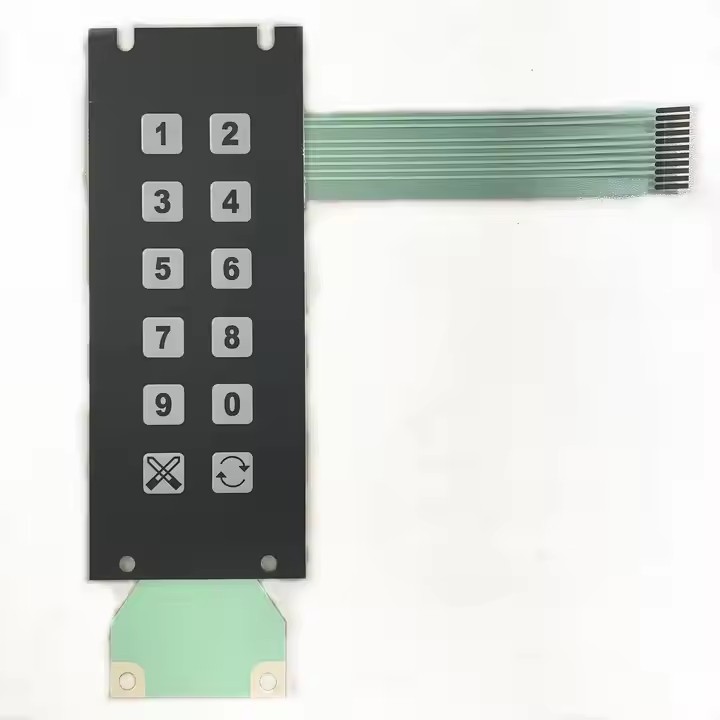
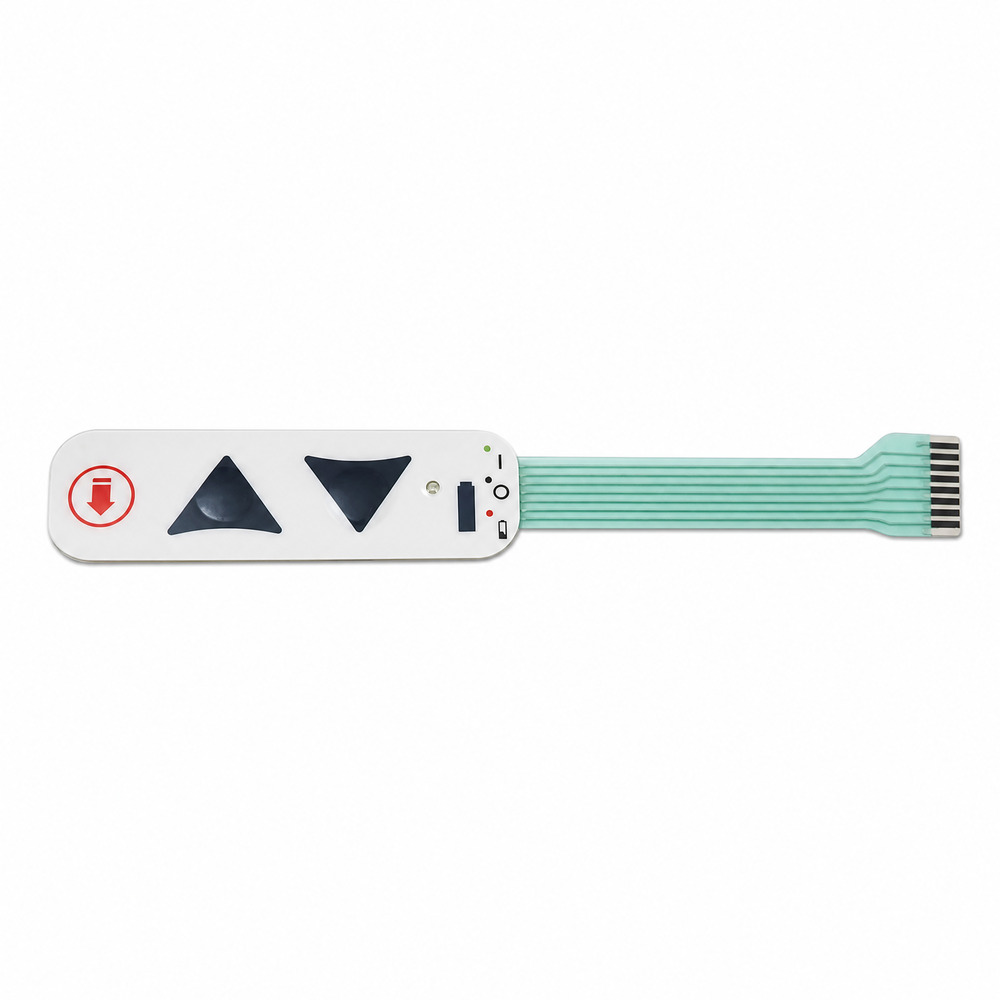
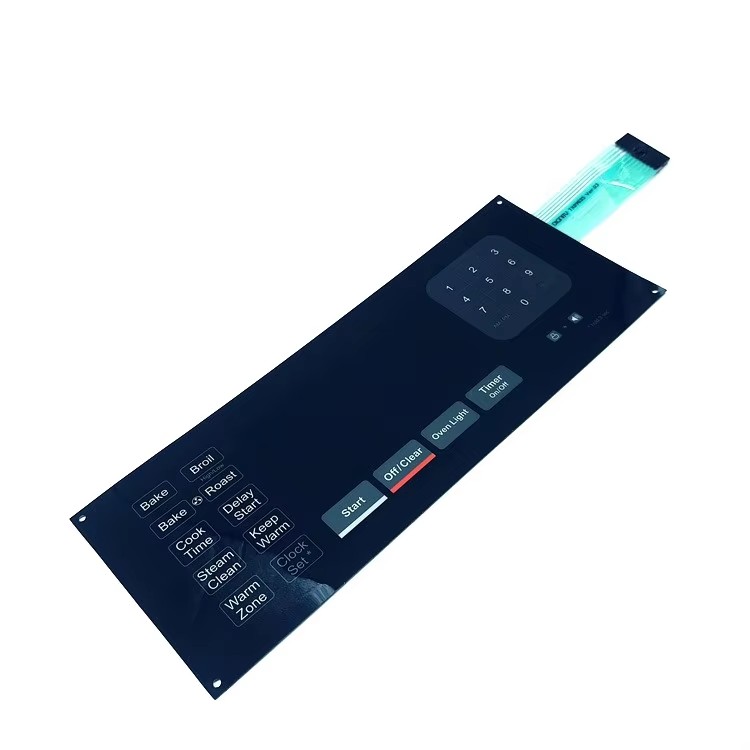
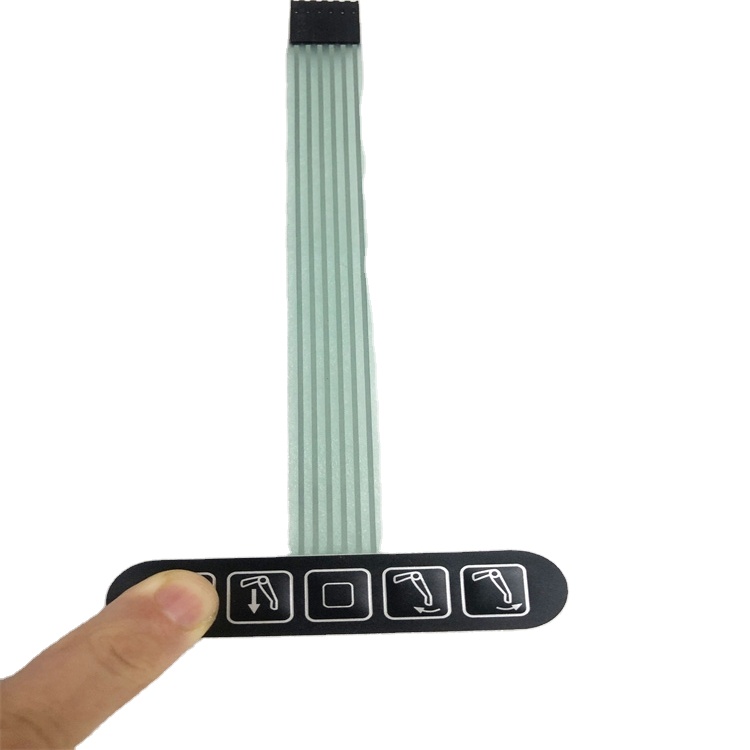
In modern industrial automation, medical instrument design, marine power electronics, and outdoor energy infrastructure, the Human-Machine Interface (HMI) serves as the critical nexus between operator input and digital execution. Traditional mechanical push-buttons and non-enclosed switch assemblies suffer from rapid mechanical fatigue, seal degradation, and susceptibility to moisture ingress, atmospheric oxidation, and chemical exposure. Dongguan Ravo Electronics Co., Ltd. addresses these engineering bottlenecks by manufacturing high-precision, multi-layer PCB-backed membrane switches and flexible printed circuit (FPC) keypad assemblies engineered to withstand rigorous operational demands.
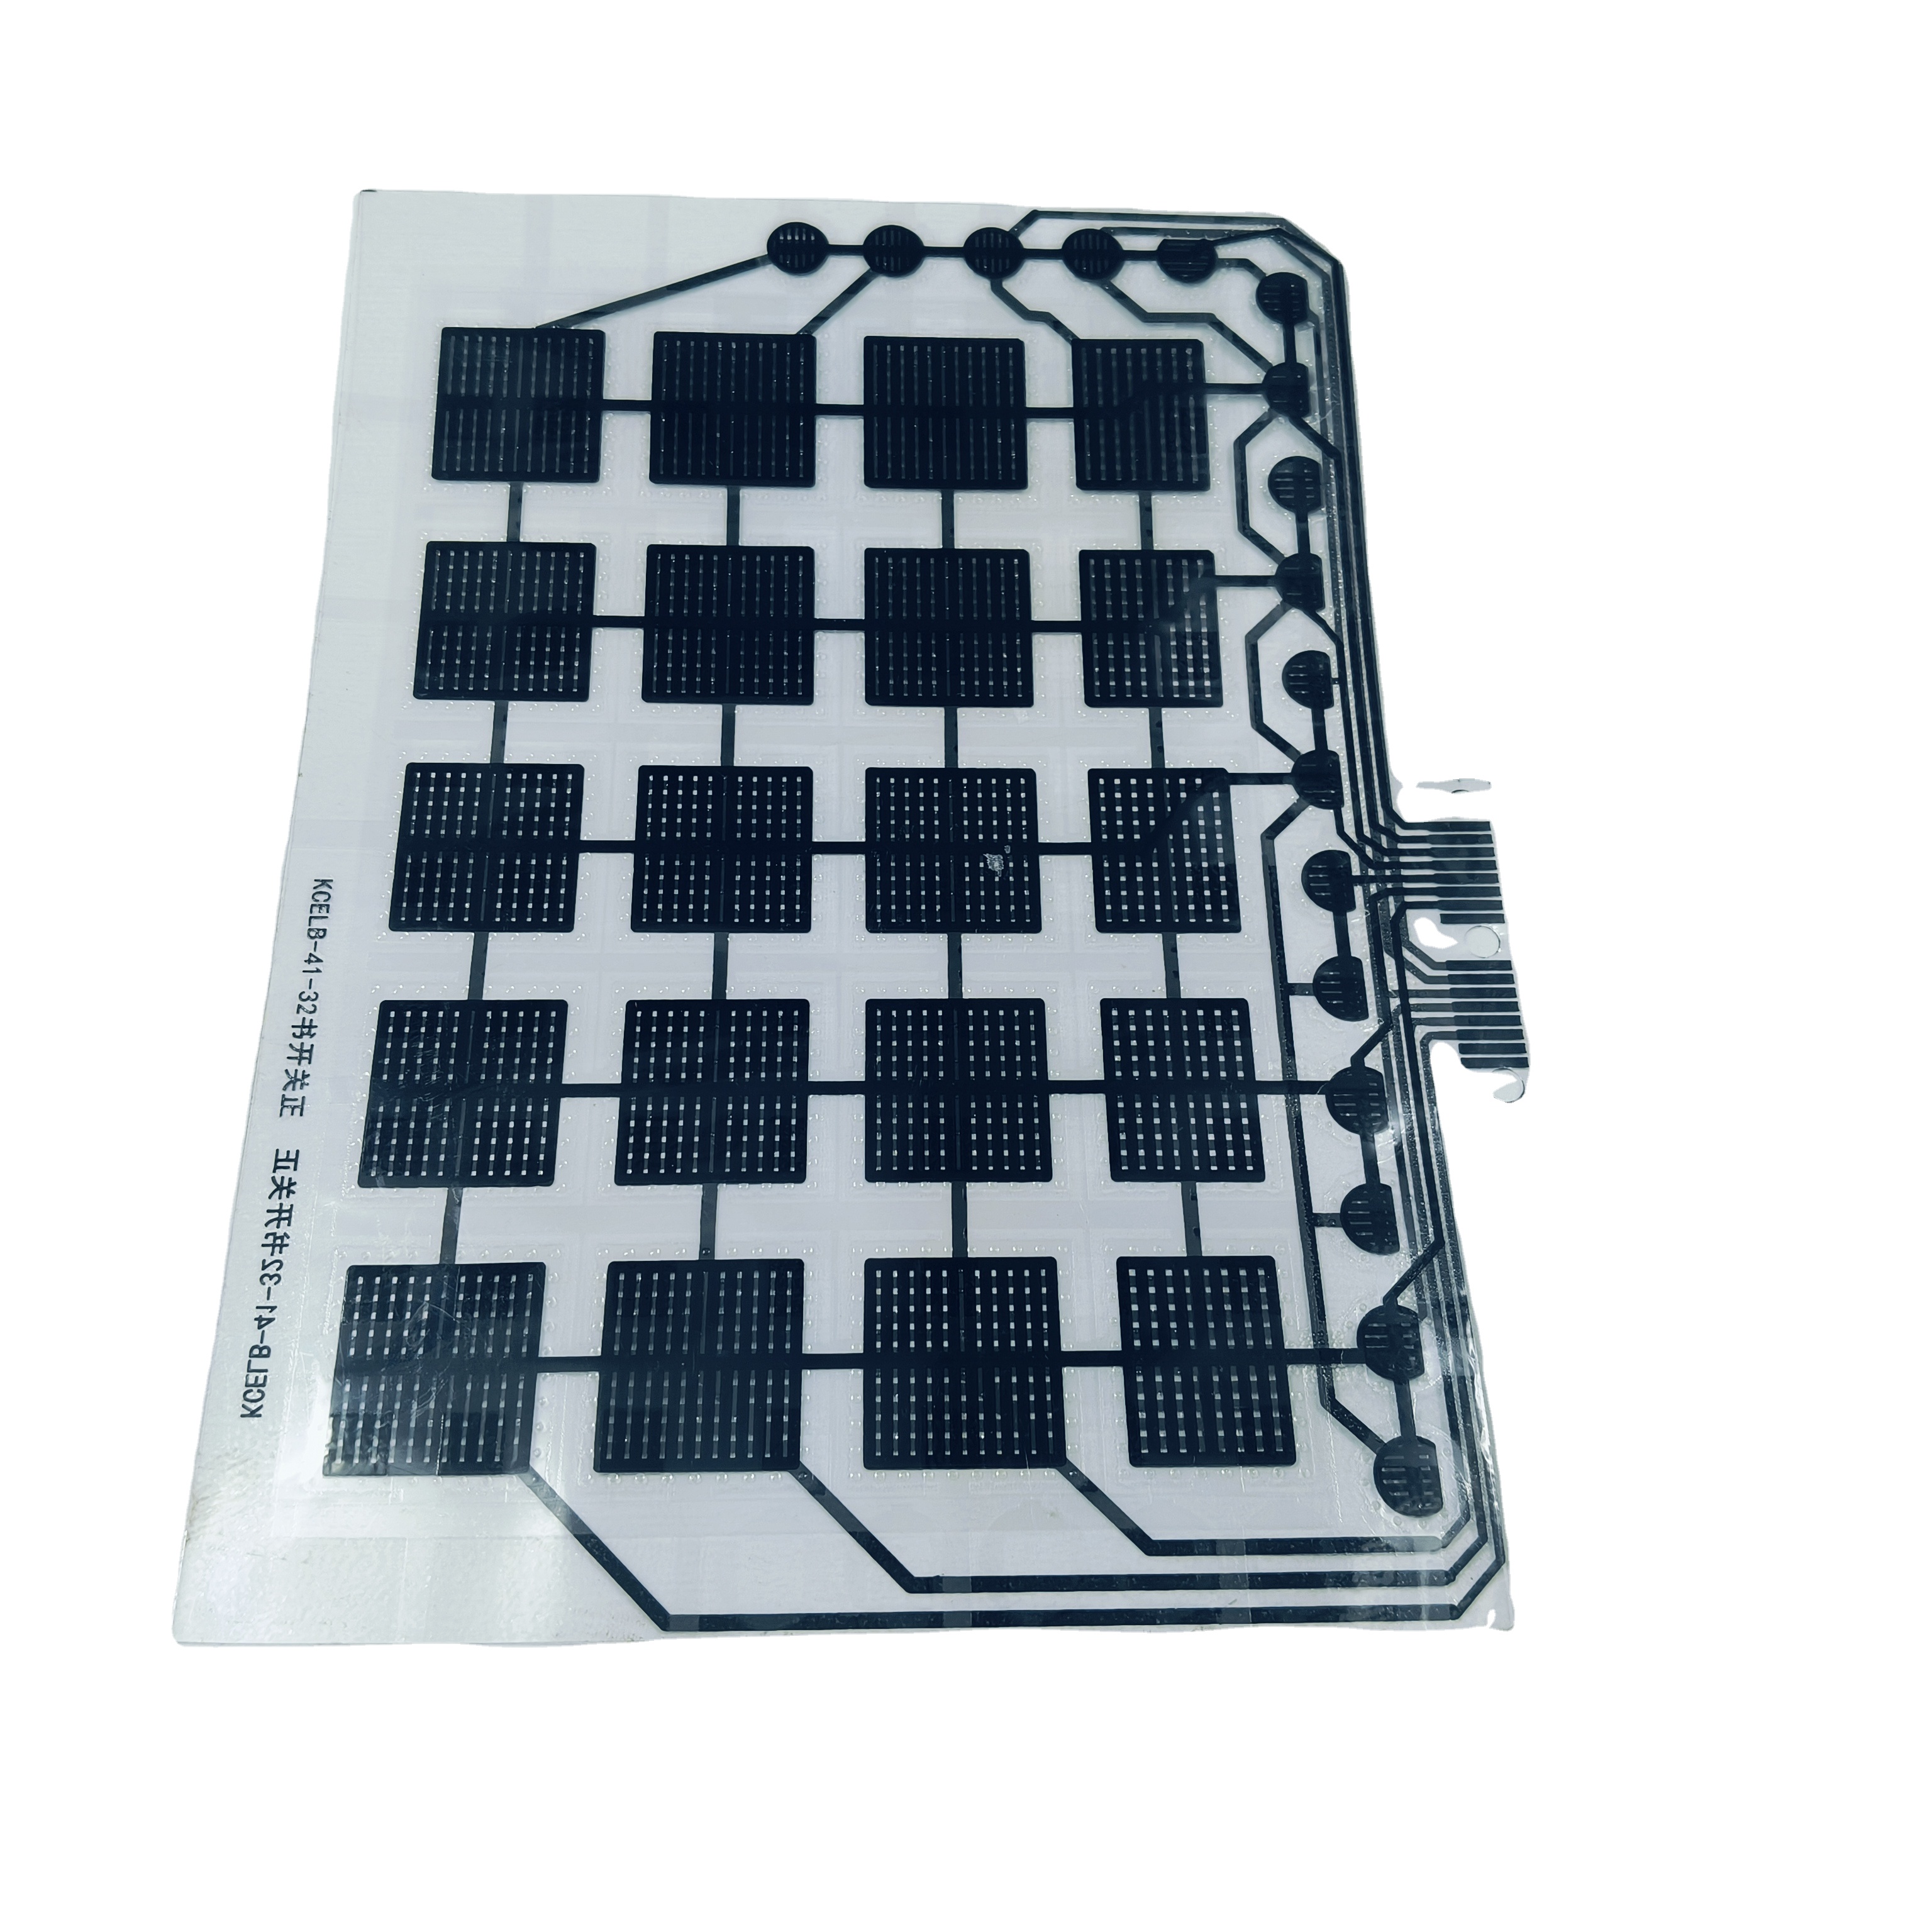
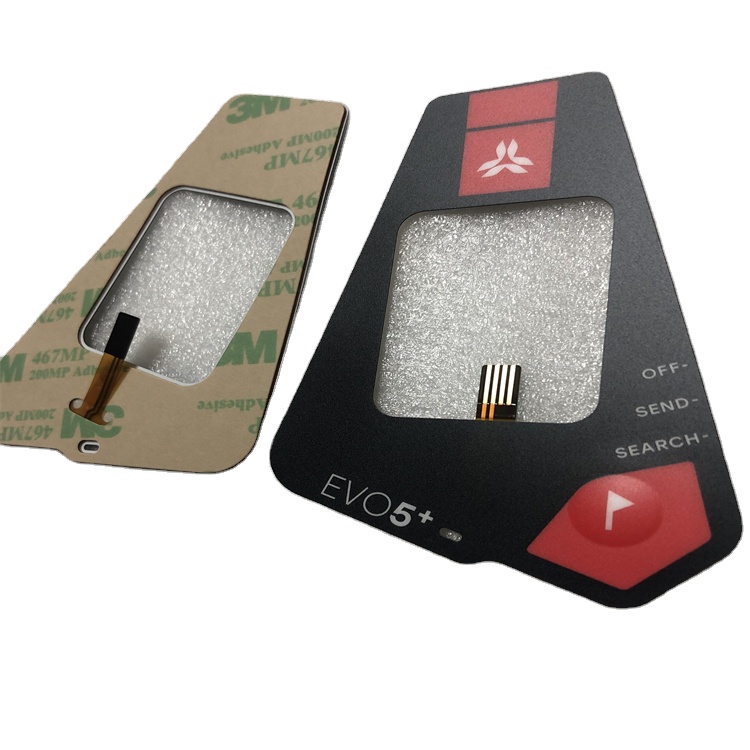
By replacing standard silver-printed PET flexible traces with rigid FR-4 printed circuit board (PCB) backer structures or polyimide FPC layers, our design engineers integrate active surface-mount devices (SMD LEDs, resistors, capacitors, microcontrollers, and board-to-board connectors) directly into the switch stack. This structural integration eliminates separate wire harnesses, reduces assembly depth, enhances signal integrity against Electrostatic Discharge (ESD) and Electromagnetic Interference (EMI), and delivers an operating lifespan exceeding 1,000,000 to 5,000,000 actuations.
A high-performance PCB membrane switch manufactured by Ravo Electronics consists of a vertically laminated, multi-functional layer stack built to exact tolerances:
Teaoraereke, situated in the South Tarawa region of Kiribati, represents a uniquely challenging operating environment for electronic devices and human-machine interface panels. As an equatorial Pacific atoll region, equipment deployed in Teaoraereke is subject to extreme atmospheric conditions characterized by continuous relative humidity (>85%), ambient temperature highs exceeding 35°C, high ultraviolet (UV Index 11+) solar radiation, intense saline aerosol (salt fog) exposure, and localized dust/sand airborne particulates.
Standard off-the-shelf membrane keypads rapidly deteriorate in such microclimates due to adhesive delamination, silver ink electromigration (short-circuiting caused by moisture micro-condensation), plasticizer embrittlement under UV rays, and contact oxidation. Ravo Electronics' dedicated PCB membrane switch solutions are custom-engineered to solve these specific environmental challenges in local infrastructure projects across Teaoraereke:
Potable water management in low-lying atolls relies heavily on reverse osmosis (RO) desalination plants and solar-powered water purification kiosks. Control interfaces must endure continuous chemical washdowns, high humidity, and wet hands. Ravo’s full perimeter gasket sealing, IP67-rated waterproof overlays, and non-corrosive gold-plated PCB contact pads guarantee zero liquid ingress and leak-proof operation.
Off-grid photovoltaic energy storage installations across Tarawa require robust user interfaces for monitoring system voltage, battery charge status, and inverter parameters. Our PCB membrane switches integrate high-brightness SMD status LEDs and UV-resistant Autotex XE polyester films that resist yellowing, cracking, and clouding under intense equatorial sunlight.
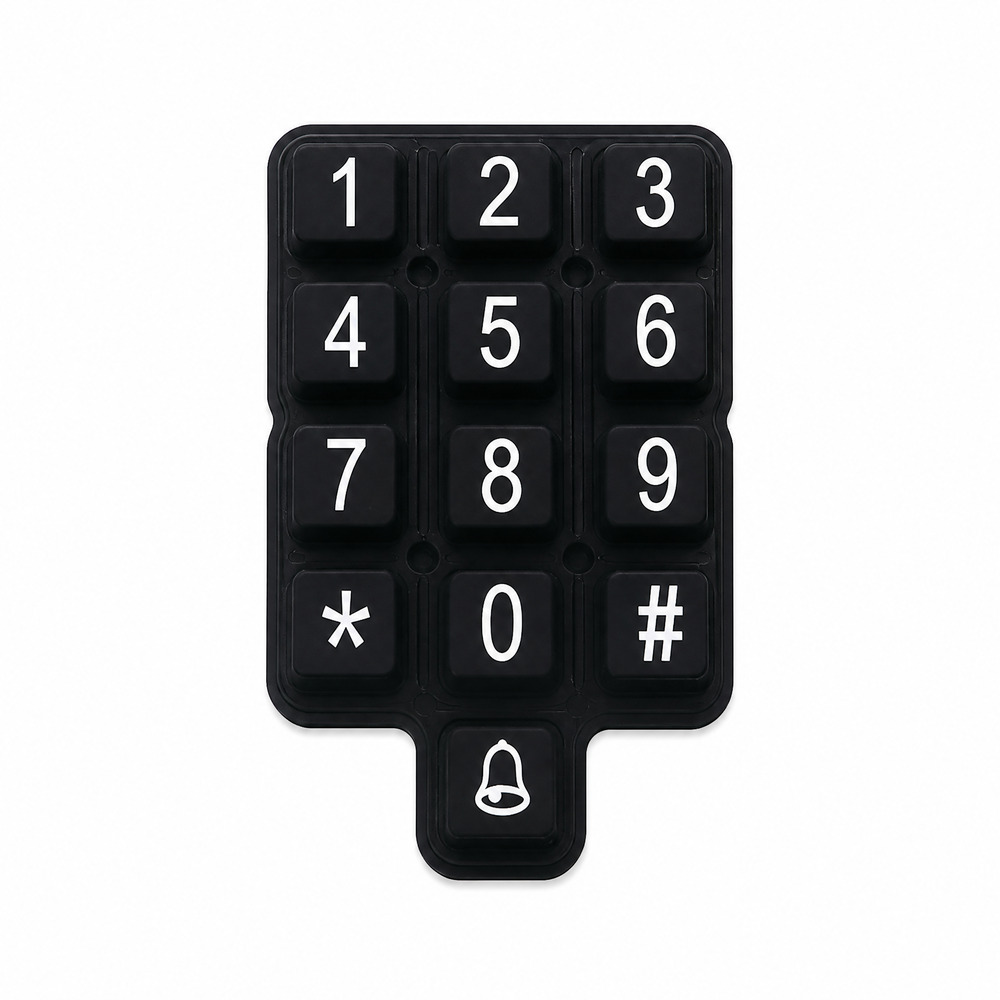
Fisheries, marine transport, and localized fuel distribution hubs demand explosion-proof, spark-free, fuel-resistant keypads. Ravo produces custom non-tactile and tactile silk-screened fuel dispenser keypads using solvent-proof sub-surface polycarbonate overlays bonded with 3M 468MP adhesive to prevent fuel permeation and surface erosion.
Island telecommunications relay stations and marine navigation controllers require tactile feedback keypads with integrated ESD grounding shields. By embedding copper foil or printed carbon grid shielding layers directly connected to the PCB ground plane, Ravo keypads discharge electrostatic charges up to 15kV without disrupting delicate microprocessors.
Selecting the optimal circuit carrier substrate is essential for balancing mechanical durability, thermal endurance, component density, and total cost of ownership. The table below outlines the core technical parameters evaluated during our Design for Manufacturability (DFM) review process:
| Technical Characteristic | Rigid FR-4 PCB Backer | Flexible Polyimide (FPC) | Silver Flex PET Circuit |
|---|---|---|---|
| Substrate Thickness Range | 0.4mm to 3.2mm (Rigid Glass Epoxy) | 0.05mm to 0.2mm (Flexible Polyimide) | 0.075mm to 0.125mm (Polyester Film) |
| Trace Conductive Material | 1oz / 2oz Rolled Copper (ENIG Plated) | 1oz Rolled Annealed Copper | Screen-printed Conductive Silver/Carbon Ink |
| Operating Temperature Limits | -40°C to +135°C (High TG Options) | -40°C to +125°C | -20°C to +70°C |
| SMD Component Soldering | Excellent (Reflow / Hand SMT) | Excellent (Automated SMT) | Limited (Conductive Epoxy Only) |
| Electromigration Resistance | Immune (Solid Copper Traces) | Immune (Solid Copper Traces) | Moderate (Requires Carbon Overcoat) |
| Ingress Protection Capability | Up to IP68 (Flat Rigid Sealing Surface) | Up to IP67 | Up to IP65 |
| Tactile Dome Life Cycle | > 3,000,000 Actuations (Firm Base) | > 2,000,000 Actuations | > 1,000,000 Actuations |
The Pacific island region is undergoing rapid digital modernization, driven by investments in renewable energy microgrids, climate-resilient water infrastructure, smart IoT monitoring systems, and modernized telecom networks. Key HMI design trends emerging across local and international procurement standards include:
Founded in 2003 in Dongguan, China—the world’s premier hardware manufacturing hub—Dongguan Ravo Electronics Co., Ltd. has spent over two decades engineering and producing custom membrane keypads, graphic overlays, flexible pressure sensors, silicone rubber buttons, and PCB switch assemblies for clients across Europe, North America, Oceania, and Asia.
Our dedicated team of senior HMI engineers reviews your CAD files (DXF, DWG, STEP), vector artwork (AI, PDF), and circuit schematics within 2 hours during business hours. We provide full Design for Manufacturability feedback, optimizing line widths, tail exit routes, pinouts, and material stack-ups prior to tooling fabrication.
We operate under a strict ISO 9001 quality management framework. Every custom switch batch undergoes 100% automated electrical continuity testing, resistance checking, actuation force curve measurement, loop resistance verification, and optical color-matching (Pantone/RAL) using high-precision spectrophotometers.
From single-piece R&D functional prototypes and low-volume initial runs (5–10 pcs) to high-volume automated roll-to-roll production, Ravo accommodates diverse procurement needs. Our in-house laser cutting, digital printing, automatic screen printing, and CNC milling tools drastically cut lead times and initial setup costs.
All raw materials—including Autotex polyester films, MacDermid polycarbonate, 3M adhesives, DuPont conductive silver inks, stainless steel metal domes, and lead-free PCB laminates—are 100% compliant with RoHS and REACH regulations, accompanied by certified material test reports.
Whether you are designing a new medical instrument, upgrading an outdoor power inverter, modernizing fuel station keypads, or deploying climate-resilient industrial controllers in Teaoraereke or anywhere worldwide, Dongguan Ravo Electronics Co., Ltd. provides the engineering authority, manufacturing precision, and competitive pricing required to bring your vision to life.
Upload your technical drawings, circuit schematics, or sample specifications today. Our engineering team will deliver a comprehensive DFM feedback report and factory-direct quotation within 2 hours.