EN
 DE
 FR
 ES
 RU
 JA EN DE FR ES RU JA
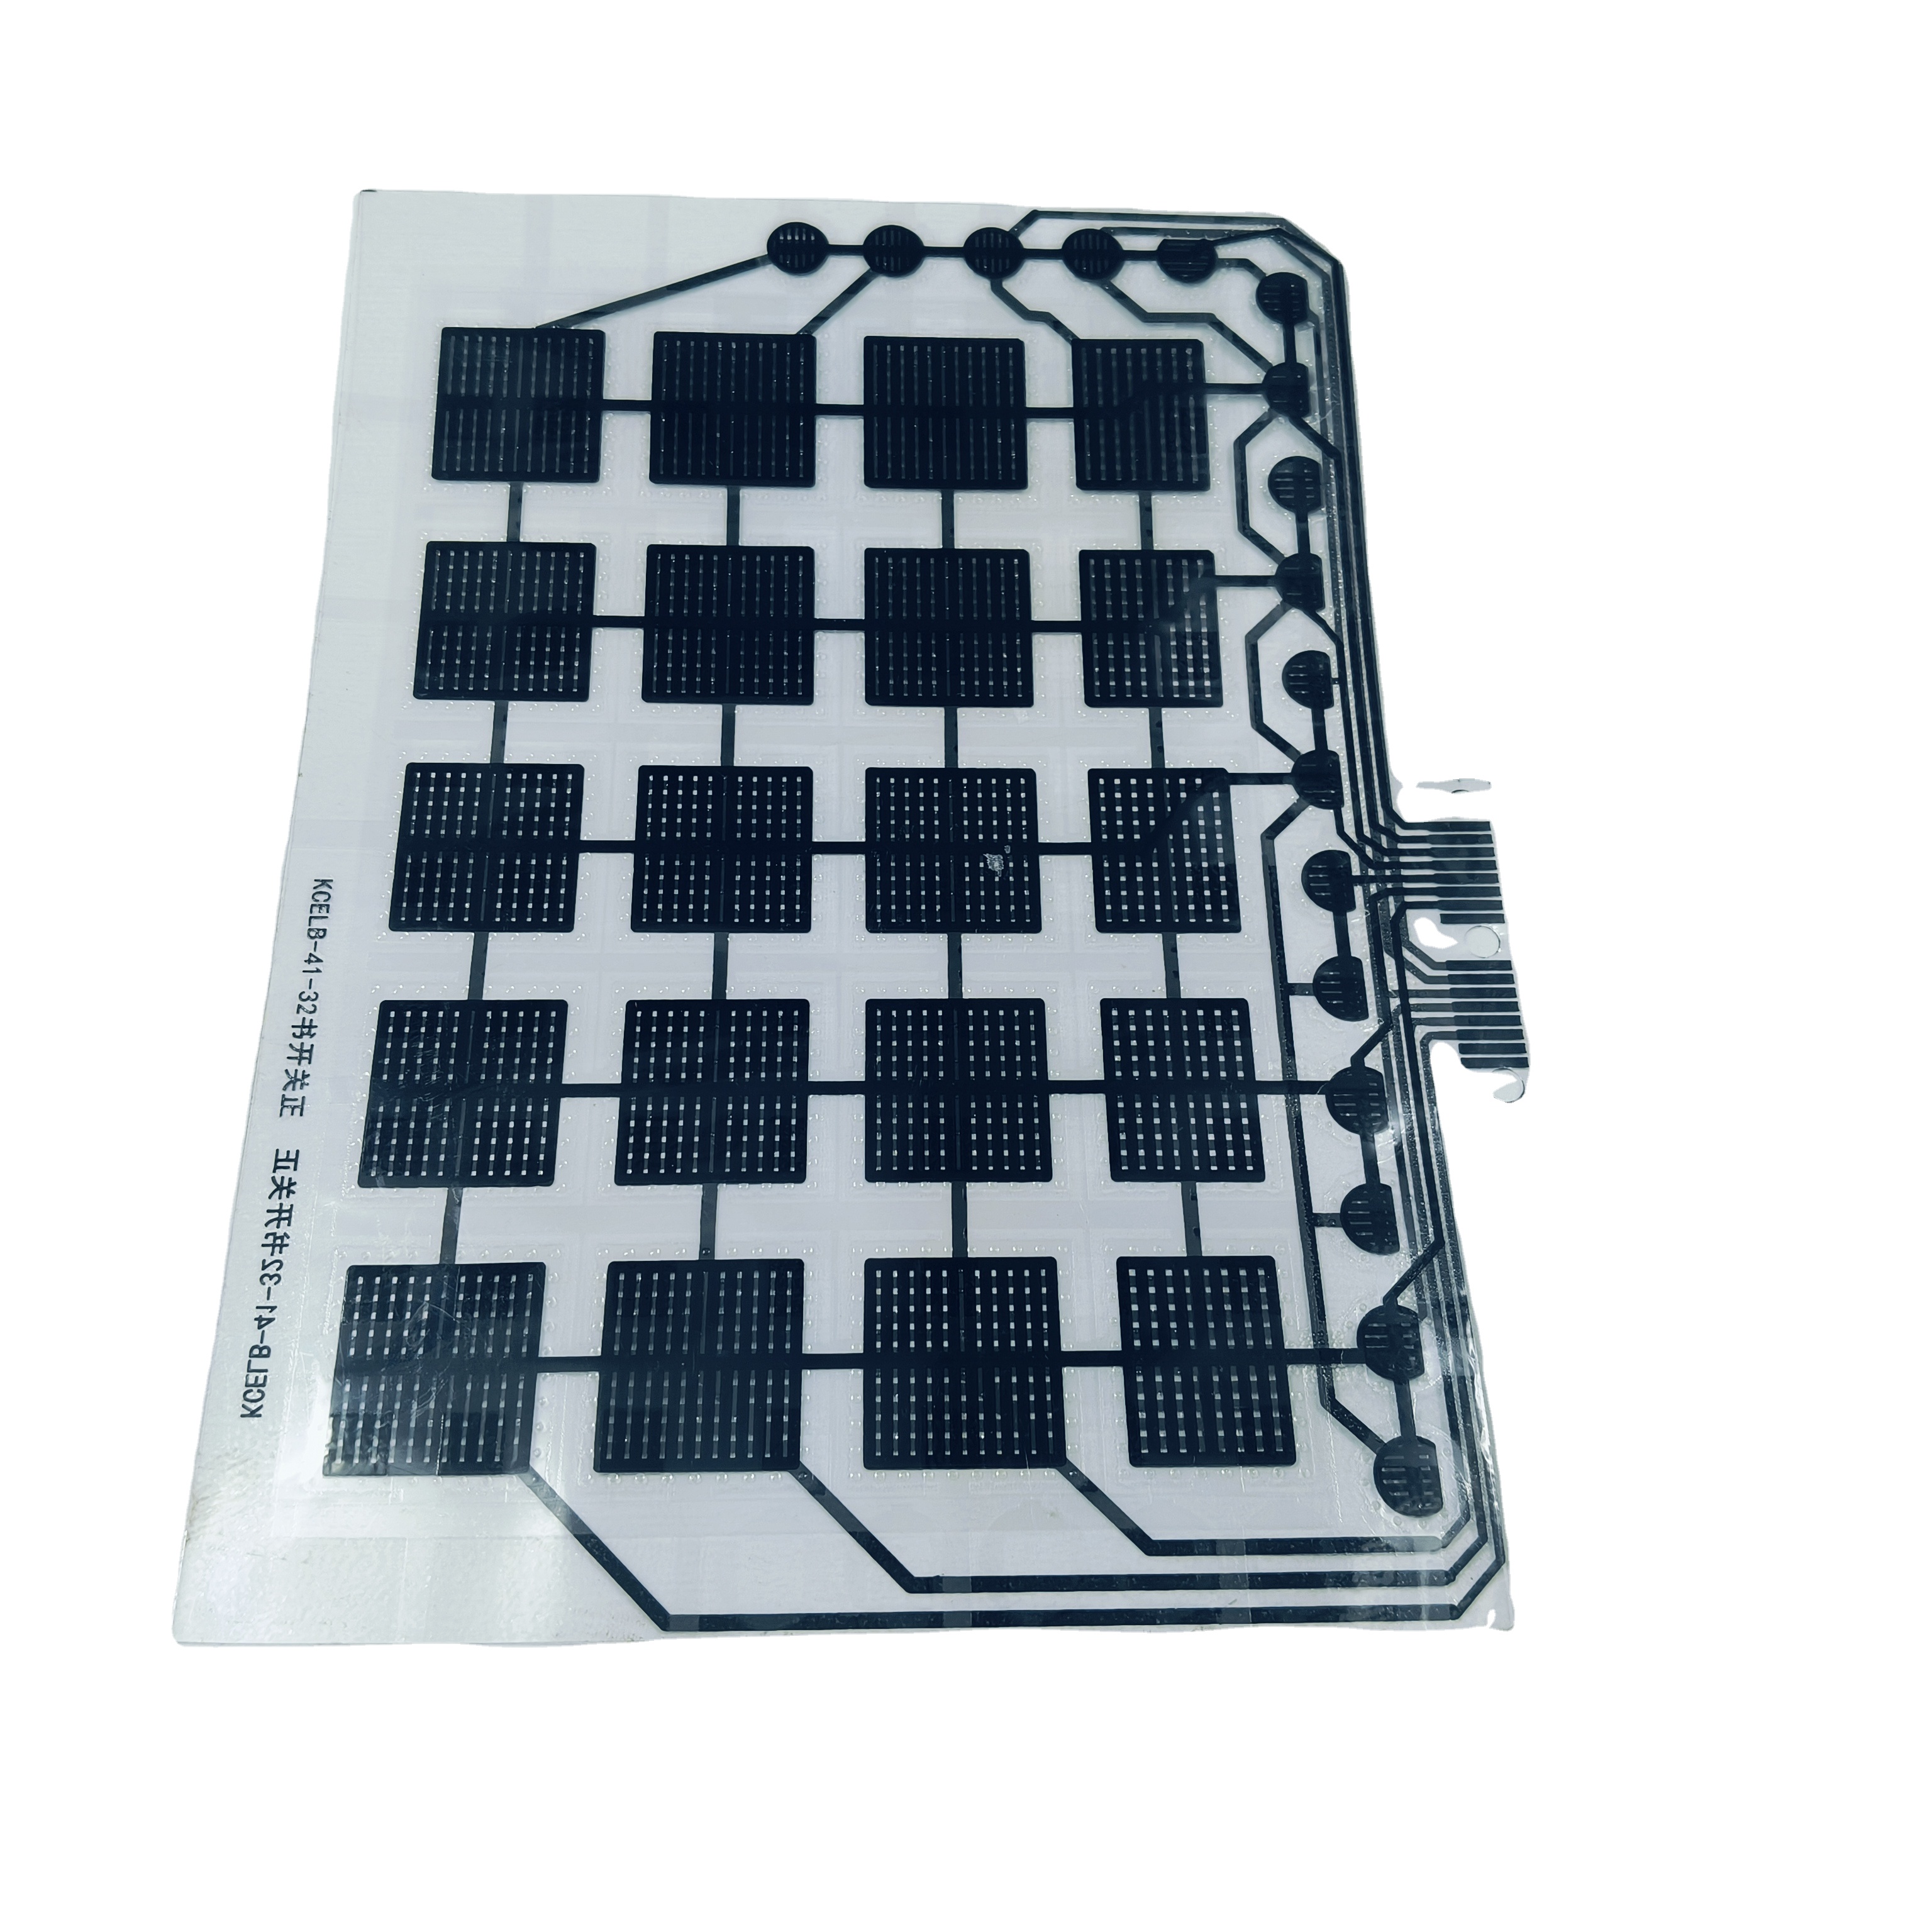
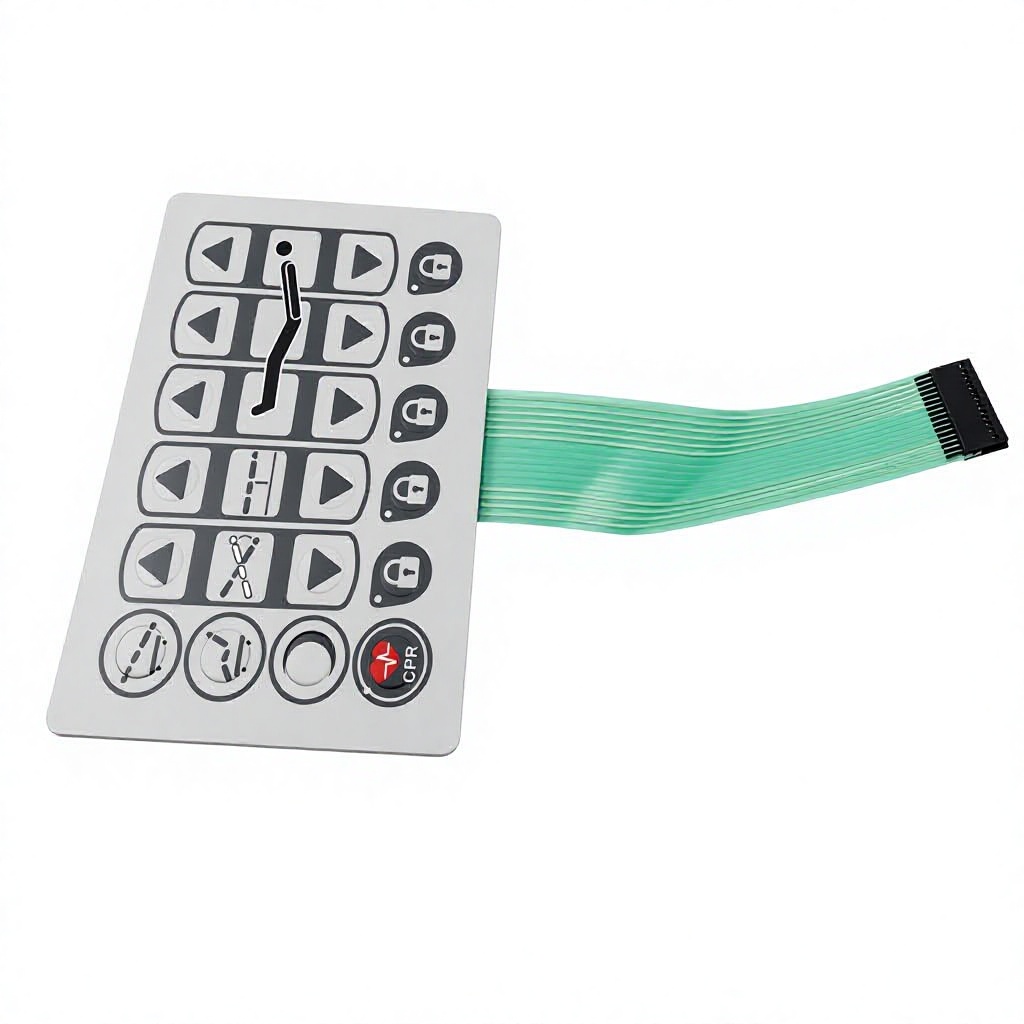
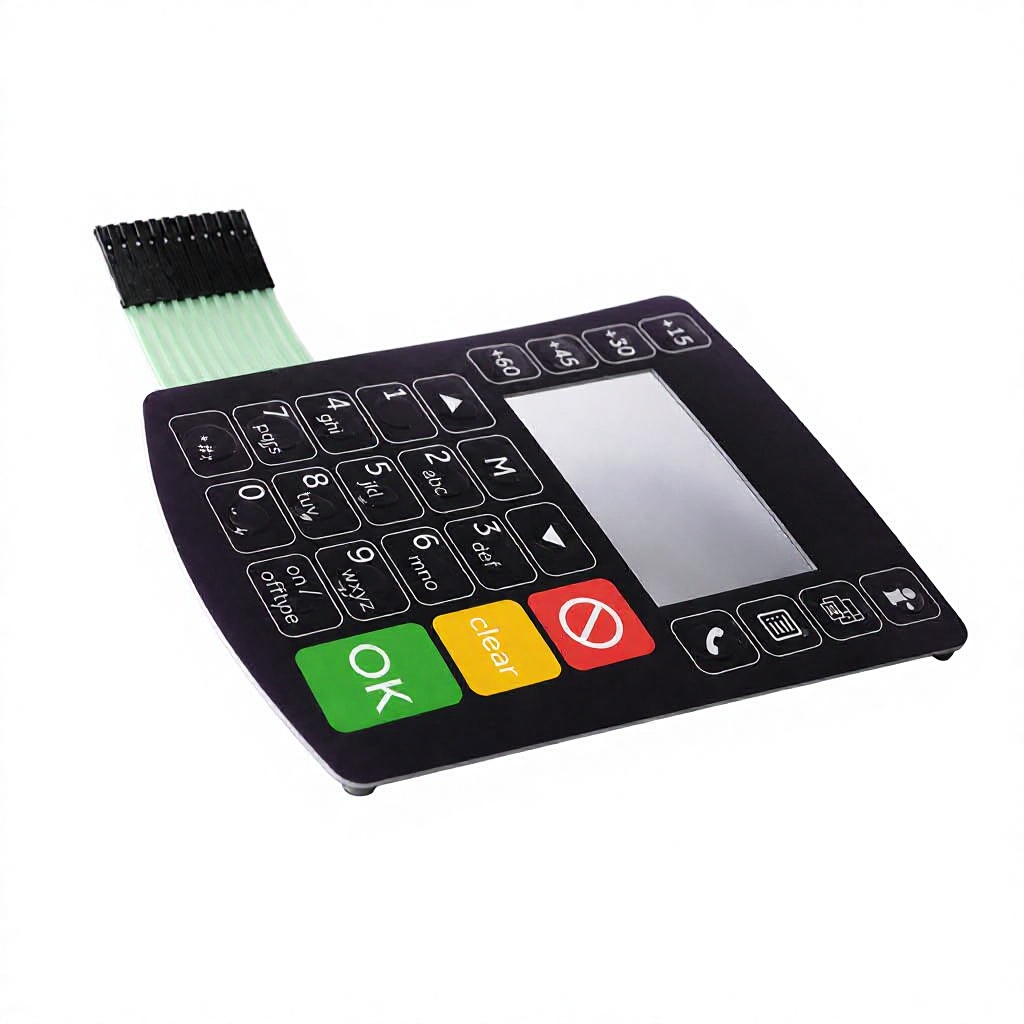
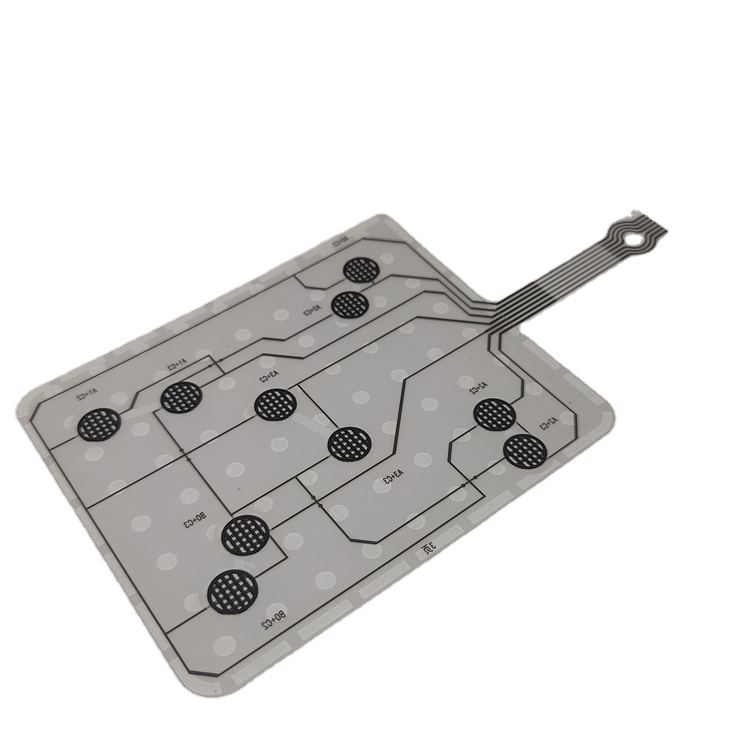
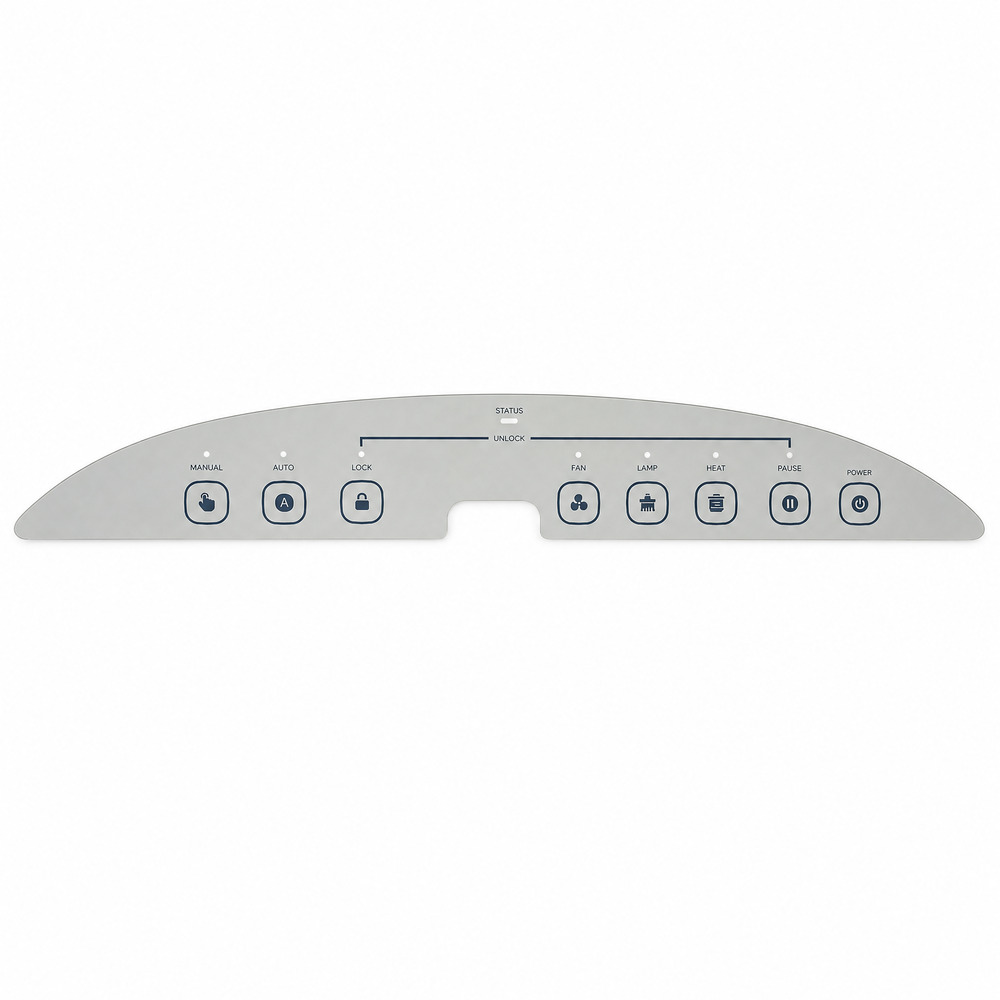
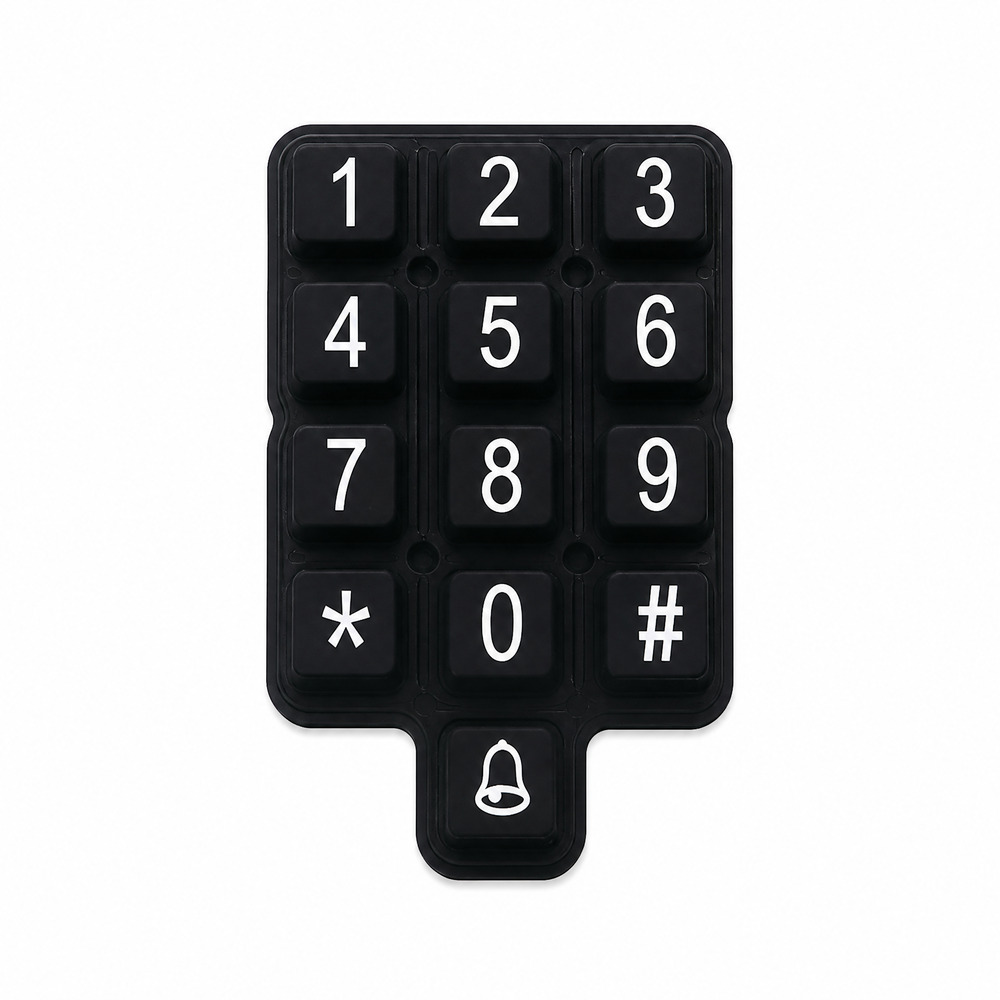
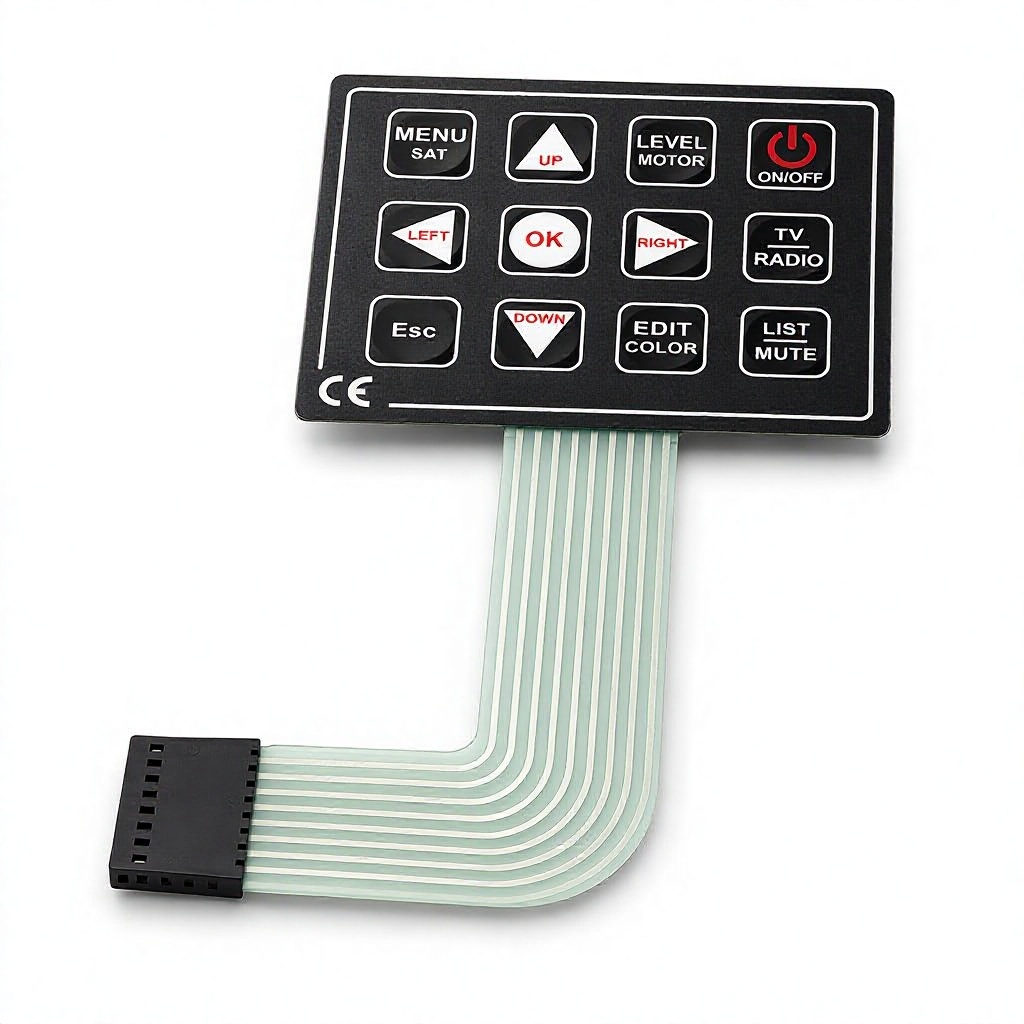
As a global pioneer in Human-Machine Interface (HMI) engineering, Dongguan Ravo Electronics Co., Ltd. (founded in 2003) operates a state-of-the-art 12,000 square meter production complex in Fenggang Town, Dongguan, Guangdong, China. Housing over 300 highly trained technicians, cleanroom screen-printing facilities, automated SMT lines, and laser die-cutting machinery, Ravo specializes in end-to-end design, prototyping, and mass manufacturing of high-reliability membrane switches, rigid PCB-backed membrane keyboards, flexible FPC circuits, silicone keypads, and force-sensitive thin-film pressure sensors.
For industrial original equipment manufacturers (OEMs), systems integrators, and engineering firms operating within Mitrovica and the broader Western Balkan region, selecting the correct control panel substrate is critical. Modern industrial facilities in Mitrovica—ranging from heavy metallurgical refining units at the historic Trepča mining complex to advanced fuel logistics hubs and municipal medical centers—require user interfaces capable of surviving intense mechanical stress, chemical washdowns, and drastic ambient temperature swings (-20°C to +70°C).
Information Gain Insight: Unlike standard flexible polyester (PET) printed circuits, a PCB Membrane Switch utilizes a rigid FR-4 fiberglass printed circuit board as its structural backer. This allows surface-mount devices (SMD LEDs, resistors, capacitors, microcontrollers, and heavy-duty terminal headers) to be directly soldered onto the backer. The result is a robust, self-supporting 2-in-1 HMI module that eliminates fragile flexible tails, resists high mechanical vibration, and guarantees over 1,000,000 switch operations under extreme industrial loads.
By controlling every step of production under ISO 9001 quality management, Ravo ensures that every exported HMI control assembly conforms strictly to EU environmental standards (RoHS, REACH) and international IP67/IP68 ingress protection standards. Our dedicated engineering team provides DFM (Design for Manufacturability) evaluation within ≤2 hours, helping Mitrovica engineering teams transition seamlessly from CAD concept to tested prototype in as fast as 5 to 7 days.
To withstand the rigorous operational demands of Mitrovica’s industrial machinery, our engineering directorate specifies premium-grade European and Japanese raw materials. Below is the multi-layer structural breakdown of a industrial-grade PCB-backed membrane switch assembly:
| Layer Sequence | Material Component | Engineering Function & Specifications |
|---|---|---|
| Layer 1 (Top) | Graphic Overlay | Autotex XE / Bayer Polycarbonate (0.125mm–0.25mm) with selective textured finishes, anti-glare display windows, and UV-resistant inks. |
| Layer 2 | Overlay Adhesive | 3M 467MP / 3M 468MP acrylic adhesive layer engineered for high shear strength and moisture barrier seal. |
| Layer 3 | Retainer & Metal Domes | Stainless steel tactile domes (Tac-Dome) offering distinct tactile snap force (280g to 450g) and long actuation life (1M+ cycles). |
| Layer 4 | Rigid PCB Substrate | FR-4 Glass-reinforced epoxy laminate (0.8mm–3.2mm thick), 1oz/2oz Copper traces, Immersion Gold (ENIG) or HASL surface finish. |
| Layer 5 (Embedded) | SMT Electronic Elements | Directly soldered surface-mount LEDs (side-lit or top-emitting), ballast resistors, noise bypass capacitors, and pin headers. |
| Layer 6 (Bottom) | Mounting Adhesive / Standoffs | 3M 9448A / 3M 300LSE adhesive for direct mounting to powder-coated steel enclosures, stainless housings, or cast aluminum chassis. |
For hardware designers in Mitrovica evaluating HMI architectures, the choice between traditional flexible PET switches and rigid PCB membrane switches comes down to structural integrity and functional density:
Heavy mining equipment, ore processing crushers, and zinc/lead refining plants in Mitrovica demand heavy-duty control panels that resist fine mineral dust, oils, and physical impacts. Our IP67-sealed PCB membrane switches utilize Autotex XE hard-coated polyester overlays with full perimeter adhesive seals. Featuring stainless-steel metal domes with high actuation forces (400g), operators wearing heavy safety gloves receive tactile feedback with every keystroke, preventing accidental machine triggers in high-noise environments.
Mitrovica’s growing network of commercial petrol stations and regional fuel depots requires weatherproof, non-tactile, or tactile keypad interfaces built for continuous outdoor operation. Ravo supplies silk-screen printed, UV-resistant non-tactile fuel dispenser keypad panels engineered with 3M 300LSE low-surface-energy adhesive backings. These keypads resist fuel splashes, chemical degradation, extreme winter frost (-25°C), and summer solar exposure without delamination or color fading.
Hospitals, diagnostic clinics, and surgical centers across Mitrovica utilize Ravo’s medical-grade tactile membrane switch panels for bed controllers, patient lifters, and sterilizers. Engineered with antimicrobial graphic overlays and seamless wipedown surfaces, these panels allow complete chemical disinfection using alcohol or bleach solutions. Integrated LED status indicators provide immediate visual feedback for medical staff during emergency bed positioning.
Mitrovica’s water treatment infrastructure and municipal power monitoring stations require capacitive touch keypads and backlit PCB switches. By replacing mechanical pushbuttons with zero-travel capacitive touch panels mounted behind transparent glass or polycarbonate enclosures, municipal operators benefit from maintenance-free, wear-resistant controls that eliminate water ingress and physical switch fatigue.
The industrial landscape in Mitrovica and the broader Balkan corridor is undergoing rapid modernization. Driven by European Union equipment standards, increased foreign direct investment in manufacturing, and local infrastructure updates, purchasing managers and engineering departments in Mitrovica are adopting modern HMI strategies:
Traditional discrete pushbuttons and mechanical switches leave panel cutouts vulnerable to water, dust, and vibration. Mitrovica equipment builders are migrating to single-piece sealed PCB membrane switch units that combine graphics, switches, backlighting, and structural mounting into a single drop-in assembly.
Industrial machinery operated in 24/7 mining shifts or low-light municipal pump houses increasingly mandates uniform backlighting. Ravo’s side-emitting SMT LED light-guide configurations deliver high-contrast key illumination without hotspots, reducing operator fatigue during night operations.
Modern commercial equipment manufacturers in the Balkans are blending sleek capacitive touch zones with tactile metal-dome switches on the same control panel—offering capacitive touch for menu navigation and tactile domes for critical Start/Stop safety commands.
With strict EU-aligned environmental mandates taking effect across the region, procurement teams require full chemical compliance (RoHS 3, REACH SVHC) along with documented material testing for UV stability, salt spray endurance, and thermal cycle survival.
Ravo has over 14 years of direct export experience to European destinations. We ship directly from our Dongguan facility via DHL, FedEx, or air freight cargo to Pristina Airport (PRN) or direct overland logistics routes serving Mitrovica. We provide full commercial documentation, HS Code classification (e.g., HS 853710 for HMI control panels), certificates of origin, and custom commercial invoices to ensure smooth customs processing.
Once your CAD drawings (DXF, DWG, Gerber, or STEP) and artwork (AI, PDF with Pantone references) are approved, engineered prototype samples are typically completed within 7 to 10 working days. Mass production lead time ranges from 2 to 3 weeks depending on order volume and SMT component sourcing.
Yes. Mitrovica experiences cold winters with temperatures dropping below -20°C and warm summers reaching +38°C. We design outdoor HMI switches using specialized Autotex XE UV-resistant polyester overlays, closed-cell perimeter gaskets, and 3M 300LSE/468MP adhesives rated from -40°C to +105°C, ensuring IP67 water/dust ingress protection year-round.
To support innovation and product development for Mitrovica engineering firms, Ravo supports rapid prototyping from as low as 1 to 5 pieces. For standard mass production runs, MOQs start at 100 to 500 pieces depending on the layer stack-up and PCB dimensions.
Every single manufactured PCB membrane switch undergoes 100% automated electrical continuity testing, resistance testing, LED polarity checks, and short-circuit verification prior to packaging. Furthermore, sample units from every production batch undergo actuation life testing (1,000,000 presses) and environmental thermal shock testing in our quality testing lab.
We accept 2D vector graphic artwork files (Adobe Illustrator .AI, CorelDraw, Vector .PDF) and 2D/3D mechanical files (AutoCAD .DXF, .DWG, SolidWorks .STEP / .IGS). For PCB routing layers, Gerber RS-274X format is preferred. Our engineering response time is ≤2 hours during business hours.
Yes. All raw materials—including Autotex polyester, Bayer polycarbonate films, 3M adhesives, FR-4 PCB laminates, lead-free solder pastes, and inks—are 100% compliant with EU RoHS 3.0 and REACH regulations. SGS material declaration reports are provided upon request.
Absolutely. We specialize in embedding SMD LEDs for individual key status indicators, edge-lit backlight panels, and dead-front hidden-until-lit graphic icons. Display windows can be clear, tinted red/green/blue, or printed with anti-scratch matte/gloss coatings for LCD and 7-segment LED screen integration.
Serving equipment builders, industrial integrators, and engineering buyers in Mitrovica and worldwide. Request a comprehensive product catalog, engineering DFM consultation, or direct price quote today.