 EN
 DE
 FR
 ES
 RU
 JA EN DE FR ES RU JA
Below is our core line of custom-engineered membrane keyboards, capacitive touch switches, and high-sensitivity user interfaces manufactured for medical apparatus, hospital control stations, and diagnostic instrumentation deployed across St. George's healthcare networks.
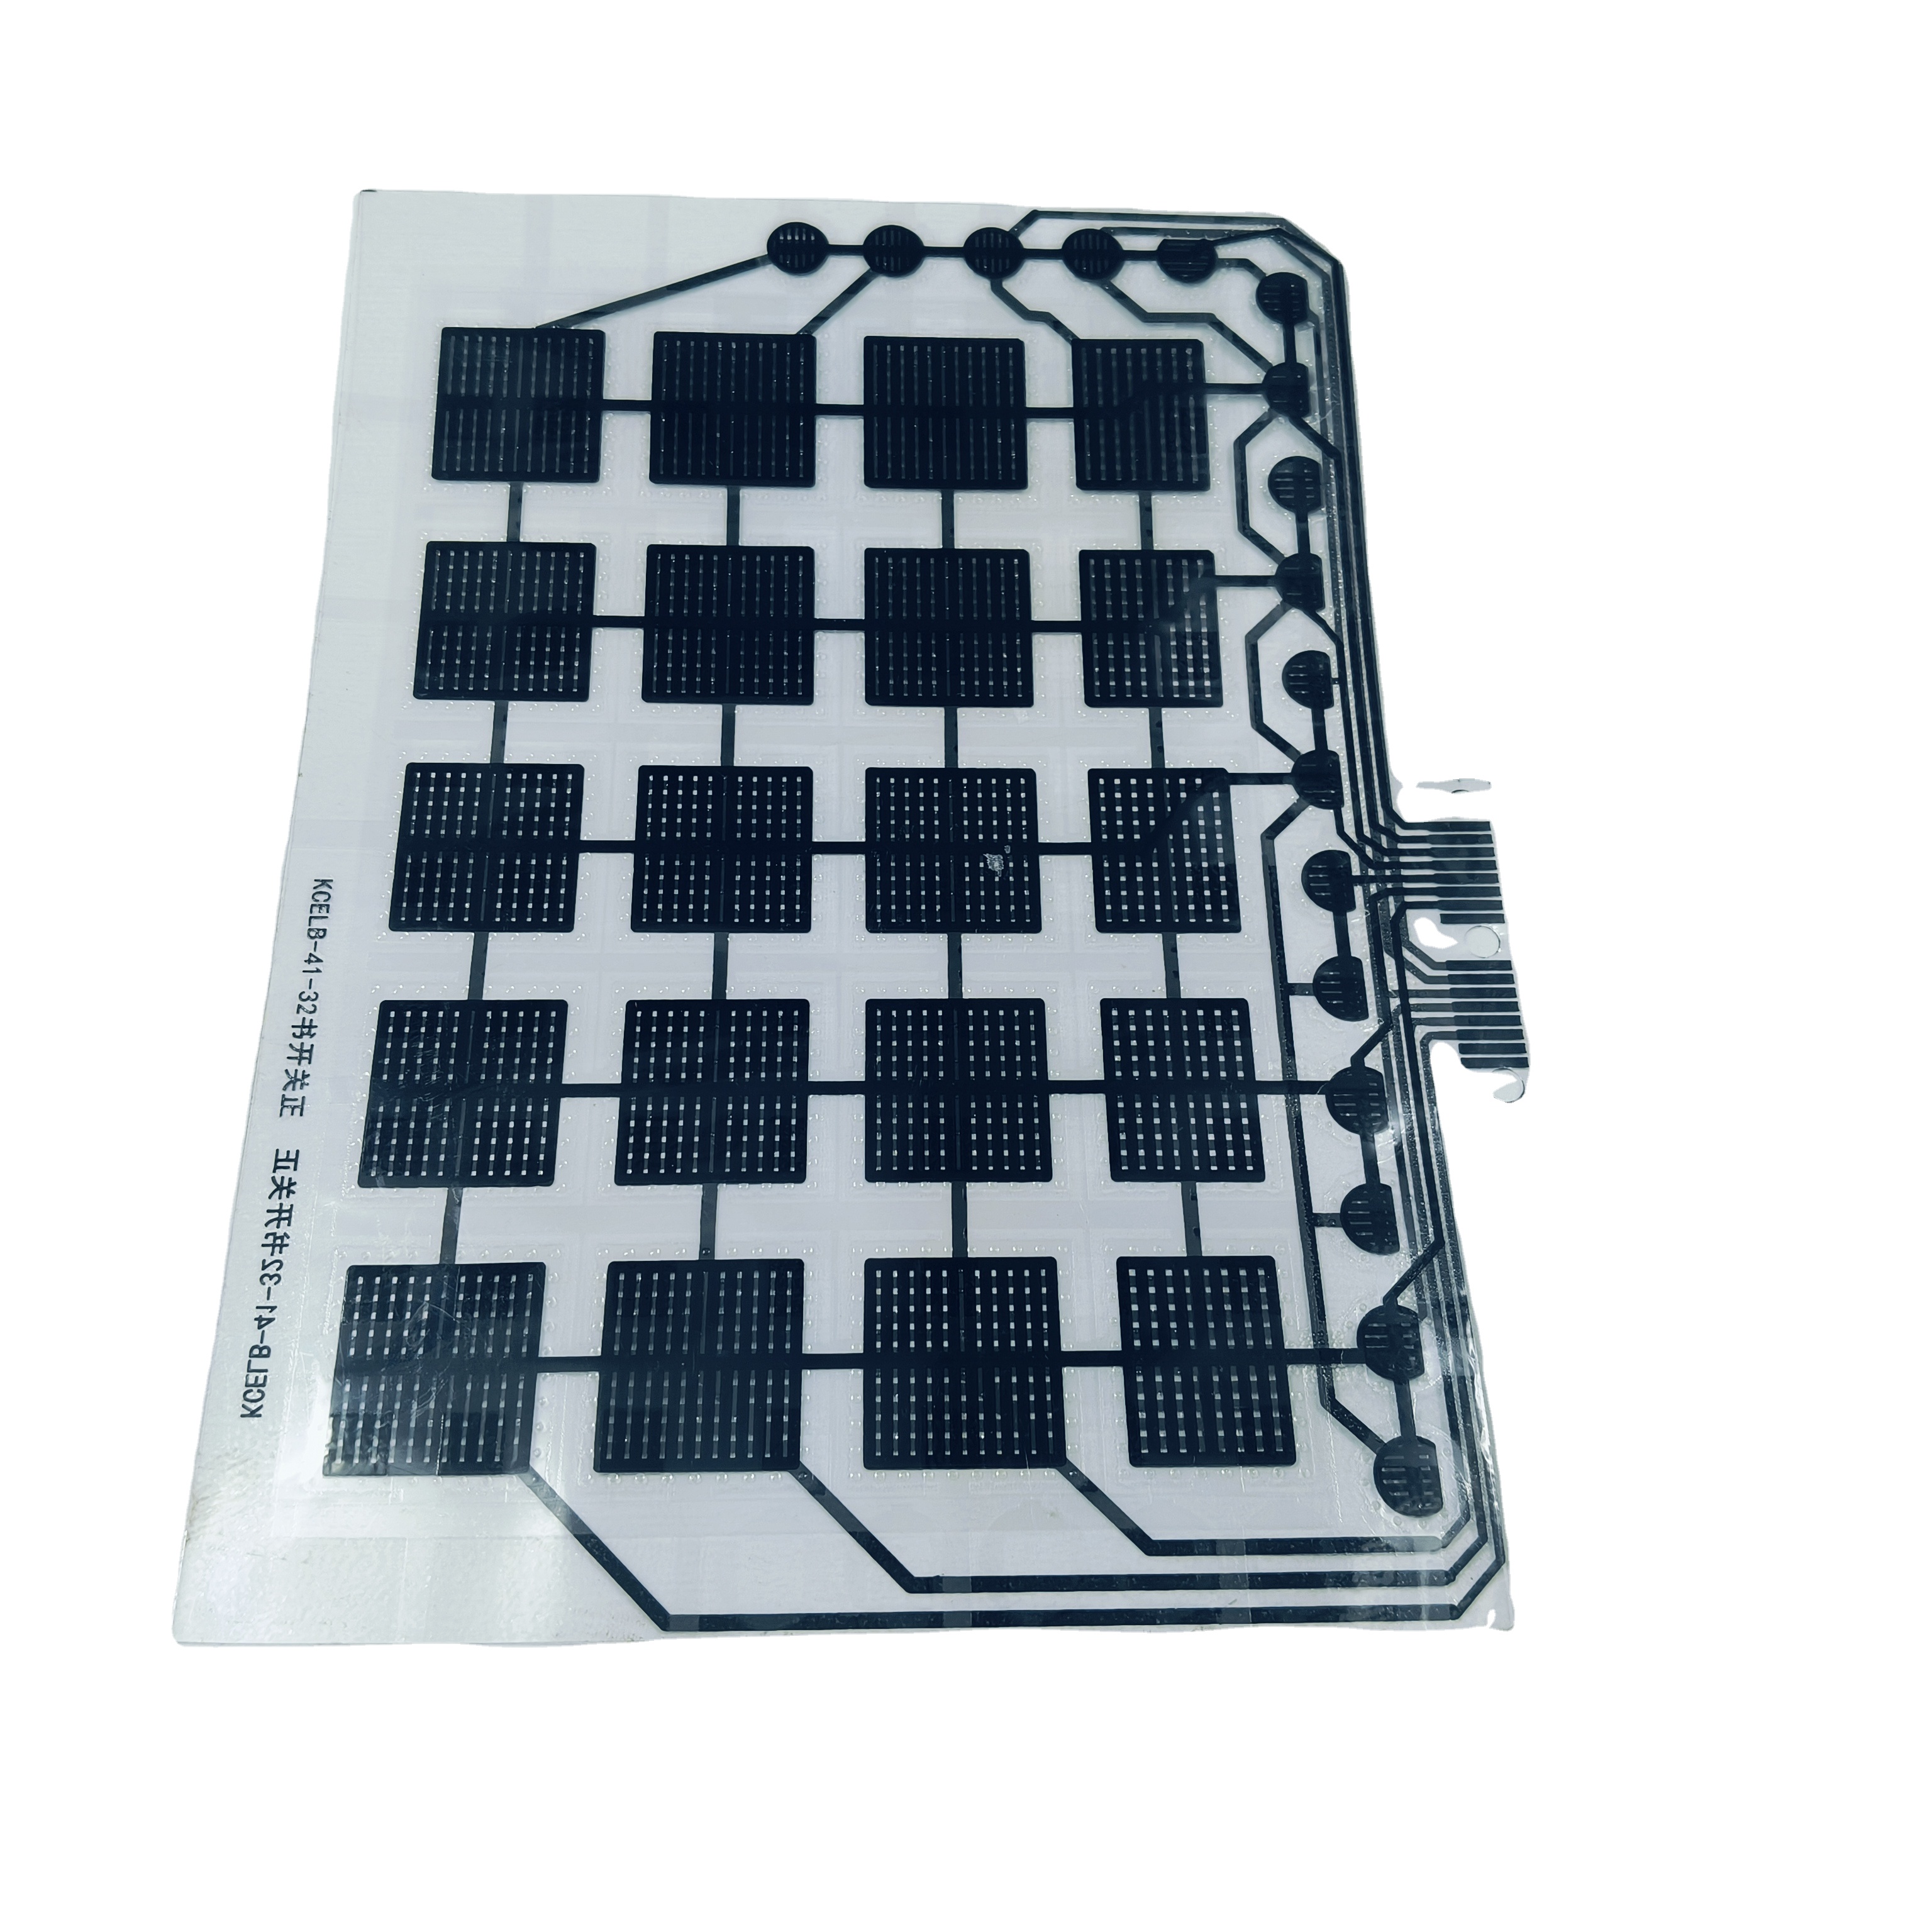
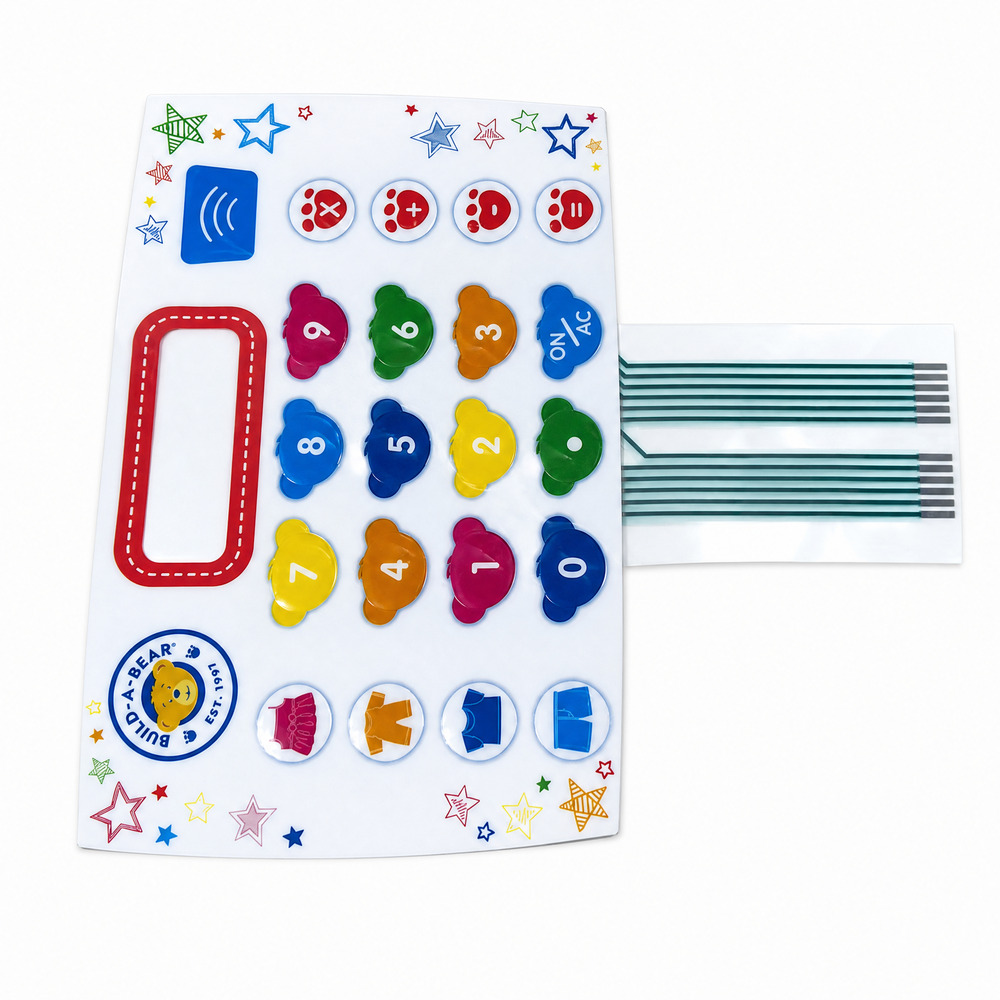
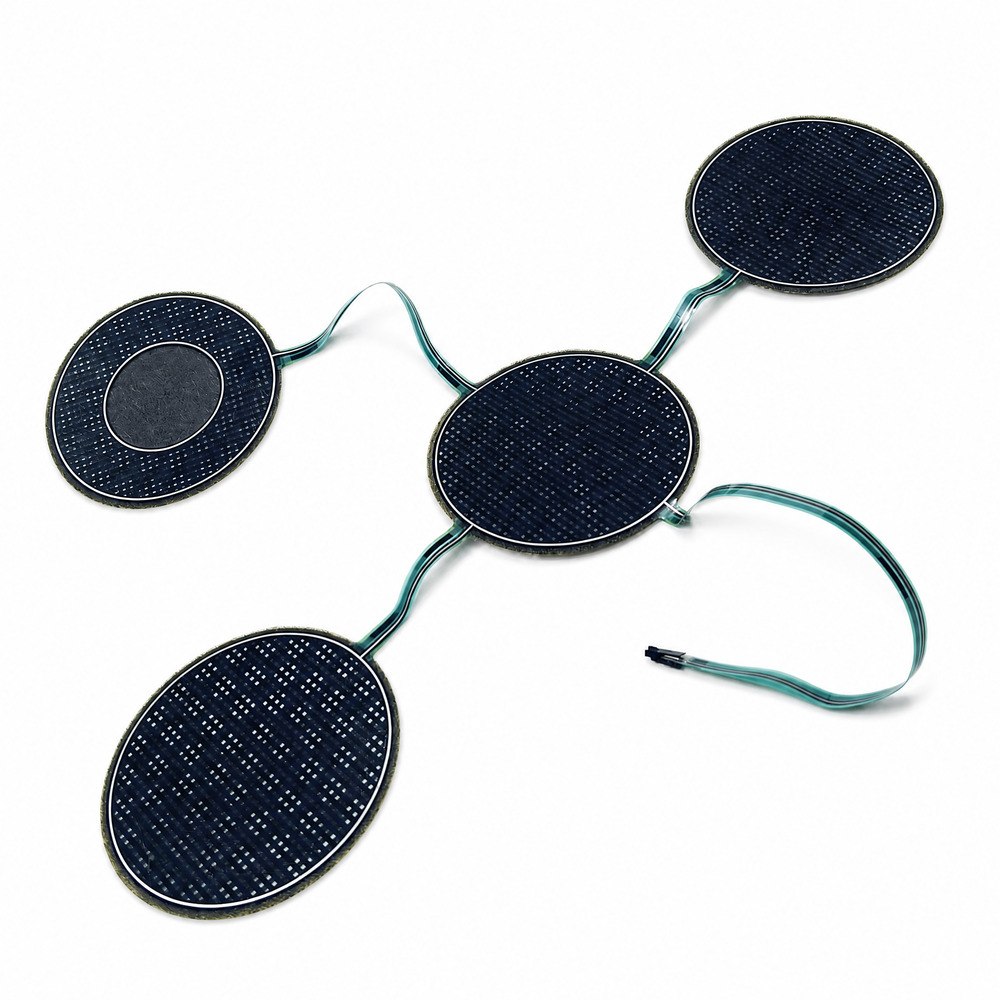
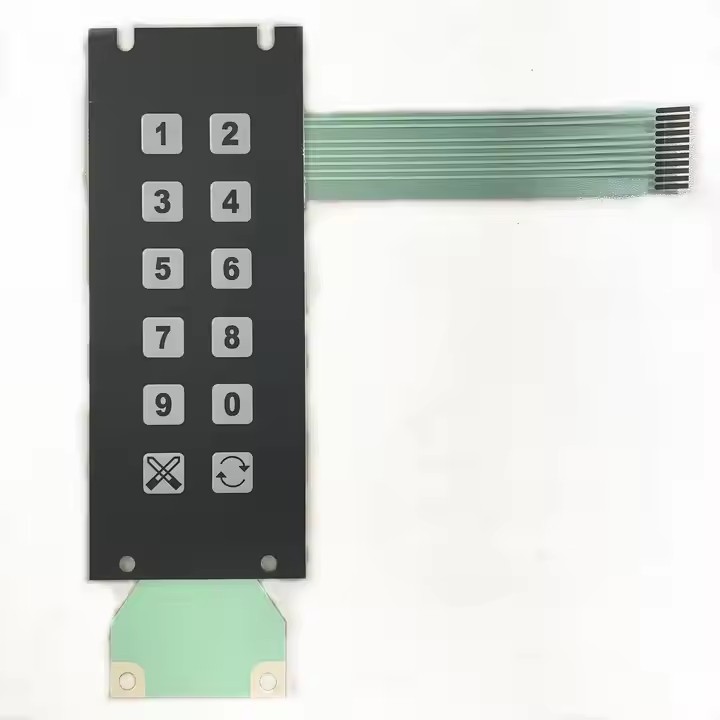
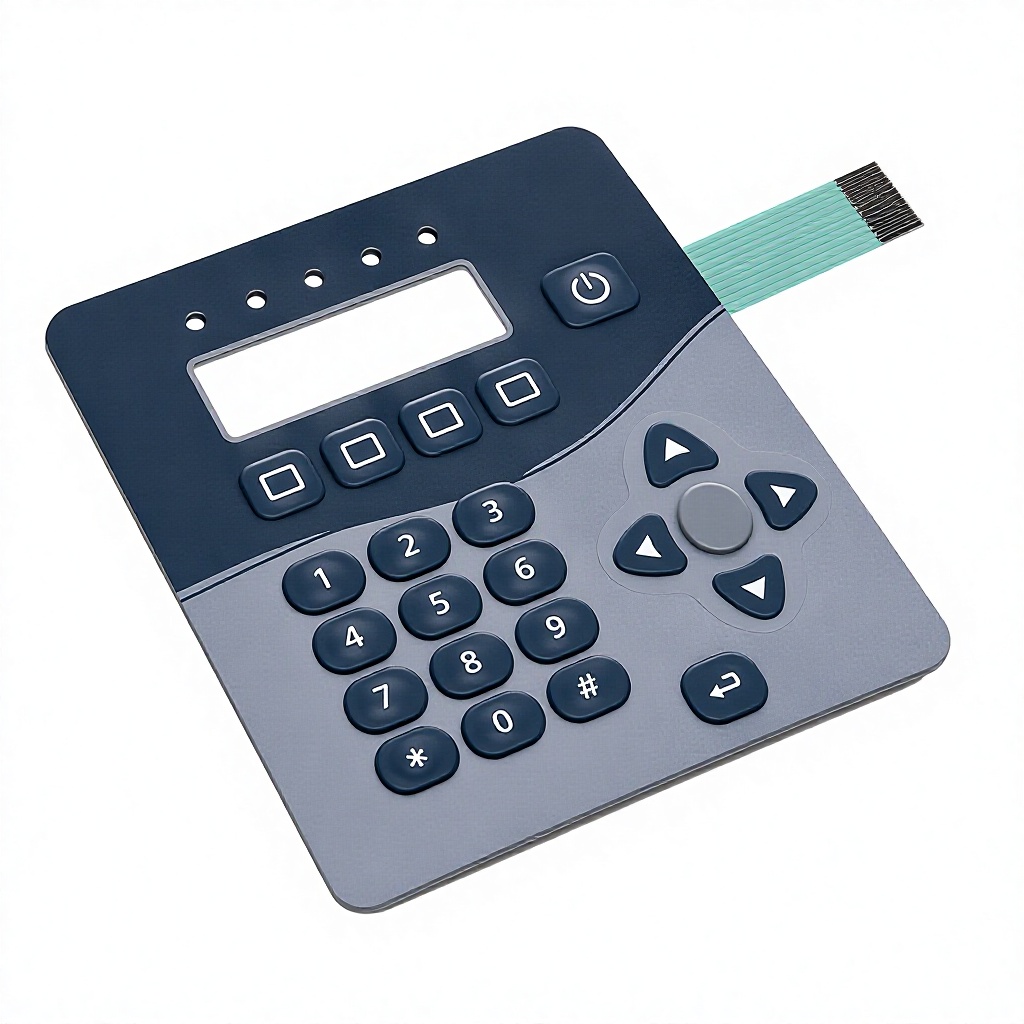
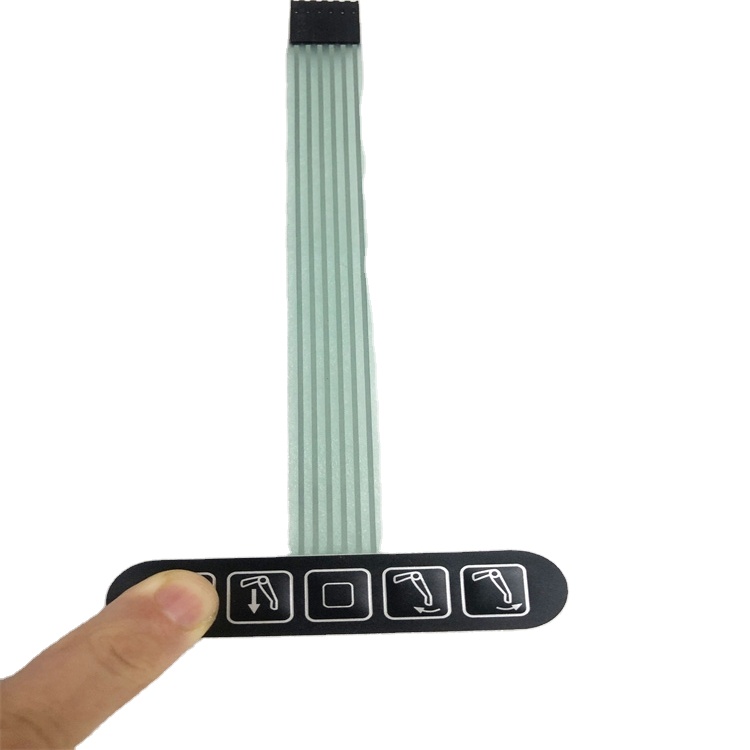
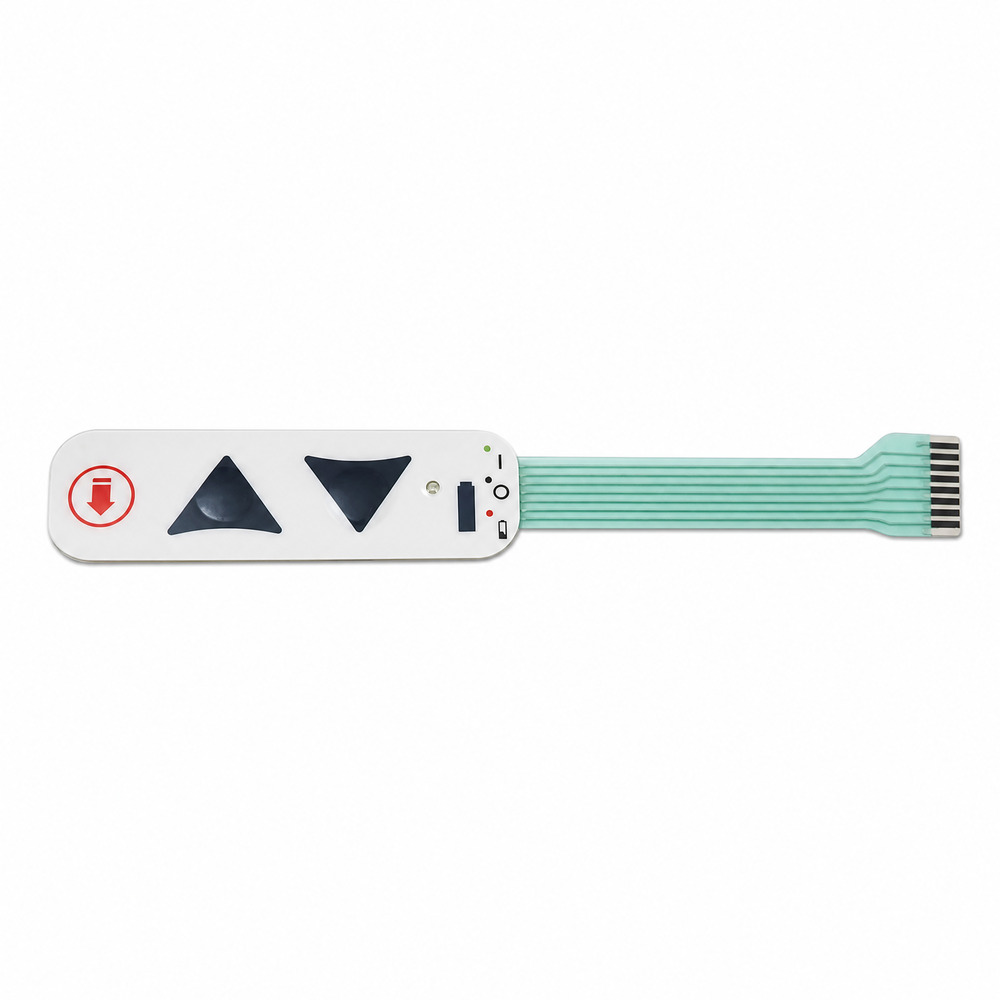
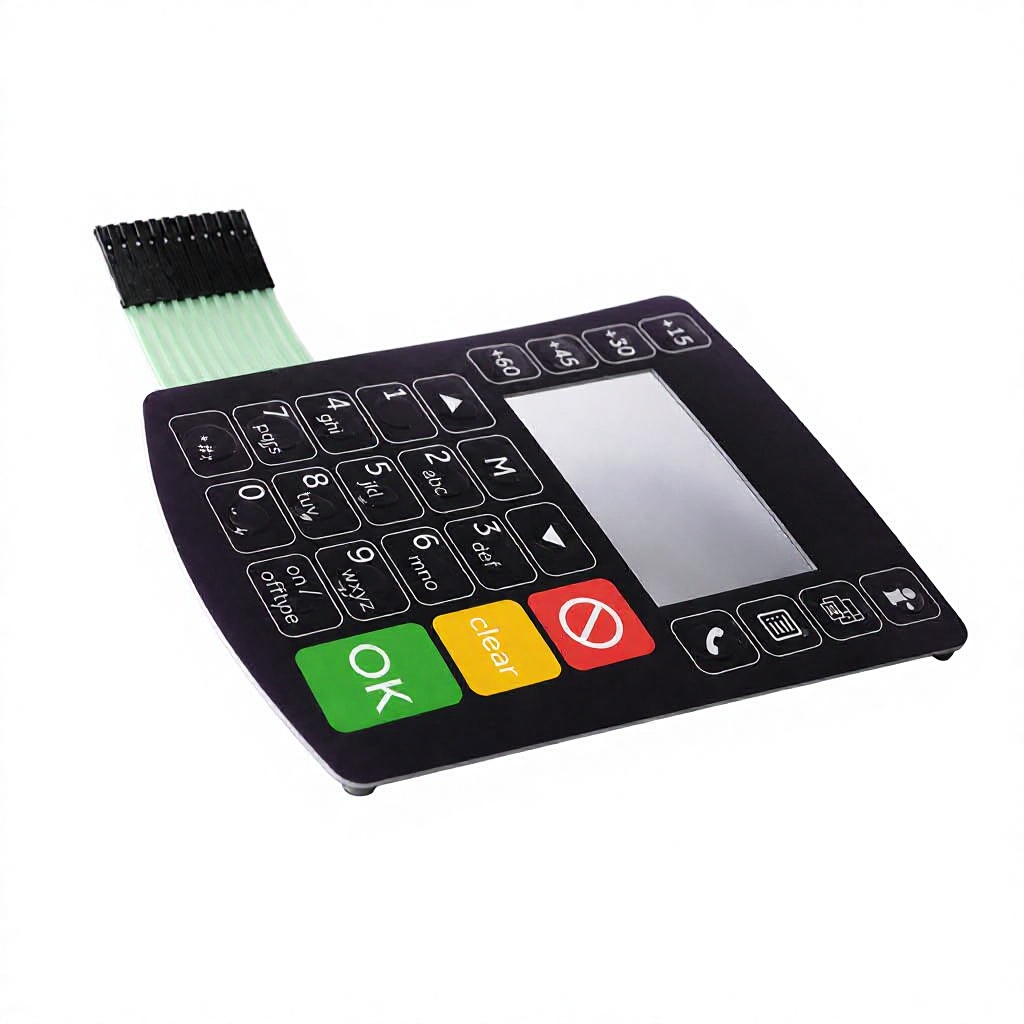
Modern medical devices deployed across healthcare networks, teaching hospitals, research centers, and clinical facilities in St. George’s demand Human-Machine Interfaces (HMIs) that go far beyond standard commercial keyboards. In sterile environments where cross-contamination risks, aggressive chemical cleaning agents, and high operational frequencies are daily realities, medical equipment engineers require custom OEM membrane switches built to strict ISO standards and exacting material specifications.
As a leading custom OEM manufacturer operating a 12,000 m² state-of-the-art facility since 2003, Dongguan Ravo Electronics Co., Ltd. specializes in translating complex medical HMI requirements into ruggedized, highly reliable thin-film switch assemblies. Whether your organization is refurbishing diagnostic equipment for St. George’s clinical laboratories, assembling portable patient monitoring systems, or engineering custom medical control units, selecting the right membrane switch manufacturing partner is pivotal to long-term device safety and user compliance.
Medical HMIs must achieve an optimal balance between infection control compliance (IP65 to IP68 sealing), tactile ergonomics (click-ratio feedback or capacitive touch), and chemical resistance against hospital-grade disinfectants like Isopropyl Alcohol (70-90%), Hydrogen Peroxide, and Sodium Hypochlorite solutions.
To deliver true "Information Gain" for procurement specialists and medical design engineers in St. George’s, we break down the exact multi-layer stack-up engineered into our custom medical switches:
Utilizing premium textured Polyester films (e.g., MacDermid Autotex AM or Melinex) impregnated with silver-ion antimicrobial agents. These built-in microbicidal barriers actively suppress bacterial growth (such as MRSA and E. coli) on switch surfaces 24/7, maintaining efficacy even after thousands of hospital cleaning cycles.
Engineered with closed-cell acrylic foam gaskets and 3M 467MP/468MP high-performance acrylic adhesives that create a complete perimeter fluid dam. This prevents ingress of bodily fluids, saline solutions, and spillages into the underlying silver trace printed circuitry.
Incorporating selective carbon-printed grid layers, solid aluminum foil, or transparent Indium Tin Oxide (ITO) shielding. This ensures full electromagnetic compatibility (EMC) and protects sensitive medical logic boards from Electrostatic Discharge (ESD) up to 15kV.
When specifying custom membrane switches for St. George's medical projects, mechanical tactile response directly impacts clinical speed and accuracy:
Deploying electronic medical equipment in St. George’s requires special consideration for both environmental conditions and operational dynamics. Whether servicing tropical coastal medical centers or urban clinical institutions, our custom OEM membrane switch solutions are tailored to local challenges:
In St. George’s ward environments, bedside remotes and nurse-call keypads must handle continuous handling by patients and medical staff. Our switches combine soft rubber silicone keycaps or embossed tactile PET overlays with sealed ribbon tails, preventing fluid intrusion while offering low-noise actuation during night shifts.
St. George’s warm, high-humidity, and saline-rich coastal air can degrade cheap commercial electronics. We utilize specialized UV-cured potting resins, gold-plated tail contacts, and corrosion-resistant silver-paste screen inks that resist oxidation and delamination under high humidity.
For sterilizers, dental equipment, and autoclaves operated in St. George’s clinics, front panels are subject to high ambient temperatures and steam exposure. Ravo engineers high-temp polyimide (Kapton) circuits and high-temperature acrylic adhesive backings capable of continuous duty up to 105°C.
Procurement departments and biomedical engineering hubs across St. George’s are witnessing several key technology transitions in medical interface design:
Use the following technical parameters as a reference when submitting custom OEM engineering drawings for St. George’s projects:
| Engineering Parameter | Standard Medical Specification | High-Precision OEM Customization |
|---|---|---|
| Overlay Base Material | Autotex Textured Polyester / Polycarbonate (0.125mm - 0.25mm) | Antimicrobial Polyester / Chemical-Hardcoated Gloss Film |
| Circuit Layer Substrate | 0.125mm Heat-Stabilized PET Film | Double-Sided Polyimide FPC / Rigid FR-4 PCB Backer |
| Tactile Actuation Force | 280g - 350g Stainless Steel Metal Domes | Custom 180g - 500g Domes / Custom Thermoformed Polydomes |
| Operating Voltage / Current | 30V DC Max, 100mA Max | Low-voltage digital logic, capacitive touch controller ICs |
| Contact Resistance | < 100 Ohms (depending on trace length) | < 10 Ohms with printed silver or gold contacts |
| Ingress Protection Rating | IP65 Dust & Water Resistant | IP67 / IP68 Hermetically Fluid Sealed |
| Operating Temperature | -20°C to +70°C | -40°C to +85°C (Extended Thermal Spec) |
| Switch Life Expectancy | > 1,000,000 Actuations (Metal Dome) | > 5,000,000 Actuations (Non-Tactile / Capacitive) |
Choosing an overseas manufacturing partner requires complete transparency, proven expertise, and flawless quality control. Dongguan Ravo Electronics Co., Ltd. offers over two decades of direct OEM engineering power:
Our engineering team delivers thorough Design for Manufacturability (DFM) reviews within ≤ 2 hours of receiving your CAD/Vector drawings. We support prototype order runs starting from just 1 piece, letting St. George's design teams validate form, fit, and electrical function before committing to mass production tooling.
Every single membrane switch produced in our factory undergoes 100% automated electrical open/short circuit testing, resistance verification, and visual alignment inspection. We perform destructive life cycle testing, actuation force profiling, and environmental chamber testing in-house.
All materials—including inks, spacer films, adhesives, and connectors—strictly comply with ISO 9001 quality systems, RoHS, and REACH environmental standards. Full material safety data sheets (MSDS) and certificate of compliance (CoC) reports are provided with every batch delivered to St. George’s.
We selectively employ premium medical-grade Autotex Polyester (PET) and hardcoated Polycarbonate overlay materials. These films are specifically formulated to resist yellowing, clouding, and cracking when continuously exposed to harsh clinical disinfectants, including 70% Isopropyl Alcohol, bleach (sodium hypochlorite), hydrogen peroxide sprays, and quaternary ammonium compounds.
We accept 2D vector files in Gerber, DXF, DWG, Adobe Illustrator (.AI), vector PDF, or CorelDraw formats. Please include graphic layer artwork, Pantone or RAL color codes, key dimensions, tail pinout assignments, and circuit schematic diagrams. Our engineering response time is within ≤ 2 hours.
Yes! We support custom prototyping runs starting from 1 piece up to 10 pieces. This allows design engineers in St. George’s to test mechanical actuation, electrical continuity, color accuracy, and enclosure fitment prior to full-scale production run approval.
Waterproof isolation is achieved by engineering a continuous perimeter adhesive gasket (using 3M 200MP or 3M 467MP/468MP) surrounding the inner circuit cavity, combined with a sealed tail exit design that prevents moisture from wicking along the silver traces into the main housing.
We supply silver-ink flex tails equipped with standard 2.54mm pitch crimp connectors (Female/Male with latch housings), 1.0mm or 0.5mm pitch ZIF (Zero Insertion Force) bare tails for direct board connector inserting, or custom polyimide FPC tails with gold-plated contacts.
Prototype samples typically ship within 7 to 10 working days following final DFM drawing approval. Standard volume production lead times range from 2 to 3 weeks. Express air freight (DHL/FedEx/UPS) delivers directly to St. George’s within 4 to 7 transit days.
Upload your 2D design files or speak directly with our senior HMI application engineers today. Receive a comprehensive DFM review, material recommendation, and competitive factory quotation within 2 hours.
Get a Quote