EN
 DE
 FR
 ES
 RU
 JA EN DE FR ES RU JA
Precision-engineered graphic panels, membrane switches, and touch controls compliant with international ISO 9001 & IP67 standards.
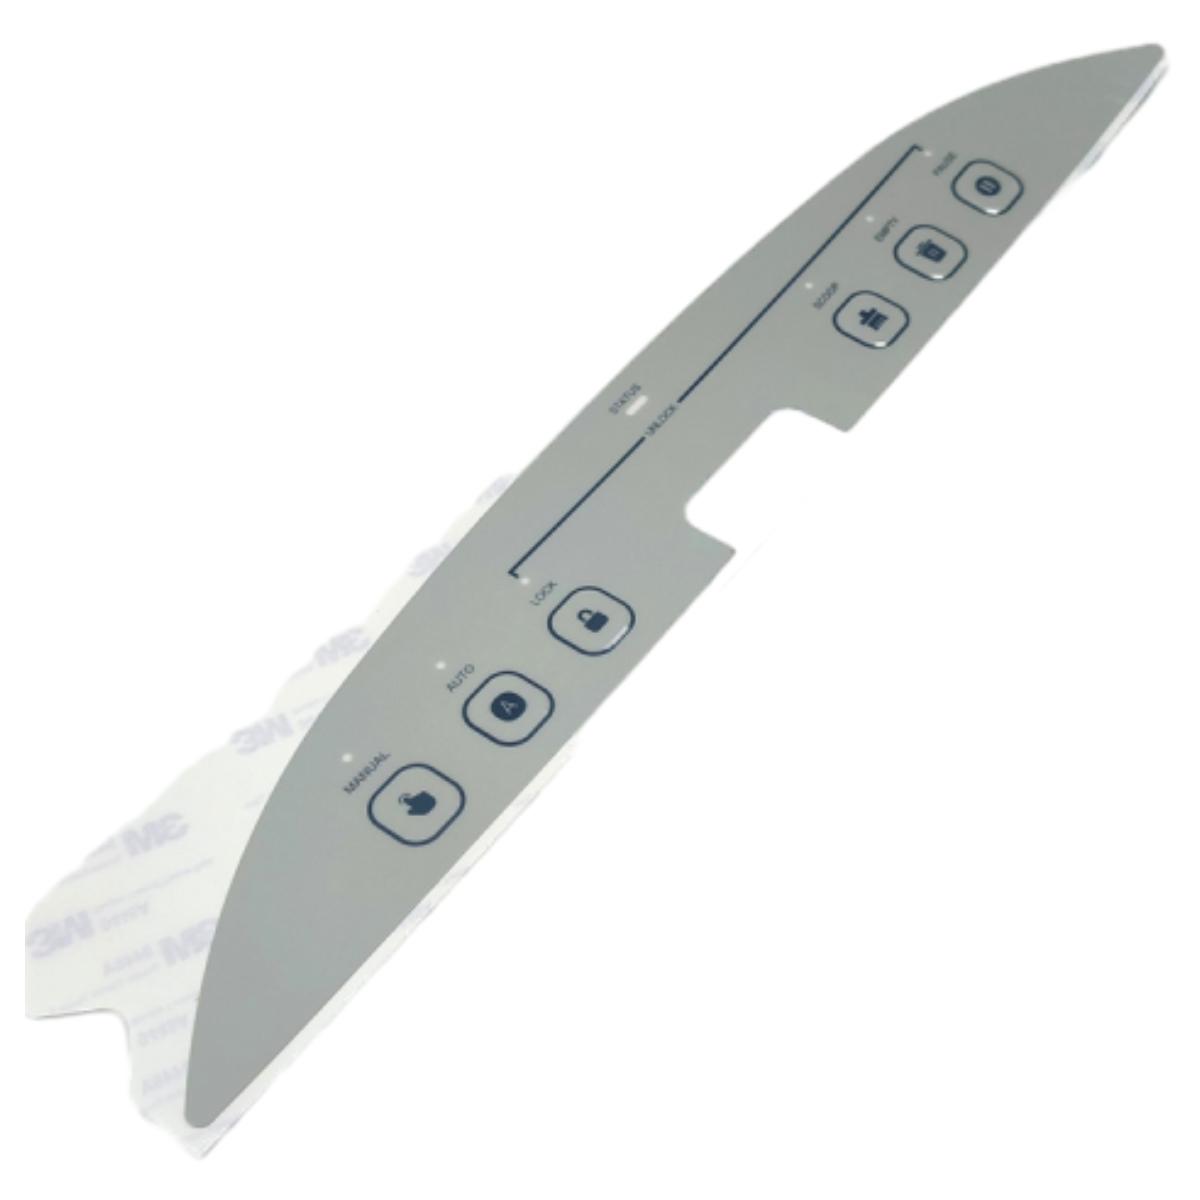
As industrial automation, maritime technology, commercial equipment manufacturing, and renewable power infrastructure expand across Kingston, the demand for high-reliability Human-Machine Interfaces (HMI) has matured rapidly. Original Equipment Manufacturers (OEMs) and system integrators operating in Kingston require control panel overlays that bridge the gap between technical durability and intuitive user interaction.
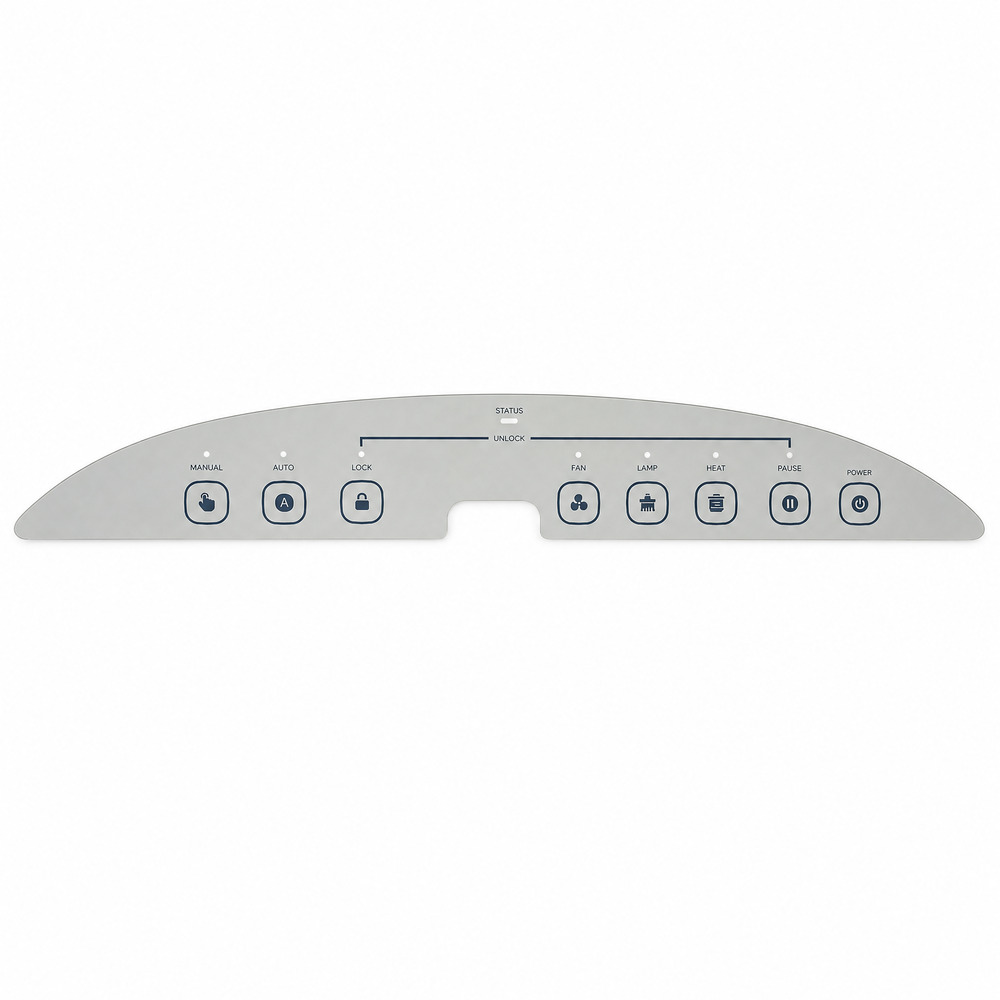
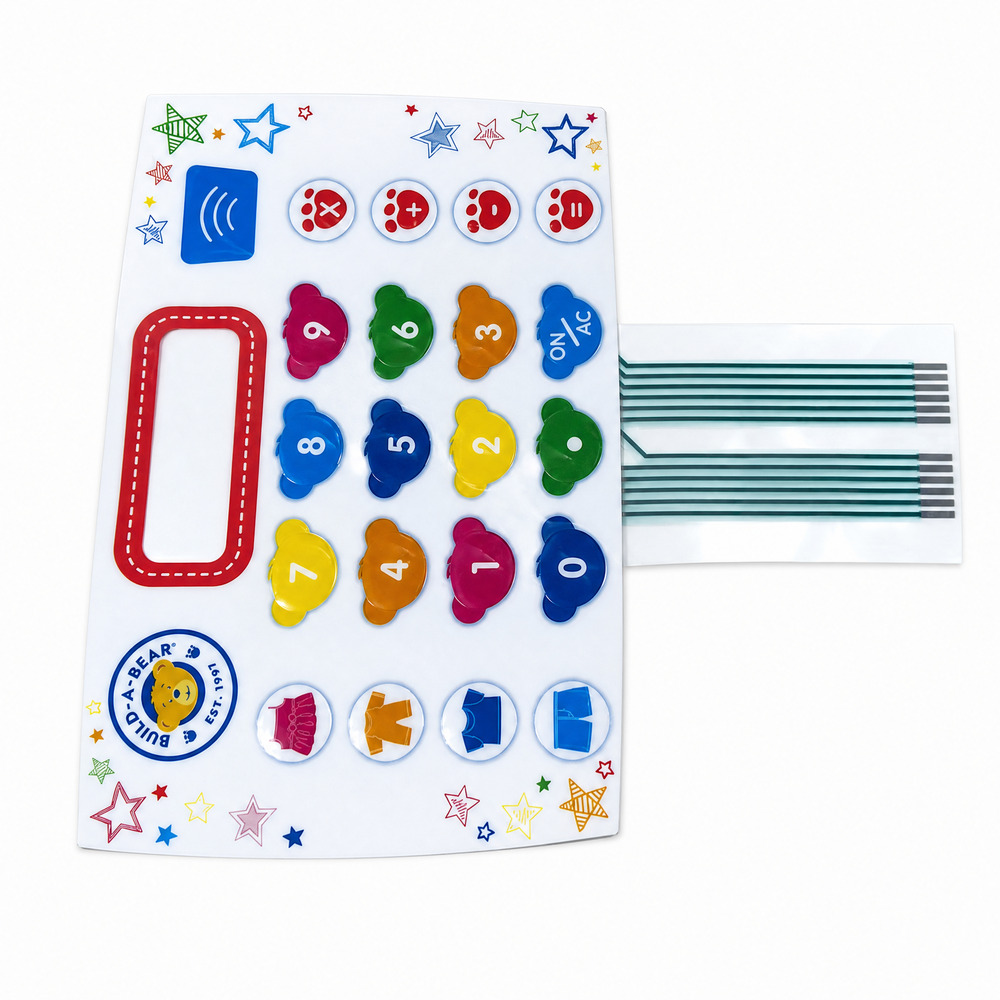
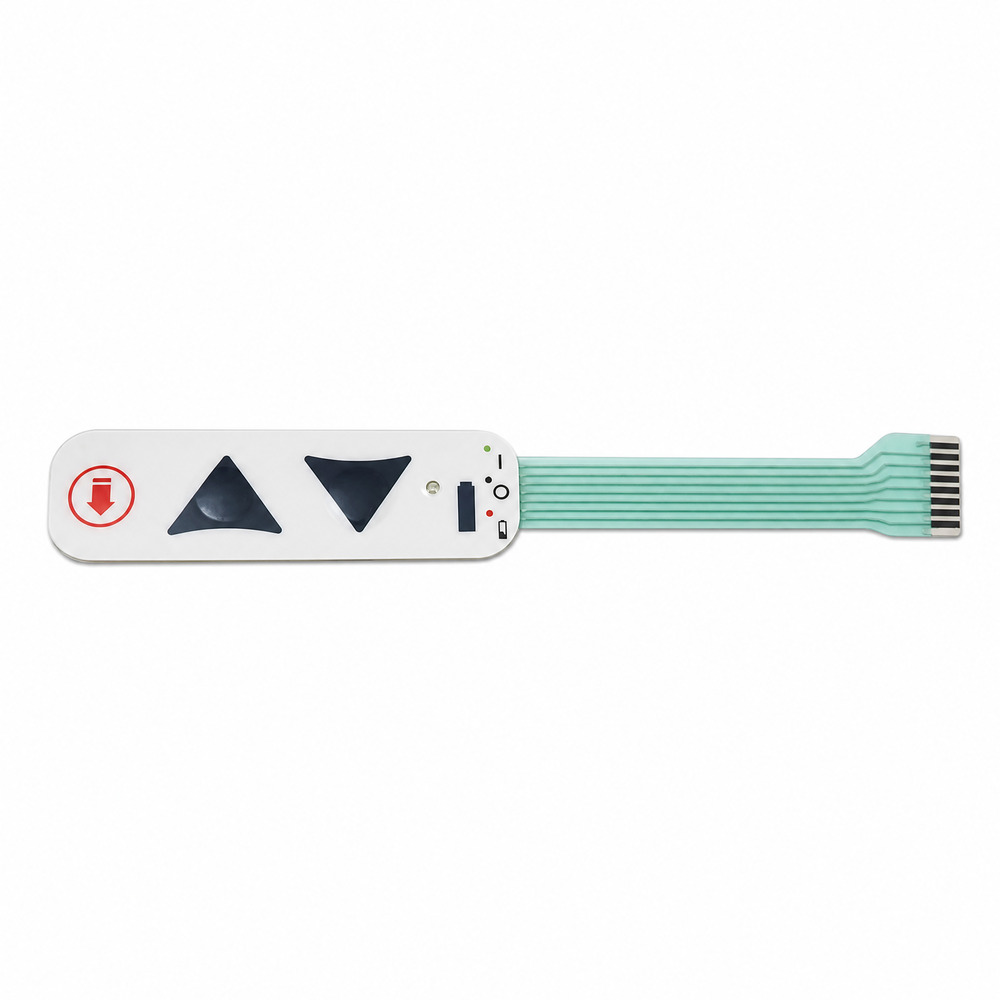
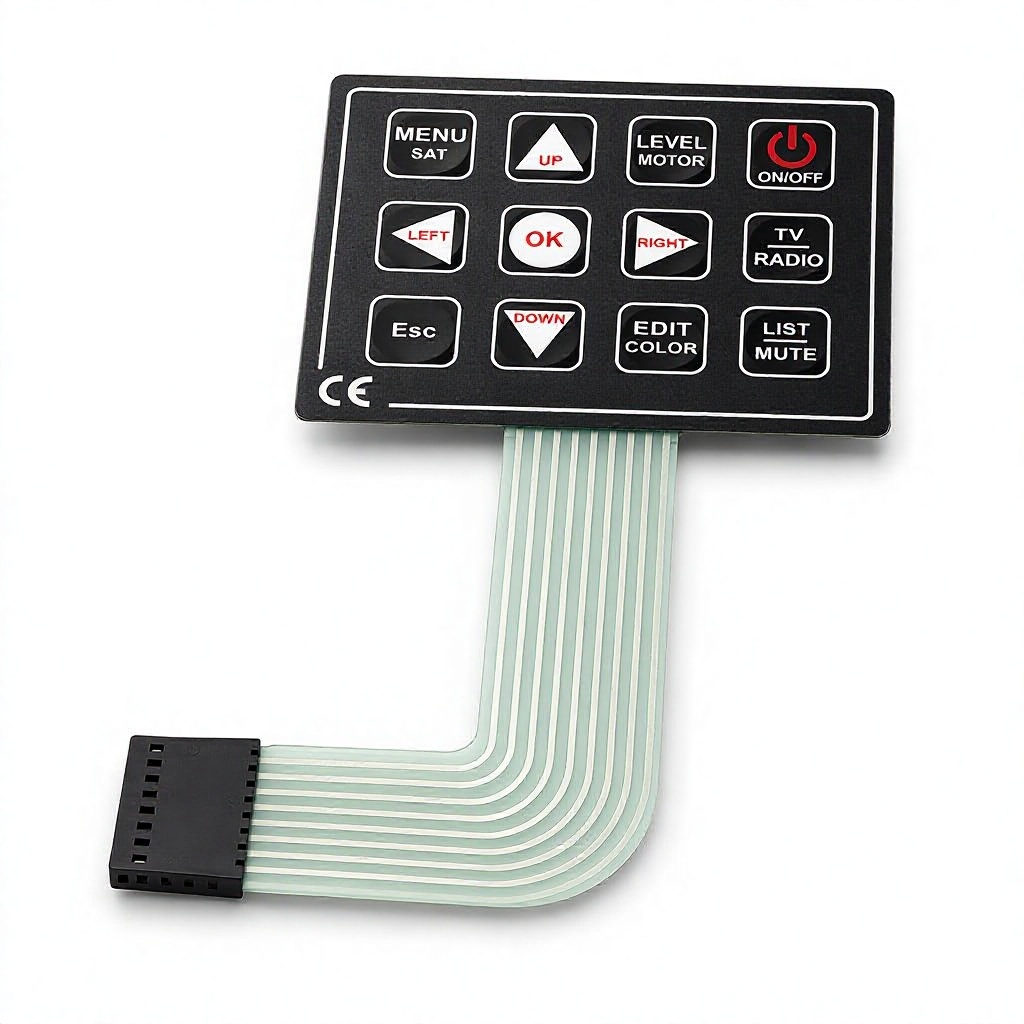
A control panel overlay serves as the outermost interface layer of an electronic device, carrying the essential responsibility of shielding internal circuitry against harsh operational conditions while displaying vital operational legends, LED status windows, and branding graphics. In Kingston’s diverse commercial ecosystem—spanning marine harbor operations, food processing facilities, solar power control rooms, and medical diagnostic centers—control panel assemblies face rigorous environmental stresses including high humidity, solar UV degradation, salt spray exposure, aggressive chemical cleanings, and continuous tactile actuation.
When selecting graphic overlays for equipment manufactured or deployed in Kingston, procurement officers and electrical design engineers must evaluate the fundamental trade-offs between substrate materials:
| Performance Parameter | Polycarbonate (PC - Lexan) | Polyester (PET - Autotex / Melinex) | Acrylic / PMMA Rigid Panels |
|---|---|---|---|
| Flexural Fatigue Life | Moderate (~100,000 actuations) | Superior (>1,000,000 actuations) | Not applicable (Rigid) |
| Chemical & Solvent Resistance | Fair (Susceptible to aromatic hydrocarbons) | Exceptional (Resistant to solvents, alcohols, acids) | Good (Resistant to mild cleaners) |
| UV & Outdoor Stability | Requires UV-stabilized hard-coat | Excellent (UV-stabilized variants like Autotex XE) | Exceptional optical clarity & UV stability |
| Die-Cutting & Machining | Easy, smooth sheared edges | Requires sharp precision tooling | CNC Router or Laser Cut |
| Typical Kingston Applications | Indoor industrial control panels, medical devices | Harsh marine keypads, outdoor power systems | Heavy-duty luxury display overlays, touch panels |
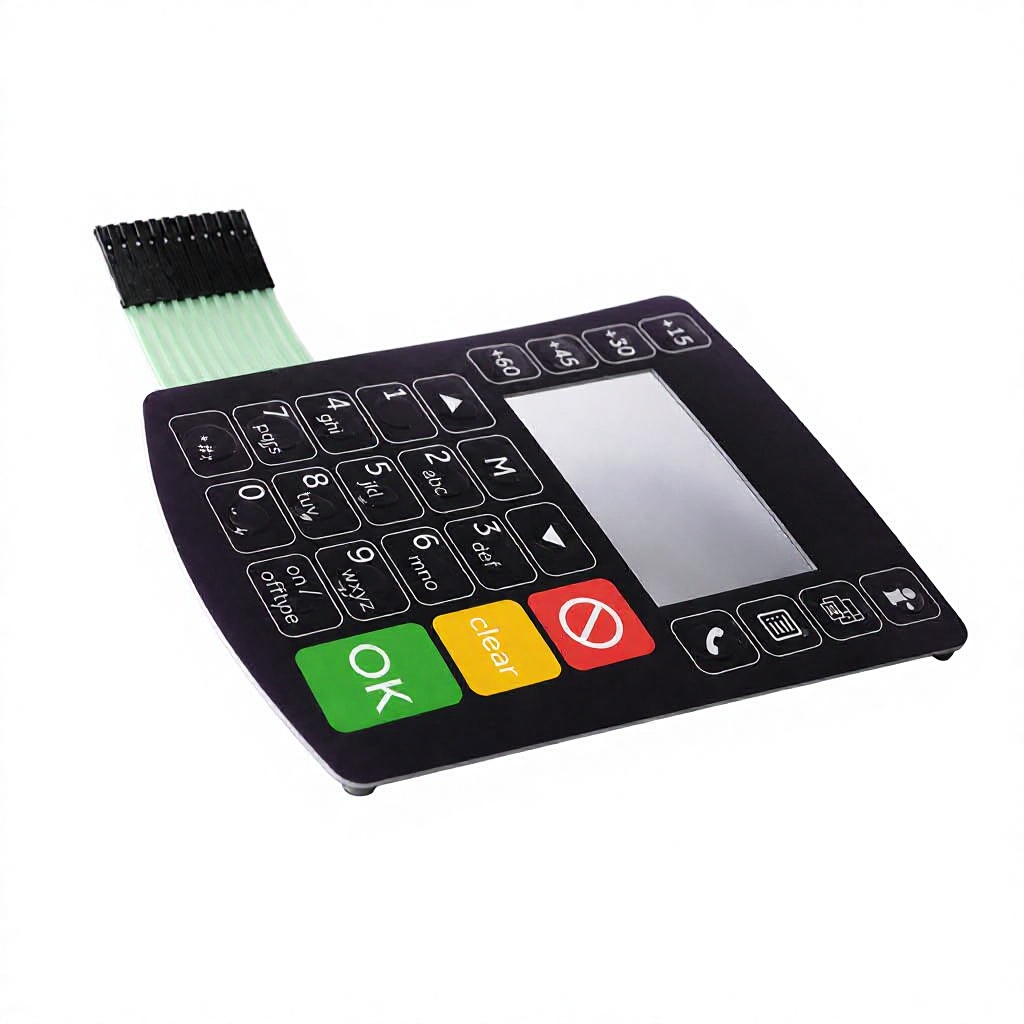
A high-performance control panel overlay rarely acts in isolation. For full HMI integration, suppliers build multi-layer stack-ups engineered to customer specifications. Below is the technical breakdown of a full tactile membrane switch control panel overlay:
Reverse-printed PC or PET film ranging from 0.125mm to 0.5mm thickness. Reverse printing protects legend graphics and custom Pantone colors from surface abrasion and chemical contact.
Application of selective matte/gloss textures and scratch-resistant hard-coats (up to 3H-5H pencil hardness) to optimize optical clarity over display windows while adding tactile anti-glare surfaces to key areas.
High-tack 3M transfer adhesives (such as 3M 467MP or 3M 468MP) precision die-cut with venting channels to secure the graphic panel to the underlying spacer without air trapped under keys.
Integration of stainless-steel metal domes (four-leg or round) or thermoformed polydomes providing crisp tactile snap feedback (actuation force from 160g to 450g) for positive user input assurance.
Screen-printed conductive silver and carbon paste paths on heat-stabilized PET film, or Polyimide Flexible Printed Circuits (FPC), or rigid FR-4 PCB backers carrying surface-mount LEDs and resistors.
Engineered perimeter sealing adhesive chosen for specific substrate mounting (aluminum housing, powder-coated steel, ABS plastic, or textured enclosure bodies) ensuring IP65 to IP67 water/dust entry protection.
Kingston hosts a robust mix of municipal infrastructure, marine port operations, commercial manufacturing, health technology, and energy projects. Custom control panel overlays must meet distinct operational challenges tailored to these local Kingston industrial environments:
Operating near Kingston Port and shipping logistics terminals exposes control interface panels to high atmospheric salinity, intense tropical ultraviolet radiation, and splash hazards. Suppliers serving Kingston marine engineers utilize Autotex XE UV-stabilized polyester combined with full perimeter gasket adhesive barriers. This combination prevents saltwater ingress into internal contact pads, guaranteeing steady operation of crane controls, boat winch remotes, and dockside fueling stations.
Kingston’s local food processing facilities demand hygienic, seamless front interfaces capable of enduring daily high-pressure washdowns using caustic alkaline detergents and hot water. Flat non-tactile overlays or capacitive touch membrane keypads feature smooth wipe-clean surfaces without open crevices where bacteria or food debris could accumulate. Overlay materials are chosen for high chemical resistance against bleach, organic acids, and grease.
With Kingston expanding its green energy footprint, solar inverter manufacturers and microgrid monitoring teams require control panels capable of handling ambient thermal spikes and continuous sunlight. Hard-coated polycarbonate panels with dead-front LED indicator display windows remain crystal-clear without yellowing or cracking under heat, ensuring off-grid operators maintain uninterrupted visibility over voltage ratings and inverter performance metrics.
Hospitals, diagnostic clinics, and research laboratories in the Kingston metropolitan zone require user interfaces meeting stringent antimicrobial and ESD (Electrostatic Discharge) shielding standards. Incorporating printed copper or aluminum foil ESD shield layers safeguards sensitive microcontroller chips against static discharges, while antimicrobial textured PET films withstand rigorous surface disinfections using isopropyl alcohol and hospital-grade germicides.
Procurement strategies among Kingston industrial buyers are undergoing noticeable technological shifts driven by IoT connectivity, miniaturization, and rapid prototyping demands:
Kingston OEMs are increasingly replacing legacy electromechanical push-buttons with capacitive touch membrane keypads integrated under sleek, edge-to-edge acrylic or glass cover panels. These hybrid interfaces provide modern consumer-grade aesthetics with industrial-grade longevity.
Smart pressure sensing technology is gaining traction in local medical monitoring, seat occupancy sensing, and industrial load testing equipment. Printed carbon paste thin-film sensors offer continuous analog pressure detection in low-profile film packages.
Night-time operation of outdoor municipal panels and emergency remote controllers requires low-power illumination. Backlit membrane switches utilizing surface-mount LEDs and uniform light-guide films allow high-visibility key backlighting without substantial heat generation.
Product development cycles in Kingston are accelerating. Local engineers now expect rapid Design for Manufacturability (DFM) feedback and low Minimum Order Quantity (MOQ) prototype batches (1 to 10 pieces) to test functional ergonomics before committing to full production tooling.
Since 2003, Dongguan Ravo Electronics Co., Ltd. has established itself as an international manufacturing benchmark in custom membrane switches, graphic overlays, silicone keypads, and thin-film pressure sensors. Serving clients across Europe, North America, and global industrial hubs like Kingston, Ravo integrates engineering expertise with vertically integrated production lines.
Spanning over 12,000 square meters of specialized plant area, Ravo houses precision screen printing presses, automated digital color matching systems, cleanroom assembly zones, CNC laser cutters, and high-speed embossing presses under one continuous quality system.
Our dedicated engineering desk evaluates buyer 2D/3D drawings (CAD, STEP, DXF, AI, PDF), providing technical Design for Manufacturability (DFM) recommendations, substrate advice, and stack-up proposals within 2 hours of inquiry receipt.
Every control panel overlay and membrane switch assembly undergoes 100% electrical continuity testing, automated optical inspection (AOI), actuation force curve measurement, and thermal/humidity stress sampling prior to export packaging.
All inks, films, spacers, and 3M transfer adhesives used by Ravo comply fully with international RoHS, REACH, and ISO 9001 quality management standards, giving Kingston buyers full audit confidence and regulatory clearance.
Answers to common technical and commercial questions raised by Kingston engineers and purchasing managers during control panel overlay sourcing:
We accept vector graphic files in Adobe Illustrator (.AI), CorelDraw (.CDR), AutoCAD (.DXF or .DWG), and high-resolution vector PDF formats. Please specify Pantone PMS color codes or RAL references for exact color matching.
We recommend heat-stabilized polyester (PET) or UV-stabilized hard-coated polycarbonate substrates combined with high-tack acrylic adhesives such as 3M 467MP or 3M 468MP. These materials prevent edge lifting, graphic yellowing, and adhesive degradation across temperature ranges from -20°C to +85°C.
Yes. Display windows can be crafted crystal-clear, selectively textured, tinted (with custom transparent color fills to match LED segment colors), or given anti-glare finishes. Dead-front windows (where indicator symbols remain invisible until backlit by internal LEDs) are also fully customizable.
For engineering prototypes and pilot production runs, Ravo supports orders starting from as low as 1 to 5 pieces. Volume pricing scales efficiently for larger manufacturing lots ranging from 100 to 10,000+ units.
By implementing a continuous perimeter gasket adhesive, sealed tail exits, and tactile metal dome switch layers, our custom overlays comfortably meet IP65, IP66, and IP67 ingress protection standards, sealing out heavy rain, seawater spray, and dust particles.
We provide rim embossing (raising key borders), pillow/dome embossing (raising the entire button surface), and custom geometric embossing tailored to key shapes. Stainless-steel metal domes (12mm, 14mm, or 16mm) can be embedded to offer crisp, audible tactile tactile feedback upon press.
We provide door-to-door express air freight (via DHL, FedEx, UPS) with transit times typically between 3 to 7 business days to Kingston. Export documentation, anti-static tray packaging, and commercial invoices are handled with full compliance.
Connect directly with Dongguan Ravo Electronics engineering directors. Receive rapid DFM feedback, technical substrate recommendations, and a formal commercial quotation tailored to your Kingston project specifications.