EN
 DE
 FR
 ES
 RU
 JA EN DE FR ES RU JA
Custom-built keypads, backlit membrane switches, and graphic overlays manufactured to exact customer specifications.
As Human-Machine Interfaces (HMIs) evolve across critical industries, backlit membrane switches have established themselves as an essential component for high-reliability, low-light, and variable-ambient operating environments. For industrial designers, electromechanical engineers, and procurement specialists based in Cork and the broader Munster technological cluster, selecting the correct illumination technology directly influences product usability, total system power consumption, thermal management, and long-term switch durability.
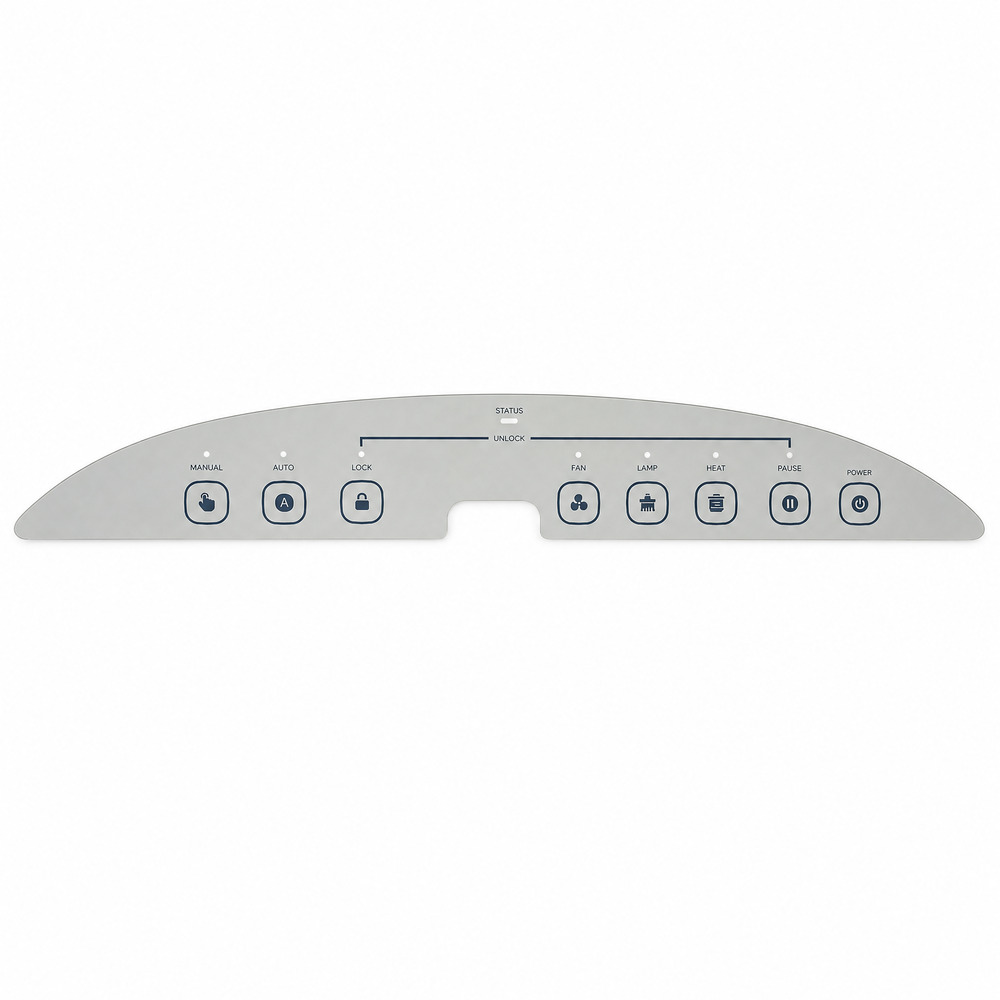
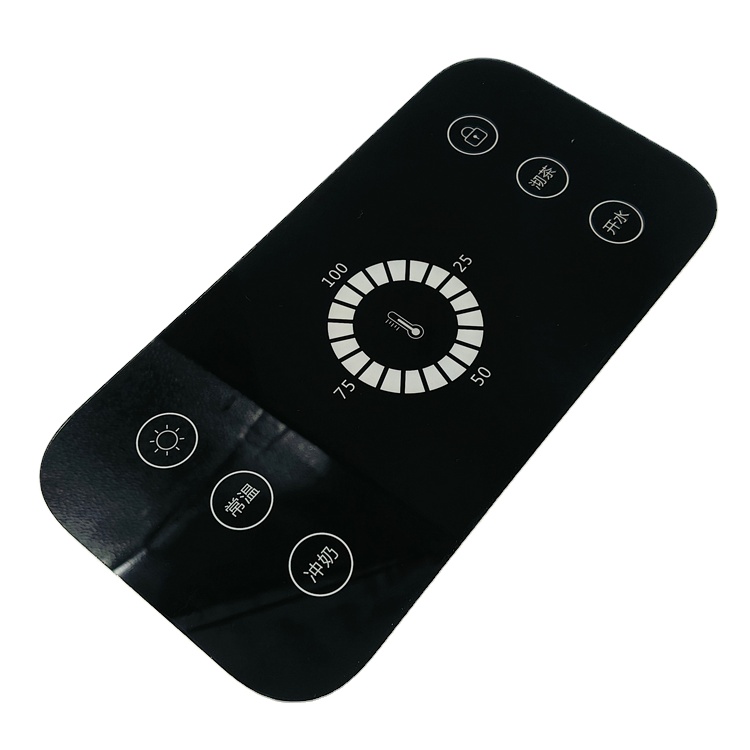
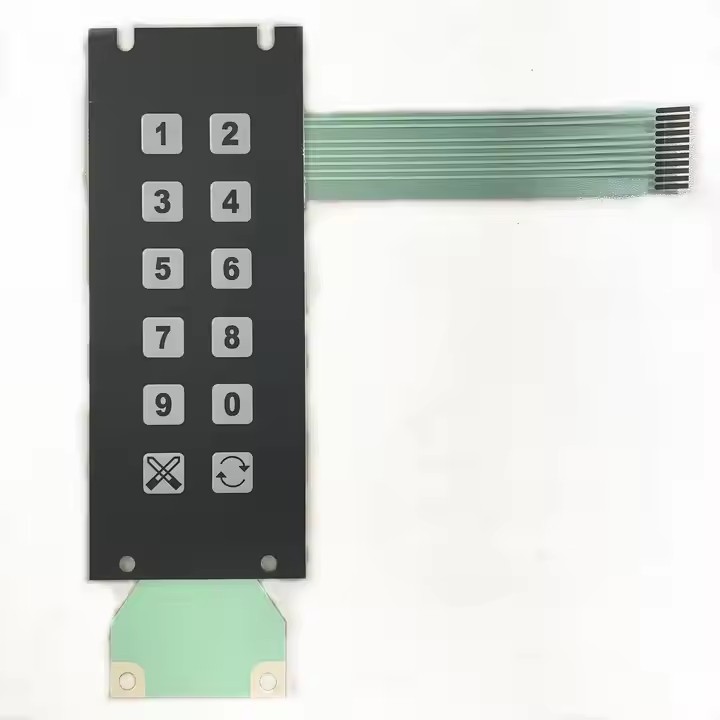
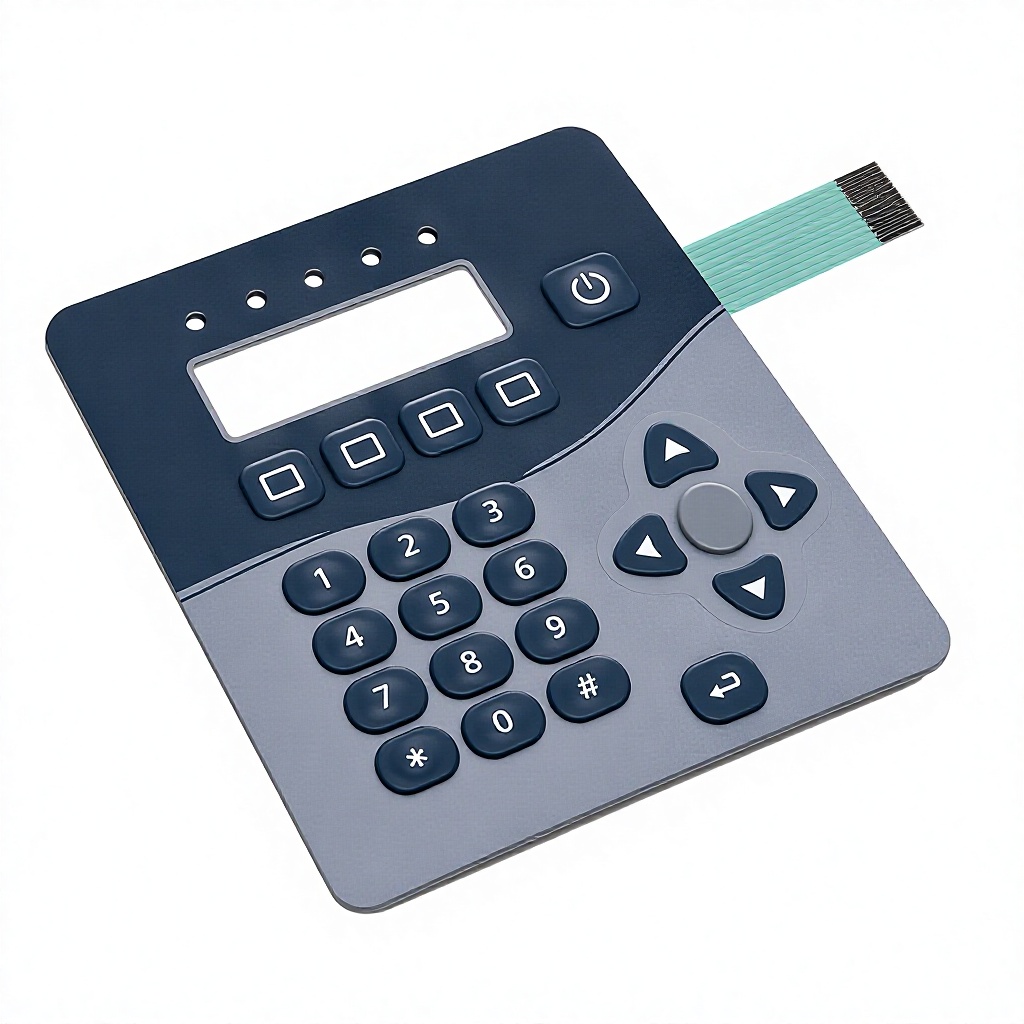
A backlit membrane switch integrates optical light delivery layers directly within a low-profile multi-layer thin-film assembly. Unlike traditional mechanical push-buttons that require bulk LED fixtures or external lightpipes, modern illuminated membrane keyboards utilize thin-profile Surface Mount Device (SMD) LEDs embedded onto Flexible Printed Circuits (FPC), Light Guide Films (LGF), or Electroluminescent (EL) panels to deliver uniform luminance across complex key arrays and graphical icons.
Information Gain Engineering Note: True backlighting performance depends on managing light scatter, internal reflections, and optical crosstalk. Standard surface-mount LEDs can produce localized hotspots if space between layers is insufficient. Advanced LGF implementations redirect light horizontally via micro-etched dot patterns, maintaining total switch stack heights below 1.5mm while ensuring light uniformity exceeding 80% across all illuminated keys.
Depending on the mechanical footprint, ingress protection requirement (IP65 to IP67), and power budget of your target device, Dongguan Ravo Electronics engineers three primary illuminated switch paradigms:
| Illumination Technology | Typical Stack Thickness | Uniformity & Brightness | Power Consumption | Recommended Application |
|---|---|---|---|---|
| Integrated SMD LED Arrays | 1.2mm – 2.5mm | High point-intensity; moderate spot uniformity | Low to Medium (20mA / LED) | Status indicators, localized key backlighting, alert panels |
| Light Guide Film (LGF) | 0.8mm – 1.5mm | Exceptional (80%+ across whole overlay) | Low (Driven by edge LEDs) | Medical diagnostic terminals, darkroom instruments, avionics |
| Electroluminescent (EL) Lamps | 0.5mm – 0.8mm | 100% surface uniform glow | Requires Inverter (AC 80-110V) | Ultra-thin military remotes, low-power night vision equipment |
| Fiber Optic Weave Panels | 1.0mm – 1.8mm | Superior crisp illumination; zero thermal output | Extremely Low (1-2 central LEDs) | Hazardous chemical zones, ATEX cleanrooms, explosive environments |
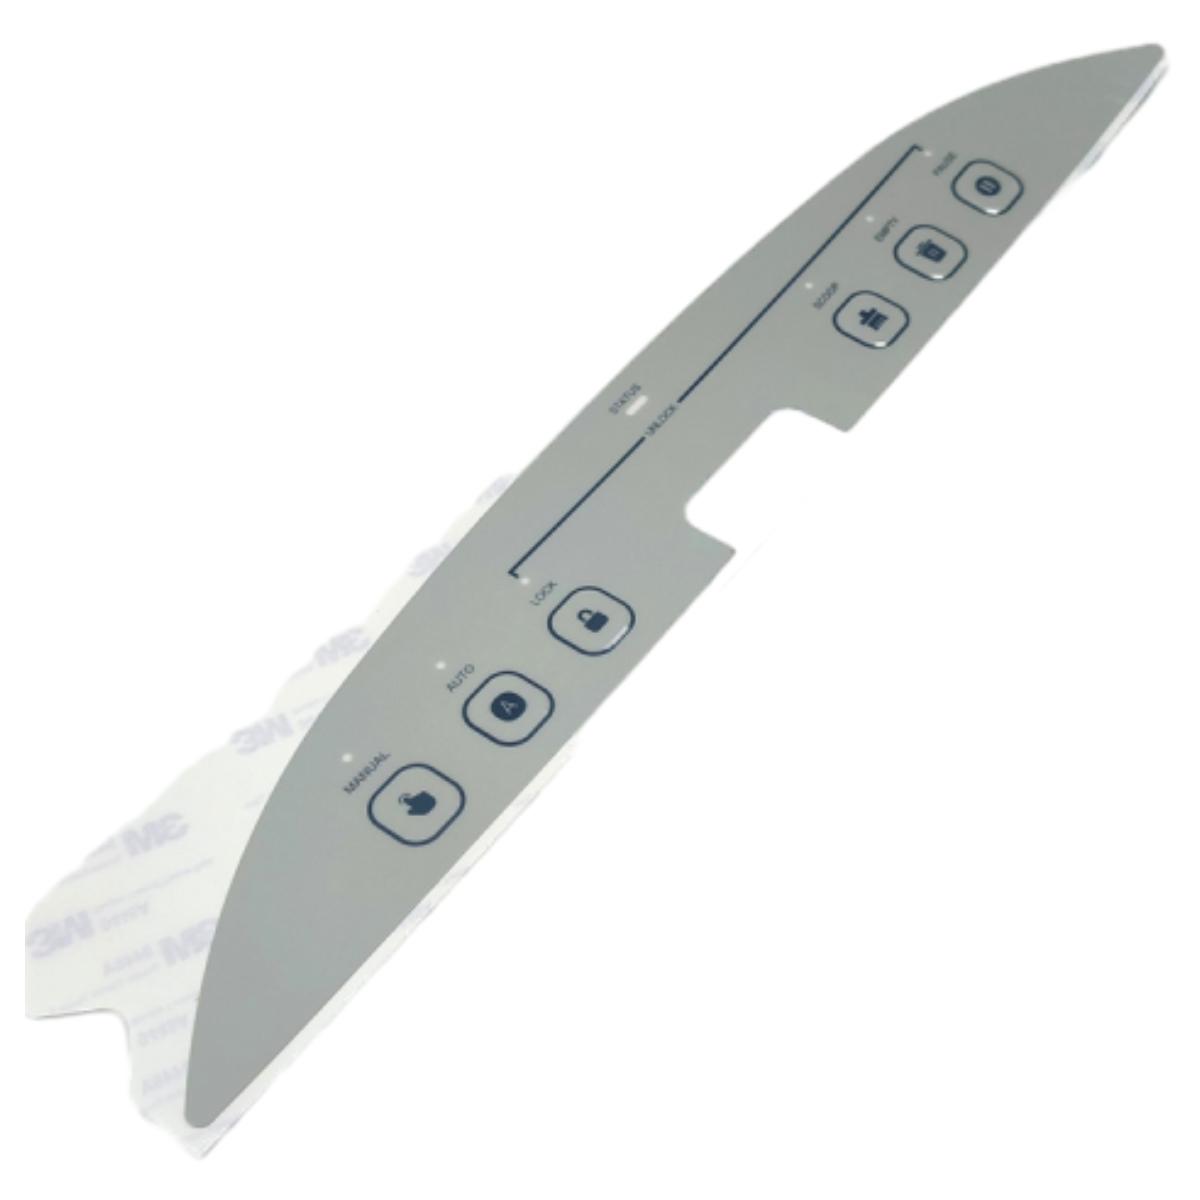
Symbols remain completely invisible or blacked-out under ambient light until backlighting LEDs are energized, creating clean, modern aesthetic control panels.
Full perimeter adhesive gasketing using premium 3M 467MP/468MP adhesives prevents solvent ingress, alcohol degradation, and moisture entrapment down to IP67.
Integrates stainless steel metal domes (122g to 400g actuation force) or thermoformed polydomes for distinct tactile tactile click responses exceeding 1 million cycles.
Tailored HMI solutions designed for the rigorous demands of Cork’s leading technology, pharmaceutical, and marine engineering sectors.
Cork hosts 7 of the world's top 10 pharmaceutical companies. Our backlit switches feature continuous Autotex PET overlays, resistant to aggressive cleaning agents (Isopropanol, Sodium Hypochlorite) with flush surfaces that eliminate biological traps.
Naval, oceanographic, and commercial marine equipment deployed in Cork Harbour require daylight-readable backlighting coupled with IP67 waterproofing and salt-mist resistant seals to survive harsh North Atlantic offshore environments.
Precision diagnostic and patient monitoring devices built in Cork require dead-front illuminated keys, bio-compatible surface materials, ESD shielding up to 15kV, and quiet tactile feedback compliant with hospital cleanroom standards.
Control consoles for agricultural processing, automated filling lines, and outdoor power generators benefit from embossed tactile domes, high-contrast LED status windows, and ruggedized polycarbonate graphic overlays designed for gloved operation.
The industrial landscape in Cork and the Munster province is undergoing a rapid transition towards smart manufacturing, Industry 4.0 integration, and human-centric machine controls. As OEMs shift away from bulky mechanical push-buttons, thin-film backlit membrane switches are seeing accelerated adoption due to several localized trends:
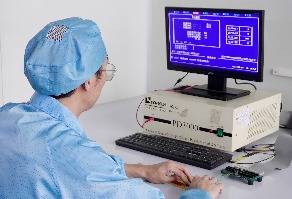
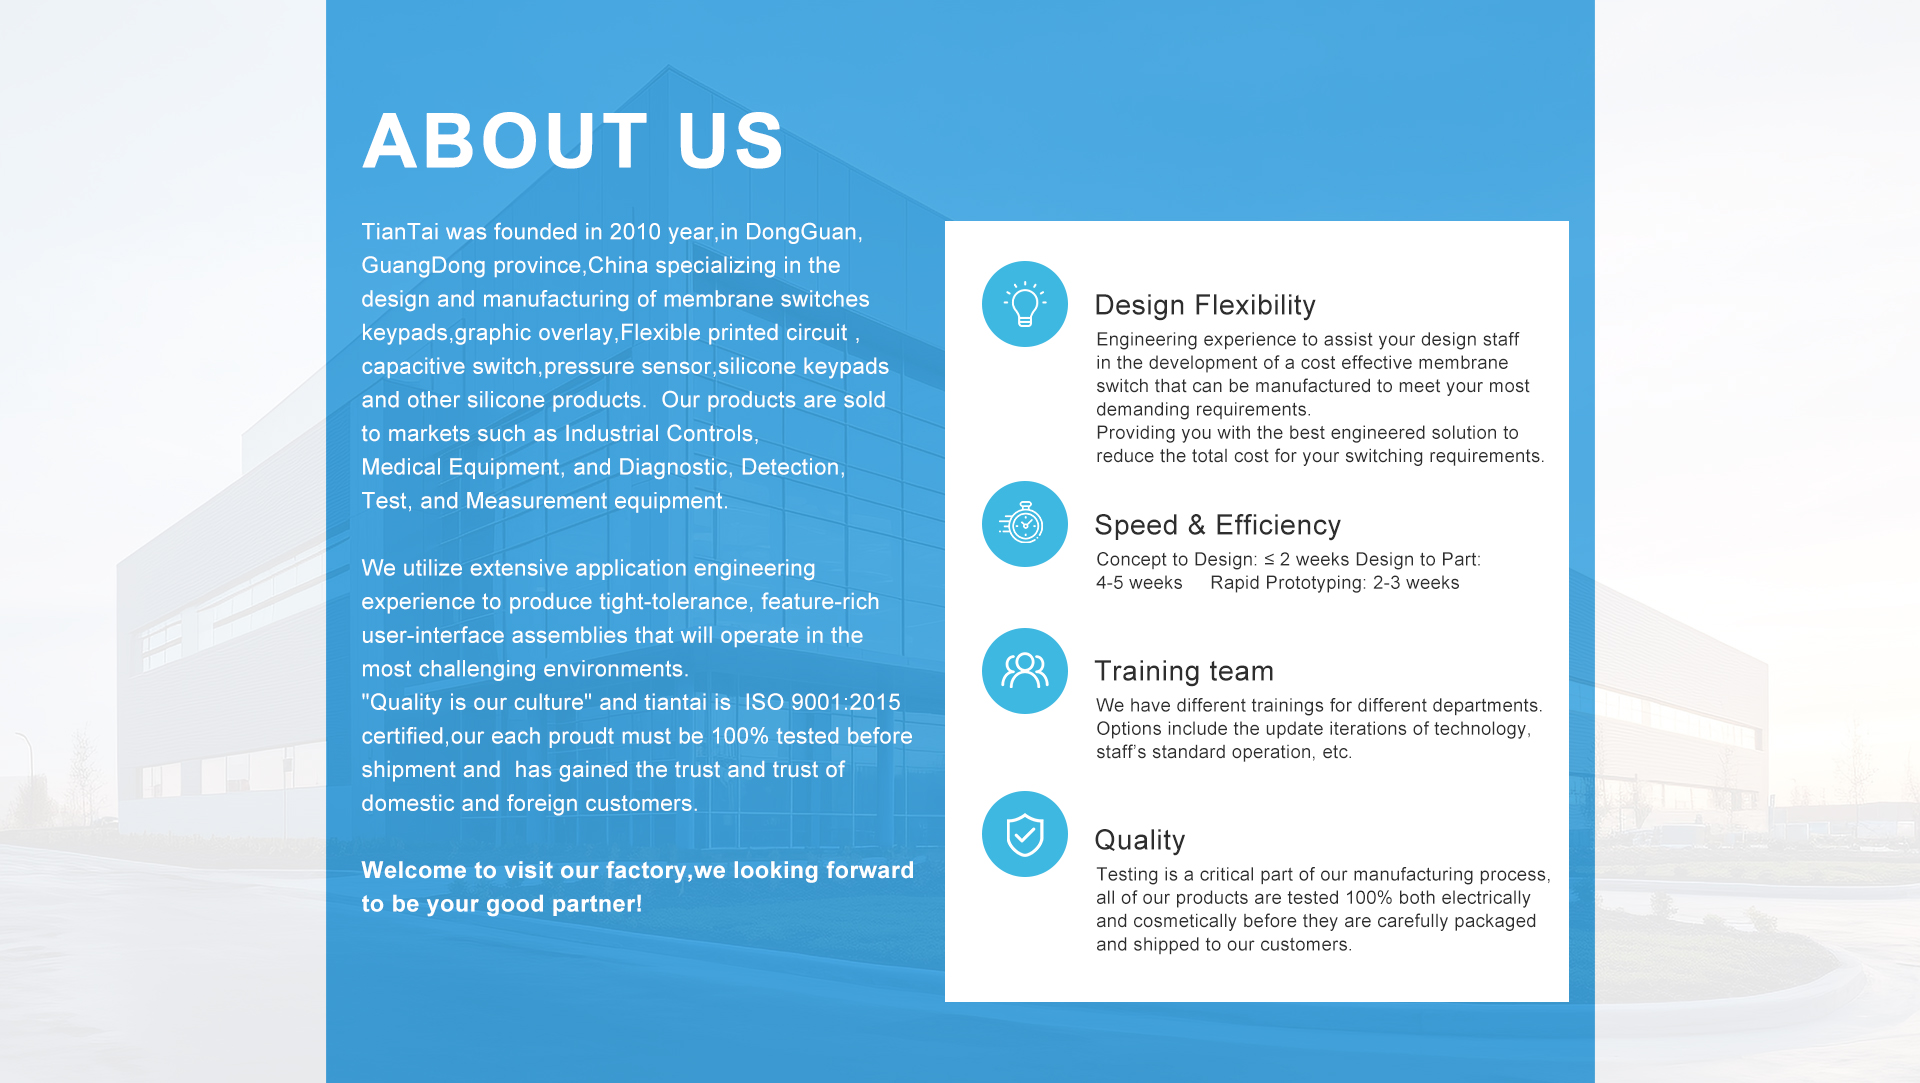
A vertically integrated manufacturer offering end-to-end HMI engineering, rapid prototyping, and direct export capabilities since 2003.
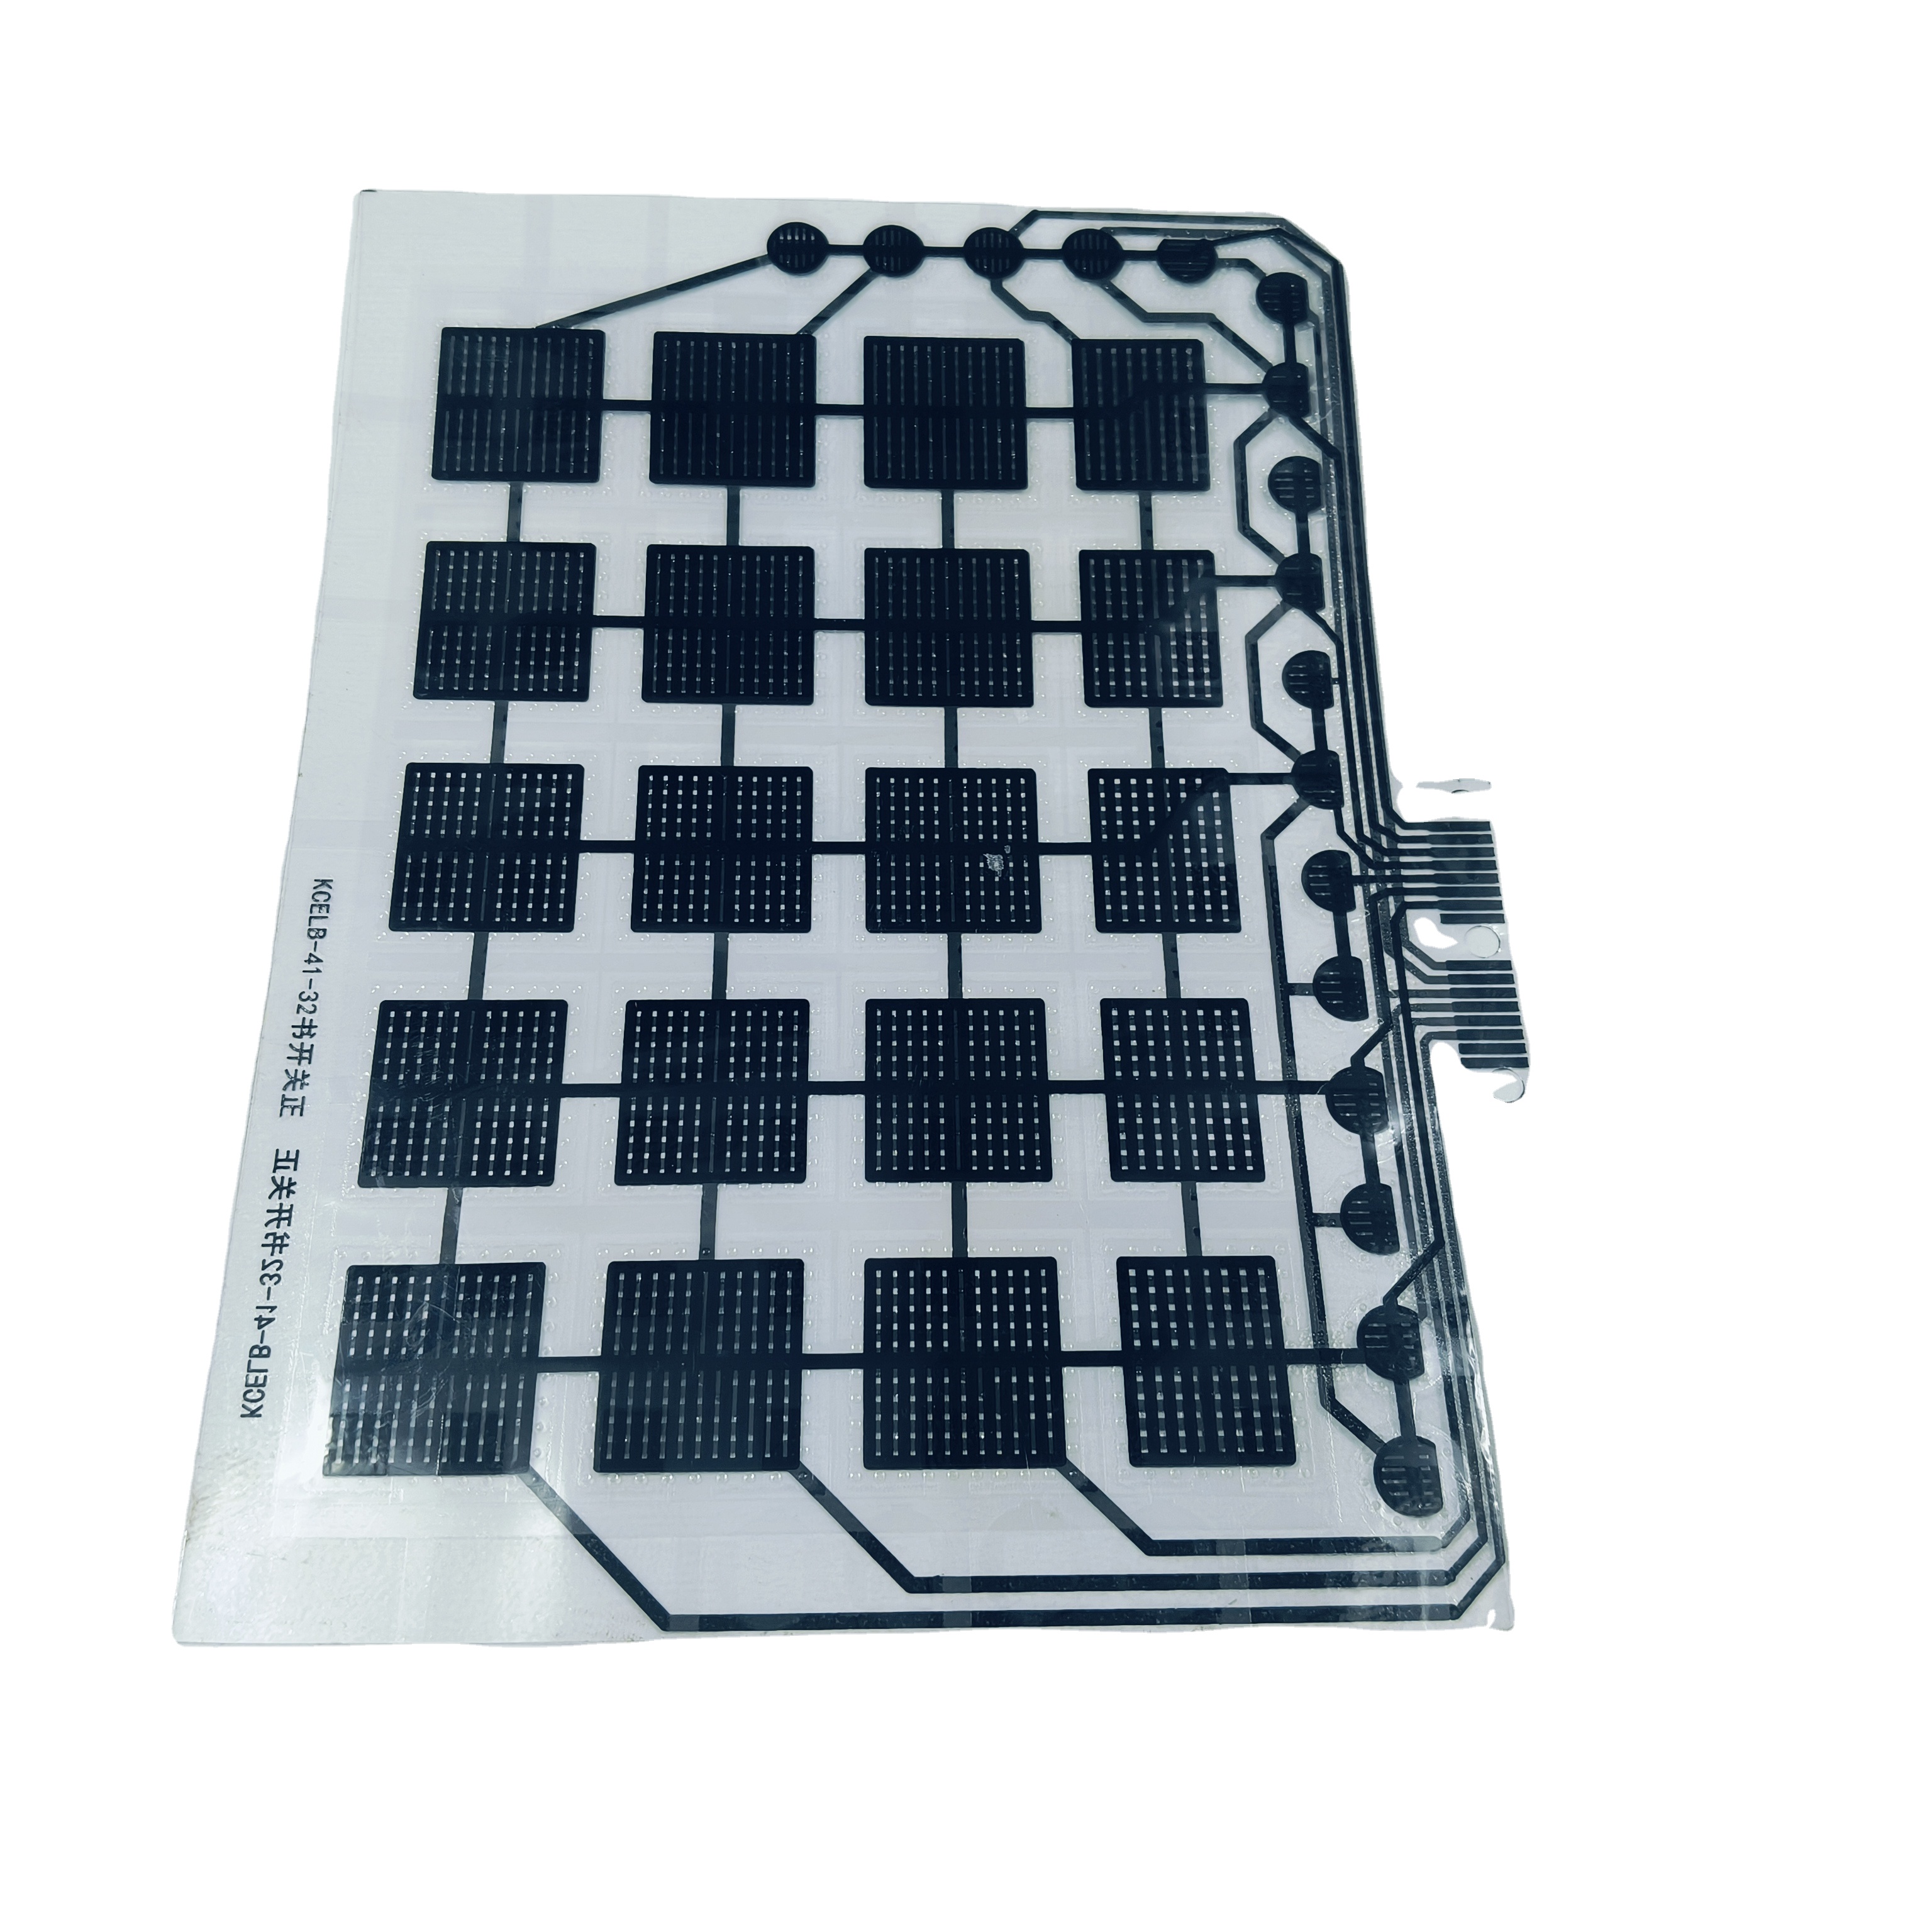
Located in Dongguan, China—the global capital for precision electronics—Dongguan Ravo Electronics Co., Ltd. controls every step of membrane switch fabrication under one roof. From screen-printing silver circuit traces to automated SMT placing of micro-LEDs, laser die-cutting, embossing, and final 100% electrical testing, we deliver factory-direct pricing without intermediary markup.
For engineering teams in Cork, working directly with Ravo means frictionless collaboration. Our technical sales engineers review your CAD files (DXF, DWG, STEP, AI) and artwork within 2 hours, offering DFM (Design for Manufacturability) insights regarding layer stack-up, connector pinouts, tail routing, and light guide optics. Prototypes can be produced in as few as 1 to 5 pieces, allowing physical verification before volume production tooling.
Addressing duty, shipping, technical documentation, and customization requirements for Irish electronics manufacturers.
Once design drawings and Gerber/AI artwork are approved, standard prototype production takes 5–7 working days. Air express courier shipment (via DHL, FedEx, or UPS) directly to Cork, Shannon, or Dublin takes an additional 3–5 working days, delivering tested prototypes to your engineering lab in under two weeks total.
For large panels or keypads with many keys, we utilize Light Guide Film (LGF) optics or multi-zone side-emitting LED channels. Our optical engineers calculate the refraction dot density across the LGF layer to eliminate light falloff, ensuring consistent brightness across all legends with light variance controlled within ±10%.
Yes. We utilize premium textured polyester films such as MacDermid Autotex PET or Bayfol PC, combined with chemically resistant perimeter adhesives (3M 467MP/468MP). This seals the internal conductive silver ink traces and LED circuits against IP67 moisture ingress, bleach, alcohol, and peroxide cleanroom wipes commonly used in Cork medical facilities.
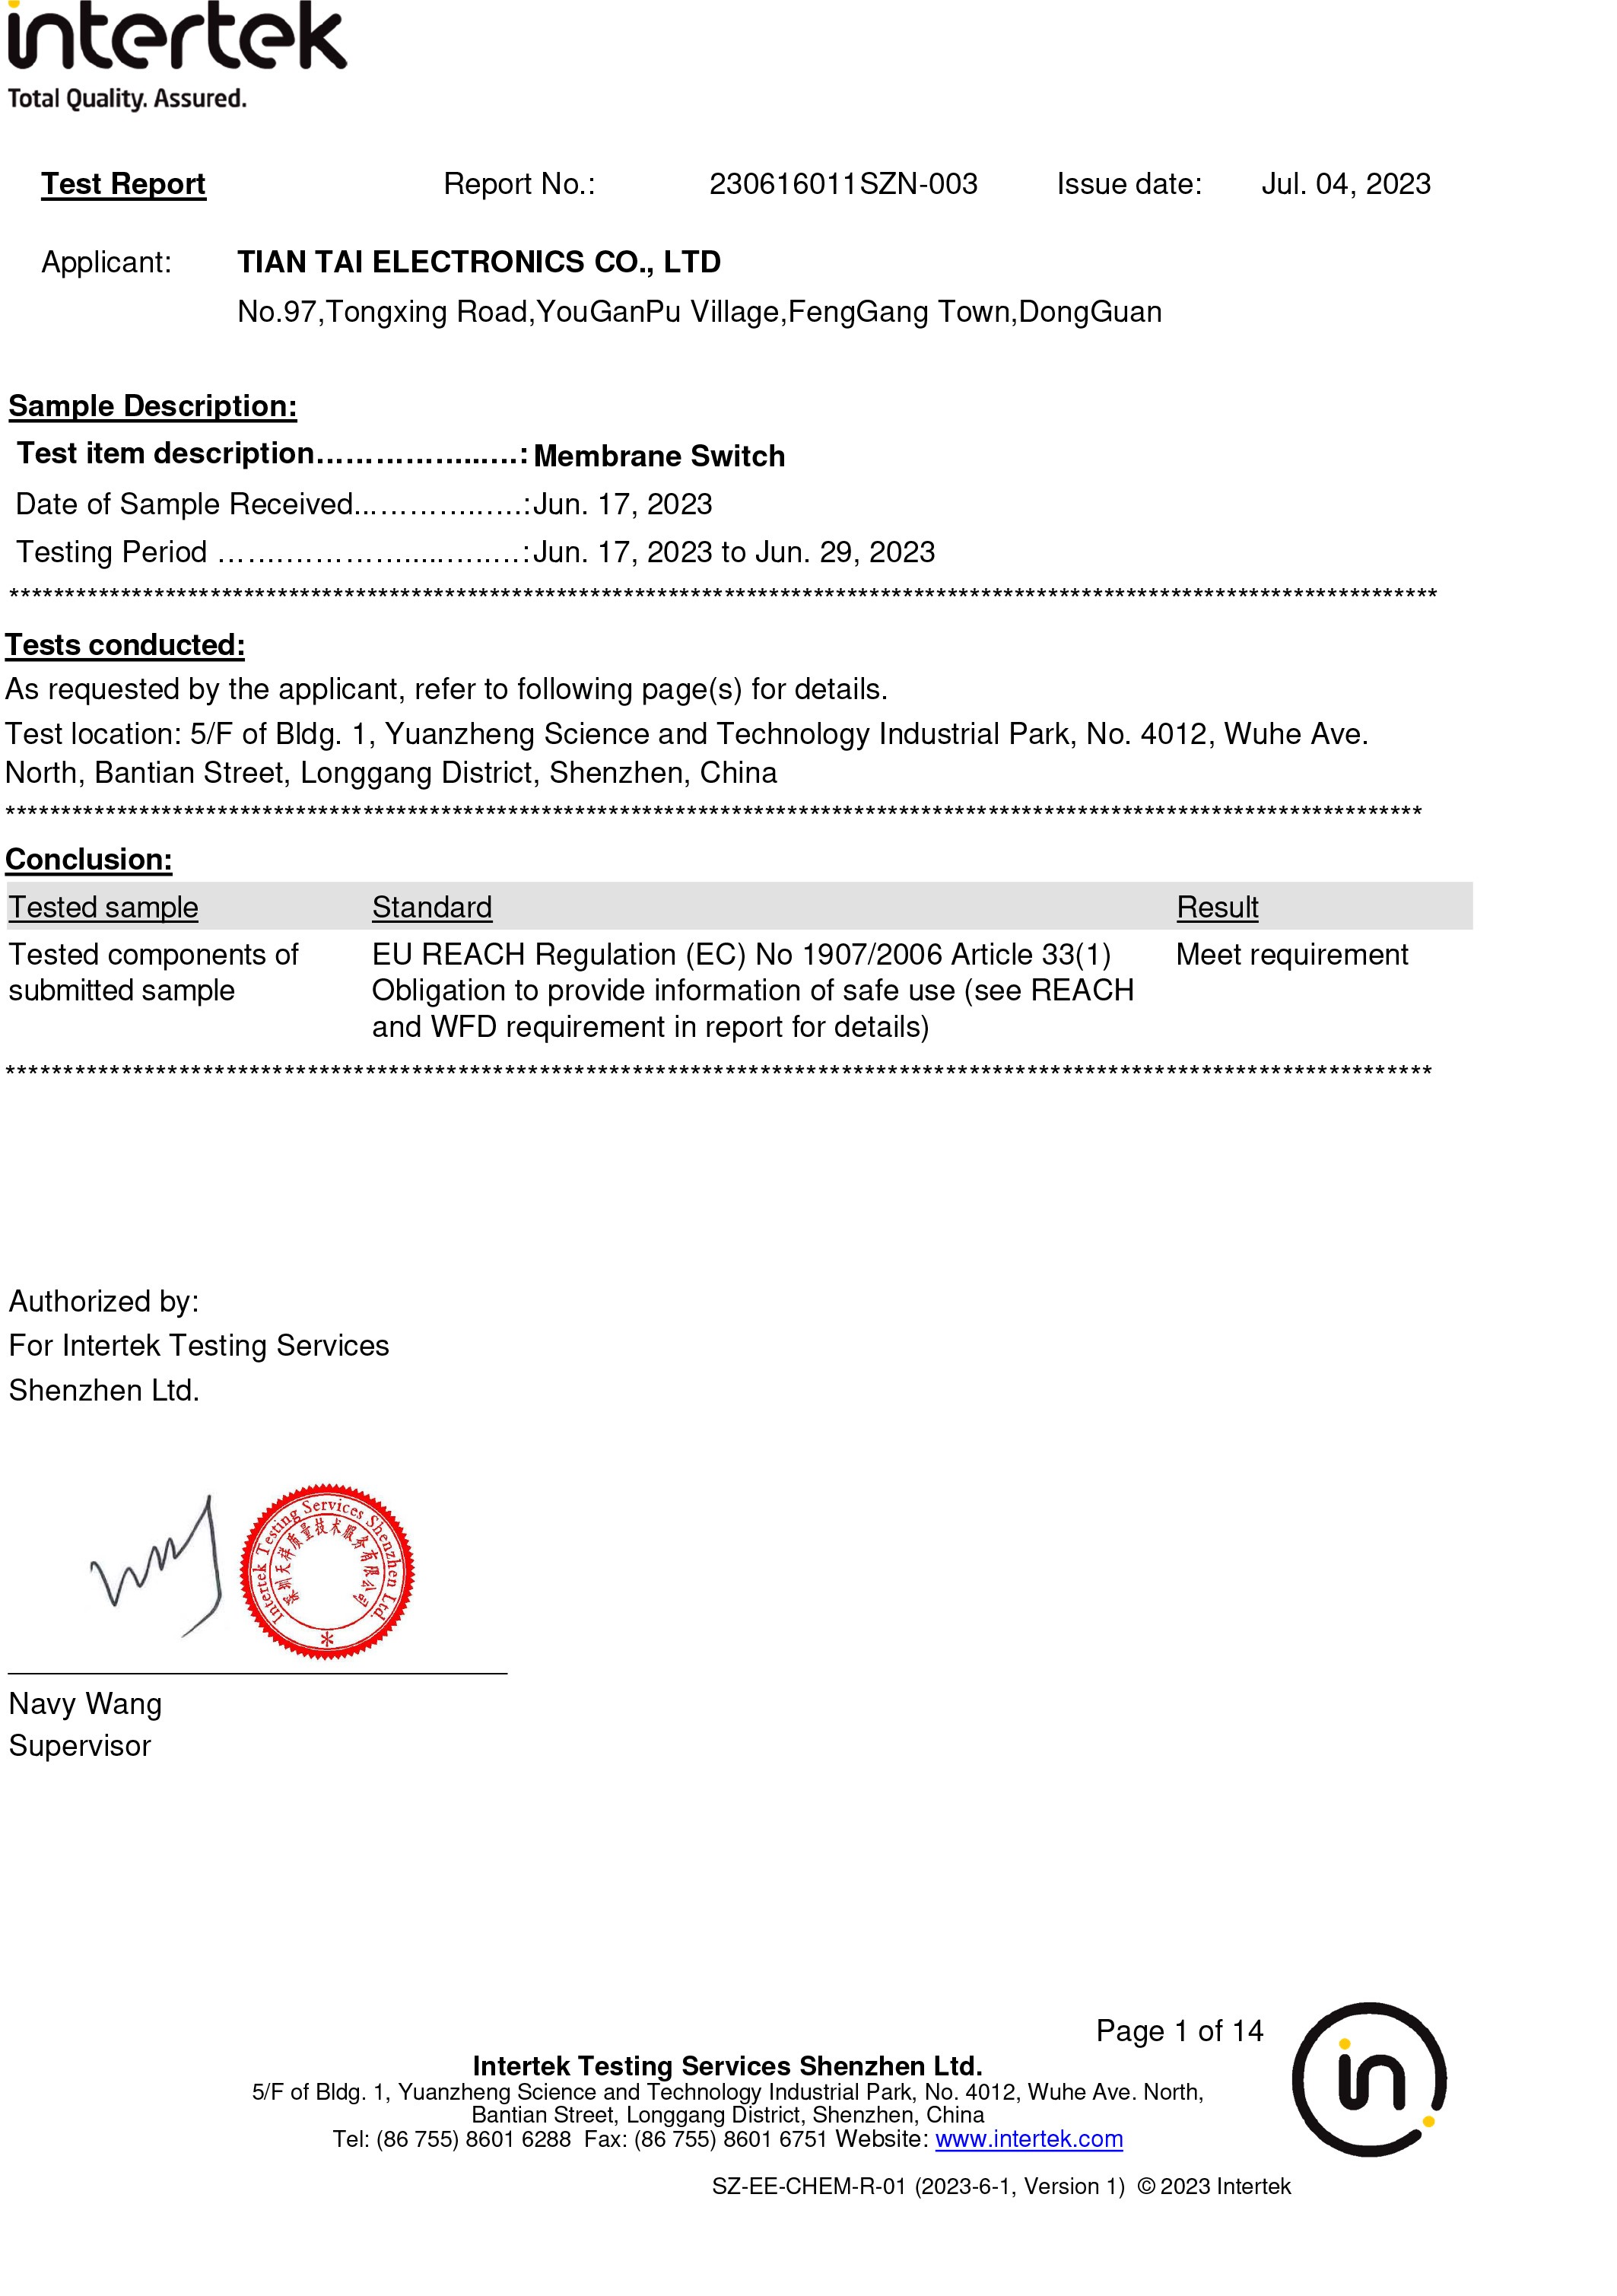
Every shipment to Ireland is accompanied by full material compliance documentation, including RoHS 3 (Directive 2015/863), REACH compliance reports, ISO 9001:2015 quality inspection certificates, and Certificate of Conformity (CoC). We also supply CE compliance data for embedded electronic components.
We offer 2.54mm pitch female crimp connectors (Nicomatic, FCI, AMP), 1.0mm or 0.5mm pitch ZIF (Zero Insertion Force) bare flex tails, and direct solderable Polyimide (FPC) tails. Tail exits can be customized with top, bottom, or side exit locations protected by strain-relief teardrop reinforcement.
You can click the Get Catalog call-to-action button anywhere on this page to immediately open our live engineering support window. Alternatively, email your 2D/3D drawings, artwork, and estimated annual usage to our engineering desk for a comprehensive quote within 2 hours.
Send your CAD drawings or technical requirements today. Our senior engineering team will evaluate your stack-up, suggest backlighting optimizations, and provide a competitive quote within 2 hours.