EN
 DE
 FR
 ES
 RU
 JA EN DE FR ES RU JA
Explore high-durability HMI panels designed for rigorous industrial, medical, and commercial environments.
Why OEM Engineers in Costa Rica are Transitioning from Flexible PET Circuits to Rigid FR-4 Printed Circuit Board Backer Assemblies
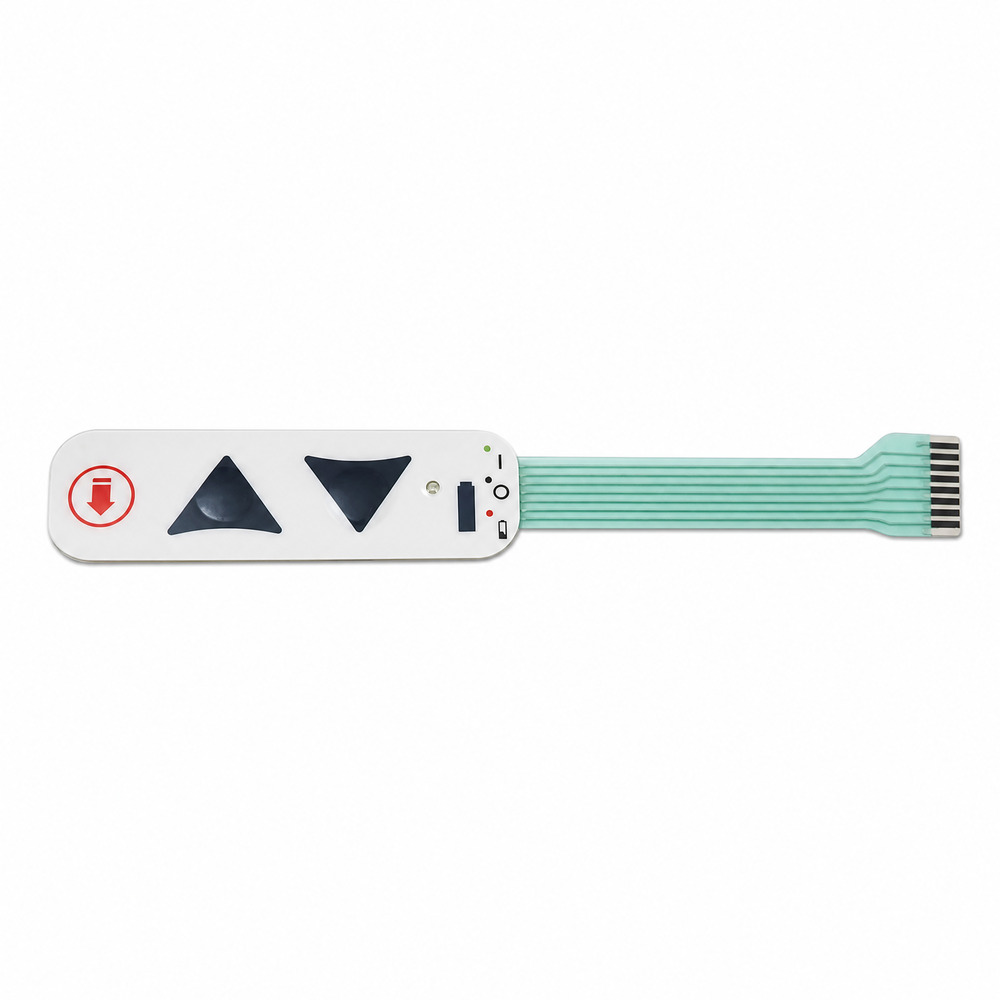
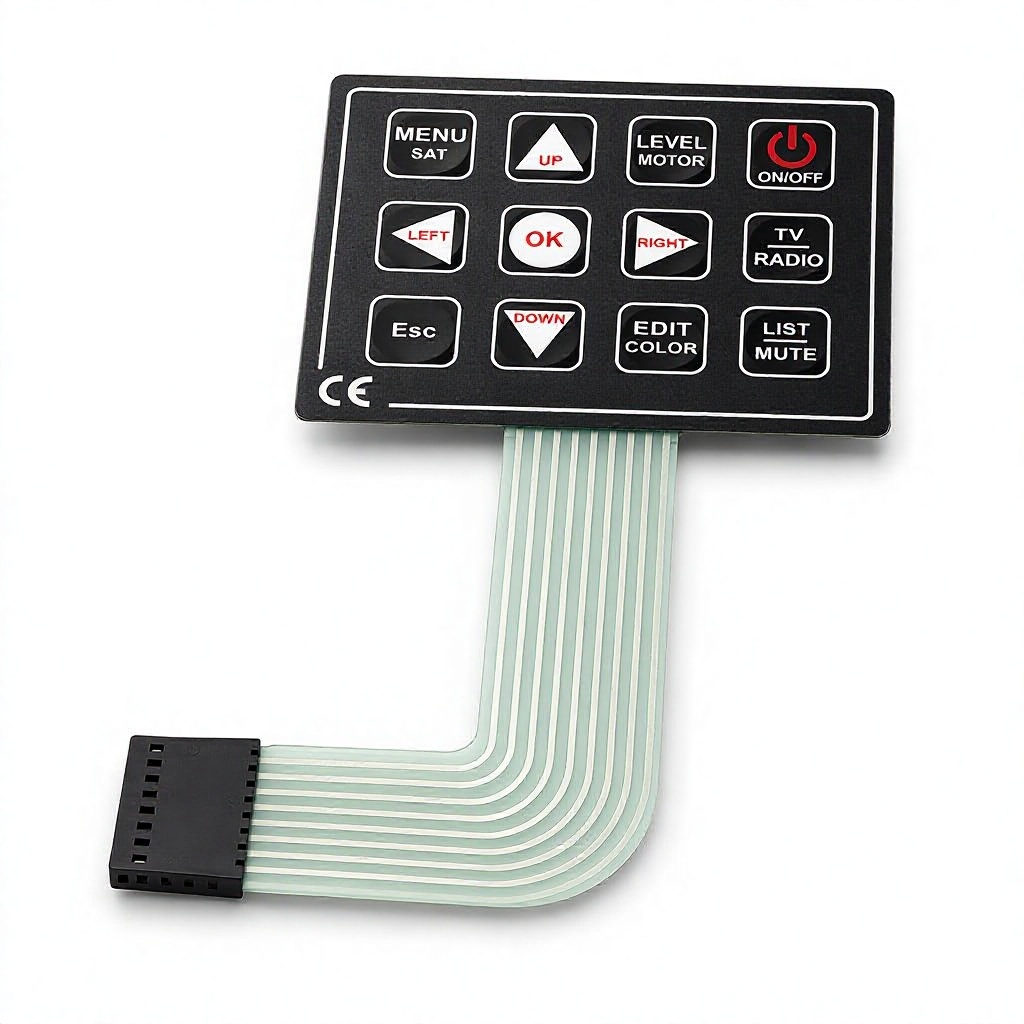
In modern electronic product design, human-machine interface (HMI) reliability determines both field operational uptime and user perception of product quality. While traditional flexible membrane switches utilize screen-printed conductive silver paste on polyester (PET) substrates, advanced industrial, medical, and agricultural applications demand physical structural integrity, high component density, and immunity to environmental degradation. A PCB Backer Membrane Switch addresses these critical demands by fusing a decorative graphic overlay and tactile actuator layer directly onto a rigid FR-4 fiber-reinforced epoxy laminate printed circuit board.
A PCB backer membrane switch is a composite multi-layer HMI unit engineered for demanding mechanical environments. Understanding the exact stack-up is essential for OEM procurement officers and hardware development leads:
Technical Insight for Costa Rican Cleanroom & Industrial Plants: Unlike standard PET membrane switches that require external tail connectors prone to trace fatigue under vibration, PCB backer membrane switches allow robust header connectors, screw terminals, or ZIF connectors to be soldered directly to the rigid board. This design eliminates flexible cable failure in high-vibration applications.
To assist engineering teams in Alajuela, Cartago, and San José in selecting optimal interface architectures, the comparative performance breakdown below contrasts PCB backer switches against conventional PET flexible switches and FPC (Flexible Printed Circuit) switches:
| Engineering Parameter | PCB Backer Switch (FR-4) | Flexible PET Silver Switch | FPC Copper Switch (Polyimide) |
|---|---|---|---|
| Structural Rigidity | Extremely High (Self-Supporting Backplate) | Flexible / Requires Metal Substrate | Flexible / Requires Stiffener |
| Trace Resistance | Ultra-Low (< 0.05 Ω/sq, Pure Copper) | Moderate to High (Silver Paste > 15 Ω) | Low (< 0.1 Ω/sq, Copper Foil) |
| Component Density | High (Dense SMD SMT Reflow) | Very Low (Conductive Epoxy Only) | Medium (Fine-Pitch Soldering) |
| Vibration & Impact Immunity | Superior (MIL-STD-810G Compatible) | Susceptible to Tail Cracking | Good (With Connector Stiffeners) |
| Moisture Migration Resistance | Immune (Solid Copper Traces) | Risk of Silver Migration in High Humidity | Immune (Etched Copper) |
| Connector Termination | Direct Header / Terminal / RJ45 / USB | Female Crimp / ZIF Tail Extension | ZIF / Direct Solder Pin Headers |
| Operating Temperature Range | -40°C to +125°C | -20°C to +65°C | -40°C to +105°C |
Engineering Customized Human-Machine Interface Solutions for Costa Rica's Premier Industrial & Free Trade Zones
Costa Rica has established itself as the leading high-tech manufacturing hub in Central America. With specialized Free Trade Zones (Zonas Francas) concentrated in Alajuela, Heredia, Cartago, and San José, original equipment manufacturers (OEMs) and contract manufacturers require HMI interface components that adhere to stringent international standards while enduring local tropical microclimates. Dongguan Ravo Electronics Co., Ltd. provides specialized OEM engineering tailored to Costa Rica's core sectors:
As Costa Rica's primary export category, medical device manufacturing demands Class 7 cleanroom-compatible control panels. PCB backer membrane switches are extensively utilized in diagnostic equipment, blood analyzers, patient monitoring systems, and surgical tools. Our medical-grade overlays utilize anti-microbial Autotex AM polyester and chemical-resistant coatings capable of withstanding daily sterilization using Isopropyl Alcohol, Bleach, and Cavicide without graphic degradation or seal breach.
From coffee milling and pineapple sorting automated lines to sugar cane refinery control rooms, food processing machinery operates under rigorous washdown protocols. Our IP67/IP68-sealed PCB membrane switches integrate full perimeter hydrophobic gaskets, preventing moisture ingress during high-pressure liquid washdowns while resisting organic acids, oils, and elevated ambient wash temperatures.
Costa Rica runs almost 99% of its grid on renewable energy (hydroelectric, geothermal, wind, solar). Control interfaces on outdoor solar inverters and hydroelectric monitoring units are exposed to extreme tropical solar radiation and heavy precipitation. Ravo supplies UV-stabilized polycarbonate overlays and gold-plated PCB contacts that prevent oxidative corrosion and UV yellowing over 10+ years of continuous outdoor exposure.
Maritime logistics equipment operating at Puerto Limón or Caldera faces intense salt fog and constant air humidity exceeding 90% RH. Traditional silver conductive paste rapidly experiences silver migration and short-circuiting under continuous DC bias in moist air. Our PCB backer switches replace silver paste with etched copper FR-4 traces protected by IPC-CC-830 certified conformal coatings, ensuring zero ionic migration failure.
Market Shifts, Nearshoring Drivers, and Climate-Specific Engineering Considerations for Central America
North American medical and industrial equipment OEMs are increasingly expanding manufacturing footprints in Costa Rica to build resilient, short-haul supply chains. This shift requires component suppliers to offer streamlined engineering turnarounds, rapid prototyping, and full DFM (Design for Manufacturability) support. Ravo supports this nearshoring trend by offering ≤2-hour engineering response times and prototyping cycles from as low as 1 piece, allowing Costa Rica-based R&D teams to accelerate time-to-market.
Modern equipment design is moving away from standalone switches toward fully integrated front-panel modules. Costa Rican buyers increasingly request single-source assemblies that combine the PCB backer membrane switch, integrated acrylic/PMMA display window, embedded capacitive touch ICs, backlighting SMD LEDs, and pre-installed housing studs. Ravo offers complete turn-key manufacturing from mechanical tooling to finished unit assembly.
Designing electronics for equatorial regions like Costa Rica requires specific material selections to prevent field failures:
Two Decades of Specialized OEM Engineering, Vertical Manufacturing Integration, and Quality Control
Founded in 2003 in Fenggang Town, Dongguan, Ravo operates a 12,000m² state-of-the-art production facility housing dust-free screen printing workshops, automated SMT lines, and precision CNC die-cutting machinery.
Our dedicated engineering department reviews your 2D/3D CAD drawings (DXF, DWG, STEP, AI) and returns comprehensive Design for Manufacturability (DFM) feedback and stack-up optimization within 2 hours.
ISO 9001:2015 certified operations. Every produced unit undergoes automated optical inspection (AOI), 100% electrical open/short continuity testing, actuation force verification, and insulation resistance checks.
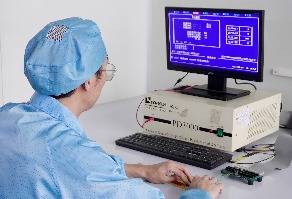
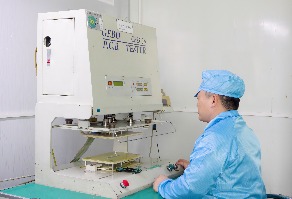
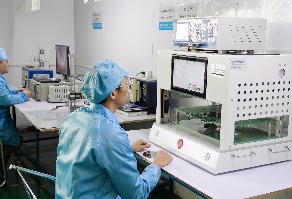
Take a virtual look inside our cleanroom workshops, automated lamination lines, and testing laboratories:
Answers to Common Technical, Regulatory, and Logistics Inquiries from Buyers in Central America
Partner with Dongguan Ravo Electronics Co., Ltd. for direct factory pricing, rapid engineering response, and world-class PCB backer membrane switch manufacturing tailored for Costa Rica and global markets.