ISO 9001
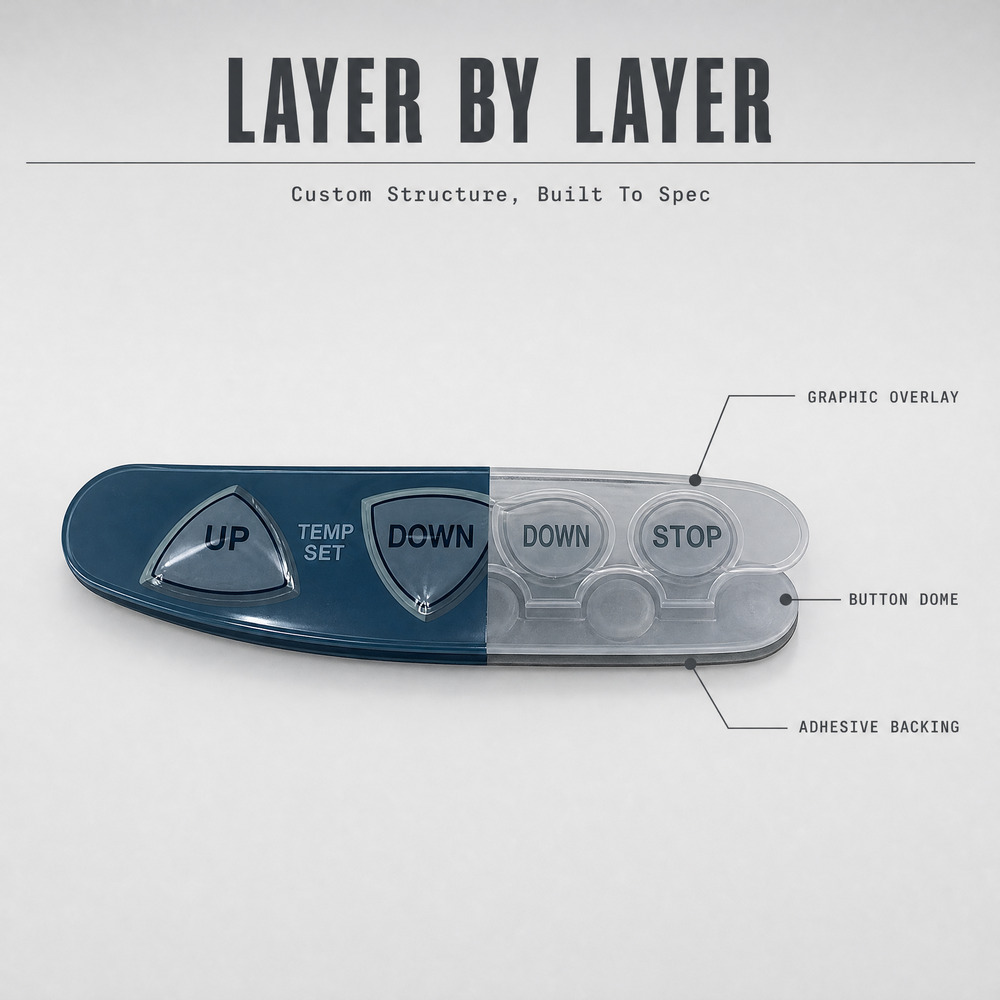
Custom Membrane Switch Silicone Overlay for Remote Controller
- Actuation Life: >1,000,000 Cycles
- Substrate: Silicone Rubber + PET Matrix
- Finish: Matte Soft-Touch UV Protective Polyurethane
 EN
 DE
 FR
 ES
 RU
 JA
Explore 8 standard and customized baseline constructions reordered by global OEM/ODM equipment manufacturers. Each assembly is fully customizable in tactile travel, substrate chemistry, IP sealing, and connector pinouts.
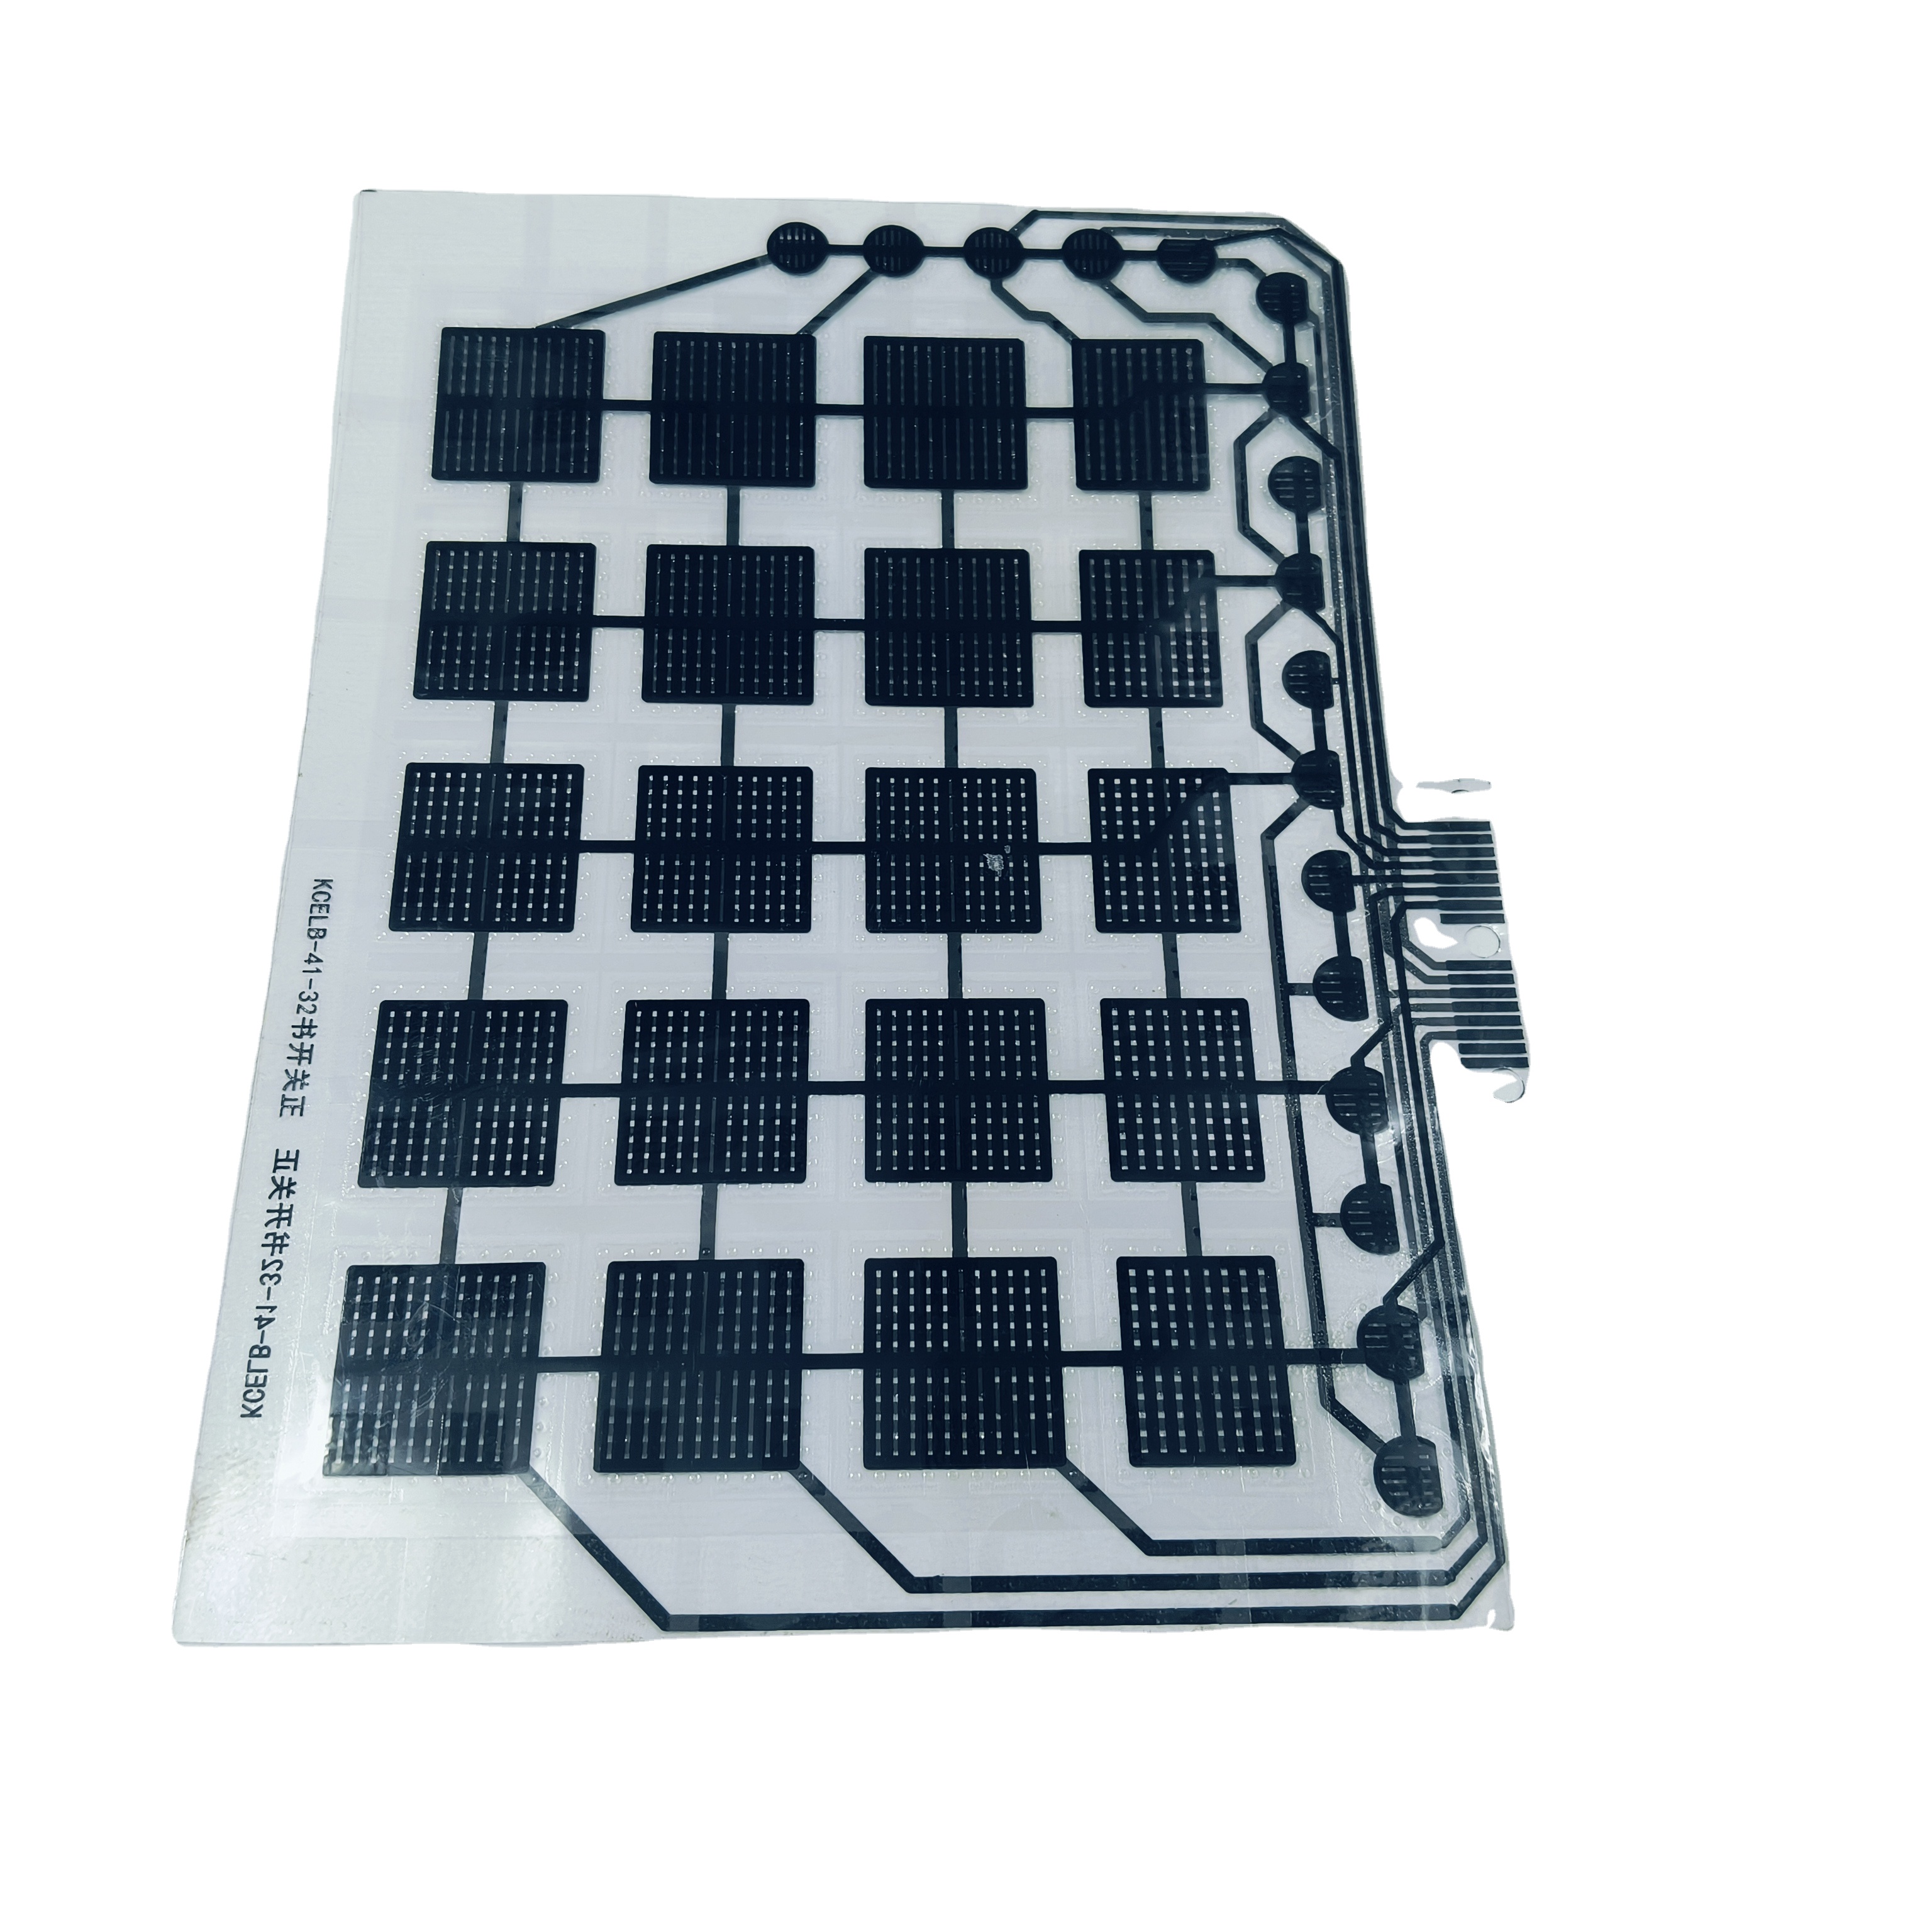
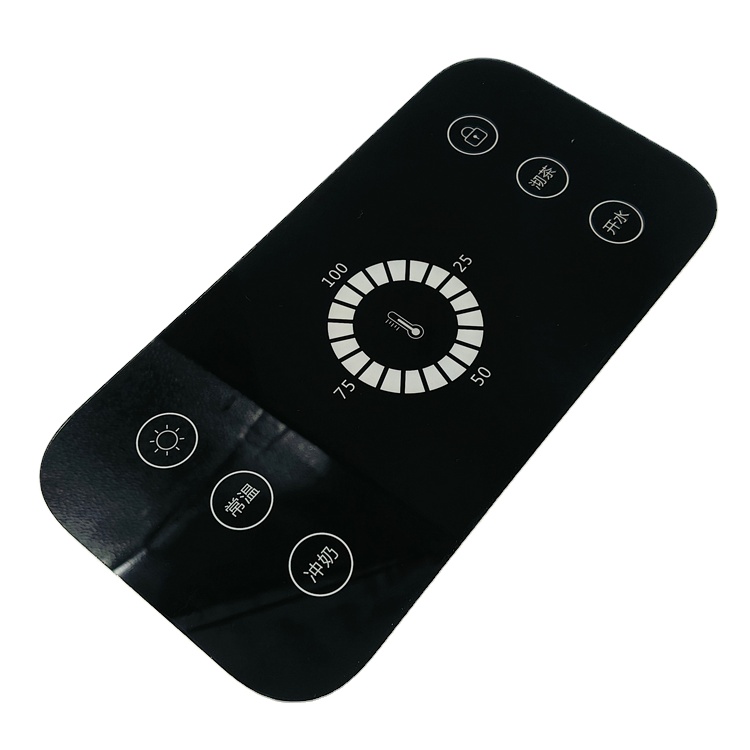
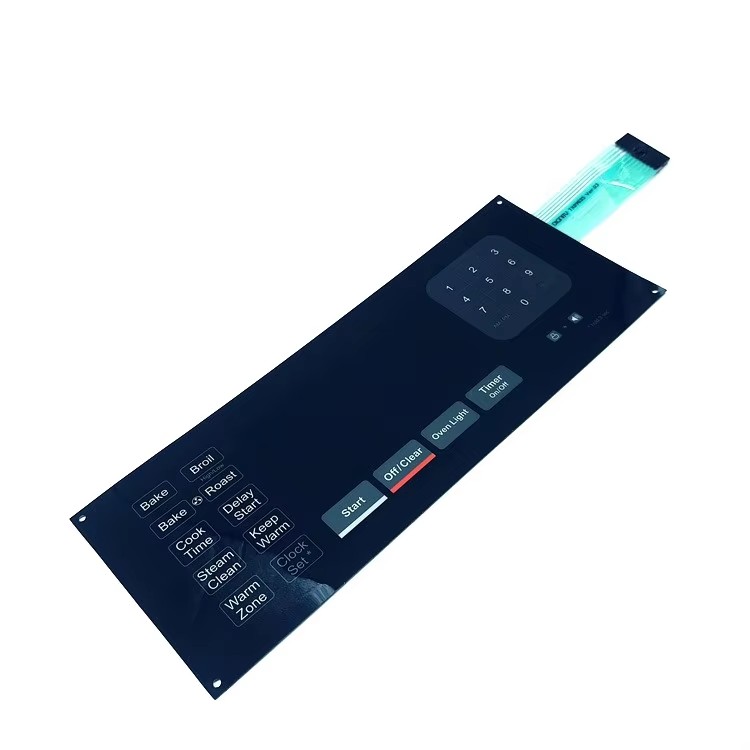
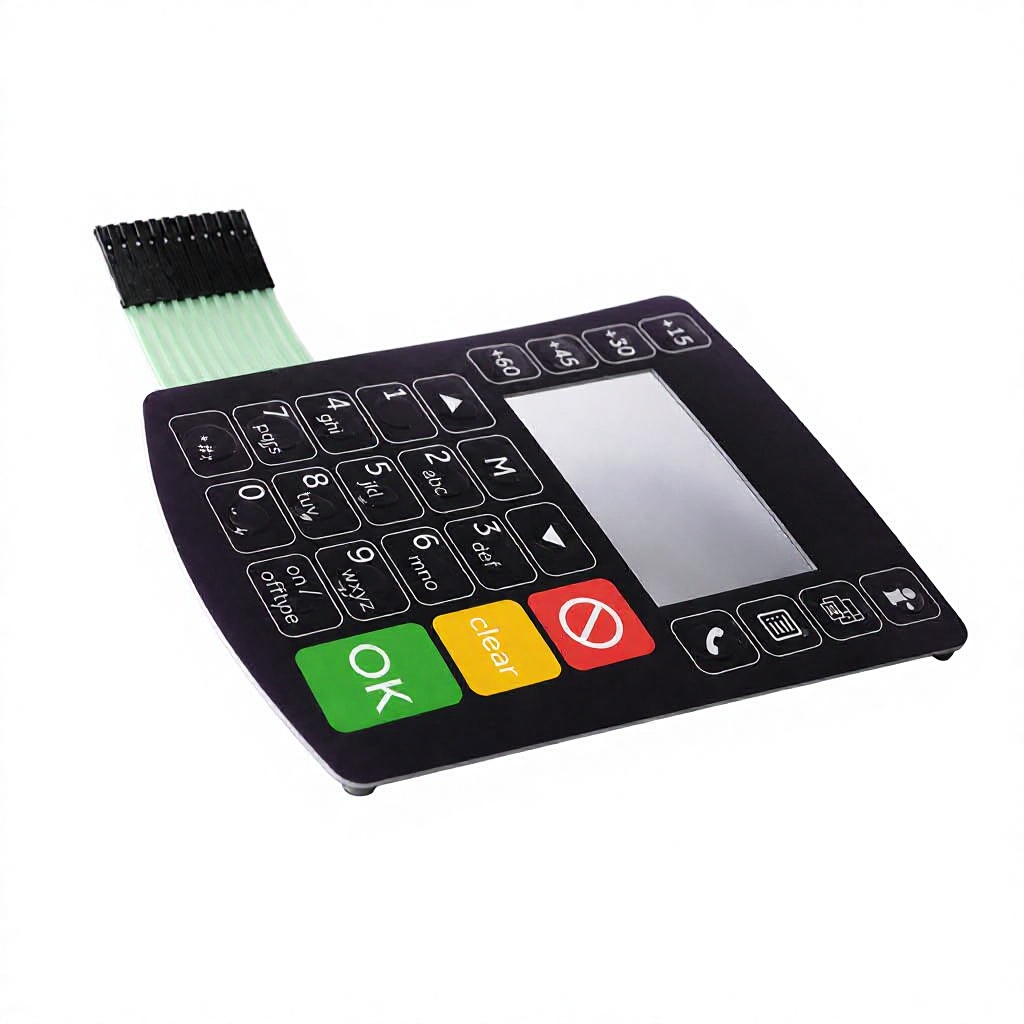
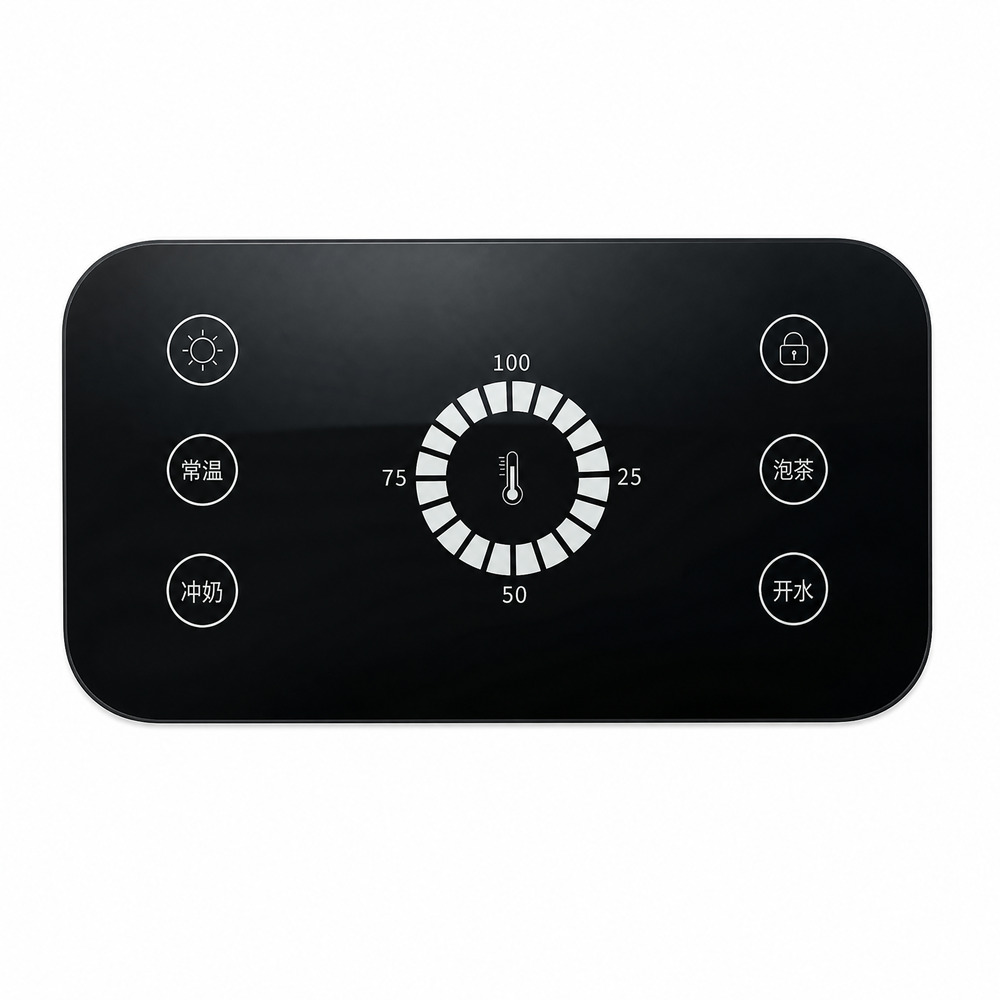
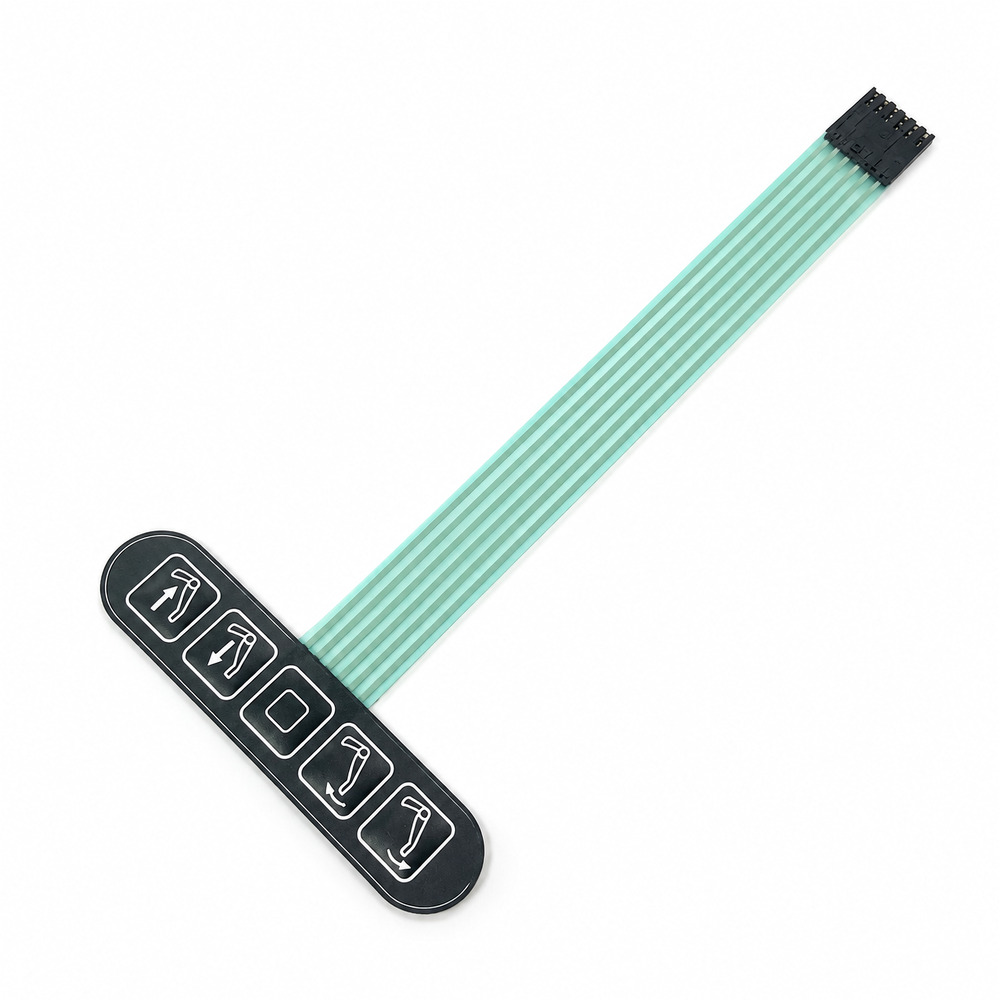
A comprehensive examination of stack-up mechanics, substrate physics, and conductive interconnect topologies for systems design engineers and B2B strategic procurement teams.
The human-interfacing boundary layer demands precise polymer selection based on operating environment. Biaxially oriented Polyethylene Terephthalate (PET, such as MacDermid Autotex) provides superior chemical resilience against industrial degreasers, ketones, and isopropyl sanitizers, alongside mechanical flex endurance exceeding 5 million switch cycles. Conversely, Polycarbonate (PC, such as SABIC Lexan 8010) offers high impact resistance, optical clarity up to 92%, and UL94 V-0 flame ratings, making it ideal for stationary indoor consoles and medical diagnostics.
The electrical path determines current capacity, impedance stability, and component density. Flexible Printed Silver (PET Screen-Printed) remains the global baseline for cost efficiency, operating with trace resistances between 10Ω and 100Ω. For demanding applications requiring dense pitch (<0.5mm), soldered active components, or severe vibration, Flexible Printed Circuits (FPC Polyimide with etched rolled-annealed copper) deliver trace impedances <1Ω. Where structural self-support is required, rigid FR4 PCB backers integrate terminal headers, relays, and microcontrollers directly into the panel sub-assembly.
Delamination and moisture intrusion represent over 80% of field failures in non-standard front panels. Implementing continuous closed-loop acrylic transfer adhesives—such as 3M 467MP (2.3 mil) for mirror-smooth powder-coated metal or 3M 300LSE / 9472LE (5.0 mil) for low-surface-energy (LSE) molded plastics (polypropylene, ABS)—prevents edge lift under thermal cycling (-40°C to +85°C). Incorporating specialized perimeter gas-venting channels prevents internal barometric pressure buildup while maintaining certified IP67 ingress protection against submersed hydrostatic pressures.
Cross-analyze tactical engineering trade-offs, mechanical feedback ratios, tooling overhead, and production MOQs before issuing Requests for Quotation (RFQs).
| Technology Platform | Actuation Travel & Force | Tactile Feedback Ratio | Rated Operating Life | Tooling & Setup Cost | Optimum Industry Application |
|---|---|---|---|---|---|
| Stainless Steel Metal Dome | 0.3mm – 0.8mm 200g – 450g Force |
Sharp, Crisp Click (Tactile Ratio 45–65%) |
>1,000,000 actuations | Moderate (Etch/Die Tooling) | Defibrillators, CNC Machining Centers, Rugged Avionics |
| Thermoformed Polydome (PET) | 0.2mm – 0.5mm 150g – 300g Force |
Soft Muted Snap (Tactile Ratio 25–35%) |
>500,000 actuations | Low to Moderate (Heat Emboss) | Commercial Kitchen Appliances, Vending, HVAC Thermostats |
| Capacitive Touch (Solid-State) | Zero Mechanical Travel 0g Touch Force |
Audible Beeper / LED Flash (Virtual Software Haptics) |
>10,000,000 touches (No Moving Parts) |
Moderate (Electrode Artwork) | Sterile Hospital ICU Suites, Consumer Smart Panels, Wet Dispensers |
| Compression-Molded Silicone | 1.0mm – 2.5mm 80g – 220g Force |
Deep Cushion Stroke (Travel Dependent) |
>1,500,000 actuations | Higher (Steel Compression Mold) | Mining Handhelds, Military Walkie-Talkies, Marine GPS Navigators |
| Rigid FR4 Backer Membrane | 0.4mm – 0.6mm 250g – 350g Force |
Crisp Tactile Click (Integrated Dome Arrays) |
>2,000,000 actuations | Moderate to High (PCB Drill/Route) | Heavy Industrial Motor Inverters, Automotive Diagnostics, Telematics |
How global supply chain volatility, functional integration, and sustainability mandates are reshaping front panel specifications for industrial and medical equipment.
Traditional utilitarian switchboards are rapidly being superseded by unified, seamless glass-like surfaces. OEM design teams are mandating "dead-front" engineering, wherein control icons and alphanumeric legends remain completely invisible until triggered by user proximity or power activation. This trend requires high-opacity selective blackout screen printing coupled with ultra-thin Light Guide Films (LGF) that channel SMD LED illumination uniformly without hotspot bleeding, delivering automotive-grade cockpit ergonomics to industrial appliances.
European Union directives including REACH Annex XVII, RoHS 3 (Directive 2015/863), and prospective Digital Product Passport (DPP) regulations are putting immense scrutiny on composite layered assemblies. The market is shifting from multi-polymer composites (e.g., PC overlay bonded to PET circuits via rubber-based adhesives) toward mono-material assemblies utilizing single-origin oriented polyester systems and solvent-free waterborne conductive inks, dramatically simplifying post-consumer disassembly and scrap processing.
The boundary between discrete switches and analog continuous sensors is dissolving. Modern equipment front panels increasingly integrate printed thin-film force-sensing matrices alongside digital metal dome arrays. By applying specialized carbon nanoparticle inks, panels can detect dual-stage activation (e.g., light touch to illuminate, firm squeeze to engage critical safety locks), significantly mitigating accidental actuation hazards in high-risk surgery theaters and aerospace instrumentation consoles.
Direct from our 12,000 m² integrated plant in Fenggang Town, Dongguan—engineering and exporting mission-critical interface assemblies since 2003.
Founded in 2003, Dongguan Ravo Electronics Co., Ltd. has developed from a precision silkscreen workshop into a vertically integrated OEM/ODM human-machine interface powerhouse. Unlike contract assembly brokers, Ravo conducts 100% of critical manufacturing processes under one roof—from cleanroom screen printing and digital vector color matching to precision CNC laser cutting, pneumatic embossing, and automated surface-mount LED pick-and-place.
Our facility houses Class 1,000 and Class 10,000 cleanrooms specifically maintained to eliminate microscopic particulate contamination during graphic window and transparent electrode lamination. Every production lot undergoes automated computerized pin-to-pin resistance mapping, Hi-Pot insulation breakdown tests, and 500,000-cycle mechanical actuator stress audits before export release.
In-depth technical answers addressing engineering constraints, lead times, regulatory compliance, and cost optimization for sourcing managers.
Connect directly with Dongguan Ravo’s senior HMI engineering team. Submit your 2D/3D drawings, artwork sketches, or custom specifications and receive a comprehensive DFM manufacturability audit, layer stack recommendation, and competitive export quotation within 2 hours.
